The Formula You Need
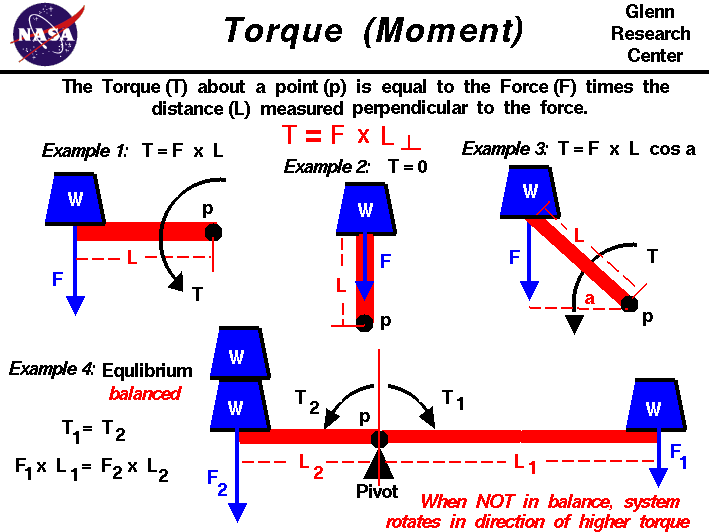
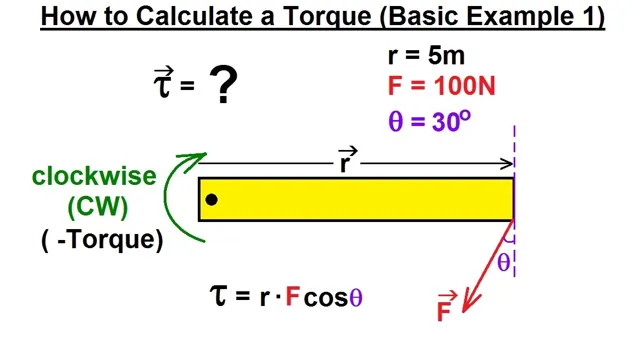
Torque is force applied at a distance from a pivot point. The basic equation is simple enough: torque equals force multiplied by the perpendicular distance from the axis of rotation to where the force is applied. That distance is what mechanics call the moment arm, and the unit you'll use depends on your system. Metric runs newton-meters or Newton-millimeters. Imperial goes pound-feet or inch-pounds. Pick one and stick with it, because mixing them mid-calculation is how people end up with bolts that are either dangerously loose or stripped because someone applied 40 foot-pounds when the spec called for 40 inch-pounds. The straightforward case looks like this. You have a wrench, you apply a known force at the end of the handle, and the handle length gives you the moment arm. Multiply them together and you have your torque. But here is the thing most guides skip: the force has to be applied perpendicular to the lever arm. If you're pushing at an angle, you need to factor in the sine of that angle. So the full equation becomes torque equals force times distance times the sine of the angle between the force vector and the lever arm. When the angle is 90 degrees, sine is 1 and the equation collapses back to the simple version. When the angle drops, you're getting less torque than you think, which is why everyone eventually learns to pull straight on a wrench instead of at some awkward diagonal. I learned that the hard way on a timing cover application a few years back. The service manual specified 15 newton-meters for a series of fasteners arranged around an aluminum housing. I had a digital torque wrench set to 15, pulled smoothly, and the readout confirmed it. Two weeks later the cover leaked. Turns out I was pulling at about a 75-degree angle the whole time because the workspace was tight and the wrench handle kept bumping against the block. The actual torque on those fasteners was closer to 14.5 newton-meters. Not a huge difference on paper, but in a sealing application where you're right at the edge of the clamp load window, 0.5 newton-meters is the difference between a seal that holds and one weeps oil after three months. I started using a universal joint extension to get the pull angle back to 90 degrees, and the leaks stopped. It took about 10 seconds to rig the joint and cost me roughly four dollars in parts.
There are other cases where the calculation gets messier. When you're dealing with rotating systems rather than static fastener applications, torque connects to angular acceleration through the moment of inertia. The equation becomes torque equals moment of inertia times angular acceleration. Moment of inertia is basically the rotational equivalent of mass, and it depends on how the mass is distributed relative to the axis of rotation. A solid disk and a hoop with the same mass will have very different moments of inertia, which means they require different torques to achieve the same angular acceleration. This matters if you're sizing a motor for anything with rotating components.
Common Pitfalls That Waste Time and Parts
One issue that comes up constantly is friction. When you're torquing a bolt, only a fraction of the applied torque actually creates clamp load. The rest is eaten by friction at the threads and under the bolt head. In dry conditions, roughly 55 percent of your torque goes to under-head friction and 45 percent to thread friction. When you apply a lubricant or use a coating like nickel plating, that distribution shifts and the total friction drops significantly. The practical result is that two bolts torqued to the same value can produce very different clamp loads depending on whether one was dry and the other was oiled. I once saw a assembly line where the torque specs changed by 20 percent between dry and lubricated fasteners on the same component, and nobody had updated the work instructions. They were producing parts that met torque values but failed load tests because the actual clamp force was off. Another thing people miss is temperature. Fastener torque values shift with temperature because thermal expansion changes the geometry of the joint and the material properties change. If you torque a bolt at room temperature and then the assembly goes into service at 150 degrees Celsius, the clamp load can drop by 10 to 15 percent depending on the materials involved. Aluminum bolts on steel housings are especially sensitive because aluminum expands more than steel. I worked on an engine build where the heads were torqued cold to spec and then during the heat cycle the clamp load dropped enough to blow the head gasket on break-in. The fix was a multi-stage torquing procedure that accounted for the thermal growth differential, adding a final check torque after the first heat cycle. Yield control torquing is worth mentioning because it's standard practice on many modern engines but completely misunderstood by people who haven't worked with it. Instead of targeting a specific torque value, you torque to a yield point where the bolt stretches plastically. The procedure usually involves a snug torque followed by an angle turn, like 60 degrees past initial contact. This gives much more consistent clamp load than pure torque control because the stretch of the bolt directly correlates to the clamp force, regardless of friction variations. The downside is that yield bolts are single-use. Once they've been stretched past their elastic limit, they won't hold the same clamping force when reused. I've seen mechanics reuse them because the part cost a few dollars each, and it always ends badly when the bolt relaxes under load and the joint separates.
Get the Full Details

If you need to calculate torque for an electric motor, the relationship between power, speed, and torque is more useful than the force-distance definition. Torque in newton-meters equals 9.5488 times power in kilowatts divided by speed in RPM. The constant 9.5488 comes from the unit conversions between watts, radians, and minutes. This is the equation you'll use when matching a motor to a load or verifying that a motor can handle the required torque at a given speed. Keep in mind that motors have a continuous torque rating and a peak torque rating, and the peak is only sustainable for short durations before thermal limits kick in. Running a motor at peak torque continuously will overheat it within minutes depending on the cooling design. The thermal time constant varies by motor size and type, but as a rough guide, a small NEMA frame motor might reach thermal equilibrium in 10 to 15 minutes while a large industrial motor could take an hour or more.
Tools and Accuracy Expectations
For manual fastener work, click-type torque wrenches are the standard tool and they're accurate to about plus or minus 4 percent when used correctly and within their specified range. Digital wrenches can hit 2 to 3 percent accuracy but need battery maintenance and periodic calibration. Beam-style wrenches are cheap and durable but harder to read precisely, which is why they're mostly used for rough work or as reference tools. Calibrated torque multiplication setups exist for high-torque applications where a single wrench can't reach the required value, but they introduce their own error margins and complexity that usually isn't worth the trouble unless you're working at several hundred foot-pounds regularly. Calibration interval matters more than most people realize. A torque wrench that's been dropped or used near its maximum capacity will drift. The general industry standard is annual calibration for critical applications, but if you're using a wrench daily on production work, six-month intervals are more realistic. Some shops calibrate every three months for aerospace and medical device work. The cost of calibration is usually between 50 and 150 dollars per wrench depending on the shop and the accuracy level required. Neglecting it is how you end up with a wrench that reads 15 newton-meters when it's actually delivering 17 or 13.
When Torque Calculation Isn't the Right Approach
Sometimes you should skip torque measurement entirely and use a different method. Hydraulic tensioners are the go-to alternative for large fasteners where torque wrenches become impractical. A tensioner stretches the bolt hydraulically, you spin the nut to the seated position, and then release the pressure. The bolt snaps back into tension and the clamp load is determined by the hydraulic pressure and the bolt's effective stress area, not by friction. This eliminates the friction uncertainty that plagues torque-based methods and gives you clamp load accuracy in the 3 percent range compared to 25 to 30 percent for standard torque control. The equipment costs more upfront, but for flange connections on pressure vessels or large bearing housings, it's the only method that produces repeatable results. Ultrasonic measurement is another option worth knowing about. Some bolt manufacturers offer ultrasonic transducers that measure the actual stretched length of the bolt under load. Since elongation is directly proportional to clamp force and independent of friction, this gives you the most accurate reading available without invasive testing. The equipment is expensive and the transducers need to be matched to specific bolt sizes and grades, so it's mostly used in high-value applications like wind turbine main shafts or large compressor assemblies where a failed bolt can mean weeks of downtime and six figures in repair costs. The bottom line is that calculating torque is straightforward when you understand what the variables actually represent and what the limitations of your measurement method are. Most mistakes don't come from bad math. They come from applying a torque value to a situation where friction, angle, temperature, or material behavior makes that value meaningless without adjustment. Factor those in before you turn the wrench.