Knifemaking is mostly heat and patience
You buy a piece of steel, you grind it into a shape, you heat treat it, and then you grind it again. That's basically it for the whole process. The parts you can't rush are the ones that actually matter. Getting the edge right and keeping the temper consistent takes more time than most people expect when they first try to figure out How To Make Handmade Knives. I'll walk you through what actually happens on the bench. Most beginners pick 1095 or 5160 because they're cheap and available at any auto parts store. These are good steels for learning. I used to run 1084 O1 from a tool and die supplier, which cost about $12 for a bar that would make two or three knives. The real question isn't what steel to use, it's what you're building the knife for. A kitchen knife needs a different heat treat than a fixed blade hunting knife, even if both are made from the same blank. If you want something that holds an edge longer, look at 154CM or CPM-3V. They cost more per pound but they take less time to sharpen in the field. For a first batch, stick with 1095. It forgives mistakes in the heat treat phase. I've seen people destroy 154CM by overheating it during their second attempt. 1095 just laughs at that.
Grinding the blank
You can start with a reciprocating saw to cut the rough outline from sheet stock, usually between .062 and .125 inches thick depending on the knife design. A band saw with a 3 TPI hook tooth makes cleaner cuts and stays on line better. Transfer your template with a marker or scribe, then cut within about a quarter inch of the line. You'll remove that margin during grinding. For the bevels, most people use a bench grinder first and then move to a belt sander. I started on a 6-inch bench grinder with a 36-grit wheel and switched to a 4x36 belt sander with 80-grit for the final bevel work. The bench grinder removes material fast but leaves deep scratches that take forever to clean up on the belt. My workaround is to skip the bench grinder entirely and go straight to the belt sander on 60-grit. It takes about twice as long but the finish is already halfway done when you're at the bevel stage. Saves me maybe forty minutes per knife on cleanup. Keep the steel cool. If it turns blue or straw-colored while you're grinding, you've started drawing the temper and ruined that section. Dip it in water every thirty seconds or so. I learned this the hard way on a batch of five 5160 blades where I ground too hot and three of them came out unevenly hardened. Wasted about $40 in stock and a morning.
Heat treating
This is where the actual transformation happens. You need an oven or a forge that can hold a steady temperature. A kitchen oven works fine for most knife steels. You heat the blade to its critical temperature, hold it there until the steel is uniformly heated, then quench it in oil. For 1095, the critical temperature is around 1450 to 1500 degrees Fahrenheit. A magnetic test can tell you when you're close: if a magnet stops sticking to the steel, you're near the Curie point, which for 1095 is roughly in that range. I use a laser thermometer for accuracy but the magnet trick is what I rely on when the thermometer acts up. It works about 90 percent of the time and saves you from a guess-and-check cycle. Auscultemp or liquid indicator paint makes this way more reliable than guesswork. You buy the small bottles online for about eight dollars. Paint it on, heat the blade, and when the paint melts at the exact right temperature, you know you're ready. This alone prevented me from warping my last six blades in a row. Before that, I was eyeballing the color and fighting with warpage.
Get the Full Details

Quenching is done in 10W30 motor oil or canola oil. The oil should be around 120 to 130 degrees F when you start. Cold oil shocks the steel too much and increases the chance of cracking. Warm it on a stove or in the oven before use. Agitate the blade gently as you lower it into the oil. Don't slam it in. Move it back and forth for about thirty seconds, then let it sit until it stops bubbling. Usually takes two to three minutes total.
Straightening and tempering
Almost every blade warps slightly during quenching. You'll notice it immediately when you pull it out. A common fix is the pipe vise method. Heat the curved area of the blade with a propane torch until it's about 400 degrees, then clamp it between the jaws of a pipe vise and apply gentle pressure to straighten it. Work in small increments. Overcorrect by about a thousandth of an inch and you'll get it close enough. After straightening, you temper the blade to reduce brittleness. Place the knife in an oven at 350 to 400 degrees F for two hours. This brings the hardness down from around 62 to 64 HRC to a more usable 58 to 60 HRC. For a kitchen knife, 58 is ideal. For a survival-style fixed blade, you can go up to 60. Harder doesn't always mean better. A blade at 62 HRC will chip if you use it as a prying tool. This is something I only learned after chipping the edge off a 1095 hunting knife I'd made at full hardness and then taking it hiking. Never again.
Grinding the bevel final
Once the blade is tempered and straight, you go back to the belt sander and work through progressively finer grits. 80, 120, 220, 320, 400. Each step removes the scratches from the previous one. You're not trying to polish here, you're establishing a clean, even bevel. If the bevel looks fuzzy under a bright light, you skipped a grit or didn't remove enough material. The bevel angle matters more than most makers admit. For a general-purpose knife, 20 to 25 degrees per side is standard. Lower angles cut better but edge durability drops. I set my jigs for 22 degrees on most of my blades. It's a compromise that works for everything from slicing vegetables to light batoning.

Tang and handle construction
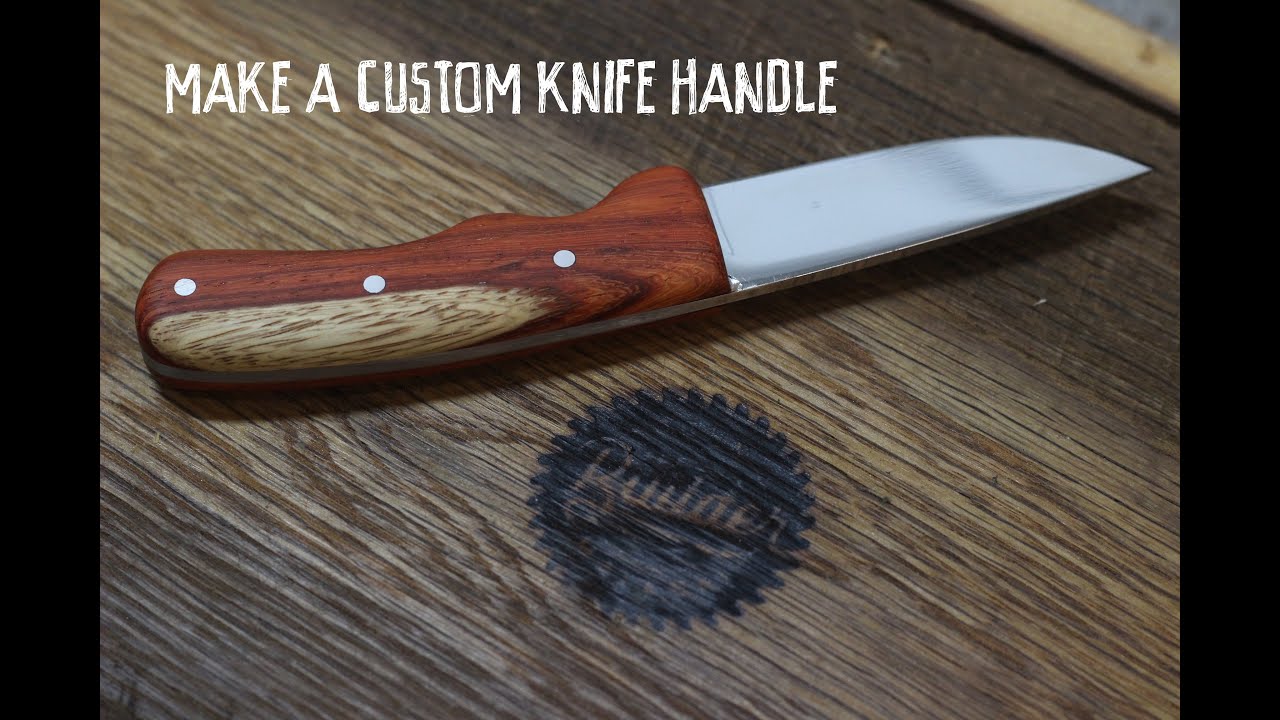
The tang is the part of the blade that extends into the handle. Full tang means the metal runs the full width and length of the handle. Stub tang is shorter and narrower, usually pinned or epoxied in place. Full tang is stronger and easier to balance but requires more work to shape the handle scales. I make full tang blades because they feel solid in the hand and they don't fail under normal use. For handle material, stabilized hardwood, micarta, and G10 are the most common. Stabilized walnut looks nice and machines well. Micarta is tough and handles moisture better than wood. G10 is basically layers of fiberglass cloth in epoxy. It's the most durable option but doesn't have the aesthetic appeal of wood. Pick based on what you actually need the knife to do. I use a drill press and Forstner bits to shape the handle cavities, then clamp the scales with epoxy. A few stainless bolts threaded into the tang keep things secure. The epoxy cures in about twenty-four hours at room temperature. Don't rush this step. If you file the handle while the epoxy is still soft, everything shifts and you end up with gaps that collect dirt.
Edge finishing
This is where the knife becomes functional. You can use the belt sander with a fine grit to establish the initial edge, then finish on sharpening stones or a guided system. I use a Wicked Edge for consistency. It takes about ten minutes to put a working edge on a blade, compared to maybe twenty minutes by hand on stones if you're careful. The guided system costs more upfront but pays for itself if you're making more than a few knives. A razor edge at 20 degrees per side will cut paper cleanly. If it's dragging, you haven't removed the burr completely. Flip the blade and check for a burr along the entire edge with your fingernail. If it catches, you need to go back to a finer grit on the sander or spend more time on the stone. This burr removal step is where most beginners fail. They stop too early and call it done.
Common problems and why they happen
Warping during heat treat is the most common issue. It comes from uneven cooling or holding the blade in the oil at an angle. Keep the blade perpendicular to the oil surface and move it steadily. If you still get warpage, it's usually a sign your temperature was too high or you didn't soak long enough for the cross-section thickness. Cracking is rare but catastrophic. It almost always happens when the steel is too hot during quenching or the oil is too cold. I cracked a 5160 blade once by dropping it into room temperature canola oil from 1550 degrees. The thermal shock created a hairline fracture near the spine. It showed up two weeks later when I was using the knife. Never happened again since I preheat the oil. If you're making knives consistently, investing in a temp-controlled heat treat oven pays for itself quickly. I picked up a used kiln controller on eBay for about sixty dollars and wired it to a standard oven element. Temperature swings are now within plus or minus fifteen degrees instead of the wide fluctuations a regular kitchen oven produces. That consistency matters more than anything else in the process.

The whole process from blank to finished knife takes about six to eight hours for a first attempt. Most of that time is waiting for the oven to heat and cool. Active work time is roughly two hours split across the days. You can do it in one sitting but splitting it up gives you time to check things like straightness and edge alignment without rushing. Rushing is what ruins the batches.


