Working With IEEE 841 Motor Standards and Baldor Documentation
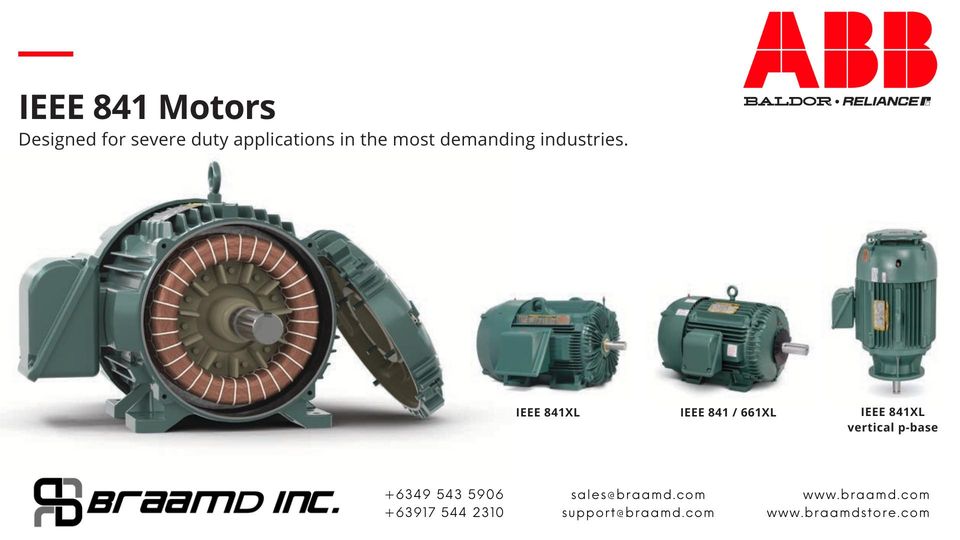
IEEE 841 covers totally enclosed fan cooled induction motors designed for premium efficiency and demanding industrial environments. It specifies performance requirements, testing procedures, and material standards that go beyond what NEMA MG-1 mandates. If you're specifying motors for hazardous locations, chemical plants, or continuous-duty applications, this is the standard that matters. Baldor built a significant portion of its industrial motor line around this standard before the company changed hands a couple of times. The standard defines minimum efficiency levels, temperature rise limits, vibration criteria, and insulation system requirements for TEFC motors in the frame sizes it covers. It also addresses bearing currents, shaft grounding, and paint/coating systems for corrosive environments. The key difference from NEMA standards is that IEEE 841 motors are held to tighter tolerances across the board. Efficiency at full load and partial load is tracked more rigorously. Temperature class ratings follow a different measurement methodology. The insulation system must withstand longer life cycles under thermal stress. When Baldor published their technical papers on IEEE 841 compliance, they typically walked through their manufacturing process, the testing protocols they ran, and how their motor designs achieved the required efficiency tiers. These papers were useful because they showed real test data rather than theoretical numbers. Baldor's approach to frame size 364 and above, for example, involved specific lamination designs and copper winding configurations that deserved the higher efficiency categories. Their papers documented the actual no-load and full-load losses measured during production testing.
Where to Find the Original Papers and Current Spec Sheets
The original Baldor-branded IEEE 841 technical papers are scattered across a few sources. Some are hosted on the IEEE Xplore digital library under the IEEE Petroleum and Chemical Industry Committee publications. Others ended up on Baldor's old technical documentation portal, which is no longer active after the ownership transitions. You'll find surviving copies on university engineering library repositories, particularly at schools with strong electrical engineering programs that maintained industrial motor research groups. For current Baldor motors, Nidec (which acquired the North American industrial motor business from ABB) hosts updated spec sheets and compliance documentation on their product portal. The numbering system shifted slightly after the acquisition, but the IEEE 841 compliance markings remain consistent on the motor nameplates. Look for the IEEE 841 trademark statement on the data plate. It should list the frame size, temperature rise class, insulation class, and the efficiency tier achieved during testing. If you need the historical Baldor papers specifically, the IEEE Standards Association website sometimes has older committee publications available for download. The PCIC (Petroleum and Chemical Industry Committee) annual conference proceedings from the mid-2000s through early 2010s contain several Baldor-authored papers on IEEE 841 motor performance and application practices. These are often the most practically useful documents because they address real installation and maintenance problems rather than just laboratory test results.
How to Specify and Verify IEEE 841 Compliance
When you're writing a specification, don't just write "IEEE 841 compliant" and move on. The standard has multiple efficiency tiers and several optional requirements that significantly affect motor performance in the field. You need to specify the exact frame size range, the insulation temperature class (usually Class F or Class H for IEEE 841 applications), the bearing type, and whether shaft grounding is required. Also specify the paint system if the motor will operate in a corrosive environment, because IEEE 841 defines coating standards that general-purpose NEMA motors don't meet. Verification is where people tend to cut corners. Receiving a motor with an IEEE 841 nameplate doesn't guarantee the unit passed all the required tests. The standard requires both design validation testing and production routine testing. Design validation involves testing a representative sample unit through a full battery of procedures including thermal testing, impedance testing, and efficiency mapping across the load range. Production routine testing covers high-potential dielectric strength, resistance measurements, and vibration checks on every individual motor produced. I once had a situation where a supplier shipped motors labeled as IEEE 841 compliant but the nameplate temperature rise was listed at 80 degrees Celsius when the specification called for 90 degrees or less. The efficiency numbers checked out on paper, but the thermal performance was degraded. The workaround was to pull three units from the shipment and run independent thermal testing using resistance method measurements under rated load. Two of the three failed the temperature rise requirement by about 7 degrees. We rejected the entire lot and required the supplier to provide documented test reports from an accredited lab before reshipping. That experience took about three weeks and cost us a production delay, but it saved us from installing motors that would have failed within two years in a continuous-duty application.
Get the Full Details

Common Pitfalls When Applying These Motors
One thing that catches people off guard is the torque characteristics. IEEE 841 motors are optimized for efficiency, which sometimes means reduced breakdown torque compared to a general-purpose NEMA Design B motor of the same frame and horsepower. If your application involves high inertia loads or frequent starts under load, the reduced torque margin can be a problem. Always check the torque slip curve in the manufacturer's published data, not just the nameplate horsepower and RPM. Another issue is the bearing arrangement. IEEE 841 specifications often call for enhanced bearing systems to handle the longer expected service life. But if you're replacing an older general-purpose motor with an IEEE 841 unit in an existing drive setup, the bearing sizing and lubrication requirements may differ. I've seen cases where someone swapped in a Baldor IEEE 841 motor into a position that previously used a NEMA premium efficient motor, and the new motor's bearing lubrication intervals didn't match the existing maintenance schedule. The motor itself was fine, but the maintenance team wasn't aware of the different relubrication requirements and either over-lubricated or under-lubricated the bearings. Check the maintenance section of the installation manual before you commit to the swap. VFD compatibility is another area where the standard doesn't cover everything. IEEE 841 specifies requirements for motors operated from AC power sources, but variable frequency drive operation introduces voltage spikes and common-mode currents that the base standard doesn't address in detail. If you're running an IEEE 841 motor on a VFD, you need to verify that the insulation system is rated for inverter duty. Most Baldor IEEE 841 motors in the current production line are inverter-ready, but older stock from before 2010 may not have the reinforced insulation needed. Check the motor's serial number against the manufacturer's database or request a written confirmation of inverter duty compatibility before installation.
Reading the Test Reports Correctly
When you receive the IEEE 841 test report from the manufacturer, focus on the right sections. The efficiency values at 25%, 50%, 75%, and 100% load are the ones that matter for your energy cost calculations. Don't just look at full-load efficiency. A motor that runs mostly at partial load will perform very differently depending on its partial-load efficiency curve. The temperature rise data should include both the resistance method and the thermocouple method if the report follows the standard closely. Discrepancies between the two methods can indicate uneven heating or airflow issues inside the motor. The no-load current and power factor at no load are also worth reviewing. These numbers tell you about the magnetic circuit design and the quality of the laminations. Abnormally high no-load current in an IEEE 841 motor can indicate core losses that are higher than they should be, which directly impacts efficiency at light load conditions. The standard sets limits on these values, and manufacturers that cut corners on core material quality will show up in the test data even if the full-load efficiency number looks acceptable. If you're evaluating multiple vendors for a large purchase, comparing their IEEE 841 test reports side by side is one of the most effective ways to identify which manufacturer is actually delivering premium performance versus which one is meeting the standard at the minimum acceptable level. The differences between vendors at the high end of the efficiency range are often small, maybe half a percentage point, but over the life of the motor in a continuous-duty application, that difference translates to meaningful energy costs. For a 200 horsepower motor running 8,000 hours per year at 75% load, a 0.5 percentage point efficiency difference is roughly 3,600 kilowatt-hours per year, or about $360 at typical industrial electricity rates. Over ten years, that's a significant amount.