What Actually Happens in a Chemical Process
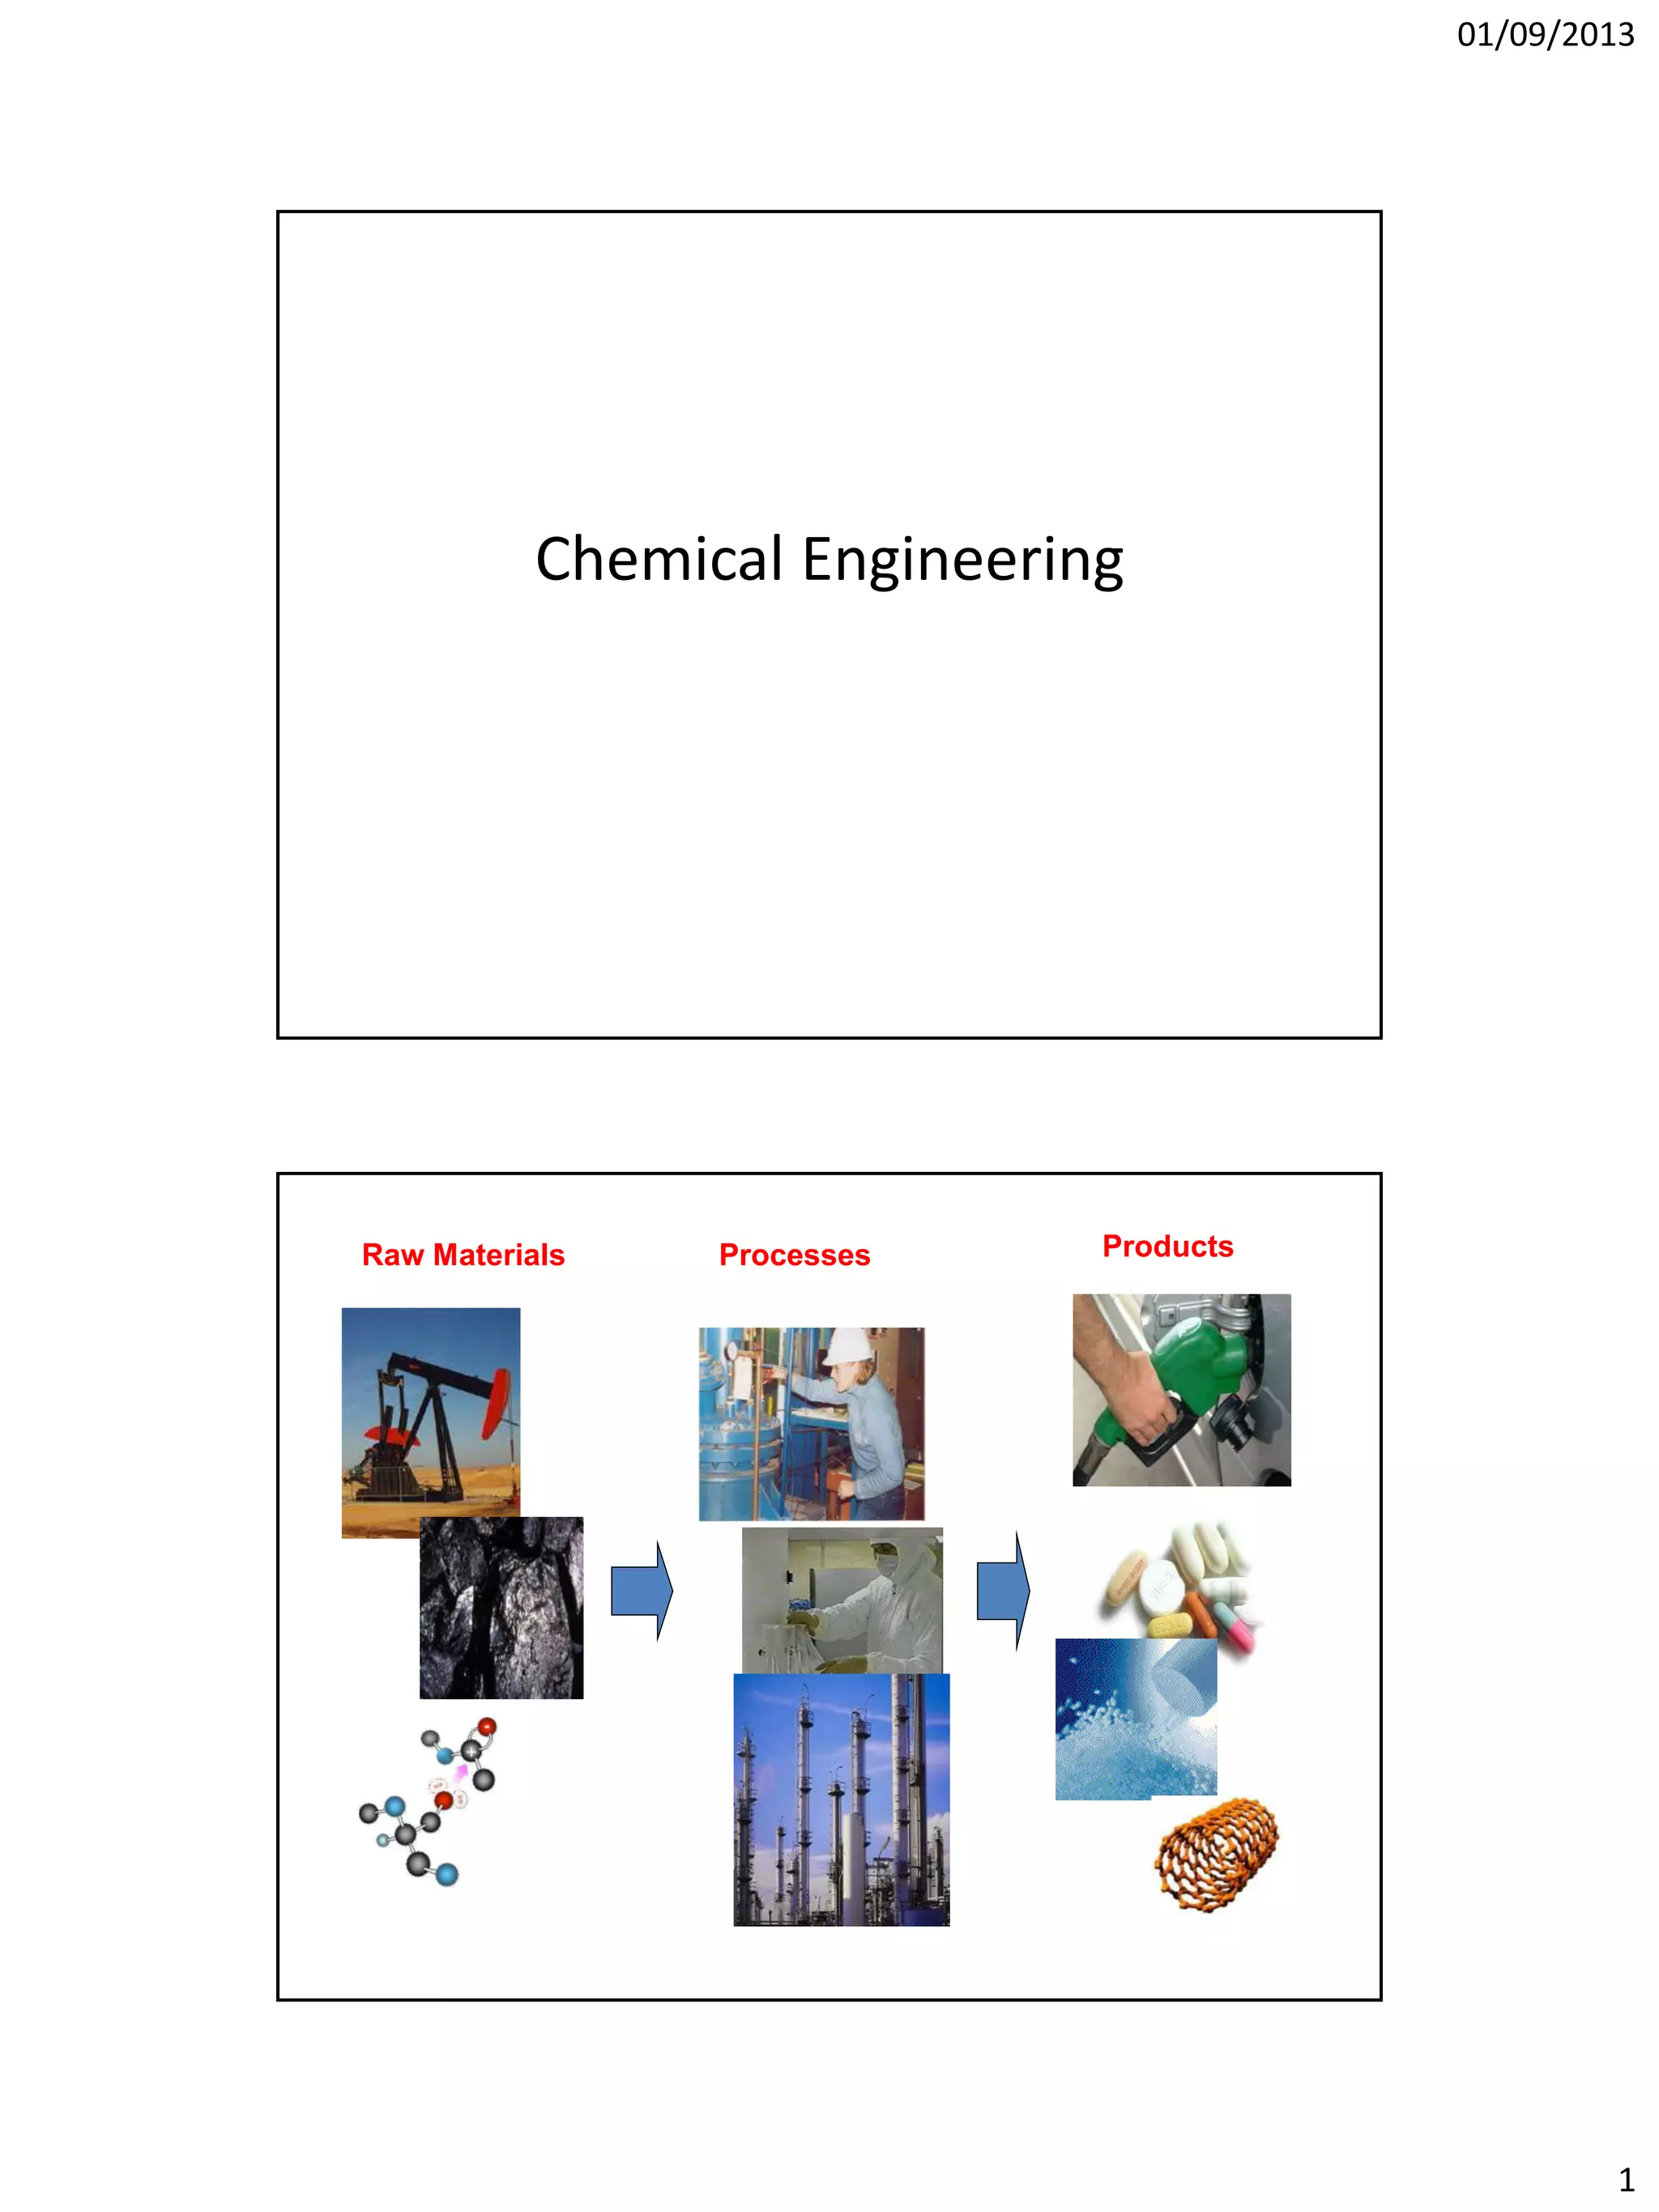
When you walk onto a plant floor, the first thing you notice is noise and heat. Everything you see is just matter moving from one state to another. Feeds go in, products come out, and somewhere in between, things get hot, cold, pressurized, or separated. That is essentially what Introduction To Chemical Engineering Processes is about: understanding how mass and energy move through a system so you can predict what comes out the other end.The foundational skill is the material balance. It sounds simple because the concept is trivial. Input equals output plus accumulation. But the moment you try to apply it to a real distillation column with recycle streams, the algebra stops being clean. I spent three days once chasing a vapor-liquid equilibrium calculation on a crude distillation unit because the initial composition assumption was off by 0.3 percent. That 0.3 percent created a 12-degree temperature drift across the column. The fix was recalculating the feed preheater duty with actual flowmeter data instead of trusting the design specification sheet. You do not need a advanced math degree to grasp the basics. What you need is the ability to draw a box around a system, label every stream that enters and leaves, and write down what you know about each one. Start there. The rest is iteration. Material balances track every component entering, leaving, accumulating, or reacting within a defined boundary. You write one balance for each chemical species if reactions occur, or one overall balance when you are tracking total mass only. The degrees of freedom check tells you whether your problem is solvable before you waste time solving equations that will never close.
Energy balances account for enthalpy changes from temperature shifts, phase transitions, and reaction heat. The common mistake people make here is ignoring kinetic and potential energy terms when they actually matter. In high-pressure gas systems, the kinetic energy contribution can shift your heat exchanger sizing by enough to change the equipment specification entirely. For liquid systems at low velocity, you can safely drop those terms. Know which regime you are in. Phase equilibria determine how components distribute themselves between vapor, liquid, and sometimes solid phases. Raoult's law works fine for ideal mixtures. Most real mixtures are not ideal. The van Laar, Wilson, NRTL, and UNIQUAC models handle non-ideality. Pick the one that matches your system's behavior. Using Raoult's law for an ethanol-water system will give you results that look reasonable until you compare them to actual operating data, then they fall apart completely. One thing nobody tells beginners about recycle streams is that they amplify small measurement errors across the entire loop. I once worked on a process simulation where the recycle ratio was so high that a 1 percent error in the separator efficiency propagated into a 15 percent error in product purity. The workaround was adding a purge stream specification and iterating on the separator performance curve until the simulation stabilized. Without the purge, the model would never converge no matter how many adjustment cycles you ran.
Unit Operations Are Where Theory Meets Hardware
A distillation column is not just a tall metal cylinder. It is a device that exploits differences in volatility to separate components. The number of theoretical stages, the reflux ratio, and the feed location all interact in ways that are easy to misjudge if you treat them as independent variables. Lowering the reflux ratio saves energy but costs separation efficiency. Raising it improves purity but increases reboiler duty. The optimal point sits somewhere in the middle and depends entirely on your feed composition and your product specifications. Heat exchangers follow the same logic. The LMTD method works for simple counter-current or parallel-flow arrangements. Cross-flow and shell-and-tube configurations require correction factors that complicate the calculation. I learned this the hard way when I sized a shell-and-tube exchanger using the basic LMTD formula without applying the correction factor. The actual required surface area ended up being roughly 40 percent larger than my initial calculation. The workaround was switching to the epsilon-NTU method, which handles complex flow arrangements more naturally. Momentum transfer and fluid flow are where the math gets ugly fast. Pipeline pressure drops depend on Reynolds number, pipe roughness, fitting losses, and elevation changes. The Darcy-Weisbach equation gives you the friction factor, but getting the friction factor requires either an iterative solution or a good approximation like the Swamee-Jain equation. Using the Hazen-Williams formula for water in a large-diameter steel pipe at high velocity introduces significant error because it was calibrated for different conditions.
Get the Full Details

Common Pitfalls That Waste Time
The biggest mistake I see people make is treating steady-state assumptions as universally applicable. Real processes drift. Feed compositions change. Ambient temperature shifts. A controller reacts. If you only simulate the nominal condition, your design will fail the moment anything deviates from that point. Run sensitivity analyses on at least two or three key variables. It usually takes maybe thirty minutes and catches problems that would otherwise surface during commissioning when they cost far more to fix. Another frequent error is neglecting the energy requirement of pumps and compressors when doing material balances. Mass balance alone does not tell you whether your pump can actually move the fluid through the system at the required rate. You need to tie the hydraulic calculations into your process model. A pump curve intersects with a system curve at the operating point. Find that intersection before you size the motor. Solving large systems of simultaneous equations by hand is impractical and unnecessary. Spreadsheet solvers, MATLAB, Python with NumPy, or dedicated process simulation software like Aspen Plus and ChemCAD handle the heavy lifting. The software will not save you if your process flowsheet is wrong. Garbage in, garbage out still applies. Validate your model against published data or pilot-scale results whenever possible. If you cannot find published data, run a simplified analytical calculation by hand and compare it to the software output. If they disagree, you have found a bug in your model setup.
There is also a tendency to trust convergence too quickly. A simulation converging does not mean it is correct. It just means the solver found a mathematical solution. Whether that solution is physically meaningful is a separate question. Check your residuals, verify that all balances close within acceptable tolerance, and confirm that temperature and pressure profiles are monotonic where they should be. Non-monotonic profiles often indicate numerical issues or an incorrect thermodynamic model.
How to Practice This Stuff Without Breaking Anything
Start with simple single-unit problems. A flash drum. A single-stage extractor. A heater. Get comfortable writing balances and checking degrees of freedom. Then add complexity gradually. A column with a condenser and reboiler. A reactor with recycle. A network of heat exchangers. Each addition tests a different skill. Use real data whenever you can find it. Manufacturer datasheets, process manuals, and published case studies contain actual numbers. Working with real numbers forces you to confront the messiness that textbooks smooth over. The numbers in a textbook problem are usually chosen to give clean answers. Real process data rarely cooperates. If you have access to a plant, spend time on the floor. Read the nameplate data on vessels and equipment. Look at the control panels. Notice where the operators adjust set points and why. The gap between a textbook flowsheet and an operating plant is where most learning happens. The textbook shows you the design intent. The plant shows you the reality.

Thermodynamic property packages matter more than most beginners realize. The same process modeled with different property methods can give significantly different results. Peng-Robinson and Soave-Redlich-Kwong work well for hydrocarbon systems with moderate pressure. NRTL or UNIQUAAC are better for highly non-ideal liquid mixtures. If you are modeling a system with water and organic compounds, make sure your chosen package handles aqueous chemistry appropriately. Using a generic package for a specialty chemical process is a reliable way to get results that look plausible but are practically useless. The field moves fast. New separation technologies emerge regularly. Membrane processes, supercritical extraction, and reactive distillation are areas where traditional approaches are being challenged. Keep up with recent literature and industry conferences. The concepts you learn in an introductory course are permanent, but the tools and techniques evolve. Understanding the fundamentals lets you adapt when the tools change.