What Actually Happens When Operations And Supply Chain Go Wrong
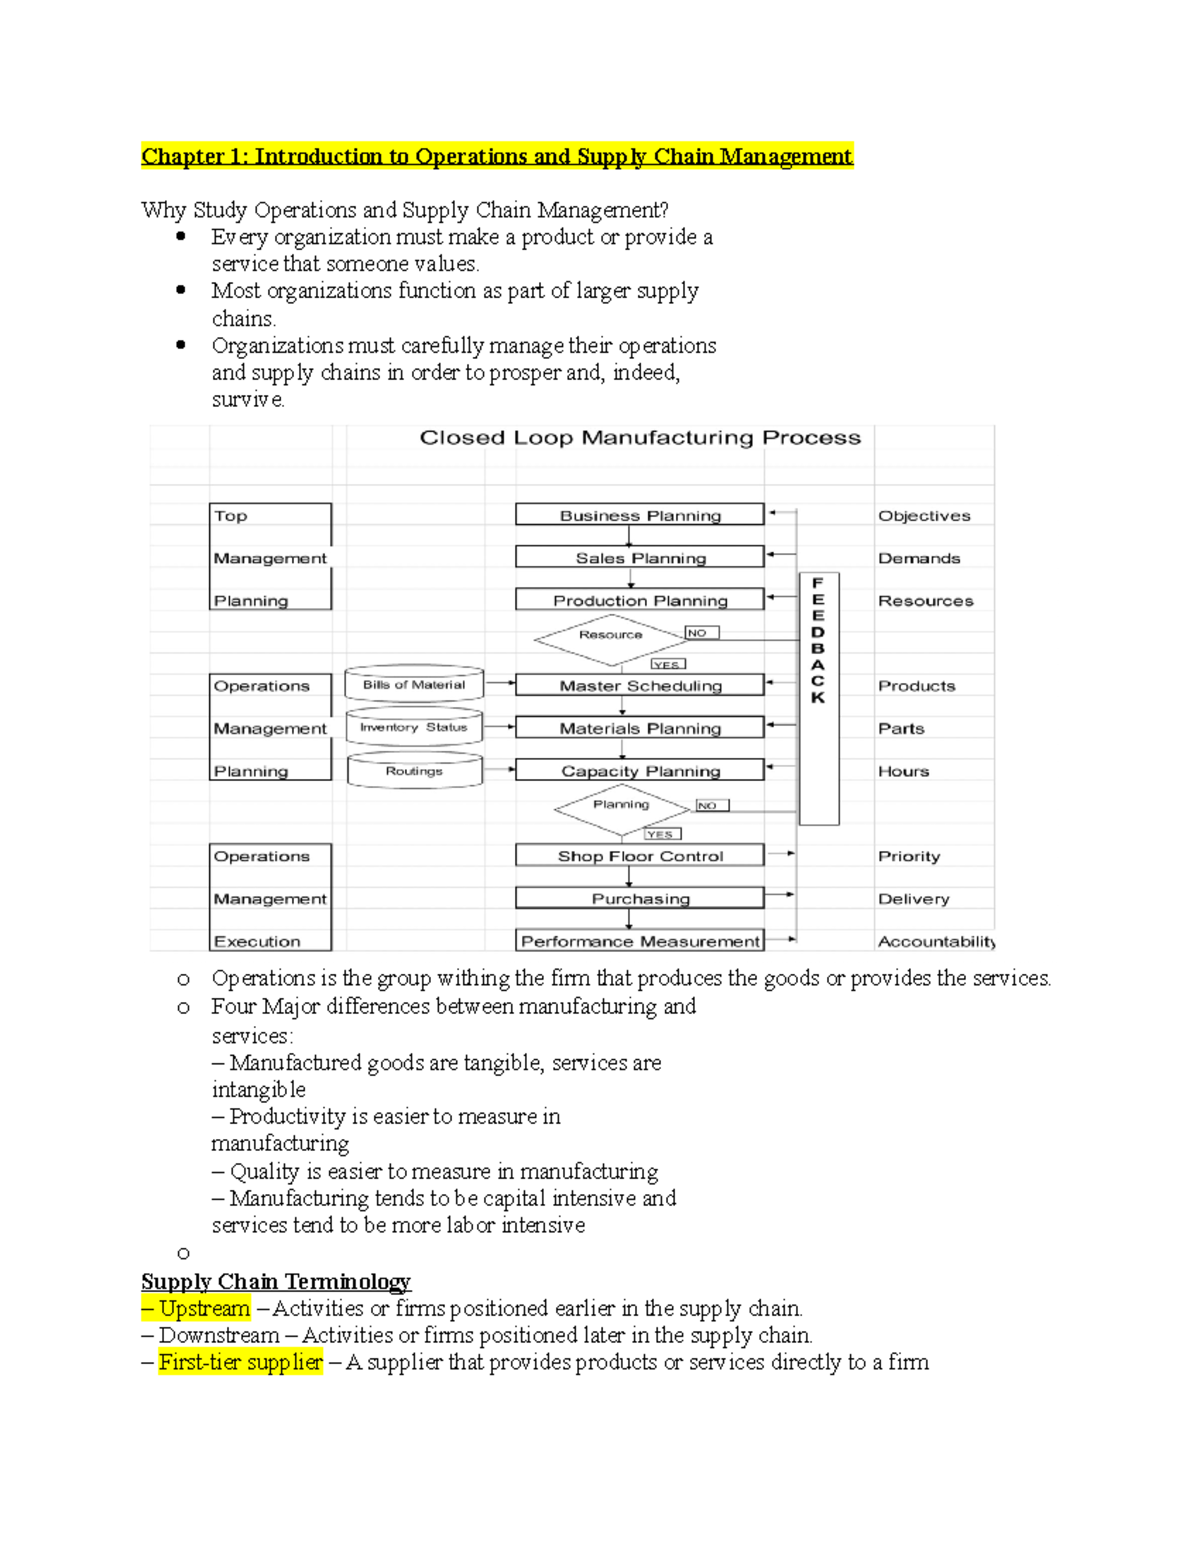
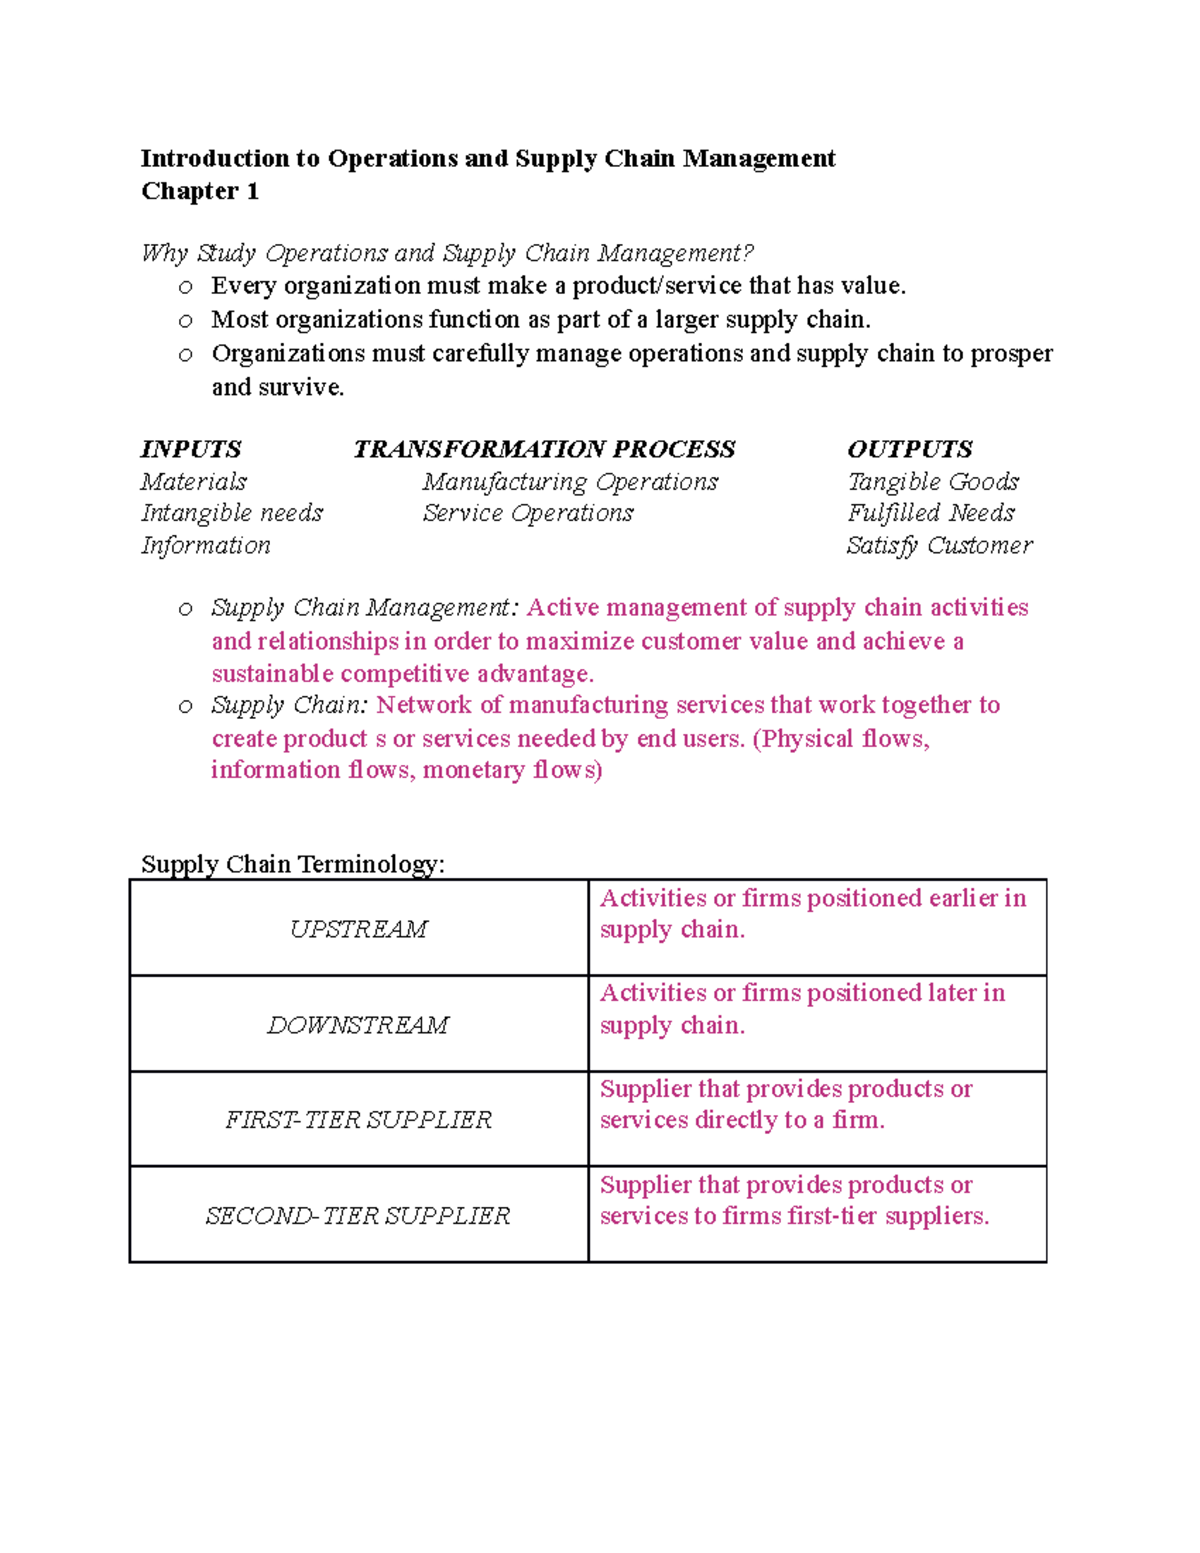
I spent three years managing inventory for a regional distributor that moved everything from HVAC parts to commercial kitchen equipment. The textbook version of operations and supply chain management sounds clean. It isn't. The actual work involves constant fire drills disguised as routine decisions, people who will not believe you when you tell them the numbers are wrong, and systems that break in exactly the ways you never predicted. This is a practical guide to understanding what the field actually requires, not what a slide deck says it requires. Operations management covers the internal side of producing goods or services. Supply chain management covers everything outside the four walls — suppliers, logistics, distributors, retailers, and the movement of materials between all of them. In practice these two functions overlap so heavily that most companies run them as a single department. The distinction exists on paper. It rarely exists in the workplace. Start with the basic loop: plan, source, make, deliver, return. That is the SCOR framework, the standard model used across the industry. Plan means forecasting demand and matching it to capacity. Source means selecting suppliers and negotiating terms. Make covers the transformation process — scheduling, quality control, throughput optimization. Deliver is order fulfillment and last-mile logistics. Return handles reverse logistics, which nobody budgets for adequately until they have a product recall or a seasonally saturated returns department.
The first thing beginners miss is that every link in that loop creates constraints elsewhere. Optimizing one area almost always degrades another. You reduce inventory costs by ordering less frequently, then stockouts spike and customer service tickets triple. You speed up production by running longer batches, then work-in-progress piles up and cash flow tightens. There is no free optimization. Every improvement has a tax attached to it. I learned this the hard way in year two when we switched a supplier from domestic to overseas to save twelve percent on unit cost. The savings were real on paper. What the spreadsheet did not capture was the three-week variance in lead time, the customs holds that added unexpected duties, and the phone calls at 6 AM on Thursdays because a container got routed through a port that had just shut down for a labor strike. We ended up holding forty percent more safety stock than before and still experienced more stockouts than the previous arrangement. The lesson was not that international sourcing is bad. It is that the visible costs are easy to model and the hidden costs are almost impossible to predict without operating in that environment first.
Core Concepts That Matter In Practice
Forecasting is the engine of operations, and almost every company uses it poorly. The most common approach is naive extrapolation — take last year's numbers and adjust up or down by a guessed percentage. This works fine when the business is stable and the product line does not change. It fails catastrophically during market shifts, new product launches, or supply disruptions. A better approach combines quantitative methods like exponential smoothing or ARIMA models with qualitative input from sales teams who actually talk to customers. The hybrid method is messier but significantly more accurate. I ran forecasts using a weighted moving average adjusted monthly by regional sales input, and our accuracy improved from roughly sixty-two percent to about seventy-eight percent over six months. Not perfect. Worthwhile. Inventory management is where most operational budgets bleed. The economic order quantity model, EOQ, gives you a theoretical optimal order size based on holding costs and ordering costs. The formula is straightforward. Real life rarely matches the assumptions. Demand is not constant. Lead times are not fixed. Storage space is not unlimited. I implemented EOQ-based reorder points for a category of high-turnover parts and reduced average inventory by twenty-two percent in the first quarter. By the third quarter, we were back to the original levels plus a new buffer because the model could not account for a sudden supplier capacity constraint that caused random batch shortages. Use EOQ as a starting framework, not a final answer. Layer in safety stock calculations based on actual demand variability, not estimates. Standard deviation of lead time demand is the metric that matters, and most companies do not track it. Capacity planning determines whether you can actually fulfill what you have sold. The bottleneck concept from the Theory of Constraints is the most useful tool here. Identify the single slowest point in your process, and everything else is secondary. I worked at a facility where management kept trying to improve throughput at every station except the actual bottleneck, which was a single CNC machine with a forty-minute cycle time. We added workers to six other departments, invested in faster equipment upstream, and restructured shift patterns. Nothing moved the needle until we added a second shift to the bottleneck machine. Only then did overall output increase by thirty-one percent. The counter-intuitive truth is that improving non-bottleneck resources is usually a waste of money. It feels productive. It is not.
Get the Full Details
Quality management in operations is not about inspection. Inspection catches defects after they exist. Quality management is about designing processes that make defects unlikely. Statistical process control, SPC, uses control charts to detect variation before it becomes a defect. The difference between common cause variation and special cause variation determines whether you fix the system or fix the symptom. Most companies treat every outlier as special cause and launch expensive investigations, when the data would show it was just normal system noise. I inherited a line where the quality team rejected nearly four percent of output and spent weeks investigating each rejection. We ran a control chart analysis and found that sixty-three percent of those "failures" fell within normal statistical bounds. The reject rate dropped to under one percent without changing any equipment or training. The process had been fine. The judgment criteria had been broken.
Supply Chain Specifics That Are Not Obvious
Procurement strategy is often reduced to price negotiation. That is a narrow view. Total cost of ownership, TCO, includes price, transportation, tariffs, quality rejects, payment terms, lead time reliability, and the cost of switching suppliers. A supplier charging fifteen percent less per unit may be more expensive overall if their on-time delivery rate is eighty-two percent instead of ninety-seven percent and their quality rejection rate is triple. I evaluated three suppliers for a critical component using a weighted TCO model. The cheapest bidder ranked third. The mid-range supplier ranked first when transportation, duty, and expected defect costs were included. We awarded the contract to the mid-range supplier and saved approximately eight percent on total landed cost within two quarters. Logistics network design determines where you place warehouses, distribution centers, and cross-dock facilities. This is a location-allocation problem that most companies solve through intuition and lease availability rather than mathematical optimization. Gravity models and mixed-integer programming can find near-optimal configurations, but the data required is substantial. I built a simplified model using a spreadsheet solver for a client considering a new regional warehouse. The model suggested a location that saved an estimated fourteen percent in annual transportation costs compared to their existing setup. The recommended site was in a rural area with limited carrier availability and no backup warehouse nearby. We modified the recommendation to a secondary site that cost three percent more in transport but had dual-carrier access and was twenty minutes from an existing partner facility. The model gave a good answer. The real-world decision required adjusting for risk factors the model could not quantify. Demand sensing is an advanced technique that uses real-time data — point-of-sale feeds, web traffic, social signals, weather data — to adjust forecasts faster than traditional methods allow. Traditional forecasting operates on weekly or monthly cycles. Demand sensing can adjust daily. Retailers like Walmart and Target use this at scale. Smaller companies often lack the data infrastructure to implement it effectively. The barrier is usually not the algorithm but the data pipeline. If your POS system does not export in real time or your ERP cannot ingest external data sources, demand sensing is not practical. Start with improving data latency and integration before attempting advanced forecasting techniques. Garbage in, garbage out applies with maximum severity here.
Reverse logistics is the most neglected area of supply chain management. Returns processing, refurbishment, recycling, and disposal are treated as a cost center rather than a strategic function. E-commerce has made this area critical. Return rates for online apparel retail average between twenty and thirty-five percent. That is not a small problem. It is a massive flow of products moving backward through the supply chain that most companies are poorly equipped to handle. I designed a returns processing workflow for a mid-sized electronics retailer that reduced average returns processing time from five days to fourteen hours and recovered approximately eighteen percent of returned inventory value through grading and remarketing. The key was separating returned items into three streams immediately upon receipt: resellable, refurbishable, and salvage. Most companies put all returns into one bin and sort them weeks later, by which point perishable value has expired and inventory has gone obsolete.
Tools You Actually Need
Enterprise resource planning systems like SAP, Oracle, or Microsoft Dynamics cover most of the core functions. They are expensive, complex to implement, and often configured poorly. A badly configured ERP is worse than no ERP because it creates false confidence in data that is systematically wrong. If you are evaluating an ERP, insist on a trial period where your actual transactions run through the system alongside your current process. Compare outputs for at least sixty days before committing. The implementation phase is where most projects fail. Budget twice the time and three times the cost that your initial estimate suggests. This is not pessimism. It is the pattern I have observed across multiple implementations. For smaller operations, Excel with Power Query and Solver can handle a surprising amount of analytical work. I have built demand forecasting models, inventory optimization tools, and logistics routing calculators entirely in spreadsheets for companies that could not justify an ERP. The limitation is scalability. When you exceed a certain transaction volume or complexity threshold, spreadsheet-based solutions become fragile and error-prone. Know when to migrate. The warning signs are delayed file performance, manual workarounds for features the tool cannot handle, and data integrity issues that require reconciliation. Supply chain management software like Kinaxis, Blue Yonder, or o9 Solutions provides advanced planning capabilities including multi-echelon inventory optimization, simulation, and scenario planning. These tools are powerful but require skilled users. A badly operated SCP system produces badly optimized plans. Training and change management are as important as the software itself. I worked with a company that installed an SCP module and expected it to replace their planning team. Six months later, they had reverted to manual planning because the system outputs conflicted with operational reality and nobody understood how to adjust the parameters. The tool was not the problem. The expectation was.
Where This Field Falls Apart
Operations and supply chain management cannot solve structural problems. If your product design is flawed, no amount of process optimization will make it profitable. If your market has declined, efficient delivery of an obsolete product is still a losing strategy. I have seen companies invest heavily in lean manufacturing, Six Sigma, and supply chain digitization while their core value proposition eroded. The operational improvements masked the decline temporarily but could not prevent it. Optimize within your strategy. Do not expect optimization to replace strategy. Certain industries resist standard supply chain approaches. Custom fabrication, made-to-order manufacturing, and project-based operations do not fit well into forecast-driven models. Push-based supply chains fail in environments where demand is truly heterogeneous and unpredictable. In those cases, a pull-based or hybrid approach is necessary, but pull systems require different capabilities — flexible capacity, responsive suppliers, shorter lead times — that many organizations do not possess. Attempting to implement pull manufacturing without the supporting infrastructure creates chaos, not efficiency. The biggest limitation of most operations frameworks is their assumption of stability. Real supply chains operate in volatile environments. A framework that works in normal conditions may collapse during disruption. The 2020 pandemic exposed this weakness across every industry. Companies with rigid, optimized supply chains suffered more than those with intentional redundancy. The lesson was not that efficiency is bad. It is that efficiency without resilience creates fragility. The optimal level of inventory is not zero. The optimal lead time is not as short as possible. There is a tradeoff curve, and most companies pushed themselves too far along it before the disruption hit.
If you are entering this field, start by understanding the basics thoroughly before adopting advanced tools or methodologies. Learn to read a balance sheet and understand how inventory valuation affects it. Learn to calculate carrying costs accurately. Learn to distinguish between correlation and causation in operational data. These fundamentals matter more than any certification or software package. The field rewards people who understand the underlying mechanics over people who can operate complex tools without understanding what the tools are doing.