Emergency Stop and E-Stop on Industrial Machinery: What Actually Works
I spent years getting people to buy into the idea that a big red mushroom-head button is a safety device. It isn't. The whole system around it is what matters, and Iso 13850 2015 Safety Of Machinery Emergency Stop is the document that spells it out. You can bolt whatever you want to a panel, but if the surrounding circuitry doesn't meet certain requirements, you have a paper shield at best. The standard covers emergency stop functions for machinery. It was updated in 2015 to better align with ISO 13850, which itself ties into ISO 12100 (risk assessment) and the broader machinery directive framework. The core premise is straightforward: an emergency stop must be a single action from the operator that initiates a path to stop risk from continuing or re-emerging. But "straightforward" doesn't mean simple, and that's where people go wrong in the field. Key requirements from the standard:
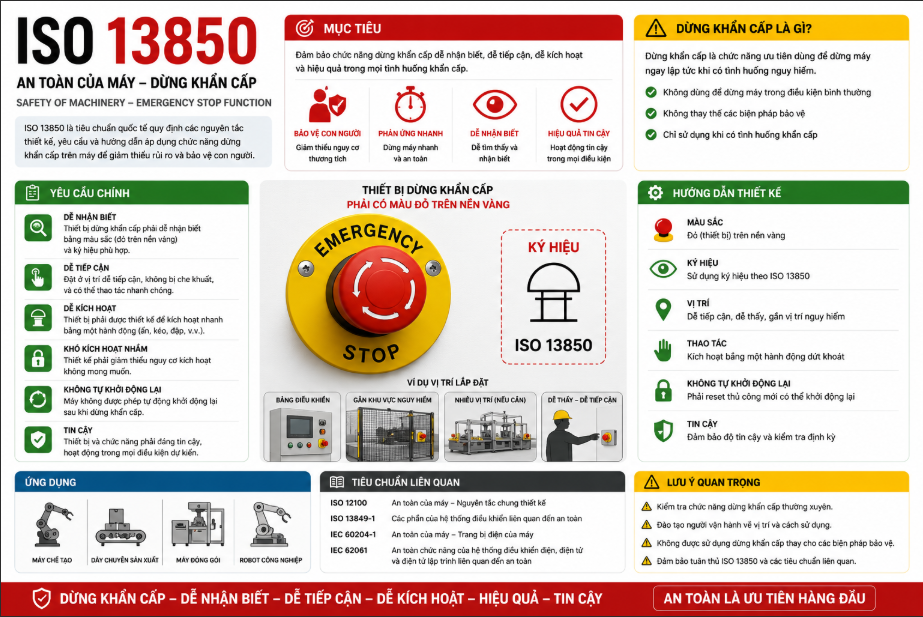
- One-action function: The operator must be able to initiate the E-stop in a single motion. No sequences, no menu diving.
- Direct mechanical or electronic path: The signal must not go through a regular PLC scan cycle before initiating the stop unless specific conditions are met. That means hardwired relays or safety PLCs with monitored channels are the norm.
- Holding on: Once activated, the E-stop must remain latched until deliberately reset. A momentary release or power loss cannot cancel it.
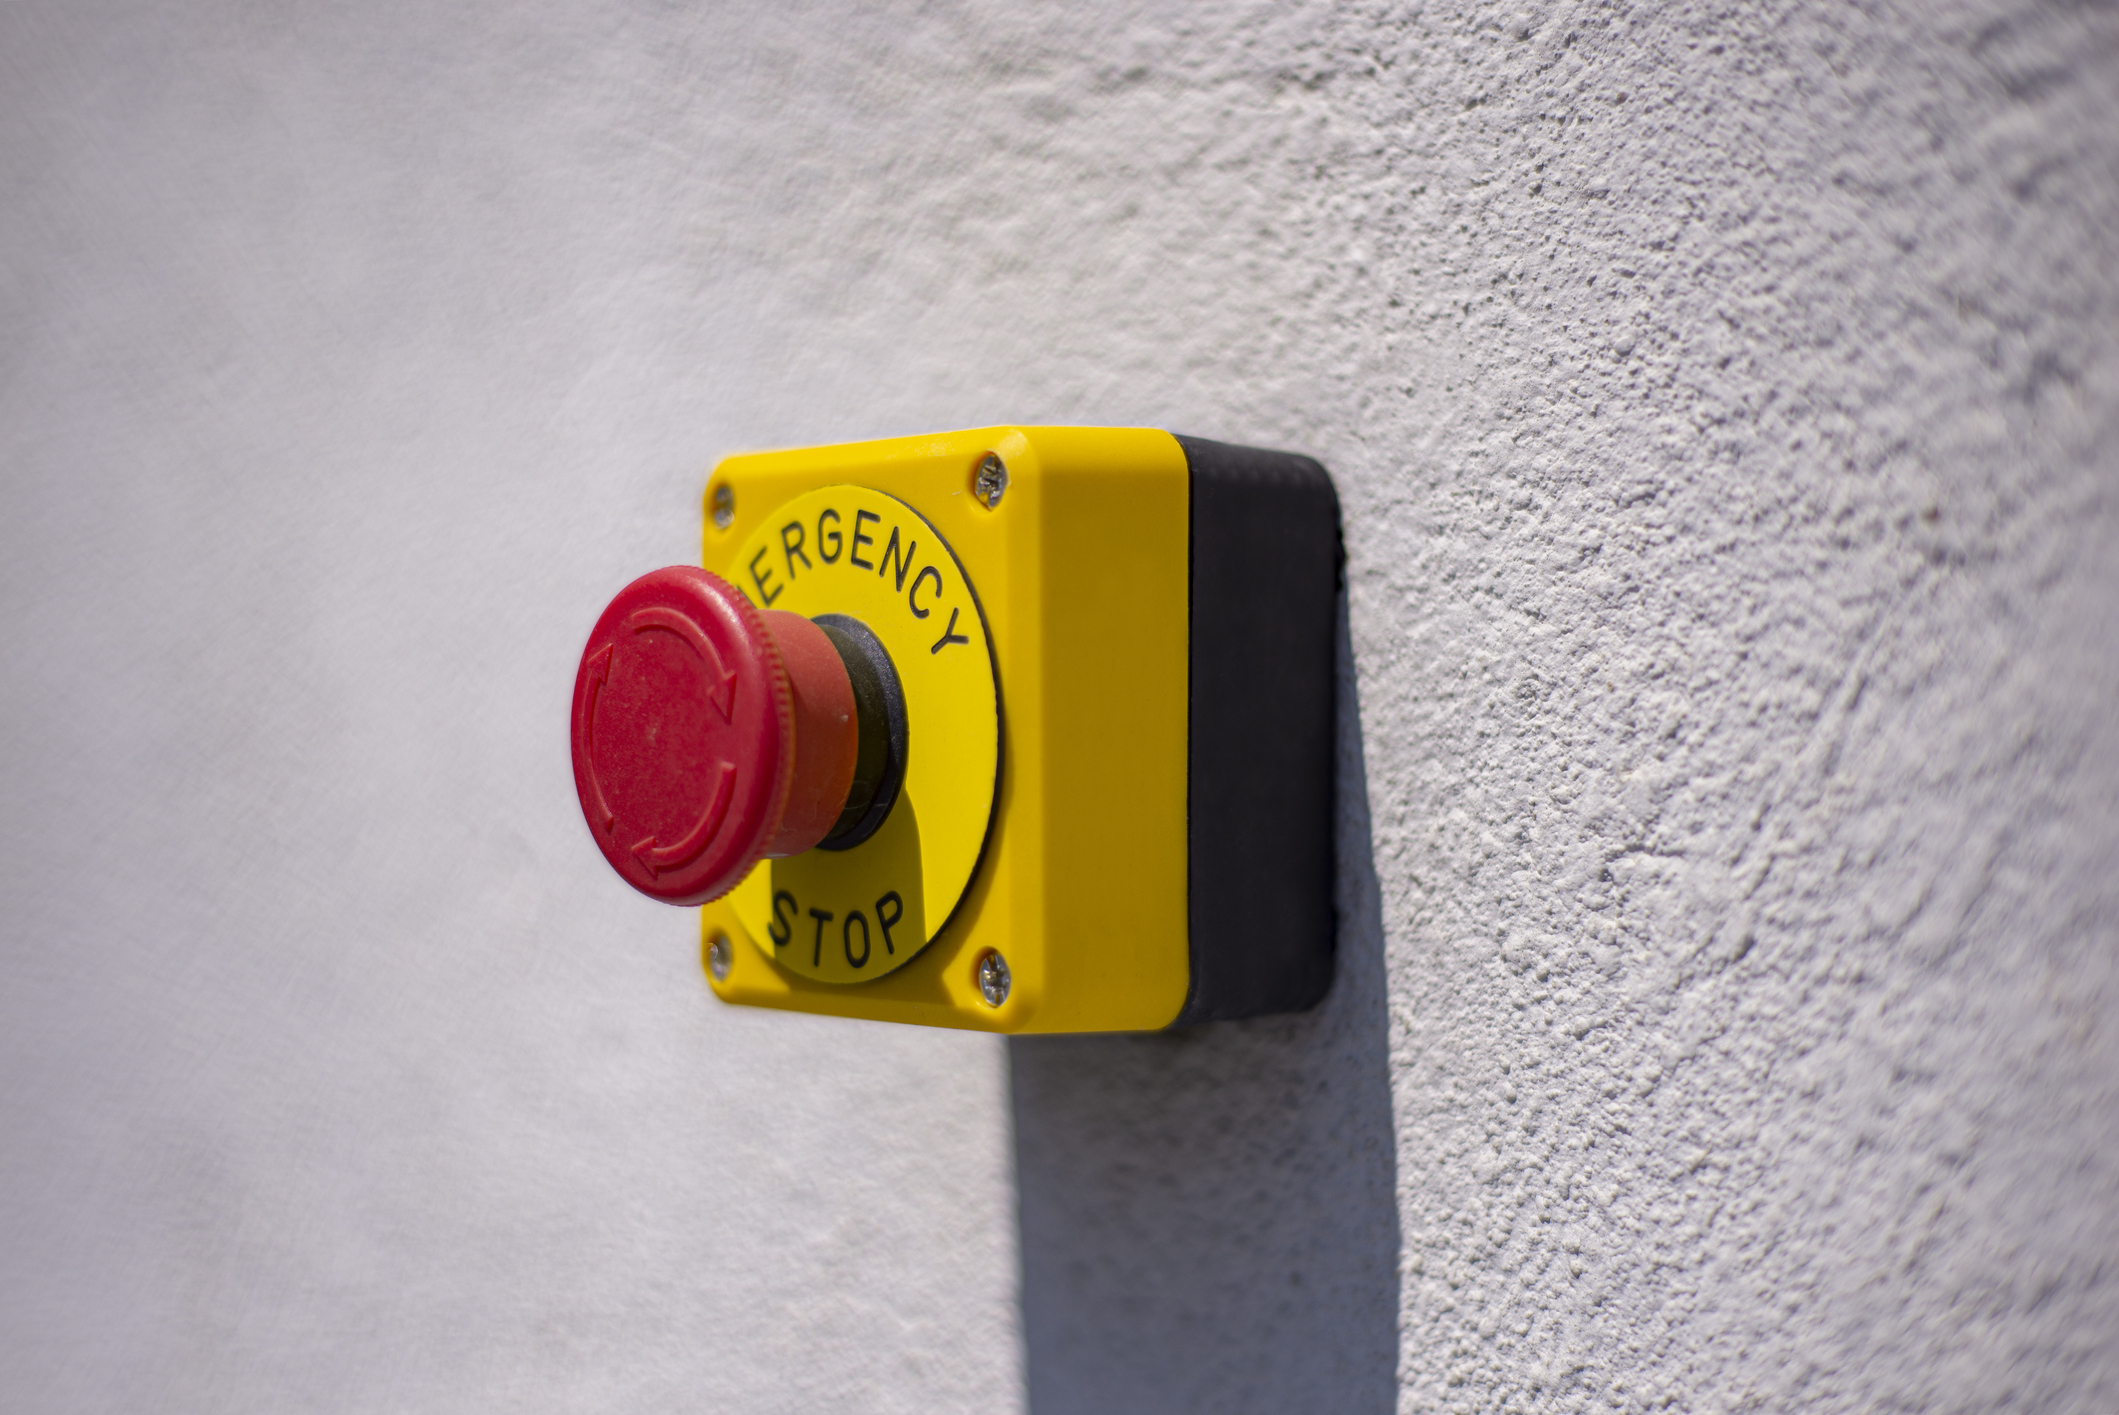
- Visual indication: The actuator must show its state. Red on yellow background, standard colors per ISO 13850 / IEC 60204-1.
- Restart is a deliberate sequence: Resetting an E-stop does not restart the machine. You press reset, then you go through a fresh startup cycle.
Here is the practical part that most people gloss over. Iso 13850 2015 is about function, not just the hardware box on the wall. The safety-related control system feeding the E-stop must achieve a certain performance level (PLr) or safety integrity level (SIL). That means redundancy, cross-checking, and fault detection. A single relay dropping out can fail open and leave the system thinking everything is fine when it is not. That is a classic latent failure mode, and auditors will call it out during a machine safety review. I worked on a packaging line retrofit where the original equipment manufacturer had wired a single-channel contactor-based E-stop circuit. It met the basic "red button stops the machine" requirement on paper. But the contactor coil was on the same phase as a variable frequency drive that caused voltage dips every time it ramped. The contactor would dropout during normal operation, the machine would stop randomly, and the operators would just reset it. The machine was "stopping," yes, but the diagnostic coverage was zero. We ended up replacing the entire safety circuit with a dual-channel safety relay module with cross-monitoring. The random stops went away, and more importantly, the system could now detect a single-point fault and go into a safe state instead of pretending everything was operational. Common pitfalls I see repeatedly:
Using general-purpose relays instead of safety-rated relays. A standard relay might do the same thing functionally, but it lacks the required fault detection and containment. The difference is regulatory and practical. When a certification body comes in, they will ask for type-examined components with a proven track record in safety applications. Ignoring the category of the control circuit. ISO 13850 doesn't specify categories directly, but it references ISO 13849-1, which does. Category 0 means uncontrolled stop (power removed), Category 1 means controlled stop then power removal. Your choice depends on the hazard analysis. A cutting saw needs a different category than a conveyor. People often default to Category 0 because it is simpler, but that might not be the right answer for every machine. Failing to account for E-stop placement. The standard requires E-stop controls to be positioned within easy reach of the operator's normal working position, and additional stations may be needed at hazardous points. I once saw a welding cell where the E-stop was mounted on a control panel that required the operator to walk past the weld torch to reach it. That is a violation waiting to happen. You need to map the reach envelope based on actual operator posture, not idealized diagrams.
Get the Full Details
Testing and validation: After installation, you need to verify the function. This isn't a checkbox exercise. Test the E-stop at every station. Confirm that it holds when power is cycled. Check that reset requires a separate action. Verify that the indicator lamp works. Run the system through a full stop cycle and measure the actual stopping distance and time against your risk assessment. If the E-stop triggers but the machine keeps moving past the expected point, you have a problem with either the stopping category selection or the mechanical braking system. Document everything. Not for the paperwork, but because six months from now when something goes wrong, you will need to prove that the system was designed and tested to the standard. I have seen companies lose years of insurance coverage because they couldn't produce test records. The cost of documentation is nothing compared to the cost of regret.
Where Iso 13850 2015 falls short: The standard covers the function well, but it does not address every modern scenario. It was written before collaborative robots and AI-driven adaptive systems became common. If you are integrating a robot that changes its path based on sensor input, the E-stop logic needs to account for dynamic hazards, not just static ones. The standard also doesn't say much about cyber aspects of safety systems. A safety PLC can be compromised by a network attack if it isn't properly segmented. That is outside the scope of 13850 and requires additional measures under IEC 62443 or equivalent guidance. There is also the question of maintainability. Safety systems degrade. Contacts weld. Springs fatigue. Insulation breaks down. The standard assumes a baseline of maintenance, but it doesn't prescribe how often you should inspect or test. That is left to the machine builder and the operator's risk assessment. A good practice is annual functional testing of every E-stop station with a calibrated timer, plus visual inspection at intervals dictated by the operating environment. Harsh environments—high vibration, temperature extremes, corrosive atmospheres—require more frequent checks.
If you need the full standard, it is available through ISO's member bodies or national standards organizations like BSI, DIN, or ANSI. It is not free, and it costs more if you want the English version from multiple sources. The cost is justified if you are designing or certifying machinery, but for learning purposes, the relevant excerpts are often summarized in IEC 60204-1 and ISO 13849-1 documentation, which are more accessible. The bottom line is that Iso 13850 2015 Safety Of Machinery Emergency Stop is a functional standard, not a hardware catalog. It tells you what the system must do and the principles behind it. It does not hand you a shopping list of components. You still need to do the engineering, the testing, and the documentation. Anyone who tells you otherwise is selling something.