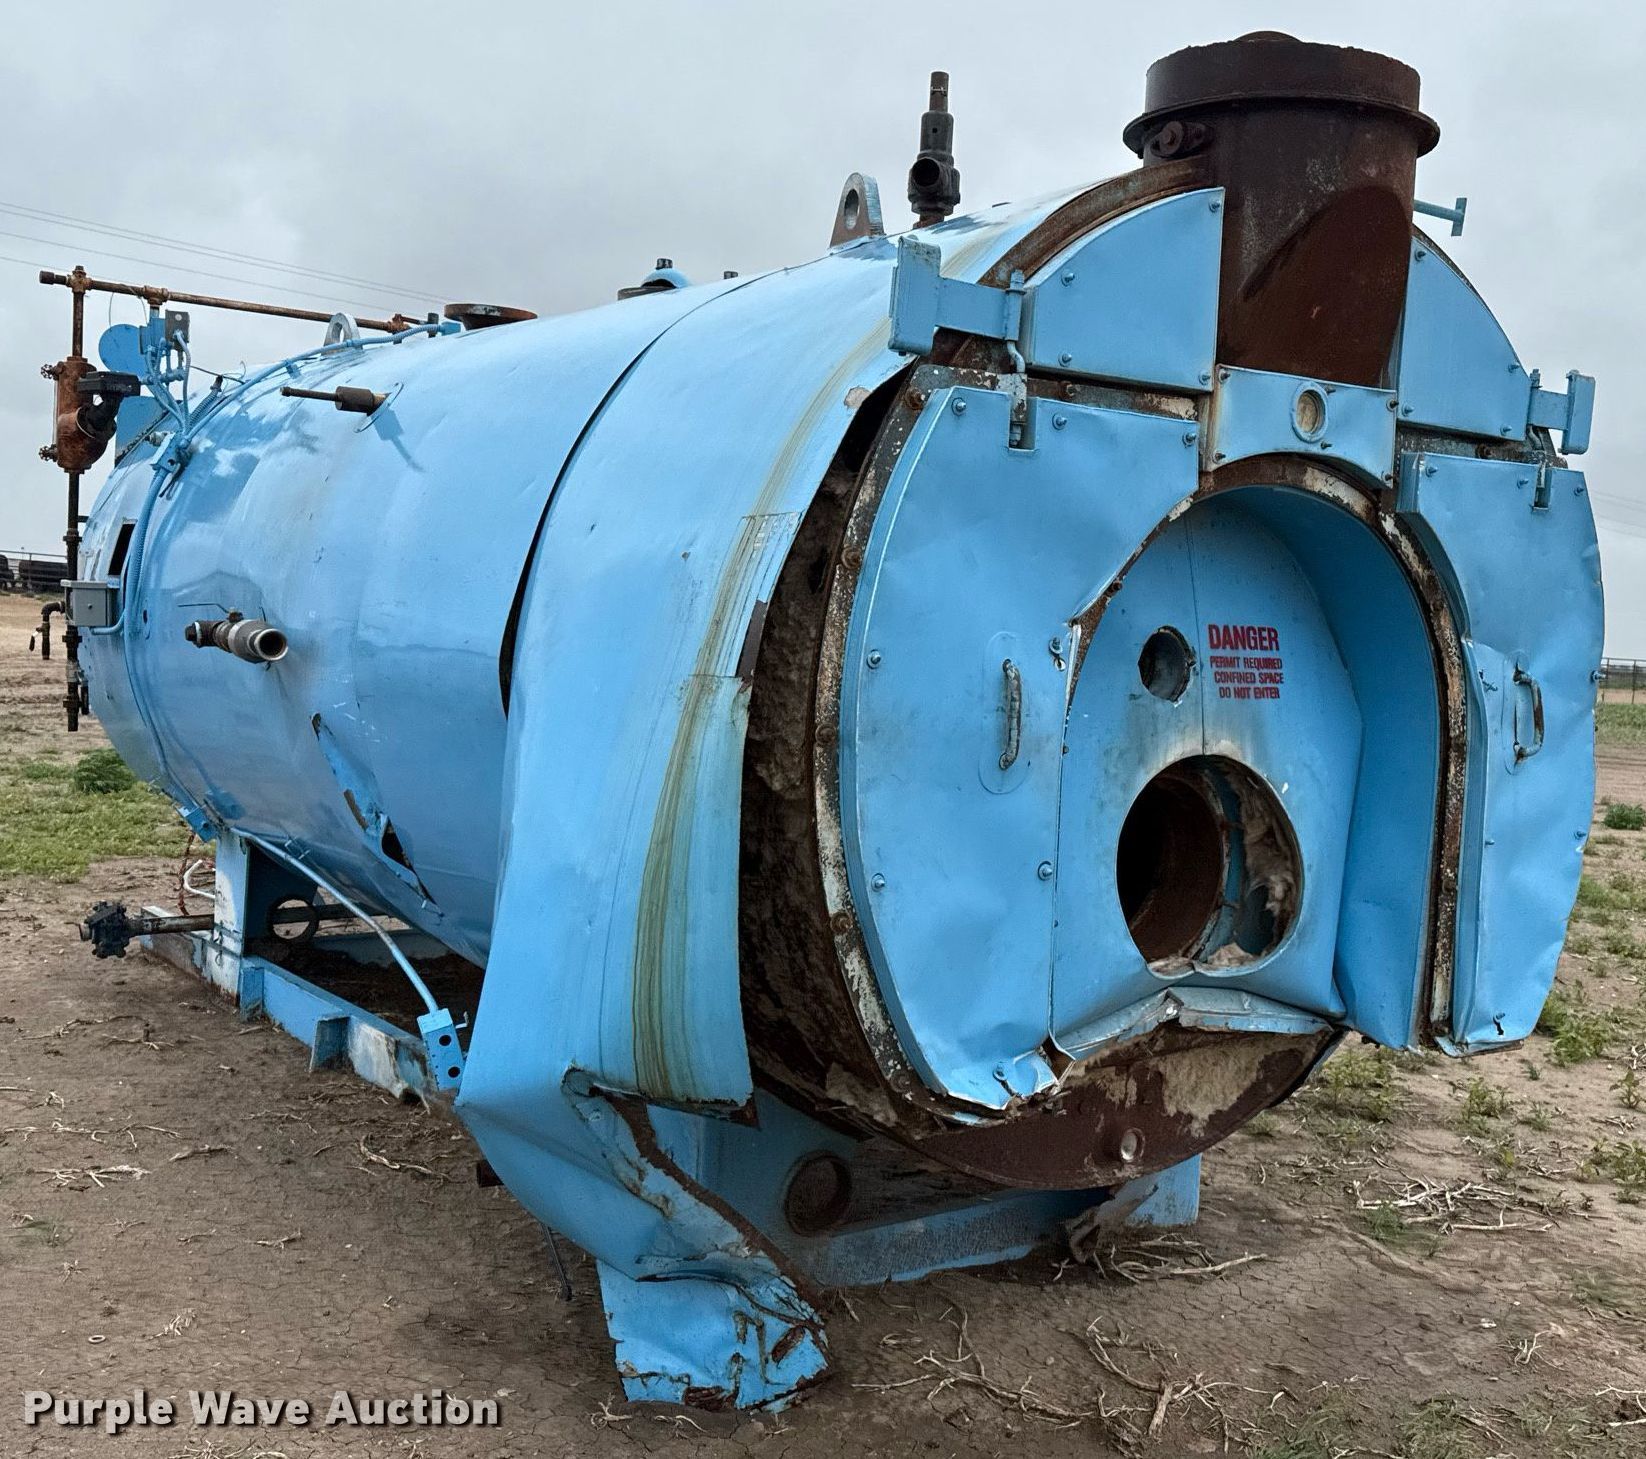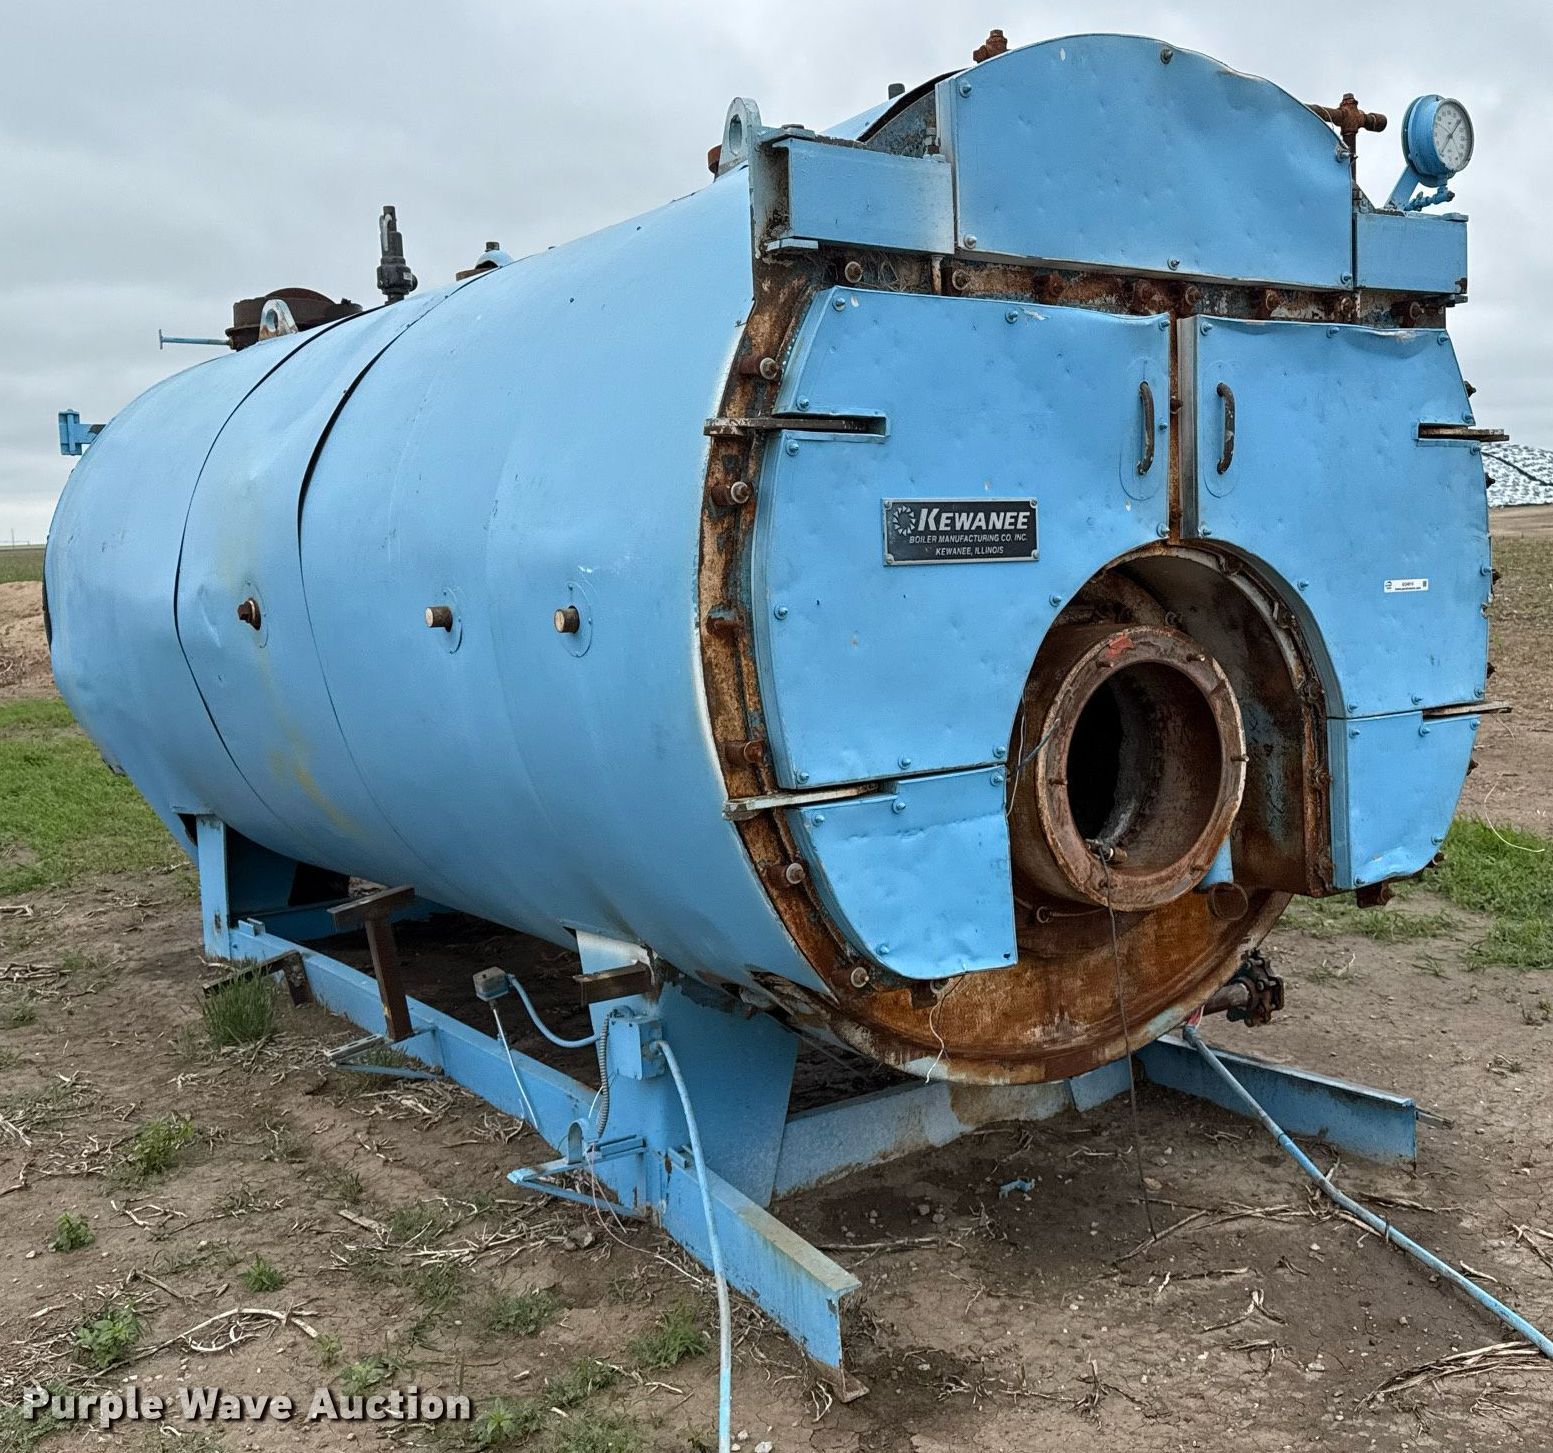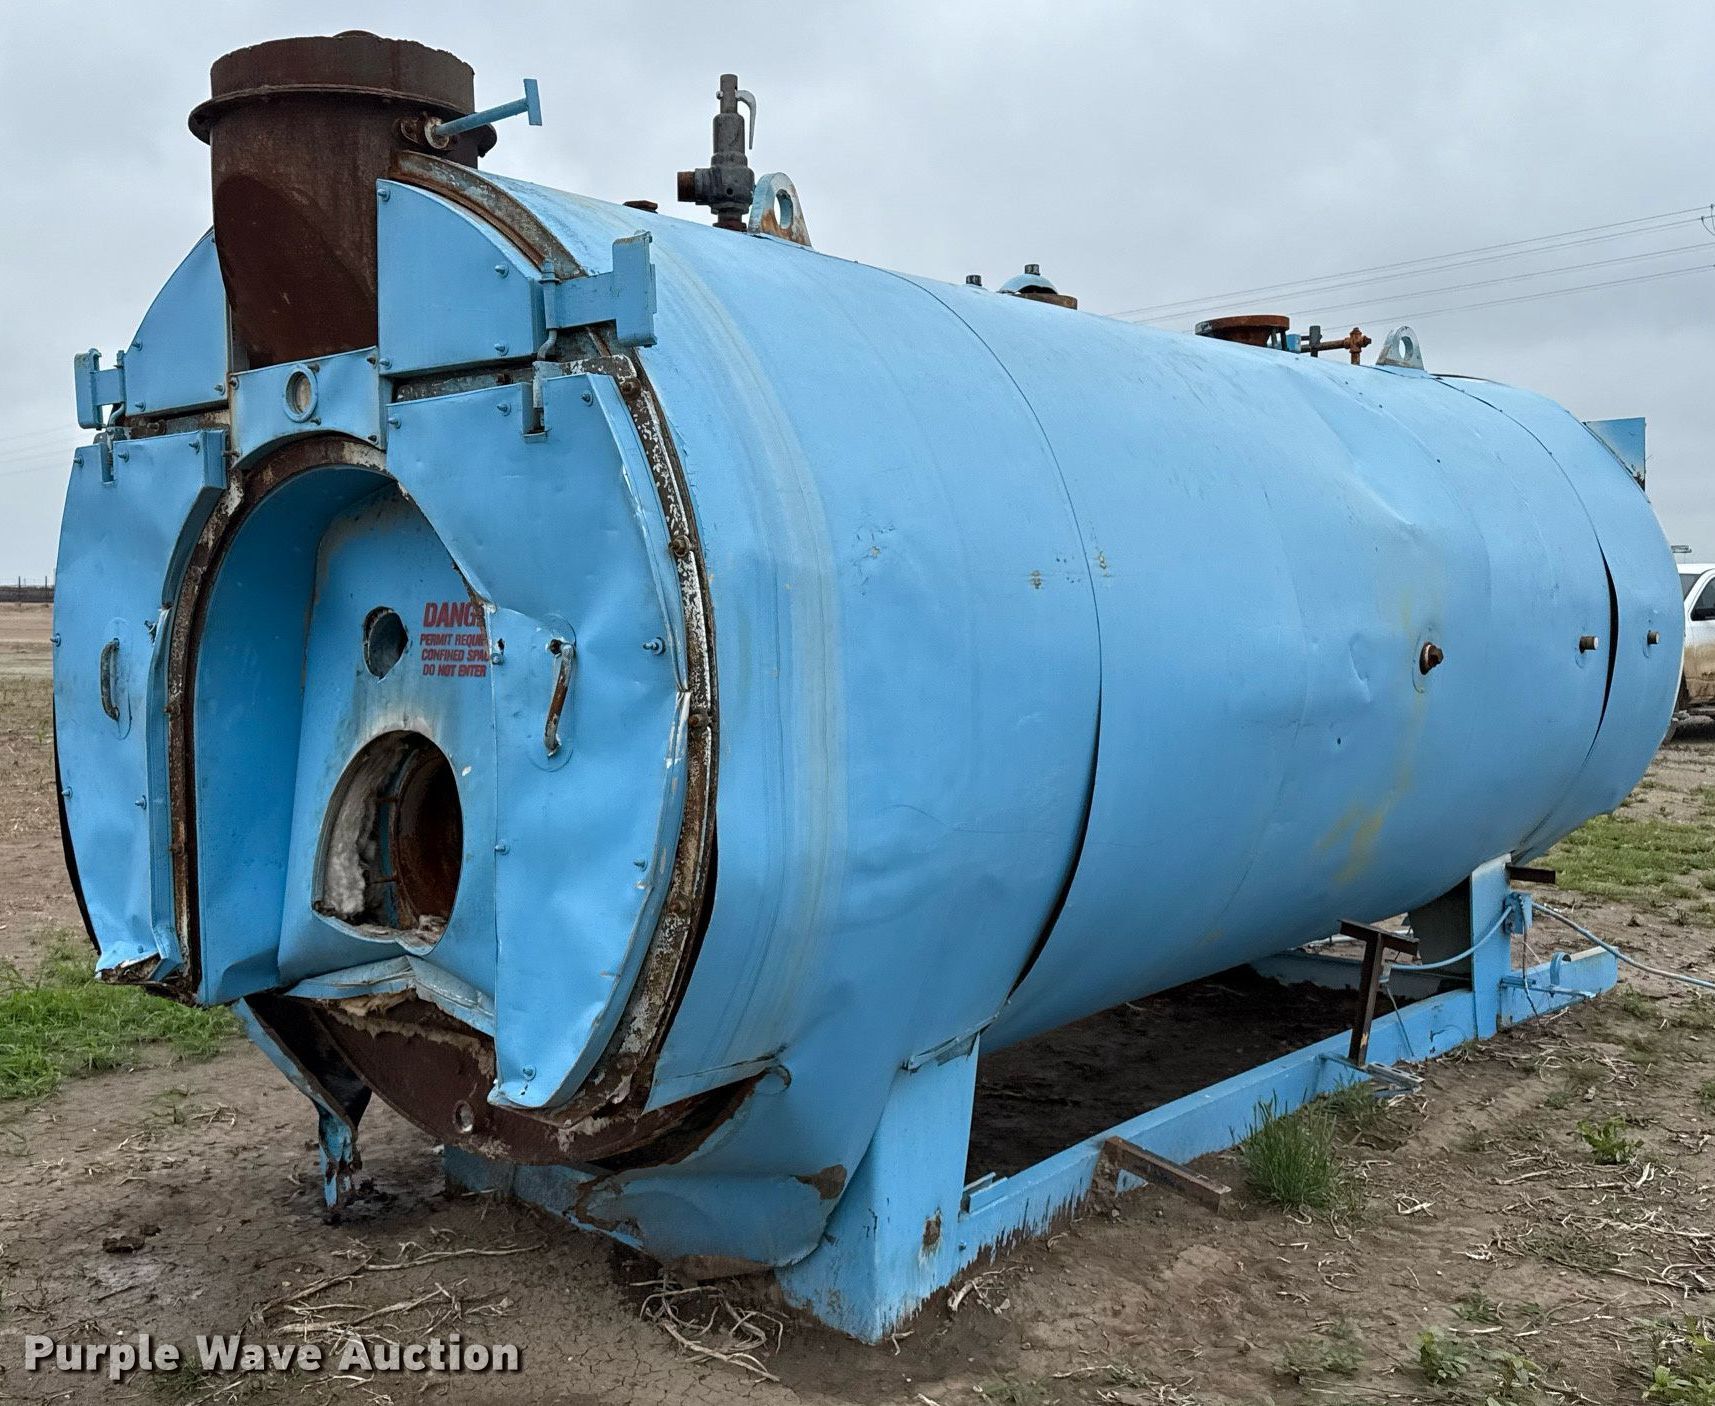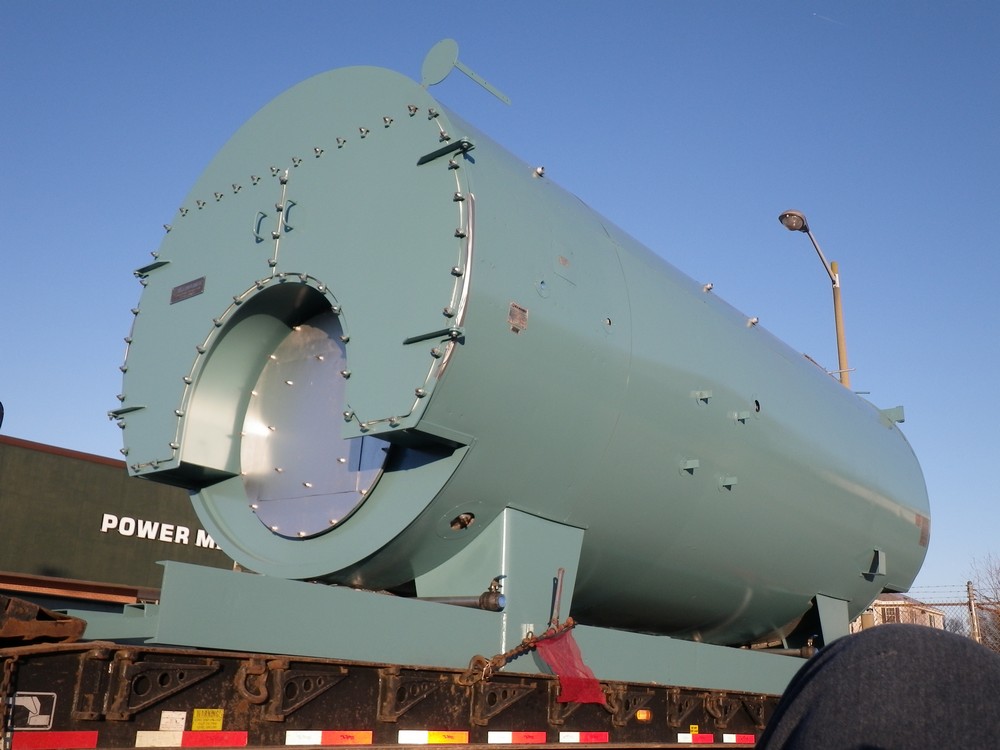
Dealing With a Kewanee 350 Hp Boiler in the Field
Kewanee made some solid cast iron boilers back in the day before Slant/Fin absorbed the line. A 350 horsepower unit is a big piece of equipment, usually running as a low water cutoff protection scenario with multiple stages of firing. When one of these shows up on a service call, you are not dealing with a residential trickledown situation. These things have their own set of expectations and failure modes that will catch you off guard if you only have experience with newer, mod-con setups. I want to walk through the basics of getting one operational, diagnosing common issues, and running maintenance, while also noting where this boiler design gets genuinely tricky. One thing nobody warns you about is the interconnecting pipe spacing between the sections. The original Kewanee design uses deep water passages with specific flow paths that are very sensitive to how the pipes are torqued during assembly. I had a job last year where a crew reassembled a 350 after replacing two cracked sections, and the boiler would not hold pressure above 12 psi on the initial fill. Turned out they were using standard universal boiler gaskets instead of the paper or rubber Kewanee specified. Once we pulled the headers and resealed everything with the correct gasket material, pressure held at design specs within twenty minutes. The wrong gasket choice was compressing too much and essentially starving the upper sections of circulation on startup.
Startup and Commissioning a Kewanee 350 Hp Boiler
Start with a full hydronic system fill and vent purge. These boilers are sensitive to air binding because of their large water volume and long horizontal sections. You need to work from the farthest radiation or index circuit back toward the boiler. If your system has zone valves, make sure each one is being exercised during the fill sequence. Do not just open the main and walk away. Check the low water cutoff before anything else. I cannot stress this enough. Install a visible water gauge glass if the unit does not already have one. The built-in probes on older Kewanee LWCOs tend to scale over faster than you would think, especially in soft water systems where carbonate precipitation is aggressive. A friend of mine watched a 350 fire dry for nearly nine minutes before the probe finally tripped on a lower flow condition. The boiler had a bypass around the safety and the water column was plumbed incorrectly, which delayed the cutoff response. Retrofitting a direct white body gauge glass and re plumbing the water column with a proper isolation valve cut the safe shutdown time dramatically. When firing up the burner, stage it correctly. The 350 hp Kewanee typically runs multiple burners or a single multi-rate burner. Bring it up on low fire first and let the metal temperature equalize across the entire bank. These cast iron sections have thick walls and a low tolerance for thermal shock. Rushing the warm up cycle can cause hairline cracks in the rear sections that will not leak immediately but will show up three months later when the cycle heat expands and contracts the metal repeatedly.
Understanding the Key Components and Their Real World Failures
The control sequence on a Kewanee 350 is relatively straightforward if you read the original wiring diagram, which is often impossible to find anymore. The stack safety, high limit, and operating control are usually wired in series. The operating control calls for heat, the induced draft fan proves flame, and then the gas valve opens. Between the operating control and the stack safety, there is a cascade of proofs that must be satisfied. One thing that bites people is the temperature and pressure gauge taps. The original Kewanee tapped ports are prone to leaking at the sealscrews because the aluminum or brass bushings crack from overtightening during factory installation decades ago. Replace the bushings, not the seal screw. I have seen countless techs crank down on a leaking gauge port and end up splitting the casting. Use a proper thread sealant rated for high temperature on the new bushings and torque them to specification, not to feel. The draft inducer motor on these units is a common point of failure. The original motors are not easy to source new anymore, and the pulleys are interference fit on the shaft. If you are pulling an inducer, use a proper puller tool. Hammering the pulley off will distort the shaft and introduce vibration that will ruin the new motor bearings within six months. I switched a few of these over to modern equivalent motors with adapter plates and it works fine as long as the belt is tensioned correctly. Loose belts are another sneaky issue. They slip under high load and the inducer slows down, the stack safety trips, and the boiler goes into lockout. The troubleshooting becomes a nightmare of chasing stack switch failures when the real problem is a worn belt.
Get the Full Details
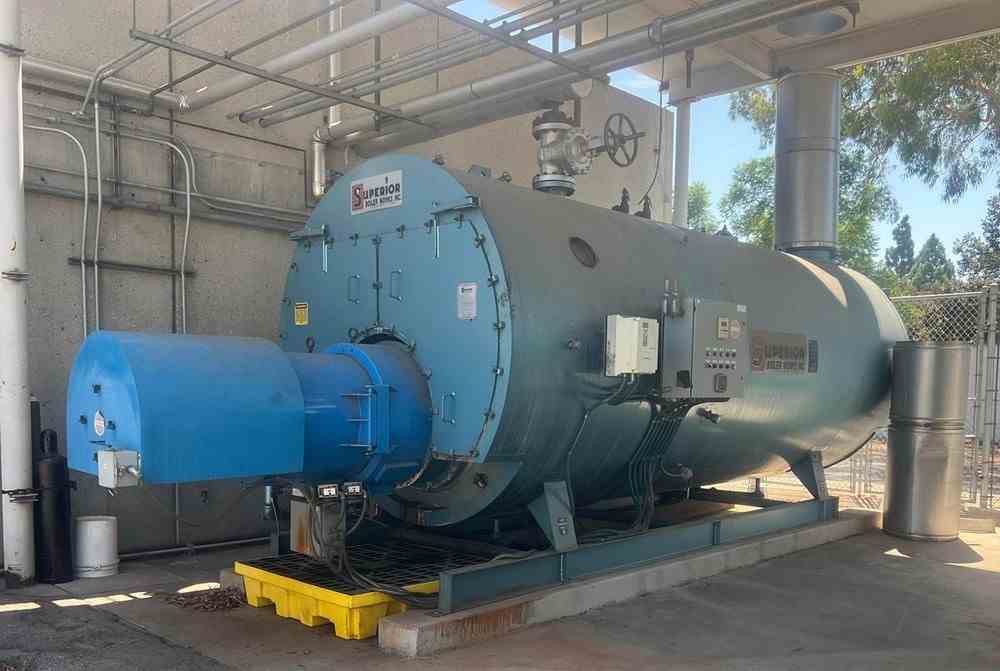
Maintenance Intervals That Actually Matter
Blow down the low water cutoff weekly during the heating season. This is not optional advice. On a 350 hp unit with that much water volume, sediment accumulates fast at the bottom of the boiler. The blowdown valve on the LWCO is small and it will clog if you skip it. I once missed this on a call where the LWCO was completely solid with scale. The boiler ran perfectly until the pressure dropped during a high demand cycle and the water level fell below the safe threshold. No damage occurred because the stack safety caught it, but the LWCO should have been the first line of defense and it was useless. Inspect the fire tube or heat exchange surfaces annually. Kewanee 350 hp units typically use a radial or return bend design depending on the exact model. Soot buildup reduces heat transfer efficiency and increases stack temperature. A clean boiler should run with a stack temperature around 300 to 350 degrees Fahrenheit at full fire. If you are seeing stack temps above 400, something is wrong, whether it is heavy sooting, incorrect air to fuel ratio, or a failing gas pressure regulator causing an overly rich mixture. Check the gas pressure at the manifold. The manifold pressure should match the burner manufacturer's specification. Too high and you get incomplete combustion, carbon deposits on the sections, and potential overfiring. Too low and the boiler will not reach rated output. I use a manometer and measure at the test port on the gas valve during a high fire call. If the pressure is out of spec, adjust the regulator screw and recheck. Do not guess based on the gas valve dial position.
When a Kewanee 350 Hp Boiler Is Beyond Repair
Not every boiler deserves the investment to keep running. If you have multiple cracked sections, particularly in the front rows where thermal cycling is most severe, and the castings are thin from years of descaling and chemical cleaning, replacement is usually more economical. I had a 350 come in with six cracked sections out of twenty four. The cost of sections, labor, and downtime exceeded half the price of a new commercial boiler. In that case, we pulled it and replaced it with a mod con unit that had significantly better part load efficiency, which mattered because this plant was cycling heavily throughout the day. Another hard failure mode is severe corrosion on the lower headers. If the water side has been allowed to drop below the recommended pH on multiple occasions, the steel headers can thin to the point where they cannot safely hold operating pressure. Hydrostatic test every header that looks suspect. If it fails the test at 1.5 times working pressure, the boiler is done. No amount of welding or patching will restore structural integrity in that situation. The bottom line is that the Kewanee 350 hp boiler is a durable piece of equipment if it gets proper care, but it demands attention to water quality, combustion tuning, and LWCO maintenance. Ignore those three things and you will spend more time troubleshooting failures than you would have spent preventing them.