Setting Up Your Mig Welder Without Burning Through Wire and Gas
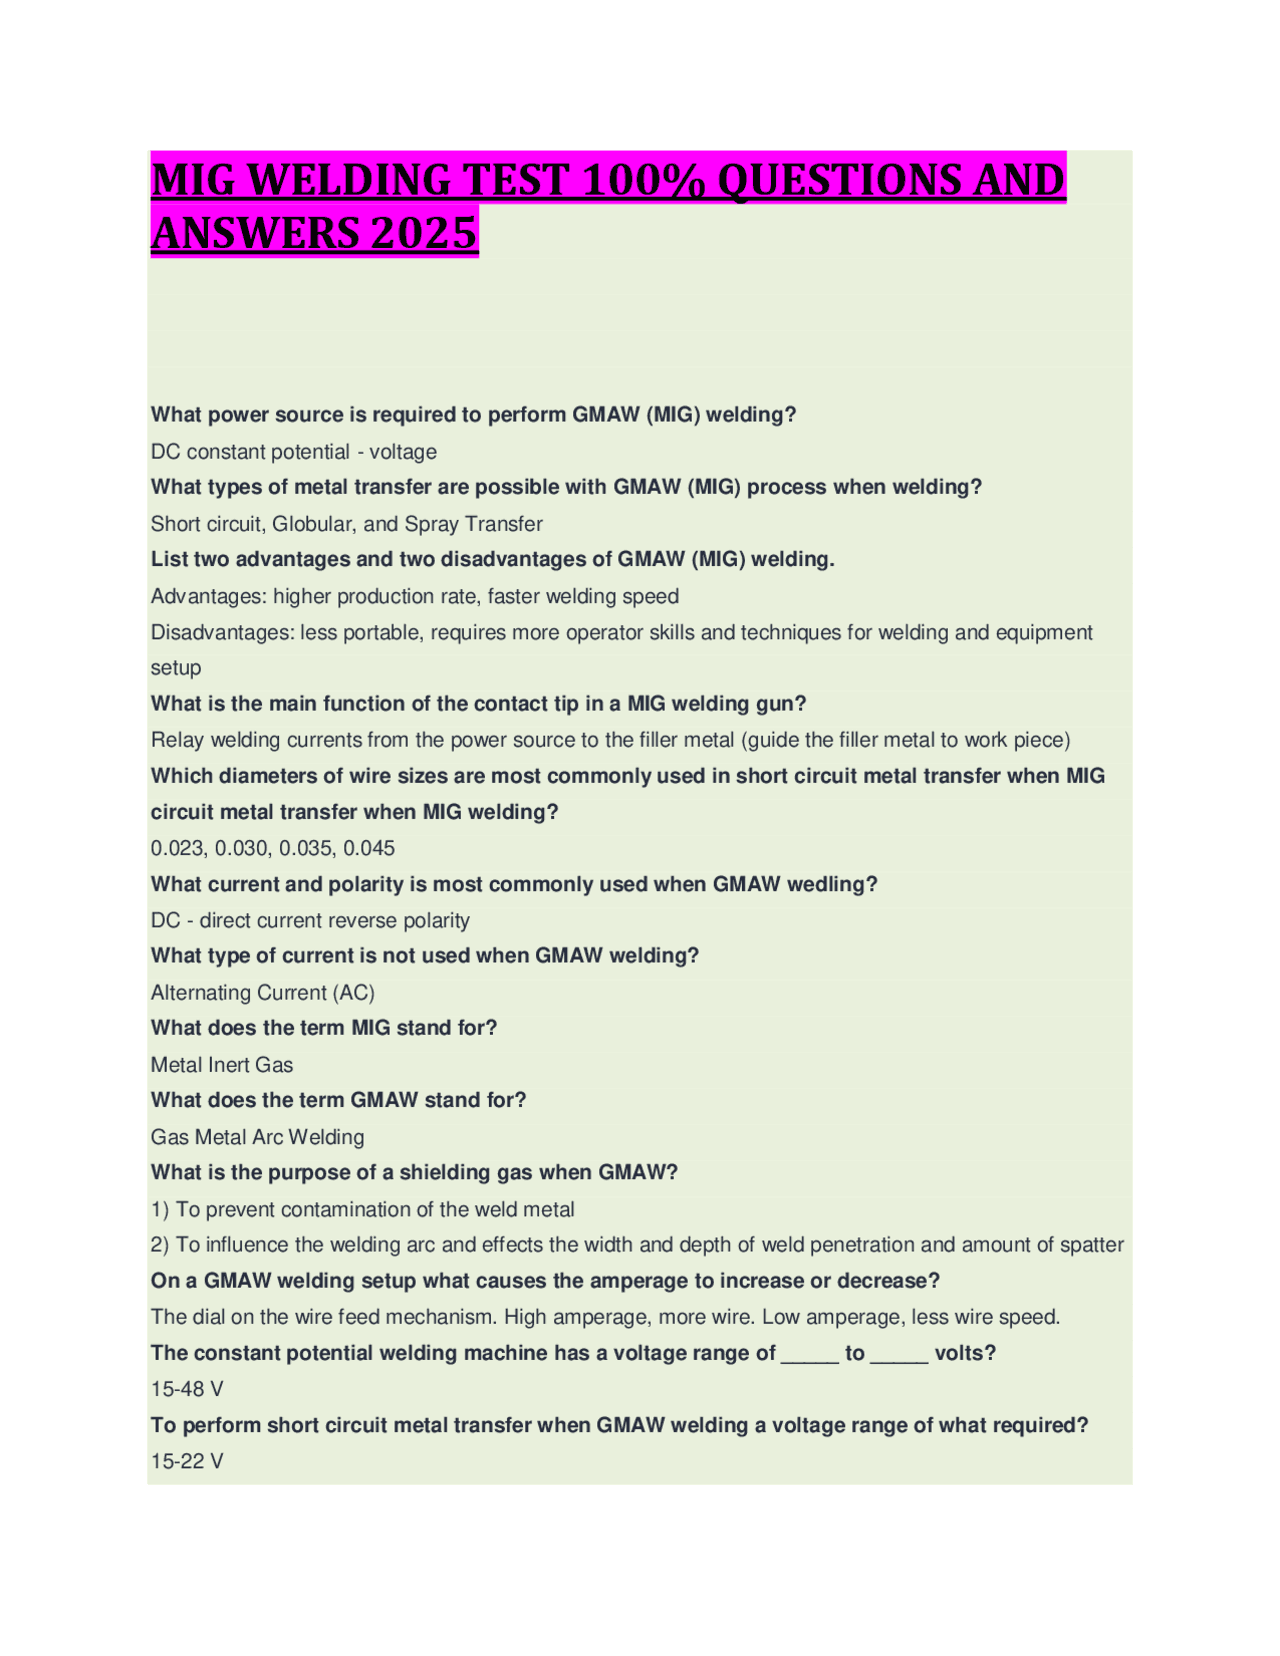
Mig welding is straightforward until it isn't. You flip the machine on, set the voltage, push the trigger, and expect a clean bead. Most people quit before that happens because they skip the stuff that actually matters. I'm going to walk through the questions people ask most, the answers that are wrong, and the ones that save you hours of grind time. What voltage should I start with for 24-gauge sheet metal? The book says something like 15 to 18 volts. In practice, you run it around 14 to 15 and go slow. Faster travel speed than you think you need. If you move at a normal walking pace, you'll burn through the material every time. The arc should sound like bacon frying, not a continuous sizzle. When it goes from crackling to a steady hum, you're in the sweet spot. Why does my wire keep birdnesting inside the liner? This is the number one frustration with syringe-style feeders. The solution isn't tightening the drive tension more, which makes it worse. Loosen the feed rollers until the wire slips when you pull it by hand. Then adjust the linear guide at the gun end so it's barely touching the wire. A quarter turn on the adjuster knob is enough. Birdnesting usually happens because the resistance downstream is too high, not because the feeder isn't pushing hard enough.
What gas mix should I use for mild steel? 75/25 argon-CO2 is the default for a reason. It gives good penetration and a stable arc. But if you've ever welded outside on a slightly windy day, you know this mix washes out fast. Switch to 90/10 argon-helium when you're in a drafty shop or outdoors. The helium makes the arc more forgiving and lets you run at higher travel speeds without losing penetration. It costs more per cubic foot, but you use less gas overall because you don't need to shroud it with makeshift covers. Here's something most beginner videos don't tell you: the contact tip size matters way more than people realize. A .035 wire in a .045 tip creates a loose fit that causes erratic feeding and spatter. The gap between wire and tip should be minimal. When I ran a job where I had to use leftover .035 wire with .045 tips on a rental machine, I got spatter buildup so bad I was changing tips every twenty minutes. Swapping to properly matched tips cut that to once per three-hour shift. The wire diameter to tip diameter ratio should always be within one size. How do I fix porosity in my welds? Porosity shows up as little holes in the bead and it's almost always contamination or gas flow issues. Check your work clamp first. If there's paint, rust, or scale under the clamp, the arc stabilizer path is compromised and electrons take a different route, which disturbs the shielding gas coverage. Grind the contact point down to bare metal. Also measure your actual gas flow with a flowmeter, not just trust the dial on the regulator. A lot of those gauges read high even when flow is low. Run it at 20 to 25 cubic feet per hour. Going higher doesn't help and just creates turbulence that pulls in atmospheric nitrogen.
I had a situation a few years back where a thick plate weld kept showing porosity no matter what I changed. Wire, gas, settings, cleaning, everything. Turned out the CO2 cylinder was nearly empty. Old CO2 tanks settle and the liquid layer at the bottom gets depleted first, leaving mostly gas phase. The remaining gas had a different composition ratio and was pulling moisture. Replacing the tank fixed it immediately. This doesn't happen often, but when it does, you'll go crazy trying to debug a gas problem that is actually a supply problem. Should I drag or push the gun? Pushing, also called forehand welding, gives a flatter, wider bead with less penetration. Dragging, or backhand welding, concentrates the heat and pushes penetration deeper. For thin material, push. For thick material, drag. The angle matters too. Keep the gun at a 10 to 15 degree angle from vertical. Anything steeper and you're blocking your own gas shield and creating a mess of spatter on the nozzle. Can I weld galvanized steel with Mig? Yes, but you need to grind off the zinc coating at least an inch on both sides of the joint. Breathing zinc oxide fumes is not a joke. It causes metal fume fever, and it's nothing to brush off. Wear a respirator even if you think the ventilation is fine. After you remove the zinc, run the wire at a slightly higher voltage than normal and use a longer contact-to-work distance. The arc needs more room to deal with the vaporizing metal. Expect more spatter. It's unavoidable with galvanized material.
Get the Full Details
My bead looks like a string of sausages. What's wrong? That's travel speed. You're moving too slowly or the voltage is too low for your speed. Increase the voltage or move faster. A good test: watch the molten puddle. It should look like a small pool of liquid metal that you're pushing along. If it looks like it's piling up behind the contact tip instead of flowing ahead of it, you're going too slow. The puddle should have a teardrop shape with the point leading forward. How much joint prep is actually necessary? More than you want to do. Mill scale, rust, oil, and moisture all cause problems. A angle grinder with a flap disc takes two minutes and prevents three hours of rework. Don't skip it. I've seen people weld over painted surfaces and wonder why their beads are inconsistent. The paint burns into the weld pool and creates porosity that you can't see until you cut the piece open for inspection. There's a common misconception that higher voltage always means deeper penetration. That's only true up to a point. After a certain voltage, the arc becomes so wide and diffuse that penetration actually decreases while spatter increases. For 3/16 inch plate, running above 22 volts with .035 wire usually just creates a messy, wide bead with poor fusion at the toes. Drop the voltage and speed up the travel. You'll get a tighter, cleaner weld with better penetration.
What about inductance settings? If your machine has an inductance or inductance control, use it sparingly. It softens the arc and reduces spatter. But too much inductance makes the arc lazy and reduces penetration. Start at the lowest setting, maybe 2 or 3 on a 10-point scale, and only increase if the spatter is unmanageable. Most production welding runs at low inductance because you want a crisp, focused arc. Preheat is another thing beginners overthink. For mild steel under 3/4 inch thick, you rarely need preheat. The exception is when the ambient temperature is below freezing or the material is thick and constrained. If you're welding a thick plate that's clamped tightly on all sides, the residual stress can cause cracking without preheat. In that case, 200 to 300 degrees Fahrenheit is sufficient. Use an indicator stick or an infrared thermometer. Don't guess by color. Steel at that temperature looks like a dull red, and most people misjudge it. If you're welding aluminum, the game changes completely. You need AC TIG or a specialized Mig setup with pulse capability. Standard Mig machines with DC don't handle aluminum well because of the oxide layer. The oxide melts at a much higher temperature than the base metal, so it traps itself in the weld and creates inclusions. If you have a MIG machine that does AC output or pulse Mig, use 100% argon and a spool gun. Inline wire feeders struggle with soft aluminum wire. The spool gun keeps the wire stiff and fed smoothly.
The biggest waste in Mig welding is consumable replacement. Contact tips, nozzles, and wire feed liners are all replaceable parts that add up. A contact tip costs about a dollar each and lasts anywhere from two to ten hours depending on your amperage and duty cycle. Running at maximum amperage for extended periods will cook a tip in under two hours. Drop your duty cycle by 10 percent and you might double tip life. It's a tradeoff between speed and cost, and the right balance depends on whether you're doing production work or occasional repair. Don't ignore your ground clamp placement. It should be as close to the weld zone as possible, on clean metal, and on the same piece you're welding. Putting the ground on a separate table or a distant part of the assembly creates a longer electrical path, which introduces resistance and unstable arc characteristics. I once spent an afternoon troubleshooting inconsistent welds on a fabricated frame only to find the ground was attached to a powder-coated bracket six inches away from the actual joint. Bare metal contact, right next to the weld, fixed it instantly. Storage of your wire matters more than most people think. Wire left in a humid shop absorbs moisture, and that moisture gets driven into the weld pool as hydrogen. Hydrogen in the weld causes delayed porosity, sometimes appearing hours after the weld is made. Keep spare spools in a sealed plastic bag with a desiccant pack. If you open a spool and don't use it within a few days, treat it like a new spool. Clean the surface by running off the first few feet before starting your actual weld.
How do I know when my settings are correct without making test welds? You don't. There is no calculation that replaces a test coupon. The variables are too many: wire brand, tip wear, gas flow accuracy, material thickness tolerance, joint fit-up, and ambient conditions. Make a test bead on scrap material of the same thickness. Cut it in half and inspect the cross section. You want penetration that reaches about 25 to 30 percent of the material thickness for a single pass groove weld. Too shallow and you have fusion issues. Too deep and you risk burn-through on thin material. For root passes on pipe welding, aim for 10 to 15 percent penetration on the inside. This gives you a narrow, controlled root that won't collapse. If you're doing structural welds where appearance doesn't matter, you can run wider beads with more travel speed. The tradeoff is heat input. More heat means more distortion, which matters if you're working on assemblies with tight tolerances. Most Mig welding problems trace back to three things: dirty base metal, wrong gas flow, and incorrect voltage-to-speed matching. Fix those and the rest is fine-tuning. Don't let anyone tell you there's a perfect setting chart. The chart is a starting point. The actual settings come from watching the puddle and adjusting one variable at a time. Change voltage, then retest. Change speed, then retest. Don't change two things at once and wonder which one fixed it.