Why You Would Even Think About Milling on a Lathe
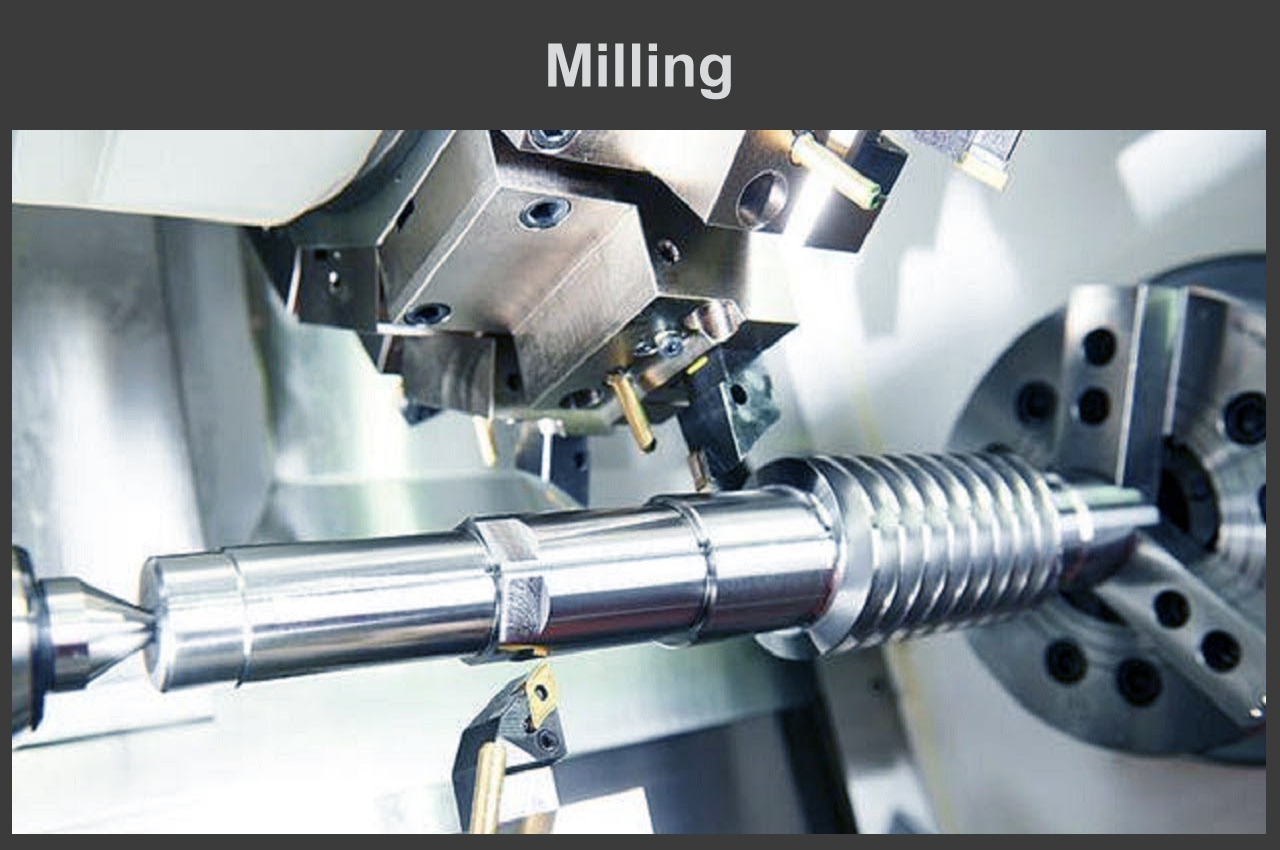
I have seen people try to mill keyways, flats, and even light slotting operations on their lathes. Most of the time it works out fine for soft materials and light cuts. Sometimes it destroys a tool or bends a setup. The difference usually comes down to rigidity and what you are actually trying to remove. This is exactly what it sounds like. You mount a cutting tool in the tool post instead of turning an external diameter. The workpiece rotates from the spindle, and you feed the tool into it laterally or axially. You are not doing heavy material removal. You are doing finishing work, light profiling, keyway cutting, slotting, or drilling cross-holes. Anything harder than that and you are better off moving the part to a mill. The basic setup involves a vertical milling attachment or a simple tool holder clamped into the tool post. A standard HSS end mill or a carbide burr works for most jobs. I use a Wabeco-style vertical mill attachment when I need accuracy. For quick-and-dirty flat faces or keyways, a boring bar with a ground insert works just as well and costs about a third of the price.
I cut a batch of aluminum brackets last year using nothing but the lathe and a half-inch end mill in the tool post. I needed four flats milled on a hex stock. The setup took about twelve minutes. Three flats came out fine. The fourth one walked out of square by about eight thousandths because I had not clamped the tool post cap screws down hard enough. You would think that is obvious. It is not obvious until it happens to you.
How the Cutting Actually Works
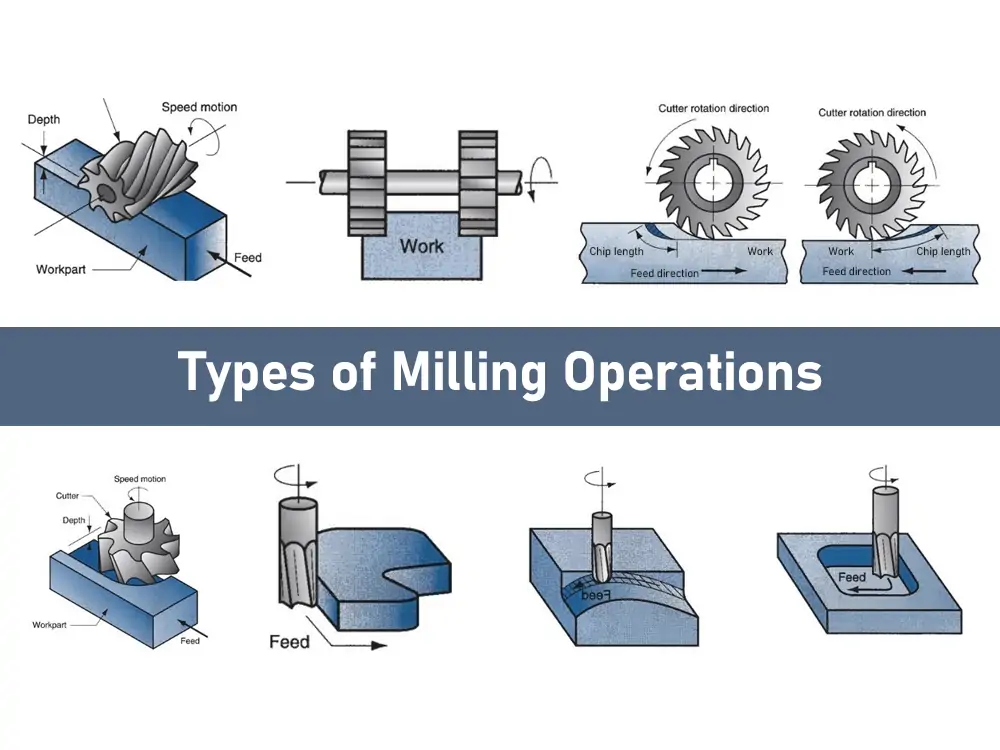
When you mill on a lathe, the chips are thrown differently than on a vertical mill. The rotation direction matters a lot here. Clockwise rotation with the tool on the right side of the workpiece tends to push the tool away from the cut. That is a climb milling situation and it can be unstable depending on your setup. Counter-clockwise is safer on most lathes because the tool gets pushed into the work, not pulled away. I always run counter-clockwise unless I have a very rigid setup and a good reason to do otherwise. The feeds are different too. On a lathe, the spindle speed for milling needs to be much lower than you would use for turning. I typically run between three hundred and eight hundred RPM for HSS tools in mild steel. Carbide can handle more, maybe up to twelve hundred, but you are still limited by the lathe spindle bearing capacity and the rigidity of your tool holder. Going faster just makes the chatter worse. Cut depth is where people get into trouble. You should never try to take more than point-zero fifteen inches on a single pass with a standard tool post setup. Two passes at point-zero zero five each will give you a better surface finish and put less stress on your spindle bearings. I once tried to mill a quarter-inch wide keyway in one pass on a piece of cold-rolled steel. The lathe groaned, the tool vibrated for about six inches, and then the insert chipped. Took me twenty minutes to swap it out and another fifteen to finish the keyway in three light passes.
Get the Full Details
What You Can Actually Cut
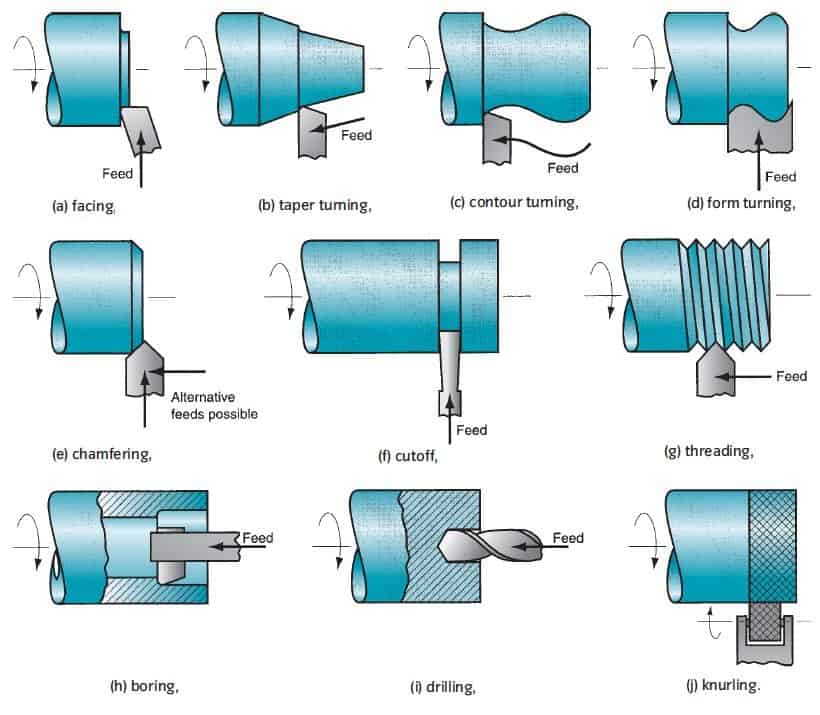
Keyways are the bread and butter of lathe milling. A standard keyway cutter or even a regular end mill will work. Use the cross slide for depth and the carriage for length. Set your depth with a dial indicator against a test piece first. Do not eyeball it. Flats on round stock are straightforward. You mill two sides opposite each other. Index the work, clamp, mill. If you need precision flat-to-flat dimensions, measure with a micrometer after each side. Lathes have radial runout, so your flats will never be perfectly symmetrical unless you are running very light cuts and checking frequently. Drilling across the face is another common operation. You can use the lathe to index holes around a pattern without an actual dividing head. I have done bolt circle drilling on flanges this way. It is not as precise as a proper indexer but it gets the job done when you do not have the equipment handy. You mark the locations, center punch them, and drill with a brace or a magnetic drill if you are feeling generous.
Slotting and grooving work similarly. A parting tool can cut slots, but a milling cutter gives you cleaner walls and better width control. I use a thin slitting saw for slots that need to be precise in width. The tradeoff is speed. A slitting saw removes material slowly and it deflects easily. I make multiple shallow passes rather than one deep one.
The Stuff Nobody Tells You Up Front
Lathe spindles are not designed for radial milling loads. The bearings take axial and tangential forces well. Radial forces from side cutting wear them down faster than you might expect. If you are doing occasional light milling, you are fine. If you plan to mill hard steel regularly on your lathe, you are going to shorten the life of your spindle bearings significantly. I learned this after my last lathe started developing a slight rumble around sixteen hundred RPM. The mill attachment had been working hard for about a year before that. It was not the only factor, but it was definitely a contributing one. Another thing is chip evacuation. On a vertical mill, chips fall away naturally. On a lathe, they tend to wrap around the workpiece or pile up against the tool. I keep a compressed air nozzle pointed at the cut and I clear chips between passes. If chips get trapped under an end mill, they can score the work surface or cause the tool to dive into an unexpected depth. Tool overhang is critical. Every inch of overhang beyond what is necessary multiplies the deflection. I keep my tool posts ground down to minimize overhang and I use the shortest end mills I can find for the job. A half-inch end mill with three inches of overhang will chatter like mad in steel. The same cutter with one inch of overhang cuts smoothly at the same feed rate.
I also learned the hard way that not all tool post mounts are created equal. The standard four-bolt mount on a South Bend or similar lathe has some play in it. Even with the lock nut tight, there is micro-movement during cutting. I solved this by machining a custom spacer that reduces the play between the tool post and the mount. It cost me about an hour of machining time and eliminated most of the vibration. You could also buy an aftermarket rigid tool post, but that runs about two hundred dollars and the DIY fix works just as well if you have the setup for it.
When You Should Just Move to a Mill
If the part is hard material like tool steel or stainless, forget about milling on the lathe unless the cuts are very light and the geometry is simple. The lack of rigidity and the spindle bearing concerns make it not worth the risk. Deep slots or pockets require tools with more reach, and more reach means more deflection. That is a losing proposition on a lathe tool post. Same with side milling where you need to engage a large portion of the cutter diameter. Lathe spindles do not have the power curve for that kind of load. Multiple sides or complex profiles are also better served on a proper mill. You spend more time indexing and repositioning on a lathe than you would on a mill with a rotary table. The accuracy suffers too because every repositioning introduces error.
I keep a list of operations that belong on the lathe versus the mill. Milling on the lathe works when the part is already on the lathe for turning and you need a quick feature added. It works when you do not have access to a mill. It does not work when precision and efficiency matter more than convenience. If you are starting out and want to practice, grab a piece of aluminum and a spare end mill. Mill a flat on a round bar. Measure it. Do it again until you can get within point zero zero two inches. That will teach you more about lathe milling than any tutorial. The fundamentals are straightforward. The devil is in the details like tool overhang, spindle speed, and clamping force.