Getting Started with Mitsubishi PLCs
Most people start with GX Works2 or GX Works3 depending on what hardware they are working with. The software is free to download from the Mitsubishi Electric website. You need an account and you have to agree to their licensing terms before you get access. I have been programming MELSEC systems since the FX series was the standard on factory floors, and the workflow hasn't changed that much over the years. The real training doesn't come from reading manuals cover to cover. It comes from wiring something up, writing a ladder logic routine, and then spending three hours on the phone with someone who actually knows what they are doing when it doesn't work. That said, there are legitimate paths through this. I would start by downloading GX Works3 and going through the built-in help documentation. It is not great, but it is better than nothing. Then grab a secondhand FX3U or Q-series PLC from eBay for around two hundred dollars. Do not buy the cheapest one you can find. The cheap ones have usually been flashed with some weird firmware or have damaged connectors. I learned that the hard way on my first purchase. The board came back with a faulty CPU and I lost a week waiting for a replacement.
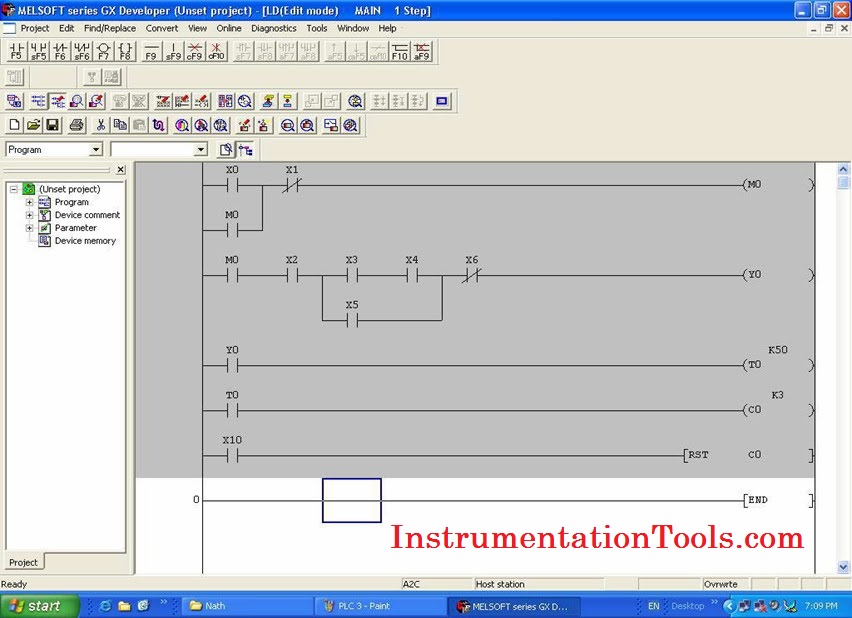
Write simple programs first. A start-stop circuit with latching. A timer-based sequence. A counter that counts parts on a conveyor. These are the things that actually get used in the field, and understanding them properly matters more than jumping into complex motion control right away. Once you are comfortable with basic ladder logic, move into instruction handling. Mitsubishi uses a broad instruction set. STL, OUT, AND, OR, ANI, ORI, Timers, Counters, Compare instructions, Data Move, Shift instructions. Learn what each one does under different conditions. The DIFU and DIFD instructions for edge detection alone will save you from countless debugging sessions. Beginners tend to ignore these and then wonder why their outputs are flickering or responding to the wrong signal edge. Communication is where most people hit a wall. RS-232, RS-485, Ethernet. GX Works3 supports all of them. I spent two days once trying to get a Q-series PLC to communicate with an HMI over CC-Link IE because the IP addressing was conflicting with an existing network segment that nobody had documented. The PLC was pulling an IP from the wrong subnet and every diagnostic LED on the back was lit up red. What fixed it was pulling the parameter file from a backup on another machine that was already configured correctly, modifying just the IP and subnet mask, and pushing it back. Saved me from rewriting the whole communication setup from scratch.
For structured training programs, Mitsubishi offers certified courses through their regional training centers. The basics course covers ladder logic programming, programming tools, and basic troubleshooting. The advanced course goes into motion control, network configuration, and process control. These run a few days and cost money, but they come with official certification which matters on a resume. Some employers require it. Online resources exist too. YouTube has decent walkthroughs. There are forums like PLCTalk.net and the Mitsubishi-specific sections on Reddit where people post actual problems and actual solutions. Those are worth more than most paid courses because they deal with the edge cases that don't appear in any textbook. A PLC that won't go into RUN mode because a program file has a corrupted data block is not something you find in an introductory manual. It is something that happens at 2 AM on a production line and nobody is around to help you. The biggest mistake people make is treating programming as purely a software exercise. The hardware matters. The power supply matters. Grounding matters. Signal noise from variable frequency drives can corrupt communication lines if they are routed improperly. I have seen entire projects fail because someone ran encoder cables parallel to motor power cables in the same conduit. The PLC worked fine in the lab. It failed immediately on the actual floor.
Get the Full Details
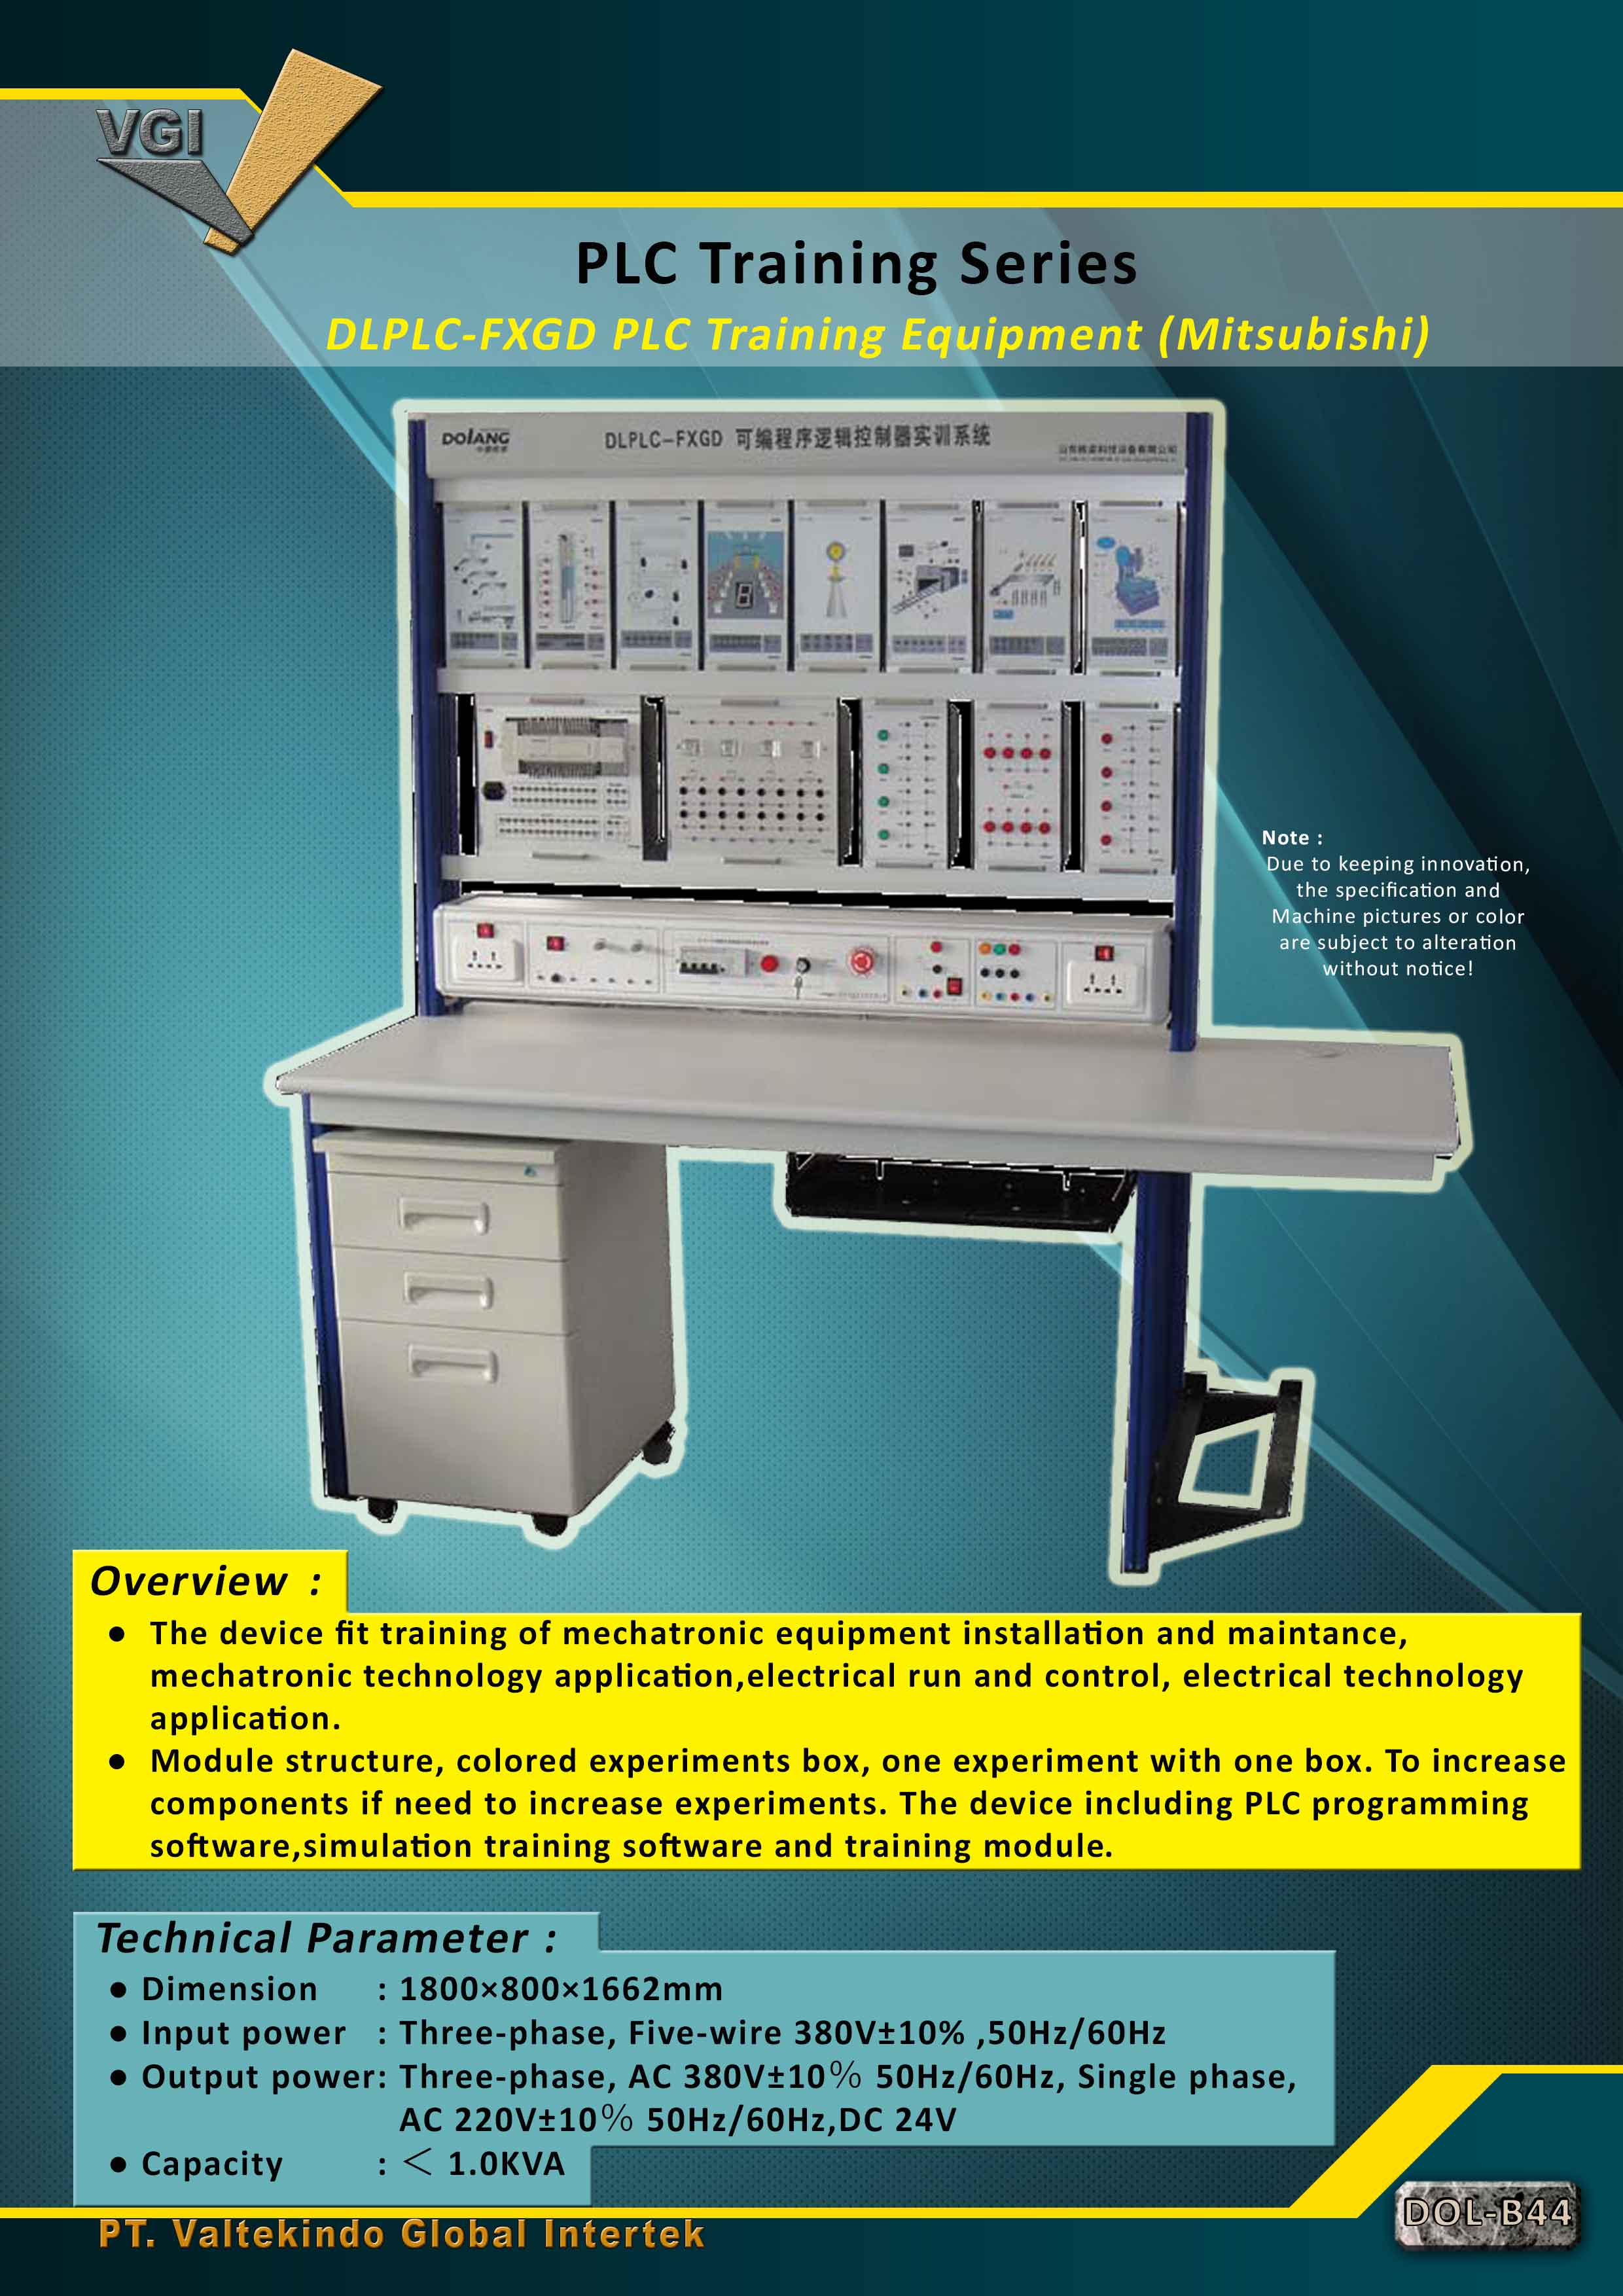
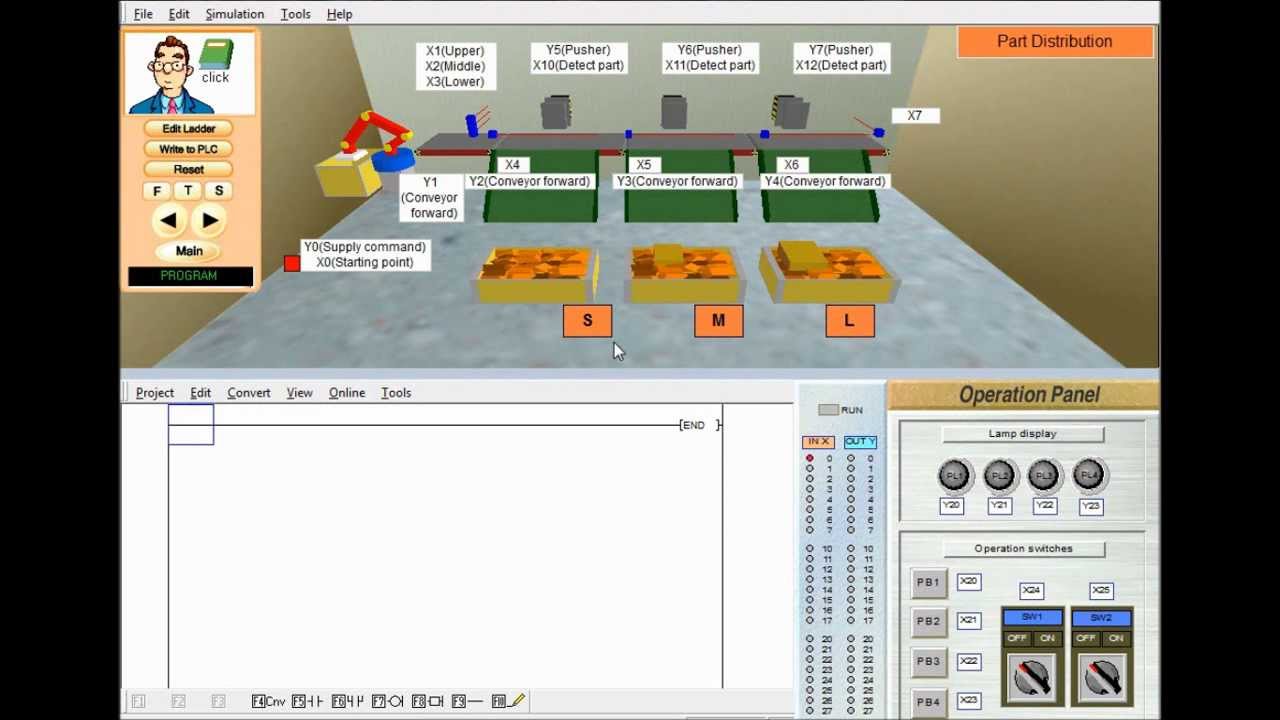
If you want to learn properly, set up a small test bench. PLC, power supply, some pushbuttons and indicator lights, maybe a small potentiometer for analog input practice. Simulators exist inside GX Works3 but they do not replicate electrical behavior. You need to see what happens when a contact bounces or a signal drops. That only shows up with real hardware. Documentation habits matter more than you would think. Name your registers, your timers, your memory bits. Use meaningful names instead of D100, T1, M500. When you come back to a program six months later and it is all generic addresses, you will be starting from zero. I have walked onto sites where someone had left and the entire program was a wall of unlabelled devices. Good luck figuring out what M8000 was supposed to do in that context. Watch for firmware versions. GX Works2 and GX Works3 are not fully interchangeable for all PLC families. FX series works with both. Q and iQ-R series primarily use GX Works3. Make sure whatever training material you follow matches your target hardware. I once followed a tutorial meant for GX Works2 on a Q-series project and spent an afternoon realizing none of the function blocks I needed were available in that environment.
Download the software yourself and start playing with it before committing to any formal program. It takes about an hour to install and another hour to understand the basic layout. After that, the learning curve is really about how much time you put into hands-on practice versus passive consumption of tutorials.