Working Through a Nfpa 654 Dust Hazard Analysis
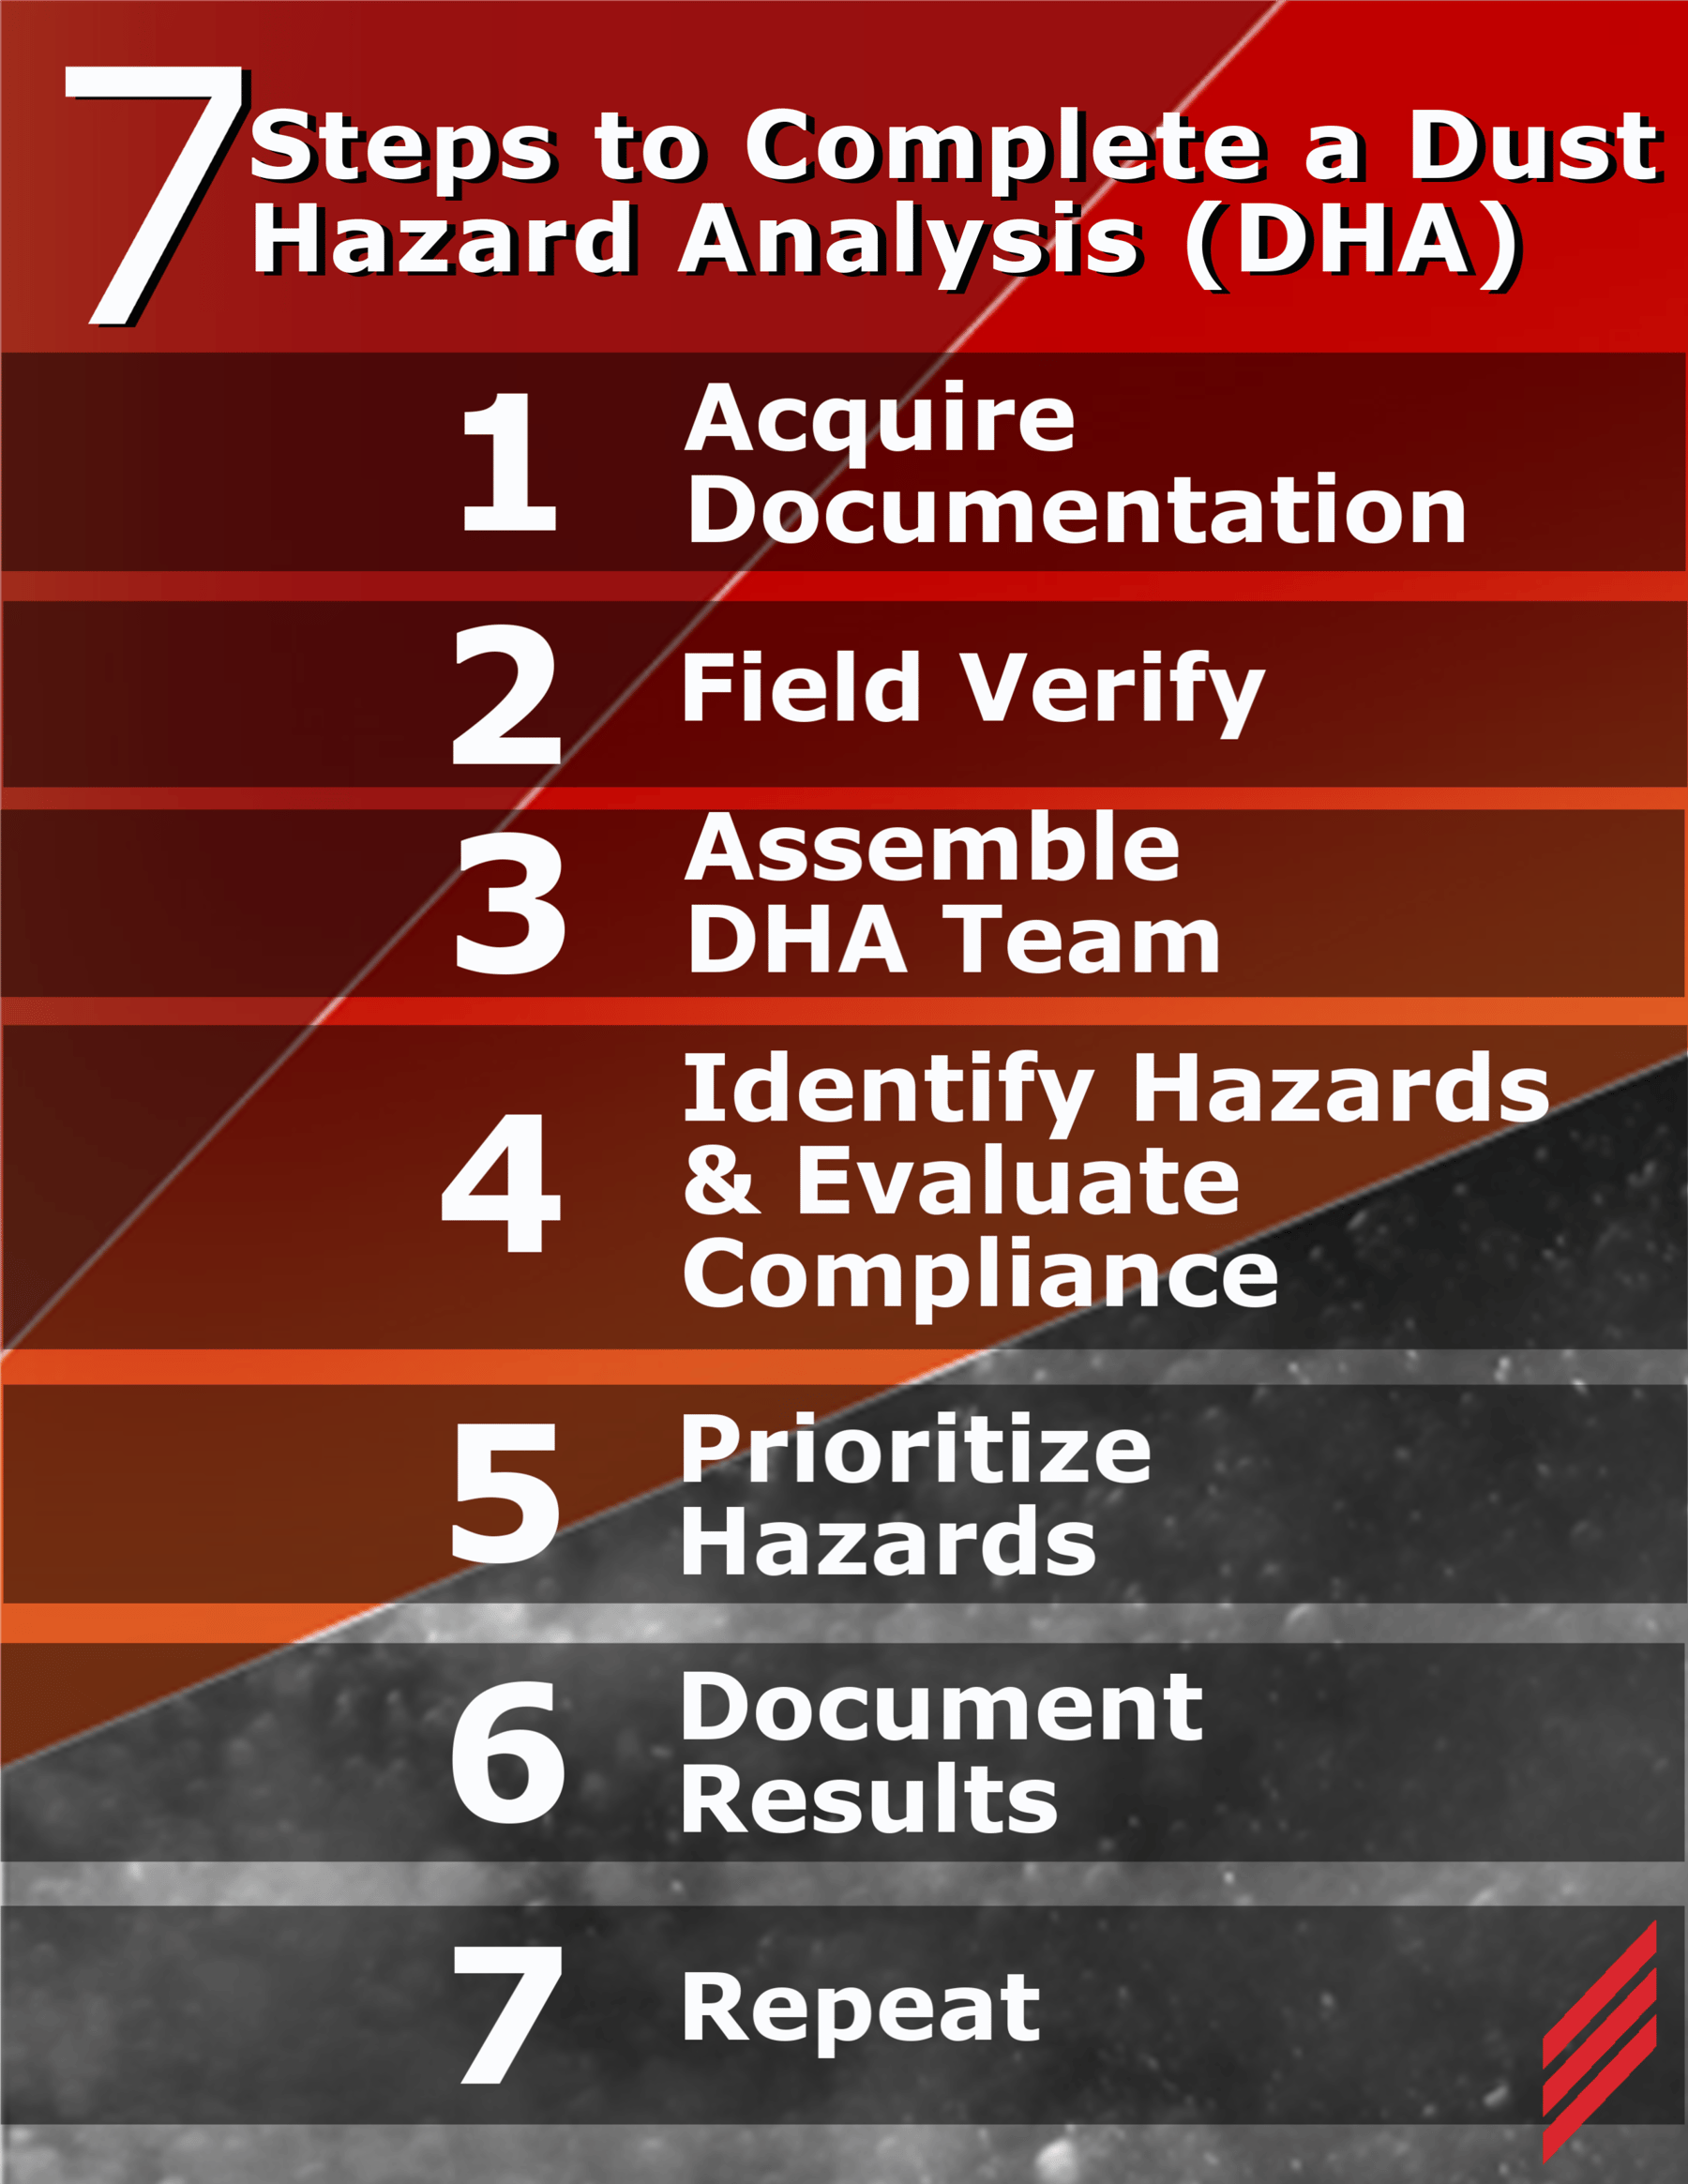
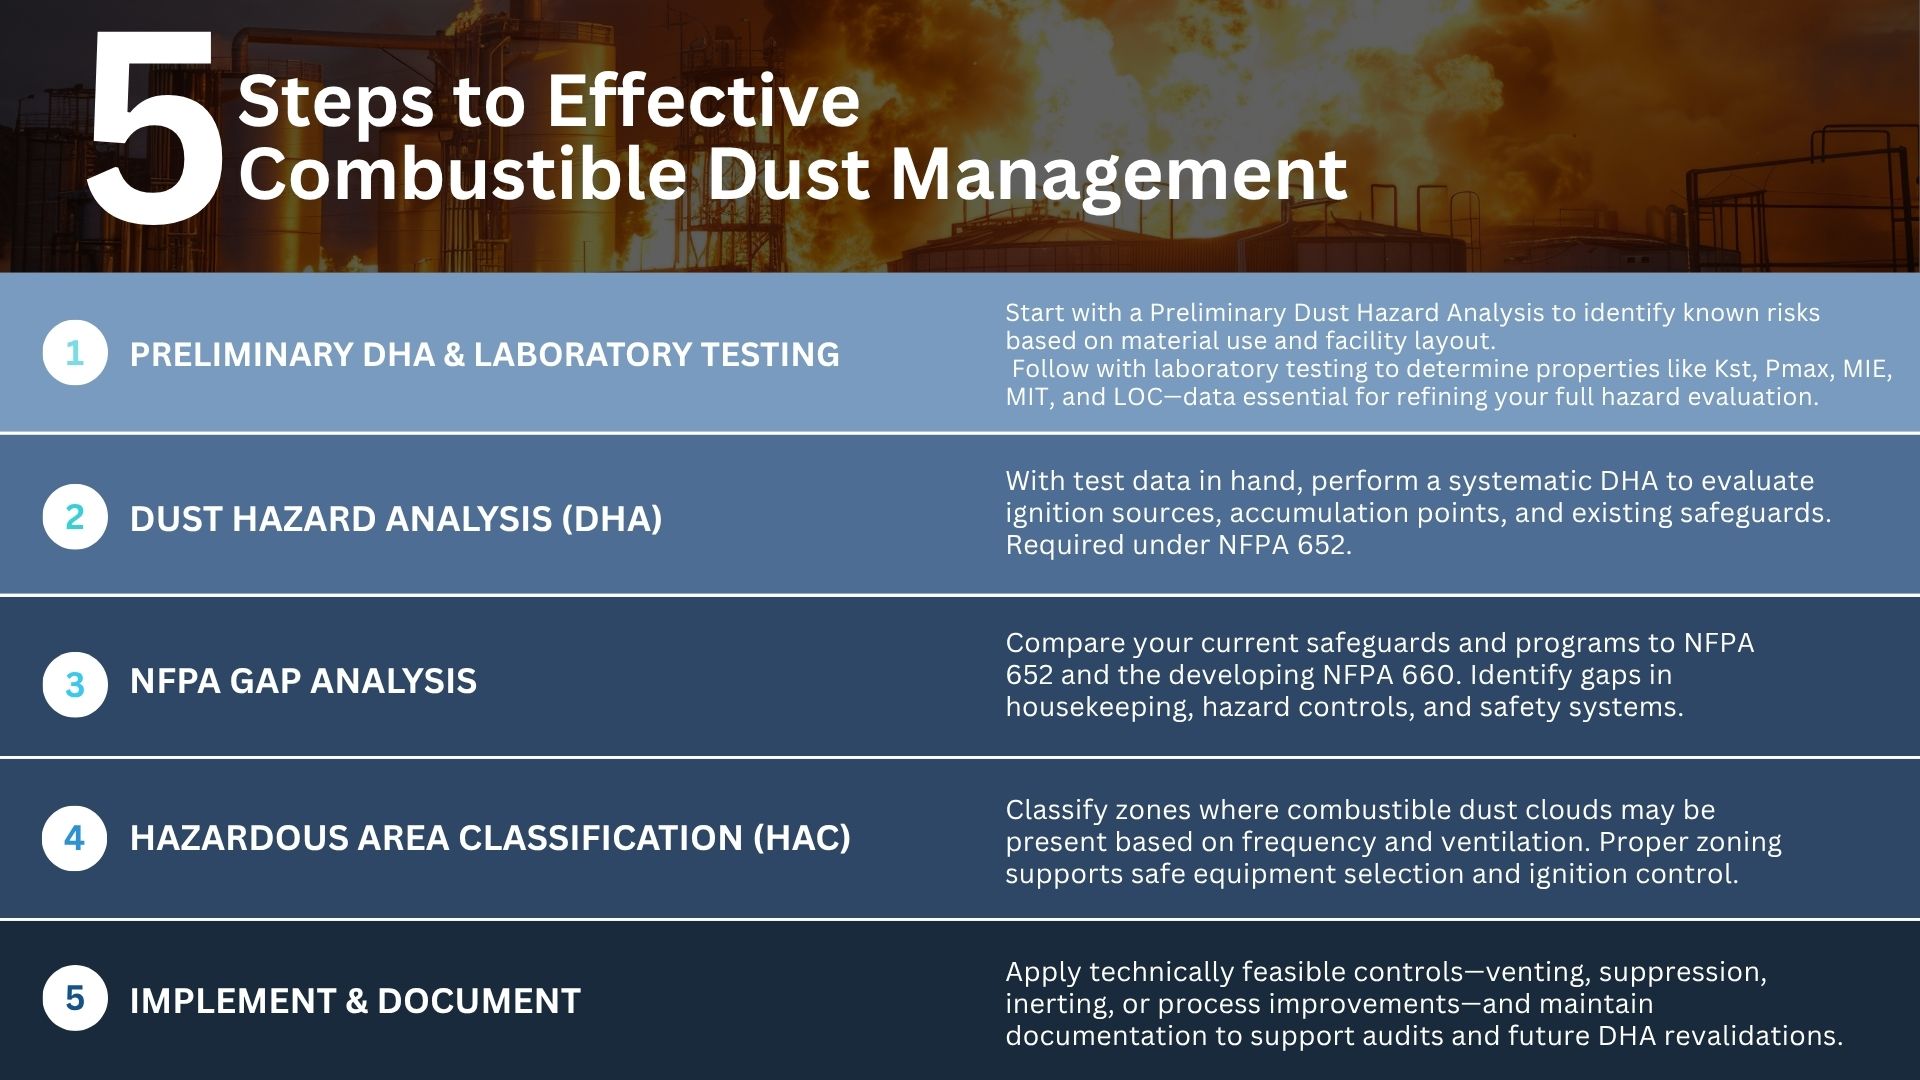
A Nfpa 654 Dust Hazard Analysis is basically a systematic way of figuring out where combustible dust explosions can happen in your facility, what the actual consequences would be, and which controls are worth spending money on. It sounds straightforward on paper. In practice it is messy, because most plants were not designed with dust explosion protection in mind. Here is how I approach it when someone hires me in. First, you need a materials inventory. Every solid material that enters the building needs Kst, Pmax, MIE, MEC, and bed ignition temperature data. If you do not have lab results, order them from a certified testing lab. Don't guess. I worked at a grain processing site once where the engineer just plugged in default values from a handbook for soybean dust and got Kst wrong by almost 40 bar·m/s. That changed the entire explosion protection strategy for the leg and receiving hopper. Once you have material data, walk the facility with a PPE map. That means partitioning the plant into zones based on dust type, concentration, and ignition sources. You are looking for five key things: dust accumulation on surfaces, potential ignition sources in each zone, dust dispersion events during normal operations and maintenance, whether deflagration venting or suppression is feasible, and where isolation is needed to prevent propagation.
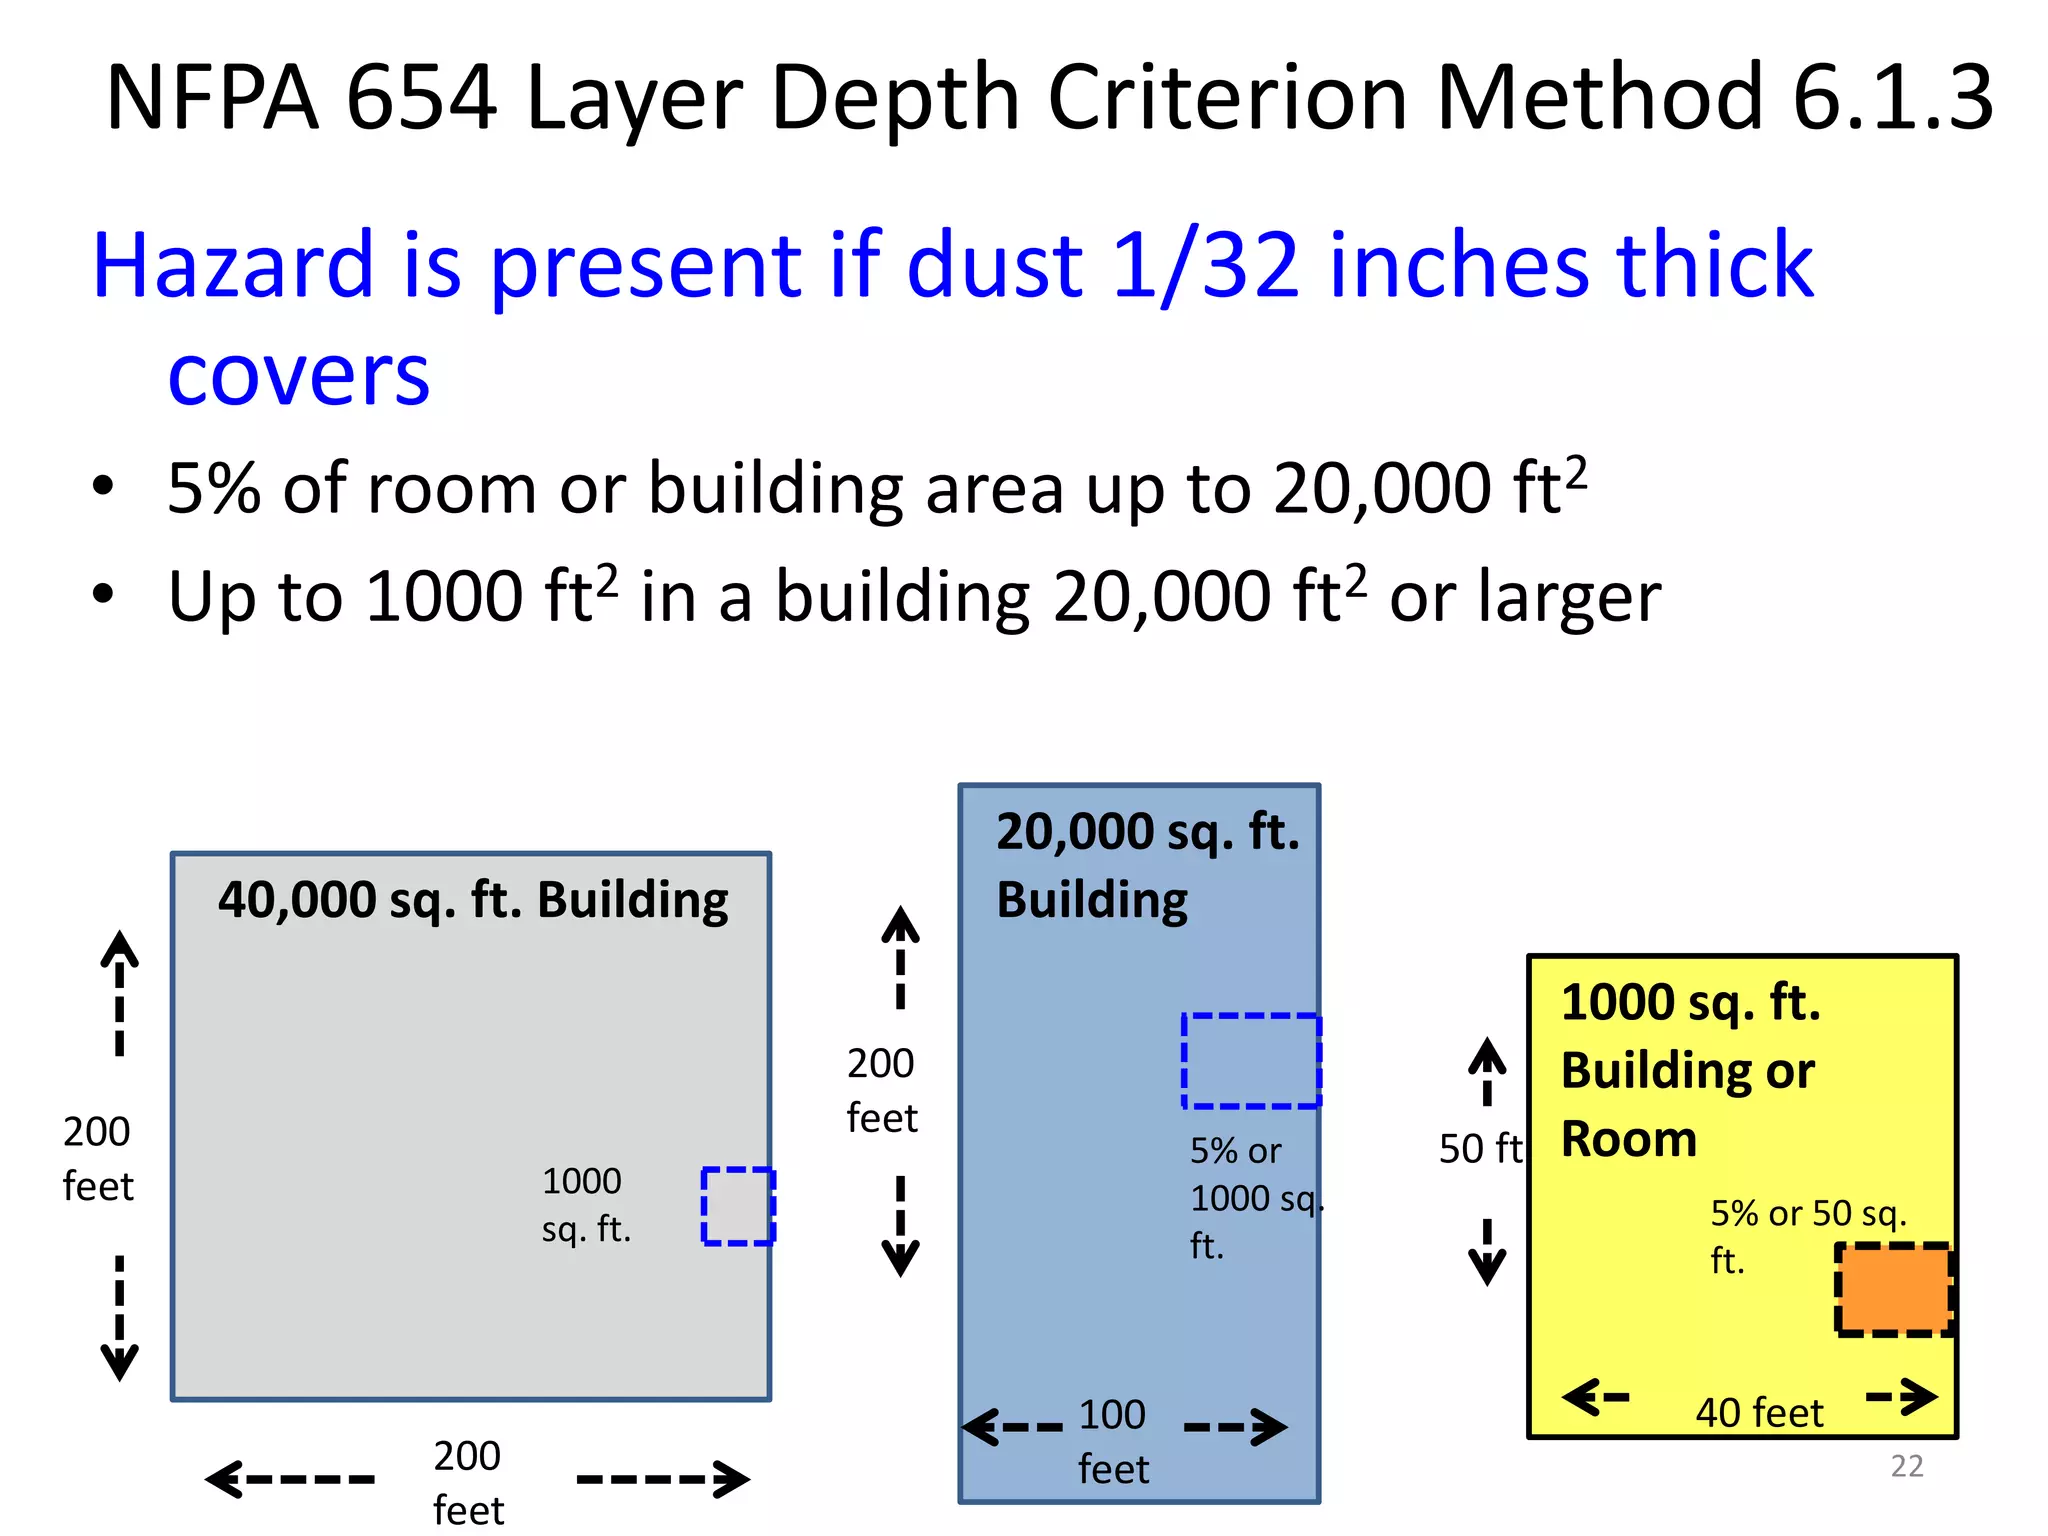
The analysis itself uses the explosion parameters to calculate the required vent area for each piece of equipment, or determines whether suppression or explosion isolation is the better route. For silos and hoppers you typically do a KSG-based vent sizing calculation. For ductwork and conveyors you need to evaluate whether an isolation device is warranted based on the volume and the Kst value. One thing people consistently mess up is the ventilation and dust accumulation assessment. NFPA 654 requires you to evaluate how much dust builds up on horizontal surfaces and whether that accumulation can be dispersed by equipment operation or normal air movement. I had a case where the initial analysis concluded a paint booth area had negligible risk because the powder coating dust layers looked thin. Then I measured the actual layer thickness during a scheduled shutdown. The accumulated dust was sitting in corners and on top of conduit runs, and when the overhead fans cycled on, it lofted into a suspended cloud well above the MEC. That pushed the area from low risk to high risk overnight. We added housekeeping protocols, positive pressure in the control cabinets, and switched the fan motors to a higher ingress rating. Another thing nobody wants to talk about is the interaction between multiple pieces of equipment in a system. If you have a hammer mill feeding a filter collector through a duct, a deflagration in the mill can propagate through the duct into the collector. The standard requires you to evaluate this propagation path and size isolation devices accordingly. Chemical isolation using two-flap valves or liquid seal devices is common, but I have seen companies spec isolation without actually verifying the response time of the device against their specific duct velocity and length. A standard two-flap valve takes roughly 100 milliseconds to close. If your duct is long and the flame speed is high, that valve might not close before the pressure wave reaches the downstream equipment. In those cases you need to either reduce the duct length, increase the flame arrestor spacing, or switch to chemical suppression at the source.
Let me also tell you about the documentation trap. Many facilities treat the DHA as a compliance document they produce once and file away. That is a mistake. The analysis needs to be revisited whenever you change materials, modify equipment, or alter process conditions. I reviewed a DHA at a fertilizer plant where they had switched from ammonium nitrate to a different blend three years earlier, but nobody updated the hazard analysis. The new blend had a significantly lower MIE and higher deflagration strength. The existing venting was undersized for the new material. We caught it during a routine audit before anything happened, and it cost us a weekend of re-venting and a few thousand dollars. Doing it proactively saved them from a potentially catastrophic event and a lot more money later. If you are doing this yourself, start with the material data, then map the facility, then work through each piece of equipment systematically. Don't skip the housekeeping assessment. Don't assume your existing protection is adequate just because it was installed during construction. And for the love of whatever you respect, verify your isolation device response times against your actual system parameters.
Get the Full Details