Why Nobody Can Agree on What a 2-Inch Pipe Actually Is
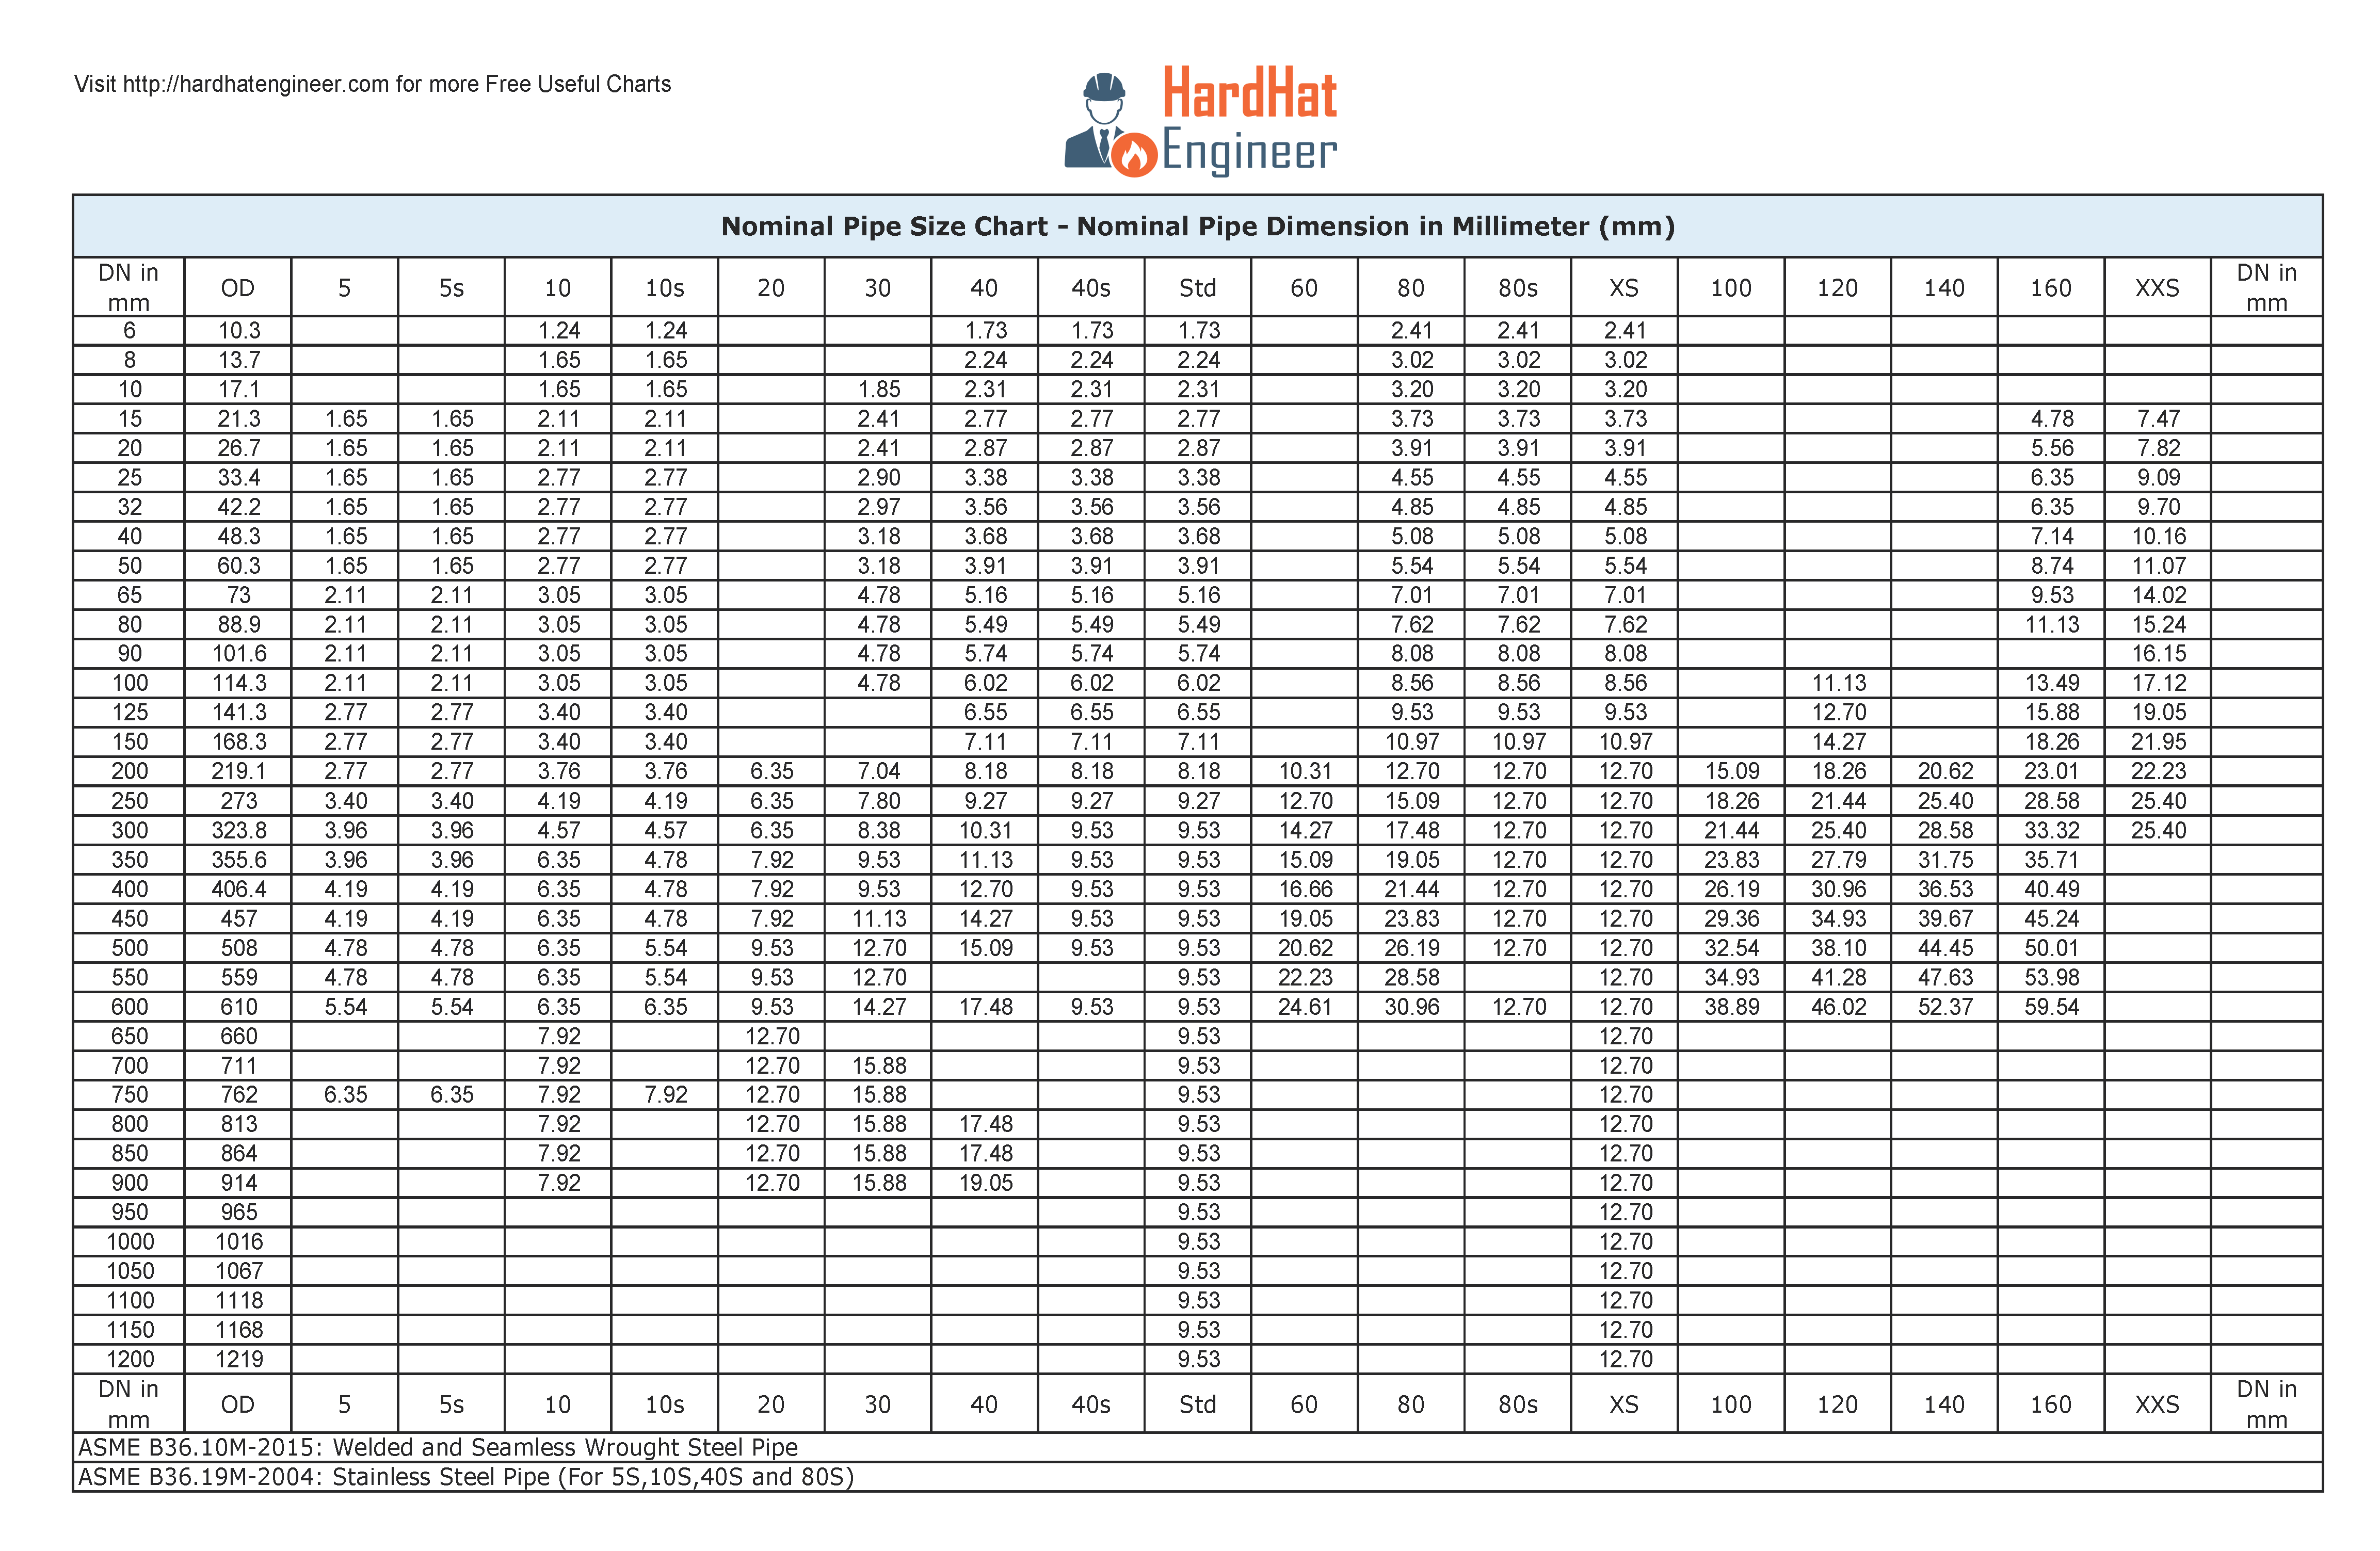
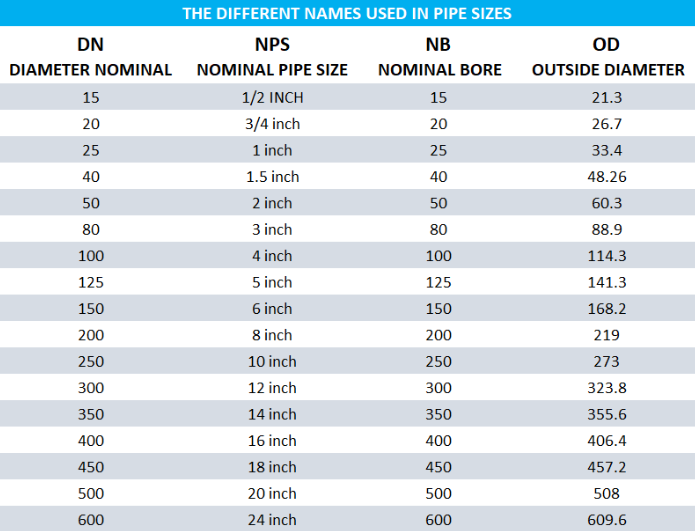
The Nominal Pipe Size system is one of those things that sounds simple until you try to use it, then realize you've been working with incomplete information for three years. A 2-inch nominal pipe isn't 2 inches in diameter. It isn't even close. The actual outside diameter is 2.375 inches for anything from 1/8 inch through 3 inch nominal size. At 4 inches, the OD jumps to 4.5 inches and stays consistent across all wall thicknesses. That inconsistency is what trips up everyone who encounters this for the first time on a real job site. I learned this the hard way when I was specifying flanges for a process piping revision at a water treatment facility. I pulled a standard ASME B36.10 chart, saw "8-inch NPS," and assumed the OD was 8 inches. My fabricator came back to me with a 45-minute silence that said everything, then pointed out the flange bore literally wouldn't align with the pipe. We ended up cutting a makeshift adapter plate out of 3/4 inch A36 steel because the order had already been placed and the lead time on replacement flanges was six weeks. The adapter held for two years before we did the proper conversion. That cost us about eight thousand dollars in lost downtime we could have avoided with a single phone call.
Where to Find a Reliable Nominal Pipe Size Chart
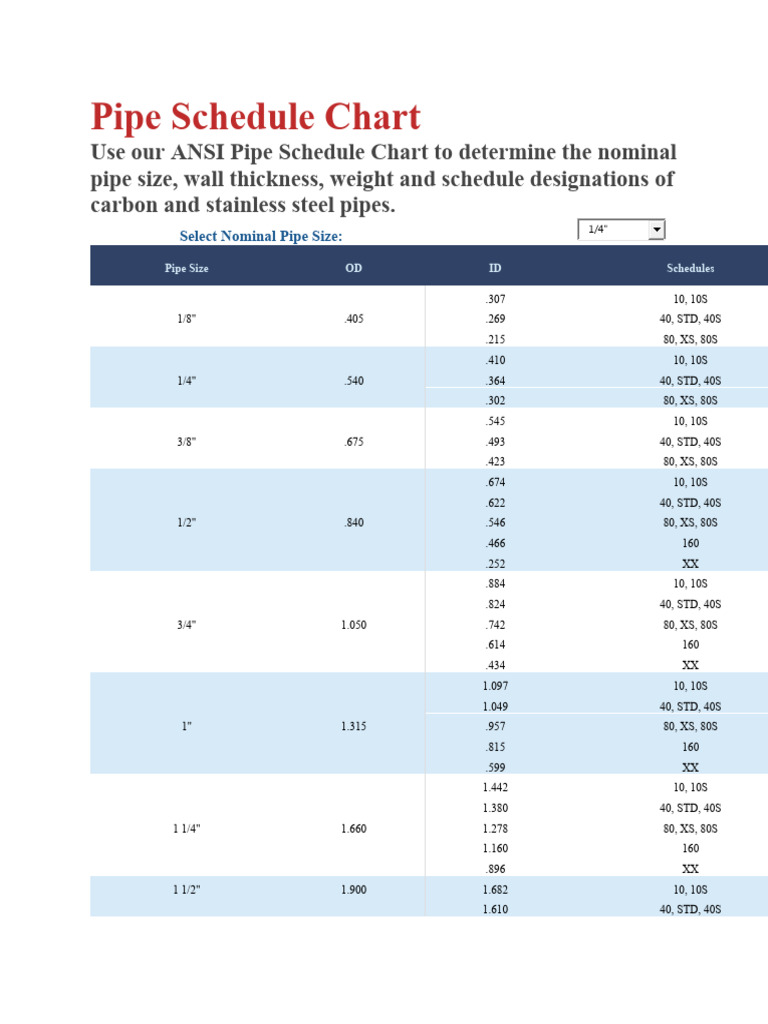
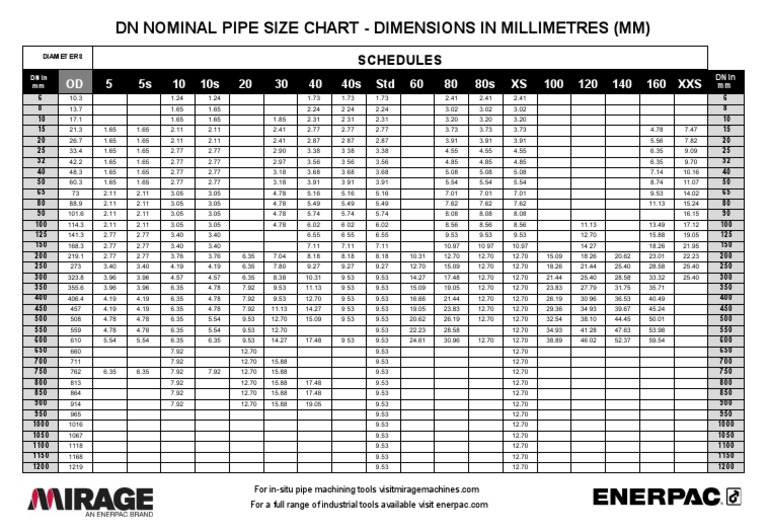
The authoritative reference is ASME B36.10M for carbon and alloy steel, and ASME B36.19M for stainless steel. Both are available as paid PDFs from ASME's store, but you don't need to pay for them if you're just looking up sizes. The full tables are replicated without modification in every reputable engineering handbook and on sites like Engineering Toolbox and piping-specialists.com. The catch is that free charts often omit the scheduled wall thickness columns beyond Sch 40, which is where things get complicated quickly. When you need Schedule 160 or Double Extra Strong dimensions, the free resources tend to drop the data or present it in a format that requires cross-referencing between two different tables. I keep a printed copy from Crane Technical Paper 410 on my desk because it lists every schedule from 5S through XXS in one continuous table with OD, ID, wall thickness, and weight per foot all on the same row. That saves me from flipping between charts during takeoff. If you're doing something more involved than a quick lookup, I'd recommend the PIPESIZE calculation tool from the Pressure Piping Institute, which let's you pull any combination of NPS, schedule, and material and spits out inner diameter, cross-sectional area, and flow capacity in one go. Takes about thirty seconds per entry versus the manual lookup that runs five to eight minutes depending on how lost you get between columns.
How to Read the Chart Without Making Expensive Mistakes
Nominal Pipe Size is a labeling convention, not a dimensional one. The number attached to it roughly indicates the inside diameter of early copper tubing that the system was modeled after, but that relationship stopped being accurate somewhere around the 1920s. What actually controls the geometry is the outside diameter, which is fixed for each NPS designation regardless of schedule. The wall thickness varies by schedule number, and that variation determines the inside diameter, flow area, and pressure rating. Here's the thing most charts don't emphasize enough: schedule numbers aren't linear measurements of wall thickness. Sch 40 and Sch 80 for the same NPS don't follow any simple ratio. A 6-inch Sch 40 pipe has a wall of 0.280 inches. A 6-inch Sch 80 has a wall of 0.432 inches. That's a 54 percent increase in wall thickness for what looks like a modest jump in schedule number. Meanwhile, going from Sch 80 to Sch 160 on the same 6-inch pipe adds another 0.280 inches of wall, bringing you to 0.718 inches total. The schedule number itself doesn't tell you wall thickness directly. You have to read the table. One practical detail people miss: for NPS 1/8 through NPS 12, the OD stays fixed at the values listed in the chart. Starting at NPS 14 and above, the OD equals the NPS number in inches. So a 14-inch nominal pipe has an actual OD of 14 inches, and a 24-inch nominal pipe has an OD of 24 inches. This transition at 12 to 14 inch is not arbitrary. It reflects a shift in how the sizing convention was historical standardized, and it's the single most common source of off-by-one errors when someone switches from small-bore to large-bore piping without rechecking their assumptions.
Get the Full Details
What the Chart Won't Tell You (And What You Need Instead)
The Nominal Pipe Size Chart gives you dimensions. It does not tell you whether a given pipe will handle your design pressure, whether the material is compatible with your process fluid, or whether the weld joint efficiency factors applicable to your construction code will derate the pressure capacity below your required margin. For that you need ASME B31.3 process piping calculations, which require the actual wall thickness including mill tolerance and corrosion allowance, not just the nominal schedule dimension from the chart. A common mistake is using the nominal wall thickness from the chart directly in a pressure calculation. ASME B31.3 requires you to subtract the mill tolerance, which is 12.5 percent for seamless pipe and 10 percent for welded pipe, before applying the pressure formula. If your chart lists a 0.500-inch wall for Sch 40 8-inch, your design wall is actually 0.4375 inches after the seamless tolerance reduction. That's a meaningful difference in the allowable pressure, especially at higher schedules where the wall is already thin relative to the OD. Another edge case that the standard chart doesn't address directly is the existence of Standard Weight (STD) and Extra Strong (XXS) designations that predate the schedule numbering system. On older drawings, especially from facilities built before 1970, you'll see references to "3-inch STD pipe" instead of "3-inch Sch 40." They are effectively the same dimensionally, but the terminology mismatch causes confusion during plant turnarounds when contractors pull specs from old P&IDs and match them against new procurement tables that only use schedule numbers. I've seen two-day delays on instrument air line replacements traced back to a procurement officer who rejected a Sch 40 substitute for STD because the drawing called for STD and the supplier quoted Sch 40, not realizing they were identical.
Practical Takeoff Procedure That Actually Works
When I'm doing a quantity takeoff from a P&ID, I follow this sequence to avoid the usual gotchas. First, I identify every pipe class on the drawing and note the NPS and schedule for each. Second, I pull the corresponding OD from the chart and confirm whether it's in the fixed-OD range (NPS 1/8 to 12) or the matching-OD range (NPS 14 and up). Third, I record the actual wall thickness for the specified schedule, then apply the mill tolerance reduction if the pipe will be used in a pressure boundary calculation. Fourth, I check whether the schedule exists for that NPS, because some schedule combinations simply aren't manufactured. NPS 3 Sch 30 exists as a standard size, but NPS 3 Sch 100 does not have a published dimension in B36.10 because it falls between Sch 80 and Sch 160 with no industry demand. The fifth step is where most people skip ahead and regret it. I verify that the fittings, flanges, and valves I'm specifying match the pipe OD, not the nominal size. A 4-inch Sch 100 flange has the same bolt circle and OD as a 4-inch Sch 40 flange because both are based on the same 4.5-inch pipe OD. But the gasket seating area and bore diameter are different, so you can't assume interchangeability just because the nominal size matches. I had a contractor on a refinery turnaround who tried to install Sch 40 gaskets on Sch 100 flanges and ended up with a leak that took four hours and a replacement gasket to fix during a window that had already been shortened by weather delays. The chart itself is straightforward to use once you stop treating the nominal size as a measurement. It's a lookup table for a standardized labeling system that predates modern engineering computation by nearly a century. The value comes from understanding what the numbers represent and what they don't, then applying the correct corrections for your specific design or procurement need. Everything else is just reading columns.