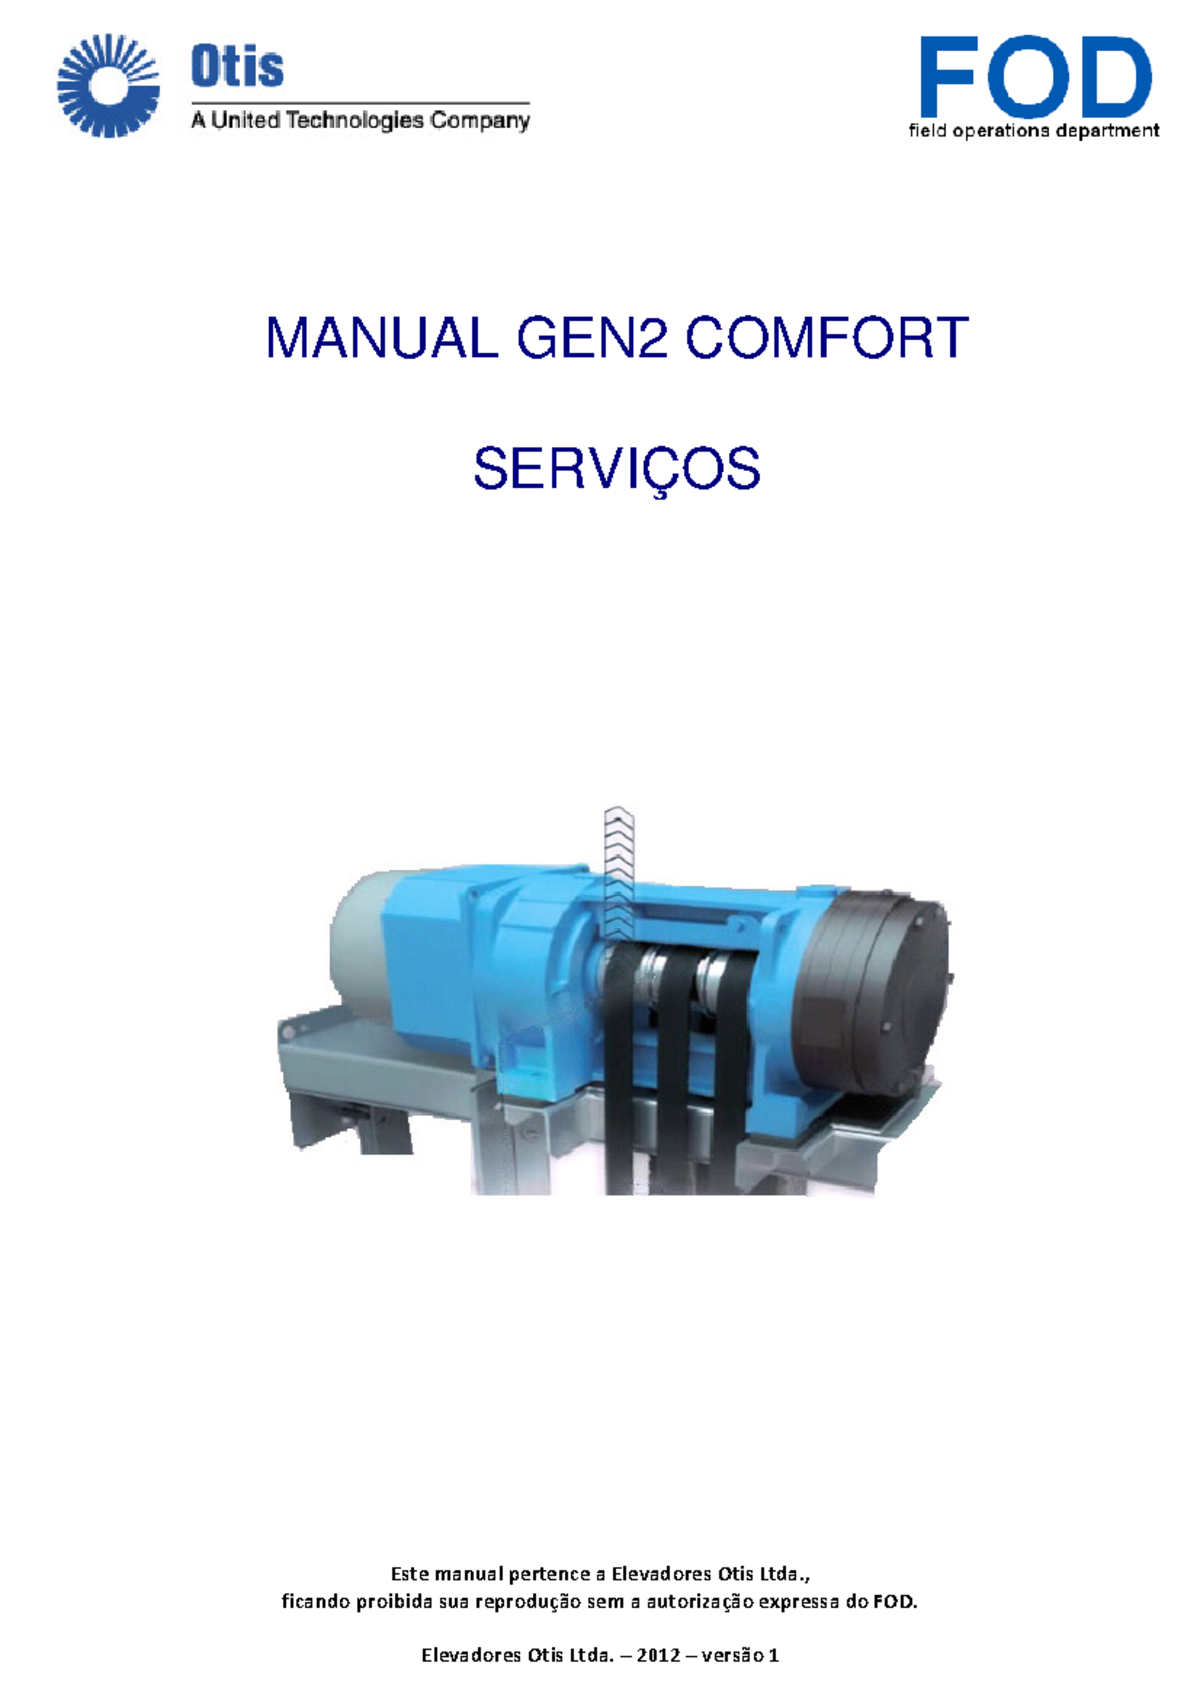
Working With the Otis Gen2 Elevator System
The Gen2 is an Otis brandless rope traction system. It uses a flat polyurethane belt wrapped around a grooved sheave and a smaller idler pulley. The belt has rubber teeth that mesh with the sheave grooves. That lets it run without the steel ropes most elevators use. The machine is typically mounted at the bottom of the hoistway instead of on top. That changes the geometry enough that service procedures are different from a standard traction setup. Otis doesn't publish their full service manuals publicly. You'll find them through authorized channels: the Otis dealer network, their internal service portal, or third-party resellers who've scanned and distributed them. If you're a licensed elevator mechanic working for an authorized company, request one through your regional field office. They'll usually get you a digital copy within a couple days. Unauthorized distributors sell PDFs online, but those copies are often outdated or missing addenda. A manual from 2014 won't cover the revision updates from 2019. Always check the revision date against the serial number of your specific unit. I learned that the hard way. I was troubleshooting a Gen2 controller fault code on a building in downtown Chicago. The manual I had recommended checking continuity on a relay that wasn't even installed on my machine version. The relay had been eliminated in a later hardware revision. The correct fix was just a loose ground strap on the I/O board. I wasted two hours flipping through pages that didn't apply. After that I started cross-referencing every component listed in the manual with the actual nameplate and hardware tag on the unit before following any procedure.
How the System Actually Works
The Gen2 uses a permanent magnet synchronous motor connected directly to the sheave. There's no gear box. That's the whole point of the design. The flat belt runs at a ratio that gives you higher roping than a traditional system, so the motor doesn't need to produce as much torque. The trade-off is that the belt tension has to be managed differently. You can't just adjust rope tension like you would on a standard traction machine. The belt is tensioned by the car and counterweight arrangement, and the system relies on the belt's own elasticity and the grooved sheave to maintain grip. The controller is typically an Otis OI-1 or OIA platform. It reads position from an encoder on the machine. Travel calculation is automatic once the initial parameters are set. That's where people run into problems. If the travel distance or floor count is entered wrong during commissioning, the elevator will stop at floors with noticeable offset errors. I've seen cars land three inches above or below the landing level because someone copied the travel parameter from a different building's specs. Always verify floor heights with a tape measure, not from a drawing.
Common Problems and What the Manual Actually Says
Belt wear is the main thing to watch. The polyurethane teeth degrade over time, especially in hot hoistways. The manual gives a replacement interval, usually around 15 to 20 years depending on cycles and temperature. But that's a general guideline. I've pulled belts at eight years that were glazed and cracked on the underside because the hoistway ventilation was inadequate. The machine room temperature ran over 120 degrees Fahrenheit. That cuts belt life dramatically. The manual mentions temperature as a factor but doesn't give specific derating charts. You'll figure that out by inspection. Another issue is the idler pulley bearing. These tend to fail between years five and eight. The sound is distinct: a low rumbling that gets louder as the car moves. The manual lists a bearing part number and installation torque. The trick is that you have to remove the machine from the mounting frame to replace it. On a Gen2, the machine is at the bottom of the hoistway. That means working overhead on a scaffold or lift, which slows the job considerably. Budget extra time for that. A bearing swap that looks like a two-hour job on paper usually takes a half day once you factor in safety setup and machine support. Controller communication faults are the third common complaint. The OI-1 uses a serial communication bus between the controller and the input/output board. Intermittent comms errors show up as random floor display glitches or loss of direction indication. The manual tells you to check the ribbon cable connections. Most of the time that's not it. The real culprit is usually a poor ground connection between the controller enclosure and the machine frame. I found this on a Gen2 in a renovated building where someone had replaced the grounding electrode conductor with aluminum wire instead of copper. The ground impedance was too high. The comms errors stopped after I installed a proper copper ground strap between the controller cabinet and the machine base. The manual doesn't cover that scenario because it assumes the grounding is correct per code.
Get the Full Details

Commissioning the Gen2
Commissioning is where the manual is most useful. You need to run the automatic travel measurement routine first. That teaches the controller the exact position of every floor. Make sure the car and counterweight are stationary during the measurement. Any vibration or drift will throw off the calibration. After the measurement completes, you'll run a leveling adjustment. This fine-tunes the stop position at each floor. The manual walks you through the process step by step, but it assumes you understand what the parameters mean. The leveling tolerance is typically plus or minus a quarter inch. Anything outside that range will fail inspection in most jurisdictions. One thing the manual doesn't emphasize enough: the counterweight ratio matters more on a Gen2 than on a conventional system. Because the flat belt has less friction capacity than steel rope, an improperly balanced car will slip the belt under heavy load. The recommended counterweight is 40 to 50 percent of the rated payload. Going below 40 percent is risky if the building has high traffic patterns. I saw a Gen2 in a hospital where the counterweight was set too light. Under full load, the belt would occasionally slip during acceleration, triggering a fault. They ended up adding weight to the counterframe to bring it into the proper range.
Limitations of the Design
The Gen2 isn't a perfect system. The belt is sensitive to contamination. Oil or grease in the hoistway from a leaking hydraulic fixture above can degrade the polyurethane. Once that happens, there's no cleaning procedure that restores the belt. You have to replace it. The machine placement at the bottom of the hoistway also means less headroom above the car, which can be a problem in buildings with limited overhead clearance. And the motor is more expensive to replace than a standard traction machine. A complete motor and sheave assembly runs significantly more than a conventional geared or gearless replacement. For newer installations where the building design accommodates the bottom-mounted machine and the duty cycle isn't extreme, the Gen2 is a solid choice. Energy consumption is lower than a comparable geared system, and maintenance intervals are longer if the environment is controlled. But if you're dealing with an existing installation that's showing belt wear or controller issues, the cost of parts and the specialized nature of the service can make a full machine replacement more economical than continuous repair. That's a decision your owner will want to make with hard numbers, not guesswork.