What You Are Looking At When You Open The Cabinet
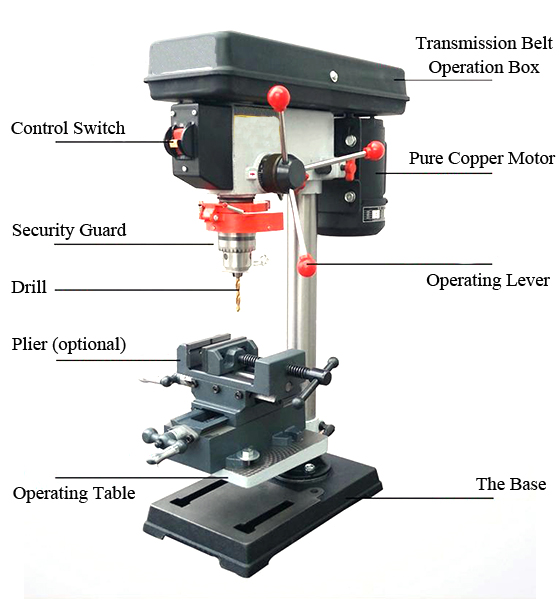
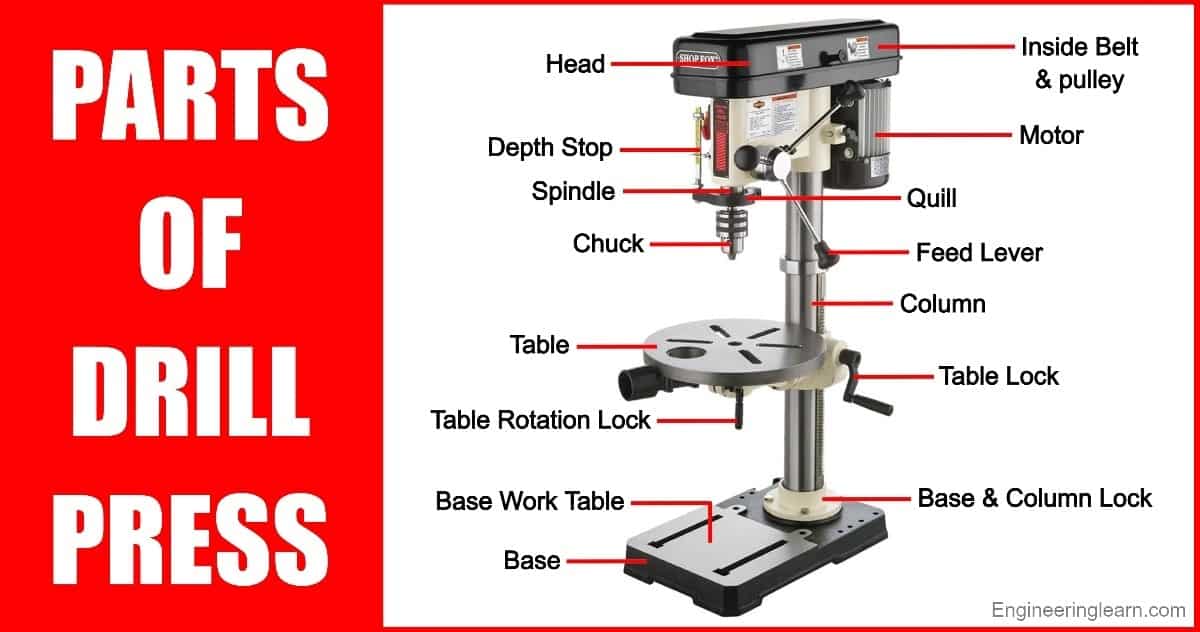
A drill press is not complicated, but most people buy one and then spend two years learning why their holes are always slightly wrong. I have fixed more misaligned bits than I care to count. The machine itself has ten functional sections and about forty fasteners holding them together. Here is what matters. The base is a flat cast-iron plate, usually six to eight inches thick. It anchors everything. I once worked in a shop where the base had micro-fractures from repeated impact loading and every hole drifted two thousandths per inch deeper in the workpiece. You cannot fix that with calibration. You replace the base or bolt the press to a separate massive table. The column is the vertical steel post. It should be hard-chrome plated. Raw steel columns develop rust pits within six months in any shop with humidity, and those pits score the quill sleeve as it moves up and down. I strip and re-chrome my columns annually. Takes forty minutes with a fine abrasive pad and some automotive touch-up compound.
The quill is the hollow spindle that moves vertically inside the sleeve. It houses the drawbar spring and the locking mechanism. The quill diameter is what matters for rigidity, not the overall size of the machine. A 1-inch quill on a 15-inch drill press will deflection more than a 1.25-inch quill on a 10-inch model. Check the spec sheet for quill diameter, not just table size. The chuck is where people go wrong most often. Keyless chucks are convenient until they are not. I switched to key chucks on every job requiring consistent torque, because keyless chucks creep open under lateral load and that is what causes bit walk on hard materials. A three-jaw key chuck with brass jaws loses less than half a thou per month if you clean the jaws weekly. The spindle speed range is determined by the motor pulley and the belt position. Most consumer presses give you six speeds. Industrial models give you twelve or sixteen. I run most operations between 800 and 2400 RPM depending on material and bit diameter. The chart on the side of the machine is a suggestion, not a law. You can go faster on aluminum and slower on steel without breaking anything, within reason.
The Table And Its Attachment System
The table slots onto the column and bolts at the bottom. It tilts on a pivot plane, usually between negative five and positive forty-five degrees. The tilt lock should have a coarse adjustment bolt and a fine lock nut. If your table sags when unlocked, the pivot bushing is worn. Replacing that bushing costs about eighteen dollars in parts and twenty minutes of your time. I have seen people replace entire tables for this. The table insert is a replaceable metal plate around the bit. It catches chips and prevents them from falling into the quill mechanism. On cheaper presses this is stamped steel and warps within a year. I made my own from half-inch aluminum plate and drilled a one-inch clearance hole. It seats flush, does not flex, and has lasted eleven years. The fence, if your press has one, attaches to the table and guides long workpieces. Most built-in fences are useless beyond four inches of width. I fabricated a T-slot fence from extruded aluminum and mount it separately. It takes thirty seconds to position and provides zero play across the full table width.
Get the Full Details
The Motor And Drive Components
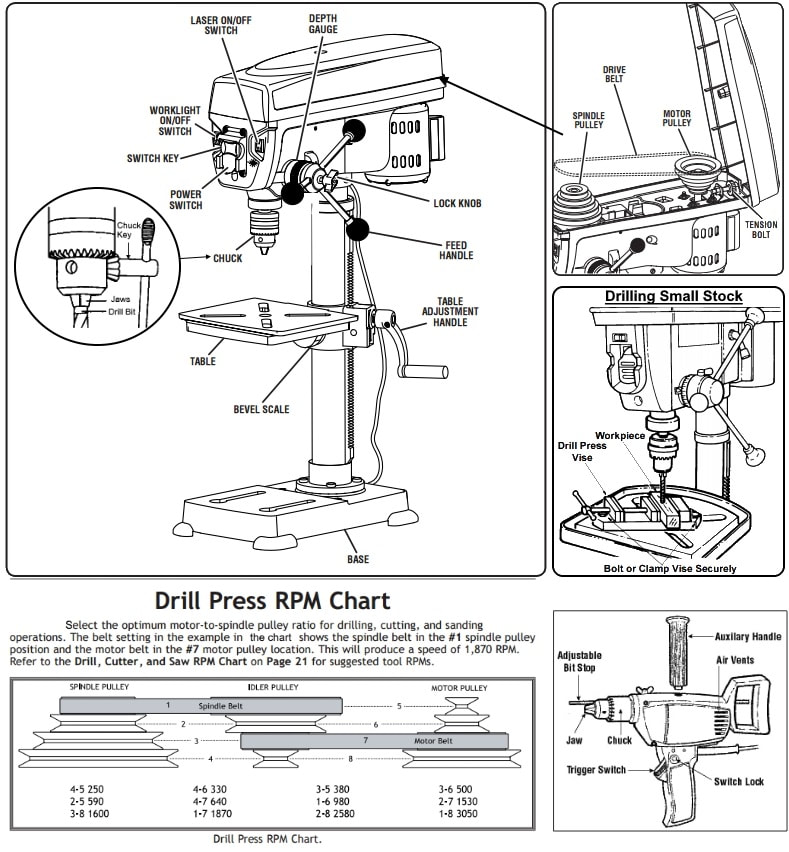
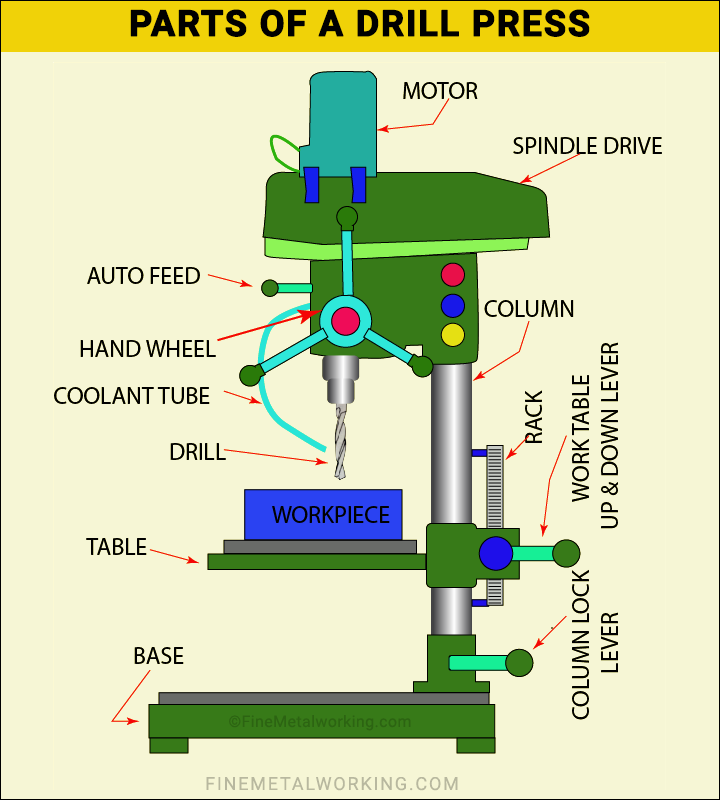
The motor is mounted on a hanger bracket that hangs from the head assembly. Belt tension is adjusted by loosening the bracket bolts and shifting the motor. There is usually a tension gauge sticker on the inside of the access panel. If there is not one, the standard is about one-half inch of deflection at the midpoint of the longest belt run. More than that and you are burning bearings. Less and the belt slips under load. The belts themselves are V-belts, usually A or B section depending on the model. I keep a spare set on hand because a glazed belt transfers power poorly and introduces vibration that shows up immediately in hole finish quality. I change belts annually regardless of visible wear. They cost about six dollars a pair. The motor mount bolts are the first thing to back out on any press that sees daily use. I thread-lock them every time I adjust belt tension. Not replacing them immediately after overtightening will cause the motor to walk forward during operation and change the effective belt length unpredictably.
The Head Assembly And Quill Mechanism
The head contains the quill drive gears, the depth stop mechanism, and the spring return. The depth stop is a threaded rod that contacts the top of the quill housing. You set it by lowering the bit until it touches the workpiece, then tightening the lock nut against the stop collar. The problem is that thermal expansion changes the effective depth by about two thousandths over a four-hour shift in summer. If you are drilling stacked panels where depth consistency matters across the batch, you need to re-check the stop every hour. The quill spring is a heavy compression spring inside the quill. It returns the quill upward when you release the feed lever. When this spring fatigues, the quill will not fully retract and chips pack between the quill and the sleeve. I clean and lubricate the spring every six months with a light machine oil.WD-40 is not a lubricant for this application. It attracts dust and gums up within weeks. The feed lever has a grease fitting on most industrial models. I hit it twice a month withNLGI grade 2 lithium grease. The lever pivot on cheaper models has no fitting and relies on sealed bushings that wear out irreversibly. If your lever feels notchy, the bushing is shot and the only fix is replacement of the feed arm assembly.
The Locking And Safety Features
The quill lock is a T-handle or lever that clamps the quill in place. It is meant for boring bar operations or when you need to remove the chuck. Most people leave it engaged because it is easier, and that is a mistake. An engaged quill lock transfers shock loads directly into the sleeve bearings every time you start or stop the motor. Disengage it whenever you are drilling. The on/off switch should have a momentary action or a keyed start. I have seen presses with switches that stay latched in the on position after a power flicker, which means the machine restarts unexpectedly when power returns. This is a real hazard. I install an external key switch on every press in my shop and keep the key in my pocket while working.

What To Do When Holes Are Out Of Position
I spent three weeks troubleshooting a pattern of holes that drifted half an inch to the right as depth increased. The bit was centered. The chuck was concentric. The table was square. The problem turned out to be the column-to-base joint. The lock bolt had elongated the slot in the base over years of adjustment, allowing the entire column assembly to tilt minutely under the side load of a large bit. I replaced the base bolt with a larger diameter shear pin and the drift stopped immediately. The fix cost seven dollars and took twelve minutes. Drill presses are rigid and accurate for vertical holes in stationary workpieces. They are terrible for hole patterns that require frequent repositioning, for angled holes beyond forty-five degrees, or for materials thinner than a quarter inch where the bit will grab and spin the work. For thin sheet metal, use a bench mill or a hand-held drill with a jig. For angled holes, use a milling machine with an angle plate. The drill press is a specialist, not a generalist. The quill sleeve bearings wear before anything else on a machine used more than an hour a day. Replacement bearings cost about twenty-five dollars and require pressing out the old ones and seating the new ones with a socket and hammer. If you feel lateral play in the quill when you push it side to side at full extension, the bearings are gone. Do not wait. A worn bearing allows the quill to wobble, which translates directly into hole diameter variation of ten to twenty thousandths.
The depth stop thread strips most commonly on machines without an adjustable stop collar. The fix is to install a brass insertion collar and thread it separately. This prevents the aluminum stop tube from taking the threading damage. I keep a parts diagram from the manufacturer on file for every press I own. When something fails, I order the exact part number rather than guessing. Generic replacements rarely match the tolerances and cause more problems than they solve.