The Basics Nobody Tells You
Before you even touch a pipe bender, you need to understand what you're actually doing. A pipe bender forces material into a curve by displacing it on the outside of the bend while compressing it on the inside. The centerline stays roughly the same length, but the walls don't. That's where problems start. I've seen people skip the layout marks because they think they can eyeball a 45-degree bend. They can't. You'll end up with something closer to 42 or 48 depending on your machine, your material, and the time of day. Mark everything. Use a protractor or a digital angle finder if you have one. Layout dye works better than a marker on steel, and a scribe works better than either on aluminum. The bend radius is the single most important spec. Most benders are rated for a minimum bend radius of two to three times the tube diameter. Going tighter than that without a mandrel bender will collapse the tube. Period. I once tried a tight-radius bend on half-inch EMT conduit with a standard handle bender and got a nice flat spot that looked like a pancake. It happened in under three seconds.
Pipe Bender Instructions for Common Applications
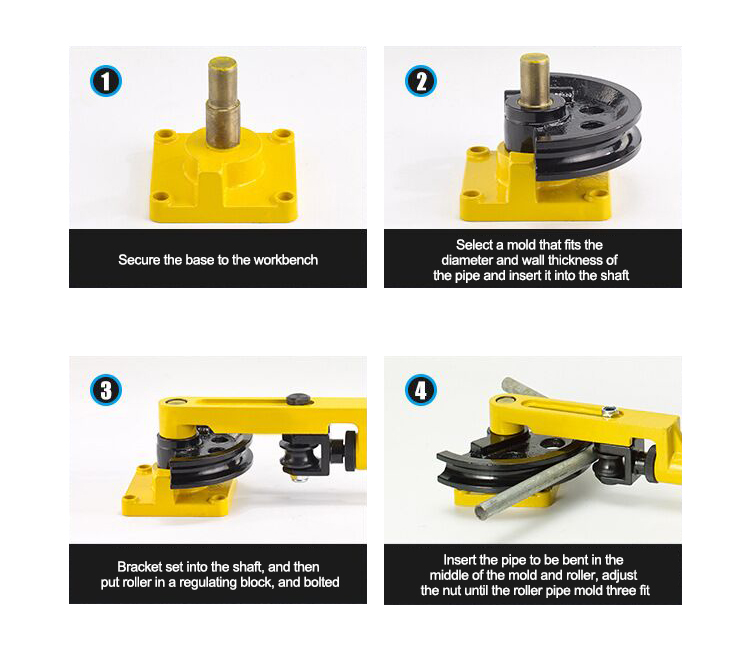
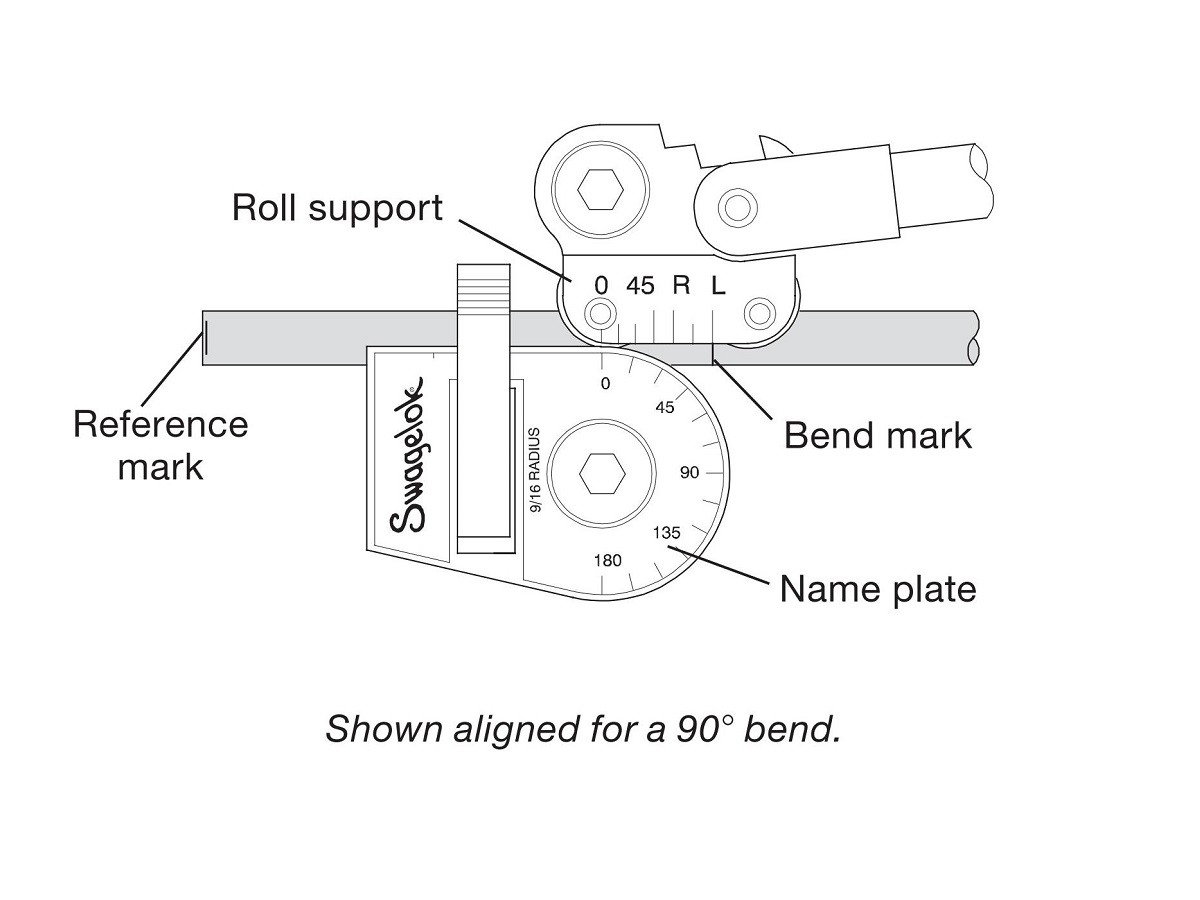
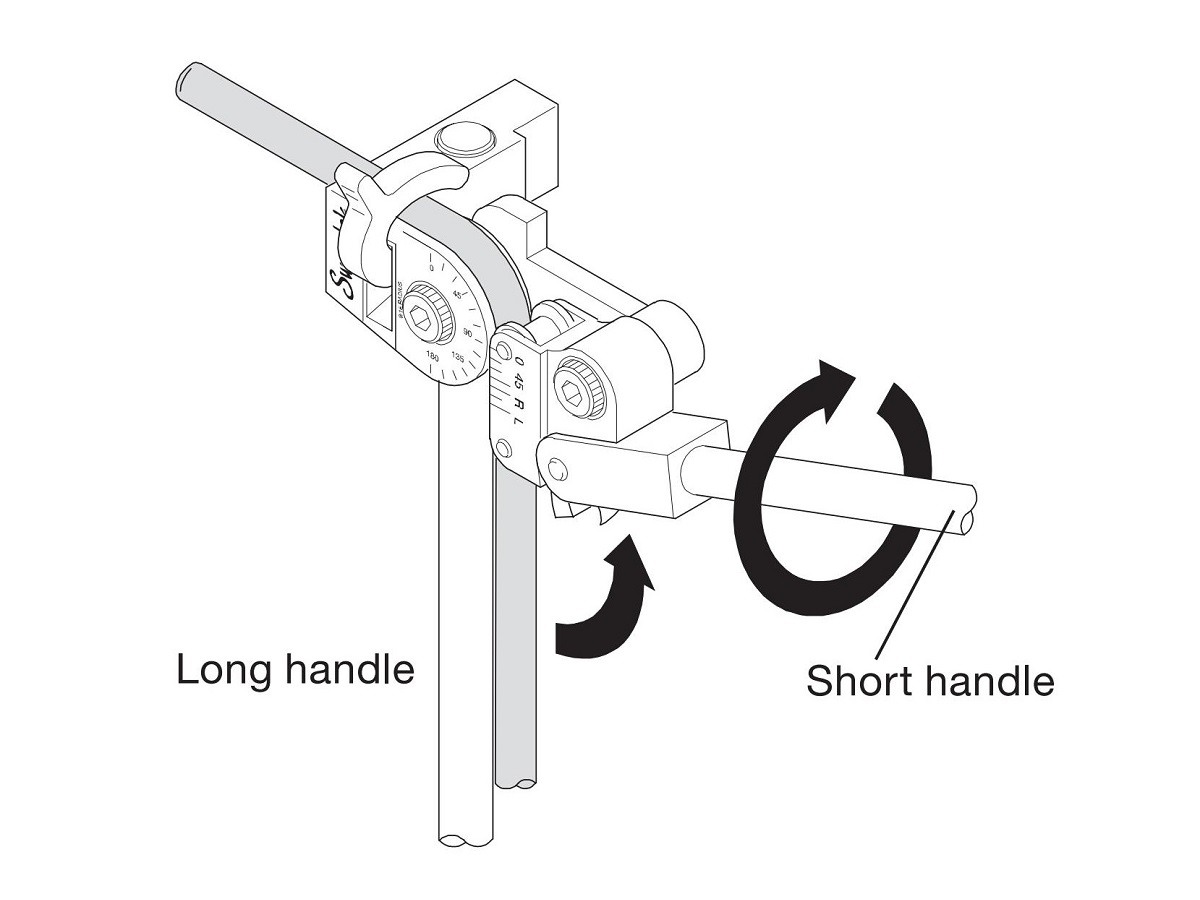
Here's how this actually works in practice. First, measure the straight sections you need. The bent portion adds length to your overall piece compared to what the blueprints might show. This is called bend deduction, and it varies by material, wall thickness, and die set. The standard approach is to calculate the developed length using the bend angle and the neutral axis shift. For soft materials like copper or aluminum, you can often bend by hand with a simple ram-style bender. For steel, especially anything over quarter-inch wall, you'll need a hydraulic bender with proper dies. The die needs to match the tube OD within a hundredth of an inch. A loose die means an inconsistent bend radius and a lot of tangling later. A die that's too tight will dent the tube before you even start bending. The process itself is straightforward: position the tube against the stop pin, align your bend mark with the die centerline, apply pressure smoothly, and release. Don't jerk the handle. Smooth, steady force gives you a consistent bend. Jerking it will give you a kink, a wrinkled outer radius, or worse, a cracked weld on pre-welded tubing if you're working with DOM or ERW pipe.
I ran into a specific issue last year when bending 2-inch Schedule 10 stainless on a machine that was calibrated for Schedule 40. The bender would stop at the marked angle, but every third bend would come out two degrees short. The problem was the spring return on the wiper die wasn't keeping consistent contact with the thinner wall. The workaround was to wrap a layer of brass shim stock around the tube at the wiper die contact point. It took maybe thirty seconds per bend and eliminated the variation entirely. Not a permanent fix, but it got the job done.
Get the Full Details
What Goes Wrong and How to Avoid It
Wall thinning on the outer radius is unavoidable to some degree. In a tight bend, you can lose ten to fifteen percent of your wall thickness at the outside of the curve. If you're working with pressure-rated pipe, that matters. Check your code requirements. ASME B31.3 has specific rules about how much wall loss you can accept depending on your service conditions. Wrinkling on the inner radius happens when you don't have enough support during the bend. A mandrel bender solves this for small-diameter tube. For larger pipe, you're looking at a rotary draw bender with a mandrel, or in some cases a filler inside the tube. I've bent three-inch stainless with a powdered filler before. It's messy, expensive, and absolutely necessary when you can't use a mandrel bender and need a clean inside surface. Ovalization is the silent killer. Even when a bend looks fine from the outside, the cross-section might be slightly elliptical. This reduces flow capacity and can cause problems downstream if you're running fluid through the line. A simple caliper check across multiple axes after bending will tell you if your bender setup is producing acceptable results.
Springback is real and it varies by material. Stainless springback is significantly higher than carbon steel. Aluminum is moderate. The trick is to overbend slightly and let the material relax back to your target angle. For a 90-degree bend in 304 stainless, you might need to go to 92 or 93 degrees depending on the radius and wall thickness. You learn this through trial and error with your specific setup. There's no universal correction factor.
Where to Get Detailed Documentation
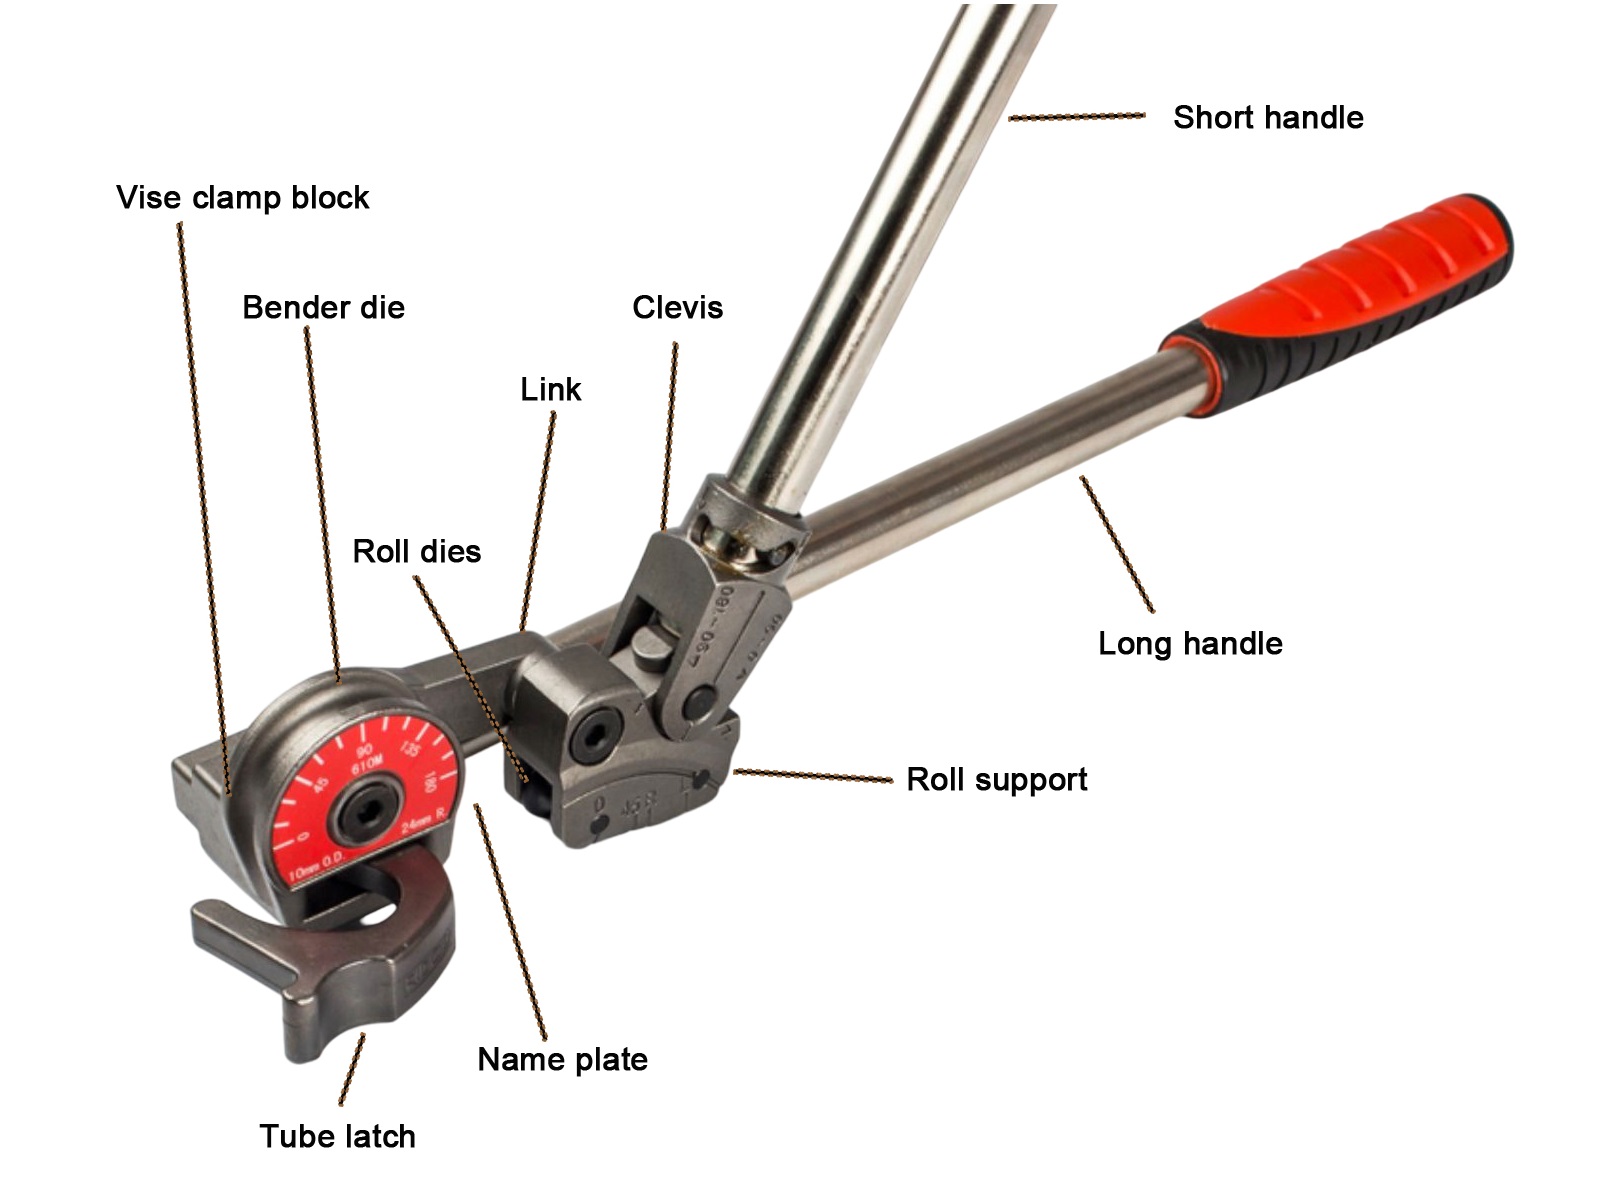
If you need comprehensive Pipe Bender Instructions for your specific machine and material combination, the best source is always the manufacturer's manual. Most major bender manufacturers like Swagelok, Parker, or local industrial suppliers provide detailed technical bulletins online. These documents include recommended die sets, pressure settings, and material-specific guidelines. For hydraulic benders specifically, look for the manufacturer's specification sheet that lists the tonnage rating, die inventory, and max bend angles. The Tonnes per inch chart is useful when you're trying to figure out whether your bender can handle a given material size. If you're bending something at the upper limit of your machine's capacity, reduce your bend angle or split it into multiple passes. Free downloadable guides from industry associations like the Tube Fabricators Association or OSHA's bending safety guidelines cover the procedural side. These are worth bookmarking. They don't replace your machine's manual, but they fill in gaps around safety, setup procedures, and inspection criteria.
The Things You Won't Find in Any Manual
Temperature matters more than most people realize. Bending cold-hardened stainless at room temperature is fine for small bends. Try it on large-radius bends in thick wall, and you'll work-harden the material right where you're trying to bend it. The tube will crack. Warming the material to maybe 300°F with a propane torch before bending can help in those cases, but you need to anneal afterward if the application requires corrosion resistance. That means solution annealing and quenching, which is a whole other process. The lubricant choice is another thing nobody talks about enough. Cutting oil or dedicated bending compound on the die contact points reduces friction and extends die life. Using nothing at all will accelerate wear and give you inconsistent bends. WD-40 is not a bending lubricant. It evaporates too quickly and doesn't provide adequate film strength. Finally, maintain your equipment. Clean the dies after every use. Check the stop pins for wear. Inspect the hydraulic lines for leaks. A bender that's not properly maintained will produce inconsistent results regardless of how well you follow any instruction set. I've spent hours troubleshooting bends that turned out to be caused by a worn stop pin that had drifted by a sixteenth of an inch. The pin looked fine. The bender was just a sixteenth of an inch off and nobody noticed until we measured the output pieces against the drawing.