Getting Started With Screw Compressor Training
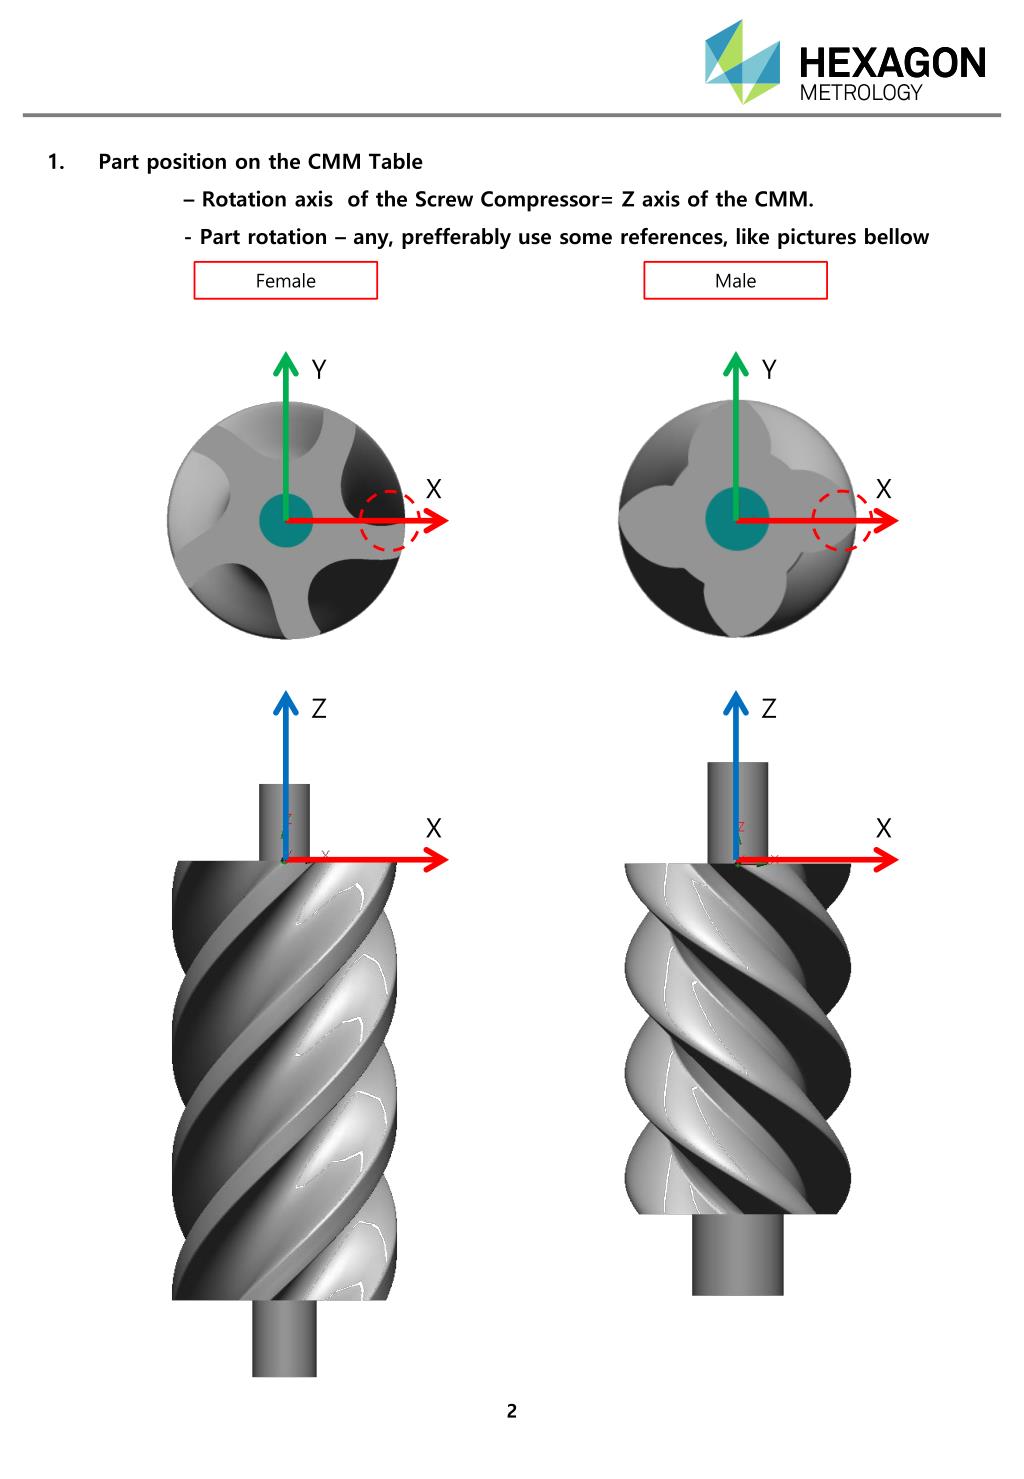
Most people treat compressor manuals like reference books they never actually read until something breaks. That is the wrong approach. A screw compressor is not a simple on-off device, and when it fails, it takes half the production line with it. I have seen it happen too many times. The basic principle behind a twin-screw compressor is straightforward enough: two rotors mesh inside a housing, trapping air between the screws and the casing, then pushing it toward the discharge port. As the volume decreases, pressure increases. Simple physics. The problem is that everything downstream of that compression stage involves oil, seals, bearings, valves, and controls that all need to work together under heat and vibration.Screw Compressor Training Manual Essentials
When you are putting together training for operators or maintenance staff, you need to cover the following areas in order. Do not skip around. People remember sequences better when they follow one. Start with the basics of how the air end works. Explain the rotor profiles, why oil is injected directly into the compression chamber, and how the oil acts as both a sealant and a coolant. Most people do not understand that without oil, a screw compressor would seize in under thirty seconds. Then move to the oil circuit: the oil filter, the cooler, the thermostat valve, and the return lines. This is where most breakdowns originate. After that, cover the intake system. Air filters, intake valves, unloader valves, and minimum pressure valves. These are service items. Show people how to inspect them and what the wear patterns look like. The control panel section is where most training falls apart. Operators need to understand what every button and alarm means, but they also need to know what not to do. I had a site manager once who kept hitting the emergency stop on a running compressor because he thought it was a normal shutdown procedure. That wore out the contactors within weeks and caused a phase imbalance that took out a bearing. The manual should clearly state: emergency stop is for emergencies only. For maintenance scheduling, break it down by hours. Every 2,000 hours: change the oil separator element and the oil filter. Every 4,000 hours: replace the air intake filter and inspect the belt or direct drive coupling. Every 8,000 hours: check the rotor bearings and inspect the oil cooler for coking. Every 16,000 hours: consider a full overhaul of the air end if the specific power has risen more than ten percent from the original specification. Specific power is one of those metrics that everyone ignores until the electricity bill arrives. It is measured in kilowatts per cubic meter per minute of delivered air. If your compressor was rated at 6.0 kW/(m³/min) when it left the factory and it is now drawing 7.2 at the same output, something is wrong. That is a twenty percent efficiency loss. Most facilities do not catch this for years. One thing that almost no training manual addresses properly is the effect of ambient conditions. I worked at a plant in Arizona where the intake air temperature regularly hit 48°C in the summer. The compressor was rated for 35°C ambient. The unit was running at 110% capacity limit just to maintain downstream pressure, and the oil temperature was consistently near the shutdown threshold. The fix was not a bigger compressor. It was rerouting the intake to pull from a cooler location and adding a finned tube heat exchanger on the oil line. That dropped the operating temperature by twelve degrees and restored normal capacity within a week.Alarms and fault codes deserve their own section. Each manufacturer uses different numbering, but the categories are universal: high temperature, low oil pressure, motor overload, phase loss, and separator differential pressure. Train people to read the code, look up the meaning, and then check the most likely cause before calling a technician. A high temperature alarm is oil filter starvation eighty percent of the time. It is rarely the cooler itself. Filter replacement intervals should be based on differential pressure, not just time. A gauge across the intake filter tells you exactly when it is loading up. When the delta reaches the manufacturer's limit, usually around 25 millibar, change it. Some sites wait until the alarm triggers, which can be twice that pressure drop. The compressor is working significantly harder at that point, and the elements are often past the point of effective filtration anyway. If you want a practical template for building your own Screw Compressor Training Manual, start with the sections I outlined above and add your specific model's data sheets, alarm code lists, and spare parts numbers. Include photos of the actual components on your machines. Generic diagrams are useless to someone standing in front of a real unit trying to find the oil sight glass. A picture of the exact location on your compressor is worth more than three pages of text.