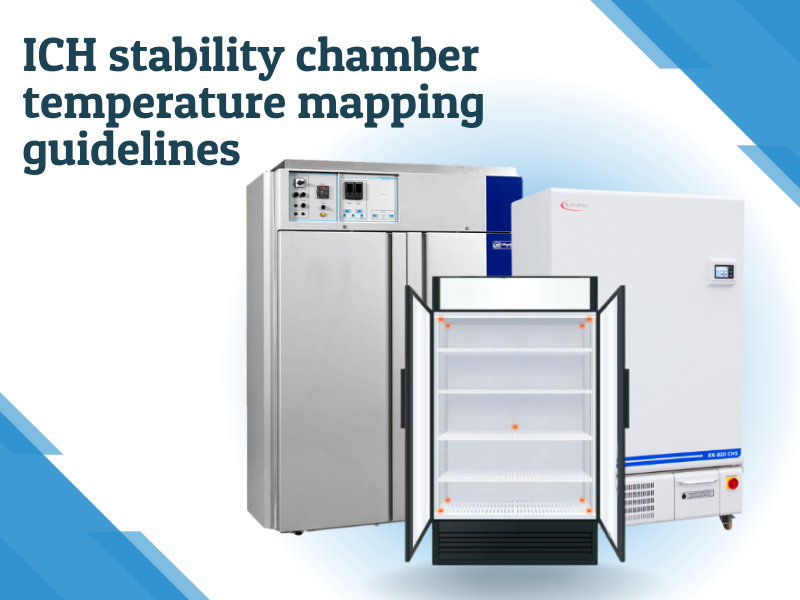
Why Temperature Mapping Actually Matters in Stability Chambers
Most people treat stability chamber mapping as a compliance checkbox. That is the fastest way to get it wrong. A stability chamber is not just a refrigerator with a timer attached. It is a complex environment where air flow, product load, defrost cycles, and door openings all interact in ways that are not always obvious. The Stability Chamber Temperature Mapping Guidelines exist because temperature gradients inside these chambers are real and they shift over time. I spent three years dealing with failed temperature mapping studies after bad vendors installed monitoring systems that didn't actually capture what was happening. The instruments were reading correctly, but they were placed incorrectly. That distinction matters more than anyone admits.
Stability Chamber Temperature Mapping Guidelines
The Core Method: What You Actually Need to Map
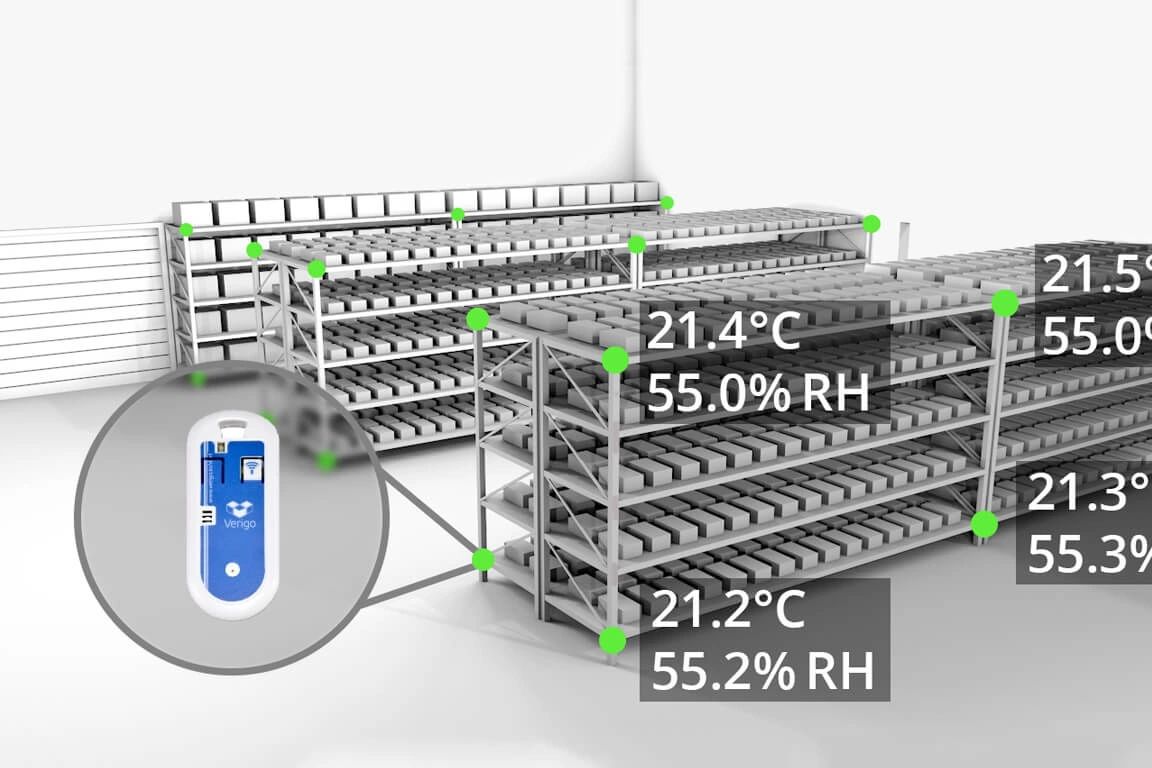
Temperature mapping involves placing calibrated data loggers throughout the chamber at strategic locations, then running the chamber under normal operating conditions for an extended period. The goal is to identify the coldest and warmest points, to understand how temperature fluctuates during defrost cycles, and to verify that every product location stays within the required range. Here is how you set it up without wasting money on unnecessary instruments. Use at least nine points for a medium-sized chamber: one in each corner near the floor, one in the center of each of the six faces, and one at the working height level in the middle of the chamber. For larger chambers, increase the grid density. The rule of thumb is no more than two meters between any two sensor points, but that number comes from ISO 12830 and some pharmacopeial guidance, not from thin air. You need sensors that are calibrated to a traceable standard. I have seen teams use uncalibrated PT100 probes bought from eBay and call it a day. That does not work during an audit. The calibration uncertainty should be less than half of your tolerance band. If your acceptable range is 2 to 8 degrees Celsius, your calibration uncertainty needs to be under 0.5 degrees. That means good quality loggers, not the cheapest ones you can find.
What the Industry Actually Requires
Different guidelines cover this topic and they overlap more than most people realize. The main references are: None of these documents are identical. They all agree on the basic principle that you need to characterize the temperature distribution in your chamber, but the specifics around sampling frequency, duration, and pass criteria vary. The EU GDP guidelines are more specific about the cold chain portion. The USP chapter is newer and covers both refrigerators and freezers. The ISO standard is the most widely cited for pharmaceutical storage conditions. For stability chambers specifically, you also need to consider ICH Q1A(R2). That document defines the test conditions for new drug substances and products: 25 C plus or minus 2 C and 60 percent plus or minus 5 percent relative humidity for long-term testing. Mapping a chamber set to 25 degrees is different from mapping one set to 2 to 8 degrees. The tight tolerance on a stability chamber makes the mapping much more demanding.
Get the Full Details

A Real Problem I Ran Into
Once I had a chamber where the average temperature across all sensors was well within spec, but the warmest point right next to the evaporator fan was spiking above 27 degrees during the fan cycling phase. The chamber controller was reading 25.1 degrees because its single sensor was in a dead zone. Nobody noticed until we did a full mapping study with fourteen sensors spread across all shelves. The workaround was to add supplementary mapping sensors near the return air duct and to run the mapping with the chamber fully loaded, not empty. Empty chamber mapping is misleading because the air flow pattern changes dramatically when you load product. The fans push air differently. Product blocks flow paths. The temperature gradient you see in an empty chamber is not the temperature gradient you see in a loaded chamber. That one chamber ended up with a confirmed cold spot near the back wall that only appeared when the door was closed and the fan was off. The defrost cycle added another layer of complexity. Every time the unit defrosted, a warm air pulse moved through the chamber and the sensors near the drain pan showed a temporary spike. Those spikes lasted about twelve minutes and went above 27 degrees. The question became whether those brief excursions were acceptable under your protocol. They were not, so we had to adjust the air flow settings and rerun the mapping.
How Long Does Mapping Actually Take
A proper mapping study usually takes between 48 and 168 hours depending on chamber size, the number of sensors, and what you are trying to prove. I recommend running at least 72 hours under steady state conditions. The first 24 hours is stabilization. The next 48 to 72 hours give you enough data to calculate averages, standard deviations, and to identify any transient events tied to the defrost cycle. If you are doing seasonal mapping, which is common in regulated environments, you should run mapping at both the high and low ambient temperatures that the room can reach. A chamber in a non-climate controlled room in Phoenix in July behaves very differently from the same chamber in Minneapolis in January. The ambient load on the cooling system changes the internal distribution pattern. I have seen chambers that passed mapping in winter and failed the same mapping three months later because the ambient temperature shift pushed the warmest point out of spec.
Common Mistakes That Break Your Study
The most frequent error is placing sensors on product. Do not do that unless your protocol explicitly requires it. Placing a sensor inside a box of product measures the product temperature, not the ambient chamber temperature. Those are two different things. Ambient temperature mapping characterizes the storage environment. Product temperature mapping is a separate exercise that is usually harder to do correctly because product thermal mass slows down temperature changes and creates additional variables. Another mistake is ignoring humidity mapping when it is relevant. For stability chambers, humidity distribution matters because ICH requires 60 percent plus or minus 5 percent. Most people forget to map humidity or assume that if temperature maps well, humidity does too. That assumption is wrong. Humidity distribution is often worse than temperature distribution because water vapor moves differently than heat. I have seen chambers where the temperature was within 0.3 degrees everywhere but the humidity varied by 15 percent between shelves.

Documentation and Data Analysis
Your mapping report needs to include the calibration certificates for every sensor used, the sensor placement diagram, the raw temperature data, the calculated statistics for each location, and the conclusions about which locations are suitable for storage. The statistical treatment matters. You should report the minimum and maximum temperatures observed at each point, the mean temperature, and the percentage of time each point spent outside the acceptable range. Some teams also calculate the hot and cold spots by taking the envelope of all sensor readings. That means at any given moment, you look at what every sensor reported and draw the upper and lower bounds across all of them. That envelope gives you a conservative picture of the chamber performance. It is not required by every guideline, but it is useful for risk assessment.
Frequency and Revalidation
Mapping should be done when the chamber is new, after any major maintenance that could affect air flow, and at least annually. Some organizations also map after any change to the product load pattern, like switching from cartons to bulk bins. The rationale is that product arrangement changes air flow paths and those changes can create new hot and cold spots. I recommend keeping a log of every mapping study and reviewing the historical trend. If the warmest point has been moving gradually higher over the past three years, that is a sign the chamber is degrading. The compressor or the fan motor may be wearing out. Catching that trend early saves you from a surprise failure during an inspection.
Software and Tools
There are several software packages designed for mapping analysis, including TSYSmap, TempMap, and the mapping modules from companies like Eltek and Sato. These tools automate the statistical calculations and generate the reports. They are worth the cost if you do mapping regularly. If you only do it once a year, a spreadsheet is sufficient as long as you validate it. For the actual data logging hardware, I recommend devices with at least 0.1 degree resolution and a sampling interval of one minute or less during the study. Slower sampling rates can miss transient events like the defrost spikes I mentioned earlier. A ten minute sampling interval would likely smooth over those spikes and give you a false sense of stability.
What Mapping Cannot Tell You
Temperature mapping does not tell you whether your alarm system will catch a failure quickly enough to protect the product. It does not tell you whether your backup systems will kick in during a power outage. It does not tell you whether the product itself is stable at the measured temperatures, which is a separate question answered by stability studies. Mapping characterizes the environment. It does not characterize the product response to that environment. If your chamber alarm threshold is set too wide, mapping might show that the environment is fine, but a power failure could still compromise product before anyone notices. That is why mapping should be part of a broader qualification strategy, not a replacement for it. You also need to qualify the alarm system separately and test it regularly.
Bottom Line on the Practical Side
Do the mapping with the chamber loaded. Use calibrated sensors with adequate resolution. Run it long enough to capture defrost cycles. Document everything. Check humidity if it matters for your product. Review the results over time. The process is straightforward when you do it right, and it is frustratingly easy to do it wrong in ways that only show up later.


