Working With The Structure Of Metals And Alloys
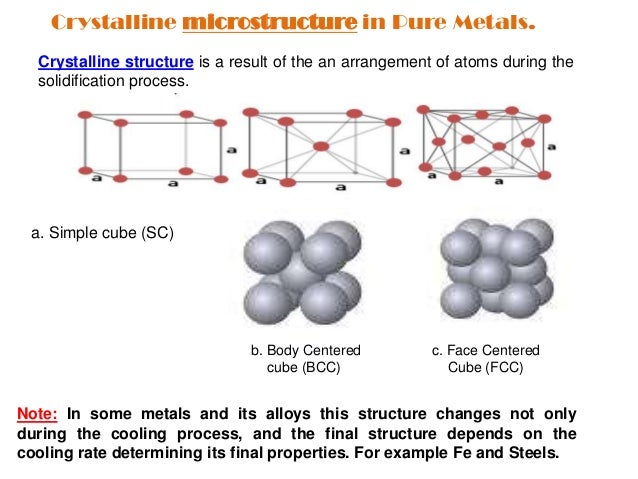
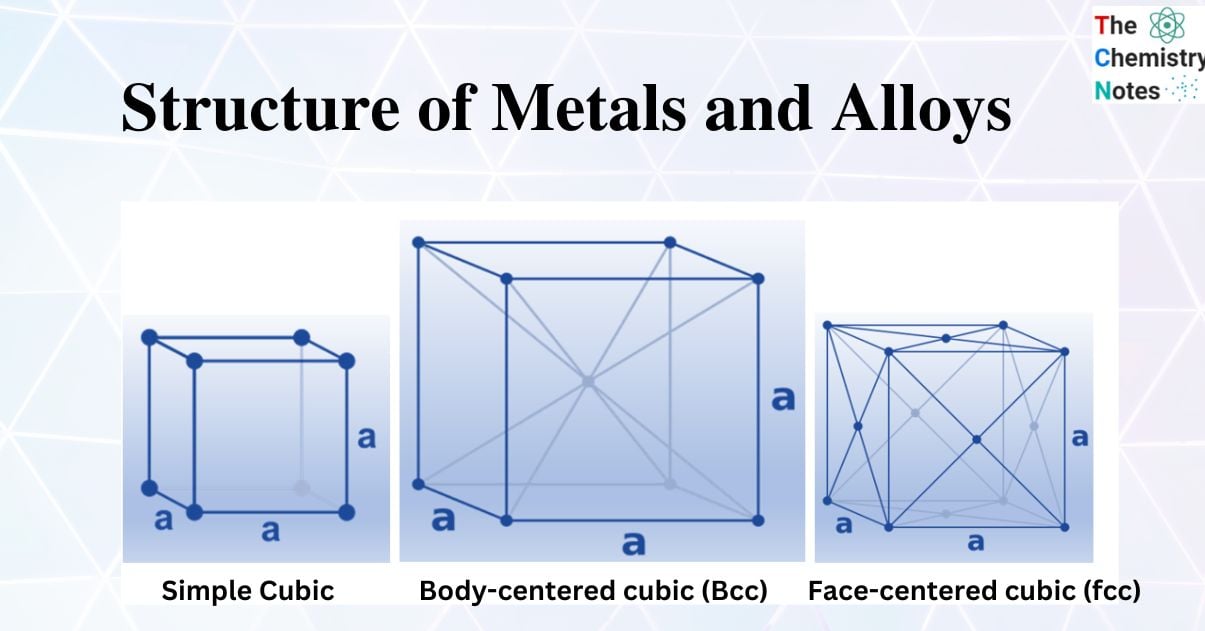
You can't really understand what's happening in a metal until you look at how its atoms are arranged. I've spent years watching engineers fail the same way over and over because they treat every alloy like it behaves the same way. It doesn't. A material that works fine at room temperature can become completely useless at 300 degrees Celsius, and it has nothing to do with the alloy being "weak" — it's entirely about what's happening at the grain level. The basic framework starts with three things: crystal structure, grain boundaries, and phase composition. Most structural metals adopt one of three lattice arrangements — face-centered cubic, body-centered cubic, or hexagonal close-packed. The difference between them matters more than people realize. FCC metals like aluminum and austenitic stainless steel tend to be more ductile because there are more slip systems available for dislocation movement. BCC metals like ferritic steel are stronger but less forgiving when you push them into plastic deformation. HCP materials like titanium and magnesium have far fewer active slip systems, which is why they're tricky to form at room temperature without cracking.
Understanding The Structure Of Metals And Alloys In Practice
Here's where it gets real. I was working on a project a few years back involving welded 316L stainless steel tubing for a low-temperature application. The specs called for maintaining toughness below minus 50 Celsius, and everything looked fine on paper — the chemistry was correct, the weld procedure was qualified, the filler metal matched the base material. We ran the impact tests and the welded joints failed consistently, sometimes at barely 10 joules when the spec required 40. The base metal was fine. Only the weld zone was compromised. Turns out the issue was sensitization. During welding, the heat-affected zone lingered in the 800-to-400 degree range long enough for chromium carbides to precipitate along the grain boundaries. That's the classic 316L problem, except I should have caught it earlier because I specifically chose the L-grade material for that exact reason. The real problem was our thermal input was too high. We were running roughly 2.5 kilojoules per millimeter on a double-groove weld, which is significantly above the recommended maximum of 1.5 kilojoules per millimeter for preventing sensitization in that thickness range. My workaround was switching to a narrow-groove joint design that cut the total weld volume in half and dropped the thermal input to about 0.9 kilojoules per millimeter. Second run, the impact values came back above 60 joules across the board. It's not glamorous, but that's basically how this work goes — you find the parameter that's drifting outside tolerance and you correct it. Grain structure is not something you can verify just by looking at a spec sheet. It depends heavily on the thermomechanical history — how the material was cast, hot-rolled, cold-worked, and heat-treated. Two bars of the same grade of 4140 steel can have dramatically different mechanical properties if one was air-cooled from the forging die and the other was quenched and tempered. The chemistry is identical. The grain size and carbide distribution are completely different.
One thing beginners miss is that grain refinement isn't always the answer people think it is. Fine grains generally improve both strength and toughness simultaneously through the Hall-Petch relationship, but there are limits. Below about 5 micrometers in many steels, you start seeing embrittlement issues during certain heat treatments because the grain boundary area becomes so large that impurity segregation reaches critical levels. I've seen this in vacuum arc remelted superalloys where the ultrafine grain structure looked great under the microscope but the fatigue life was terrible because of excessive grain boundary cavitation at service temperature. Coarser grains in those cases actually performed better at elevated temperature because there was less boundary area for damage to initiate. Phase diagrams are useful but they're equilibrium diagrams, and real manufacturing rarely achieves equilibrium. When you see a microstructure showing pearlite and ferrite in a plain carbon steel, that's close to equilibrium. When you quench the same steel and get martensite, you're looking at a diffusionless transformation that the phase diagram doesn't predict directly. You need the continuous transformation diagram for that. People who skip the CCT diagram and only consult the iron-carbon diagram will make mistakes about hardenability, especially in anything beyond the simplest geometries.
Heat Treatment And Microstructural Control
Get the Full Details

Austenitizing temperature is where most people make careless decisions. Going too hot produces excessive grain growth, and going too low means incomplete transformation. For most medium-carbon steels, the rule of thumb is 30 to 50 degrees above the upper critical temperature, but that's a starting point, not a prescription. The actual temperature needs to account for section thickness, alloy content, and what you're trying to achieve. If you're normalizing a thick forging, you might need the higher end of that range to ensure the core fully transforms. If you're doing a thin gear blank, the lower end prevents grain coarsening. Quenching medium requires as much attention as the austenitizing step. Oil quenching gives you a moderate cooling rate that reduces distortion risk compared to water, but it won't harden through-section on anything substantial in plain carbon steels. For through-hardening in larger sections, you need alloy steels like 4340 or 8620 where the added elements shift the nose of the CCT diagram to longer times, allowing martensite formation even at slower cooling rates. I've had cases where someone specified 1045 for a shaft that needed 55 RC hardness throughout a two-inch diameter, and it simply wasn't going to happen. The center would never achieve martensite no matter how aggressive the quench was. Switching to 4140 solved the problem without any geometry changes. Tempering is where the final properties are actually set, and it's the most overlooked step. As-quenched martensite is extremely hard but also very brittle, with high residual stresses locked in. Tempering at 200 degrees Celsius for two hours will relieve some stress and slightly reduce hardness while improving toughness marginally. Tempering at 600 degrees Celsius will give you a fully tempered sorbitte structure with significantly lower hardness but much better impact resistance. The trade-off is always there. There's no free lunch in heat treatment.
Alloying Additions And What They Actually Do
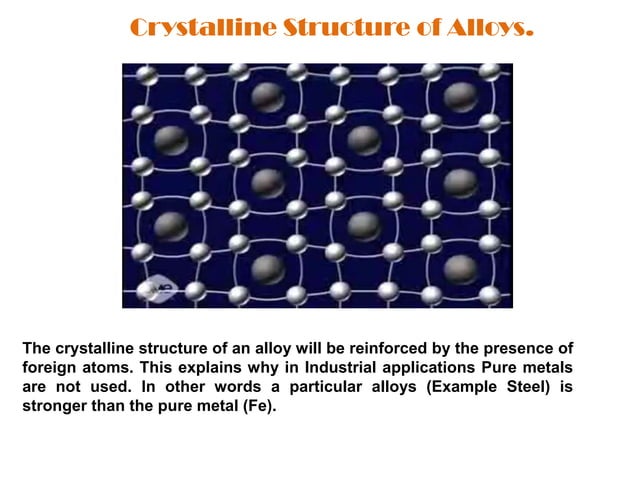
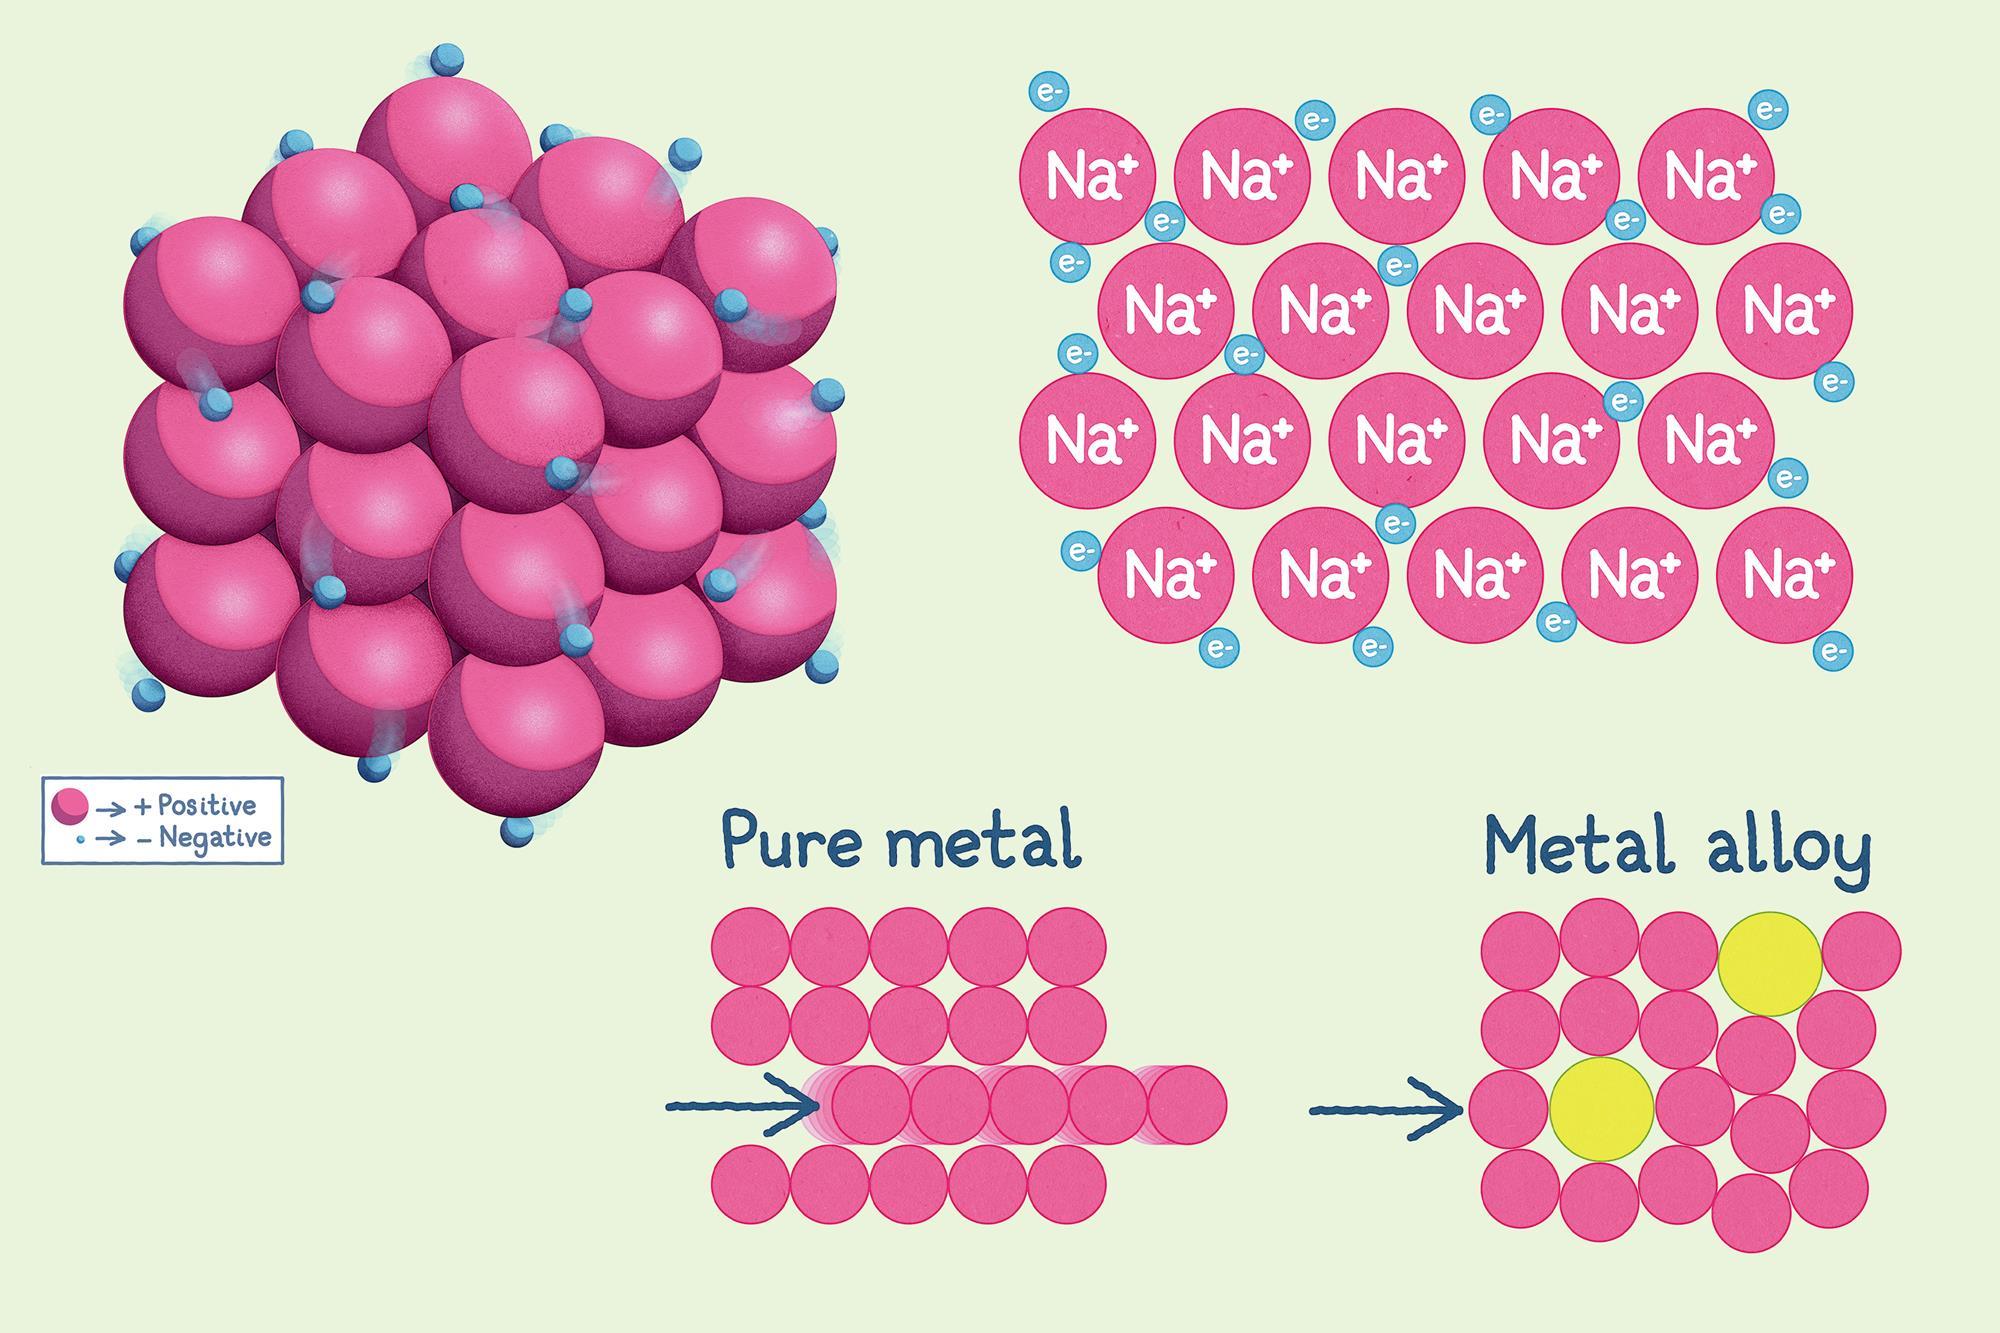
Carbon is the primary hardening element in steels, but it's not the only one that matters. Chromium improves corrosion resistance and forms carbides that enhance wear resistance. Nickel increases toughness, especially at low temperatures, and stabilizes the austenite phase. Molybdenum retards temper softening and improves high-temperature strength. Vanadium refines grain size and forms fine carbides that inhibit grain growth during heat treatment. Each addition has a specific role, and combining them creates synergistic effects that single-element additions can't achieve. Aluminum and titanium are often added as grain refiners in casting. They form nitrides and aluminides that act as nucleation sites during solidification. This is why cast aluminum alloys with small additions of titanium and boron have much finer grains than the same alloy without those additions. The grain refinement can improve tensile strength by 10 to 15 percent and significantly improve elongation. It's a cheap modification that makes a measurable difference, and it's one of those things that gets skipped when cost-cutting happens on a foundry run.With titanium alloys, the alpha and beta phase stability is controlled by different alloying elements. Aluminum is an alpha stabilizer that increases strength and raises the alpha-to-beta transition temperature. Vanadium and molybdenum are beta stabilizers that lower the transition temperature and increase hardenability. Ti-6Al-4V, which is roughly 90 percent of all titanium alloy usage, sits at that where you get a duplex microstructure after typical solution treating and aging. That balance is why it's the default choice — good strength, reasonable toughness, and it responds well to heat treatment. If you need higher strength, you go to something like Ti-10V-2Fe-3Al. If you need better creep resistance at temperature, you move toward alpha alloys like Ti-6242. But those come with their own processing challenges.
Characterization And Quality Control
Optical microscopy is the bread and butter of metallography. You mount, grind, polish, and etch a sample, then look at it. Etchants tell different stories depending on what they reveal. Nital etches steel microstructures by attacking grain boundaries and different phases at different rates, making pearlite colonies, ferrite grains, and martensite laths visible. Klemms reagent does the same for copper alloys. Vilella's reagent works on aluminum. The etchant choice matters because using the wrong one will either produce no contrast or over-etch and destroy the features you're trying to see.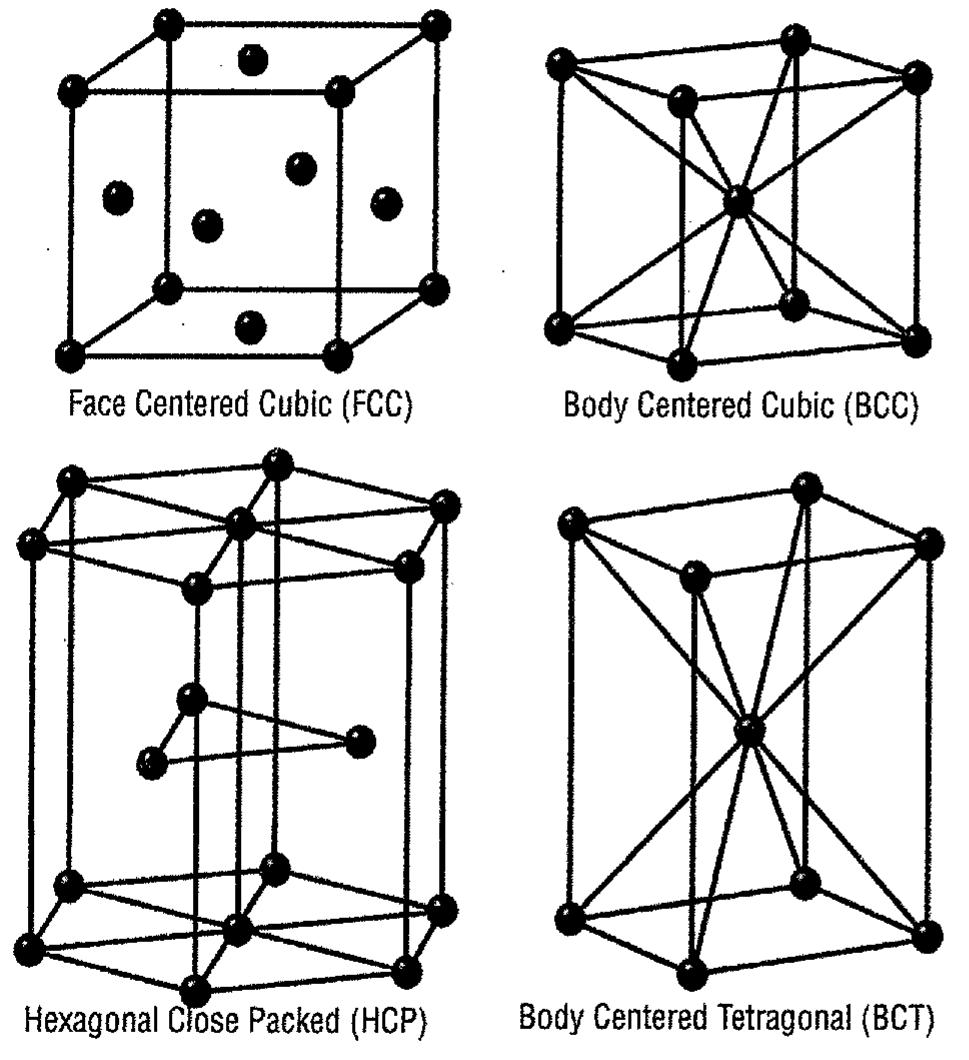
Scanning electron microscopy adds resolution and allows compositional analysis through EDS. You can see carbide morphology at a scale that optical microscopy can't resolve, and you can confirm whether a precipitate is actually what you think it is. I once spent three days trying to figure out why a precipitation-hardened stainless steel part was underperforming in hardness tests. Optical microscopy showed what looked like a normal aging microstructure. SEM with EDS revealed that the carbides weren't the fine precipitates we expected — they were coarse chromium-rich particles that had formed during an unintended exposure to the sensitization temperature range during a prior fabrication step. The part had been baked accidentally at about 450 degrees for too long. The microstructure looked fine at low magnification but was compromised at the grain boundaries. Hardenability testing through Jominy end-quench tests is still the standard way to verify that a steel batch will respond correctly to quenching. The distance from the quenched end where a specific hardness is achieved tells you directly how deep you can harden a part of a given diameter. It's a quick test — about 30 minutes from start to finish — and it catches batch variations that chemistry alone won't reveal. Two heats of the same steel grade can have the same nominal composition but different hardenability if the trace elements like boron or manganese vary slightly. The Jominy test catches that before you put it into production.
Common Pitfalls To Avoid
Assuming that hardness equals overall performance is probably the most damaging misconception. A piece of tool steel at 65 RC will be extremely hard but may fracture under impact loading that a piece at 50 RC would absorb without damage. Hardness is just one property. Tensile strength, yield strength, elongation, reduction of area, impact toughness, fatigue strength, and creep resistance are all separate measurements that don't always correlate with each other. Another mistake is ignoring the effect of cold work on subsequent heat treatment responses. Cold-rolled or shot-peened surfaces have residual compressive stresses that improve fatigue life, but those stresses can be relieved during stress-relief annealing if you're not careful about temperature selection. I've seen components where a successful shot-peening operation was followed by a stress-relief bake that removed all the beneficial compressive layer, leaving nothing but the original tensile residual stresses from machining. The fix was switching to a lower-temperature stress relief at 300 degrees instead of the usual 550, which preserved the peened surface layer while still relieving bulk machining stresses. Not accounting for thermal cycling during service is another area where people get burned. Components that experience repeated heating and cooling — exhaust manifolds, turbine blades, forging dies — undergo cyclic thermal stresses that can cause fatigue cracking independent of mechanical loading. The material's thermal expansion coefficient, thermal conductivity, and temperature-dependent mechanical properties all play roles here. A material that performs well in a static test may fail quickly under thermal cycling because the expansion mismatch between phases or between different sections creates localized stress concentrations that propagate cracks over time.
Hydrogen embrittlement is worth mentioning specifically because it's insidious. High-strength steels above roughly 1000 MPa tensile strength are susceptible, and hydrogen can enter the material during electroplating, pickling, or even from corrosion reactions during service. The damage doesn't show up immediately. Parts can sit in inventory for weeks before failing. The classic sign is delayed fracture under static load, often with a brittle fracture appearance despite the material normally being ductile. Stress relieving at 200 degrees for several hours after plating can diffuse the hydrogen out, but the part needs to be treated within a few hours of the hydrogen-exposing process, or the window closes. The Structure Of Metals And Alloys is something you work with directly, not just read about. Every heat, every weld pass, every quench bath changes the microstructure in ways that affect what the final part can actually do. The theory gives you a framework for understanding, but the details come from experience and from paying attention to what the material is telling you when you look closely enough.