What the NCCER Welding Test Actually Looks Like
The NCCER Level 1 welding credential splits into a written section and a hands-on performance portion. The written part covers weld symbols, joint classifications, safety requirements, and equipment recognition. The performance portion typically includes groove welds in plate across several positions, plus a pipe weld. That 6G pipe test is where most people get stuck. It's a fixed-position test on a 2-inch schedule 40 pipe set at a 45-degree angle, and you're not allowed to rotate the work. I've walked people through this test enough times to know exactly where the failures cluster. The written exam is pass/fail at roughly a 70 percent threshold depending on your module completion status, but the performance side is what separates the candidates who've actually practiced from the ones who've only watched videos. Undercut limits are usually capped around 1/32 inch on most NCCER evaluations. Porosity is strictly limited, and the bend test that follows your weld will reject any significant lack of fusion or incomplete penetration. These are objective measurements, not opinions.
Study Guide For Nccer Weld Test
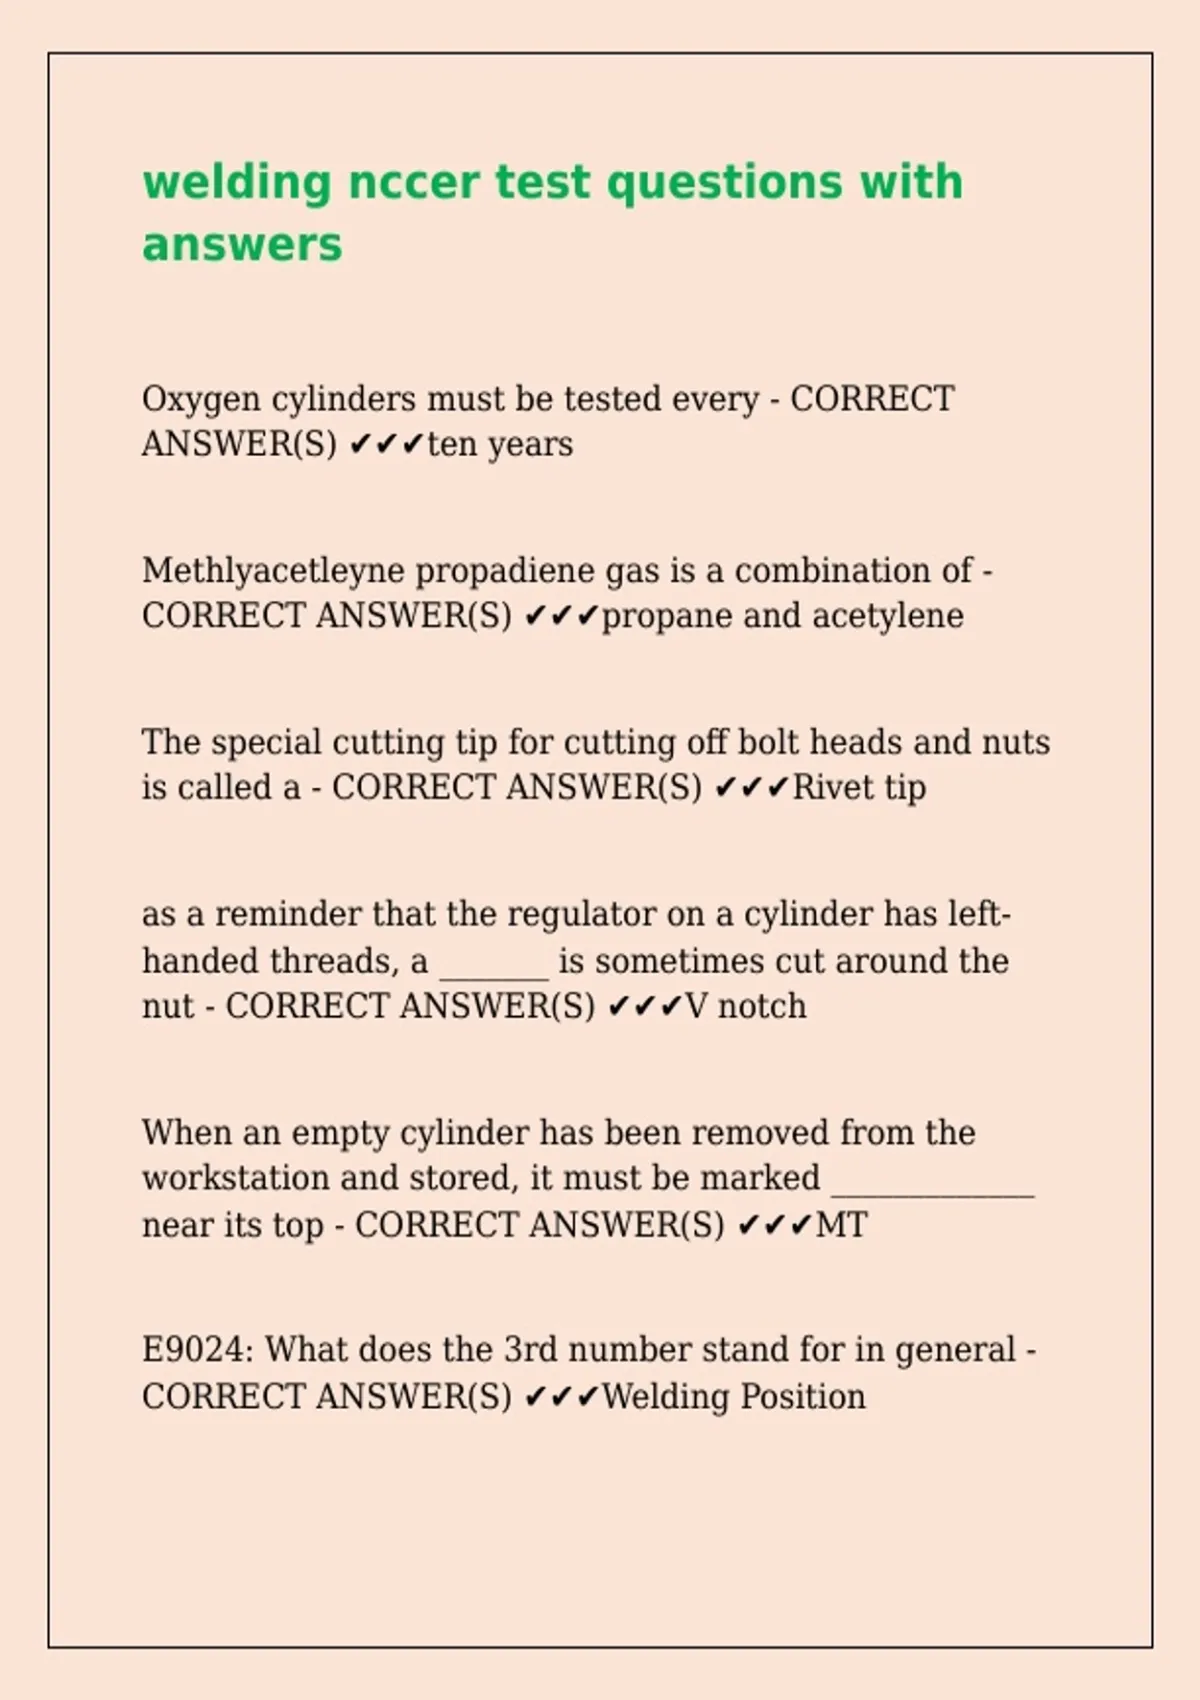
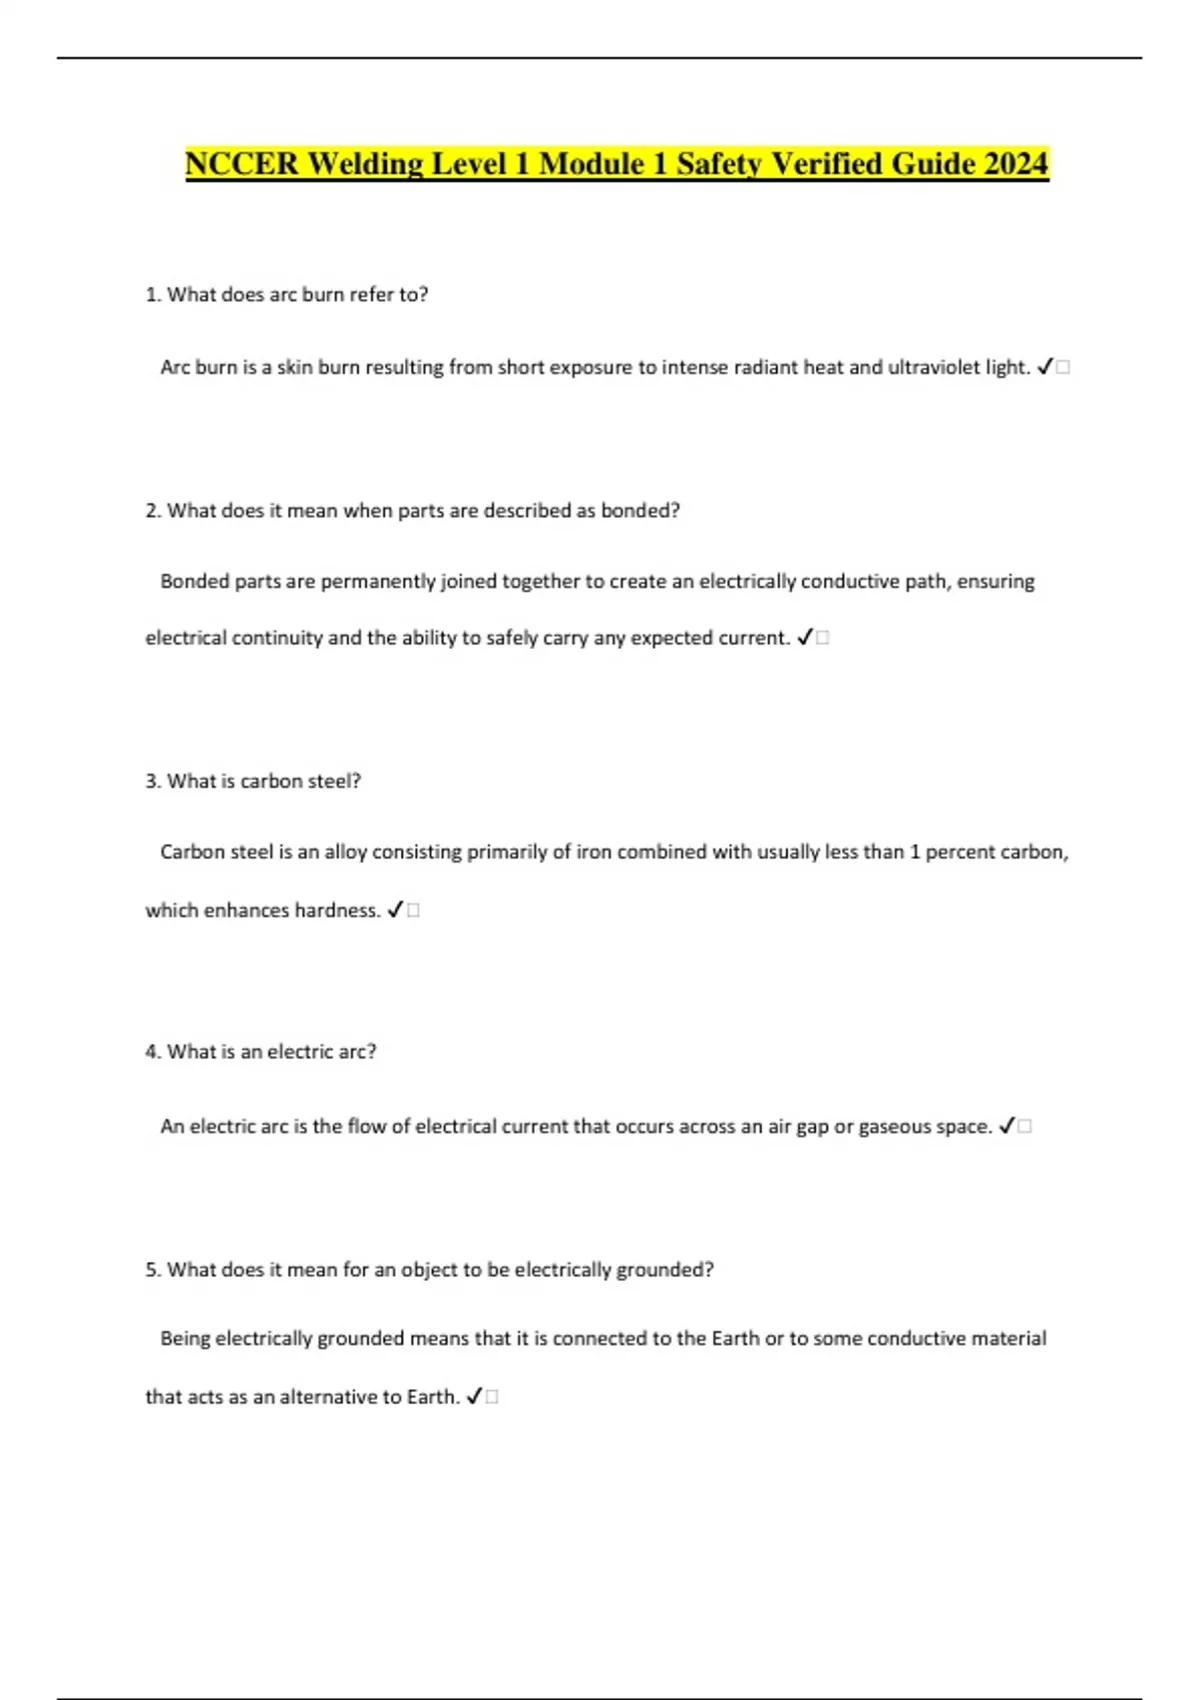
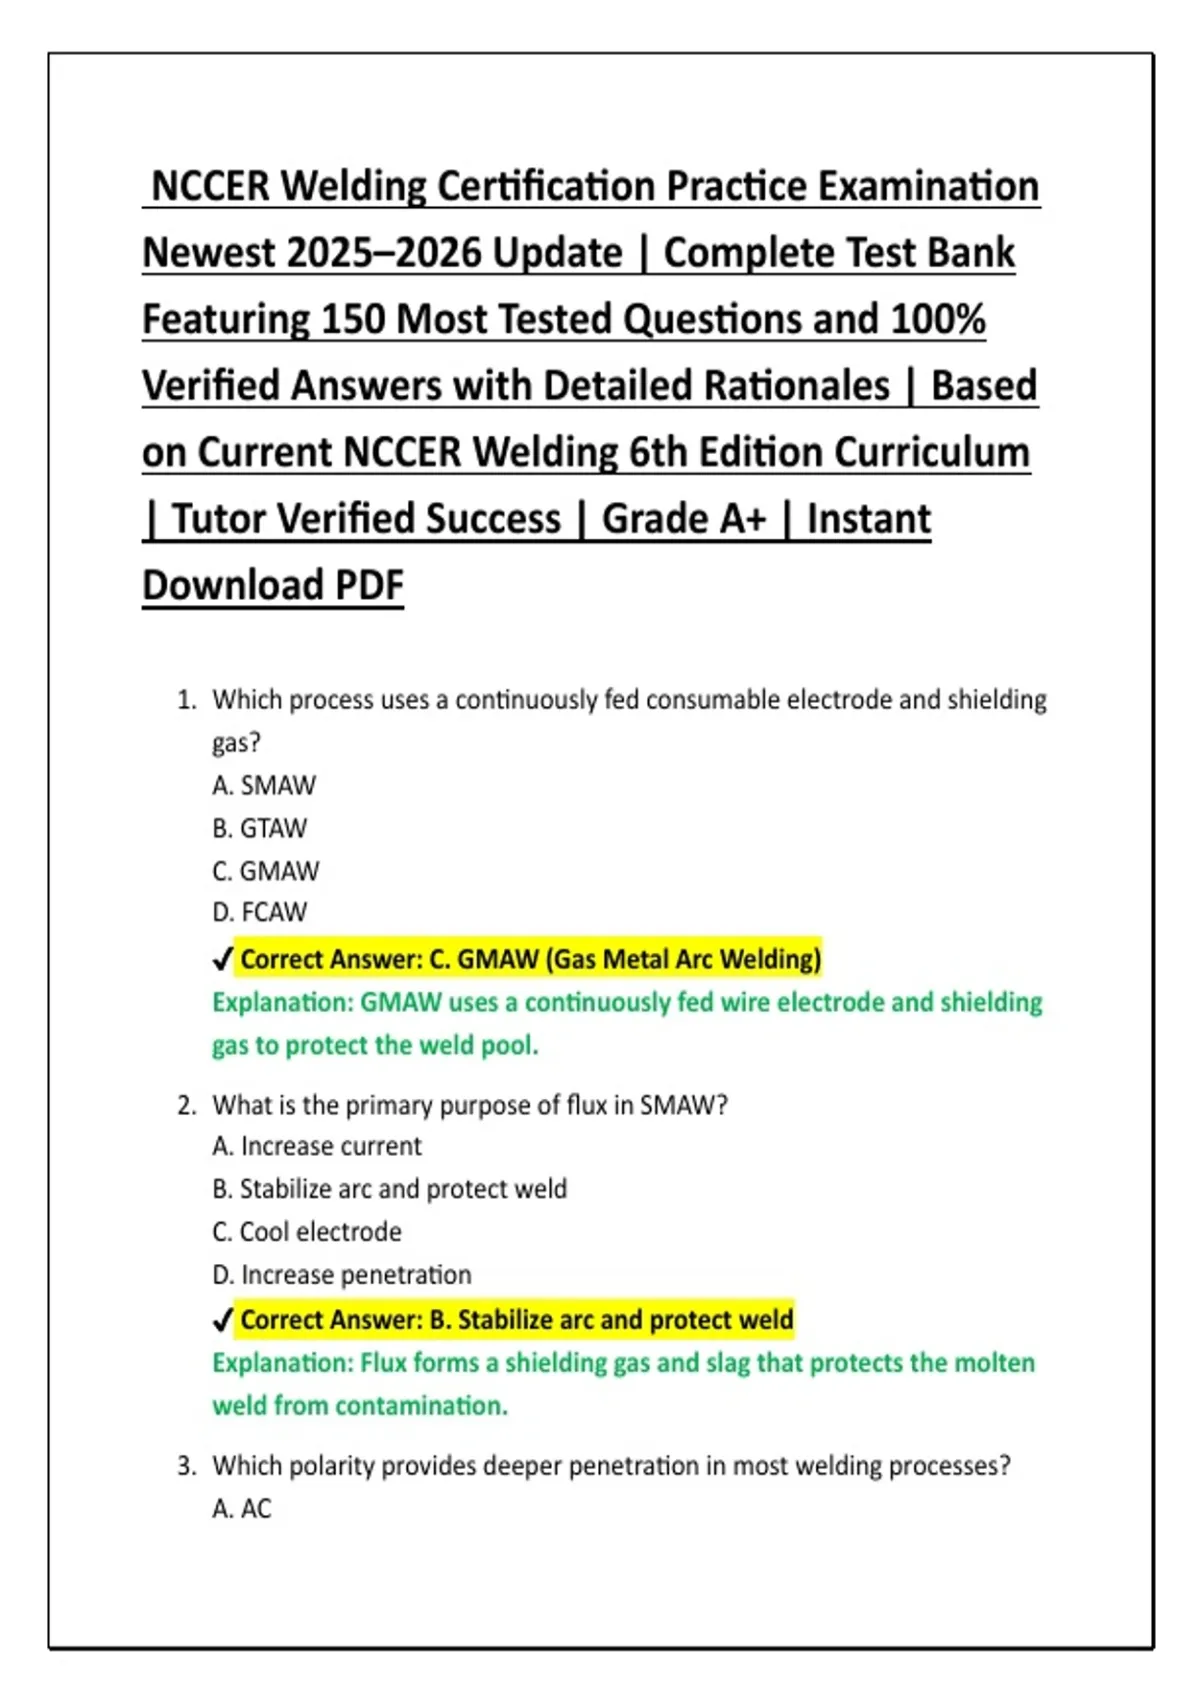
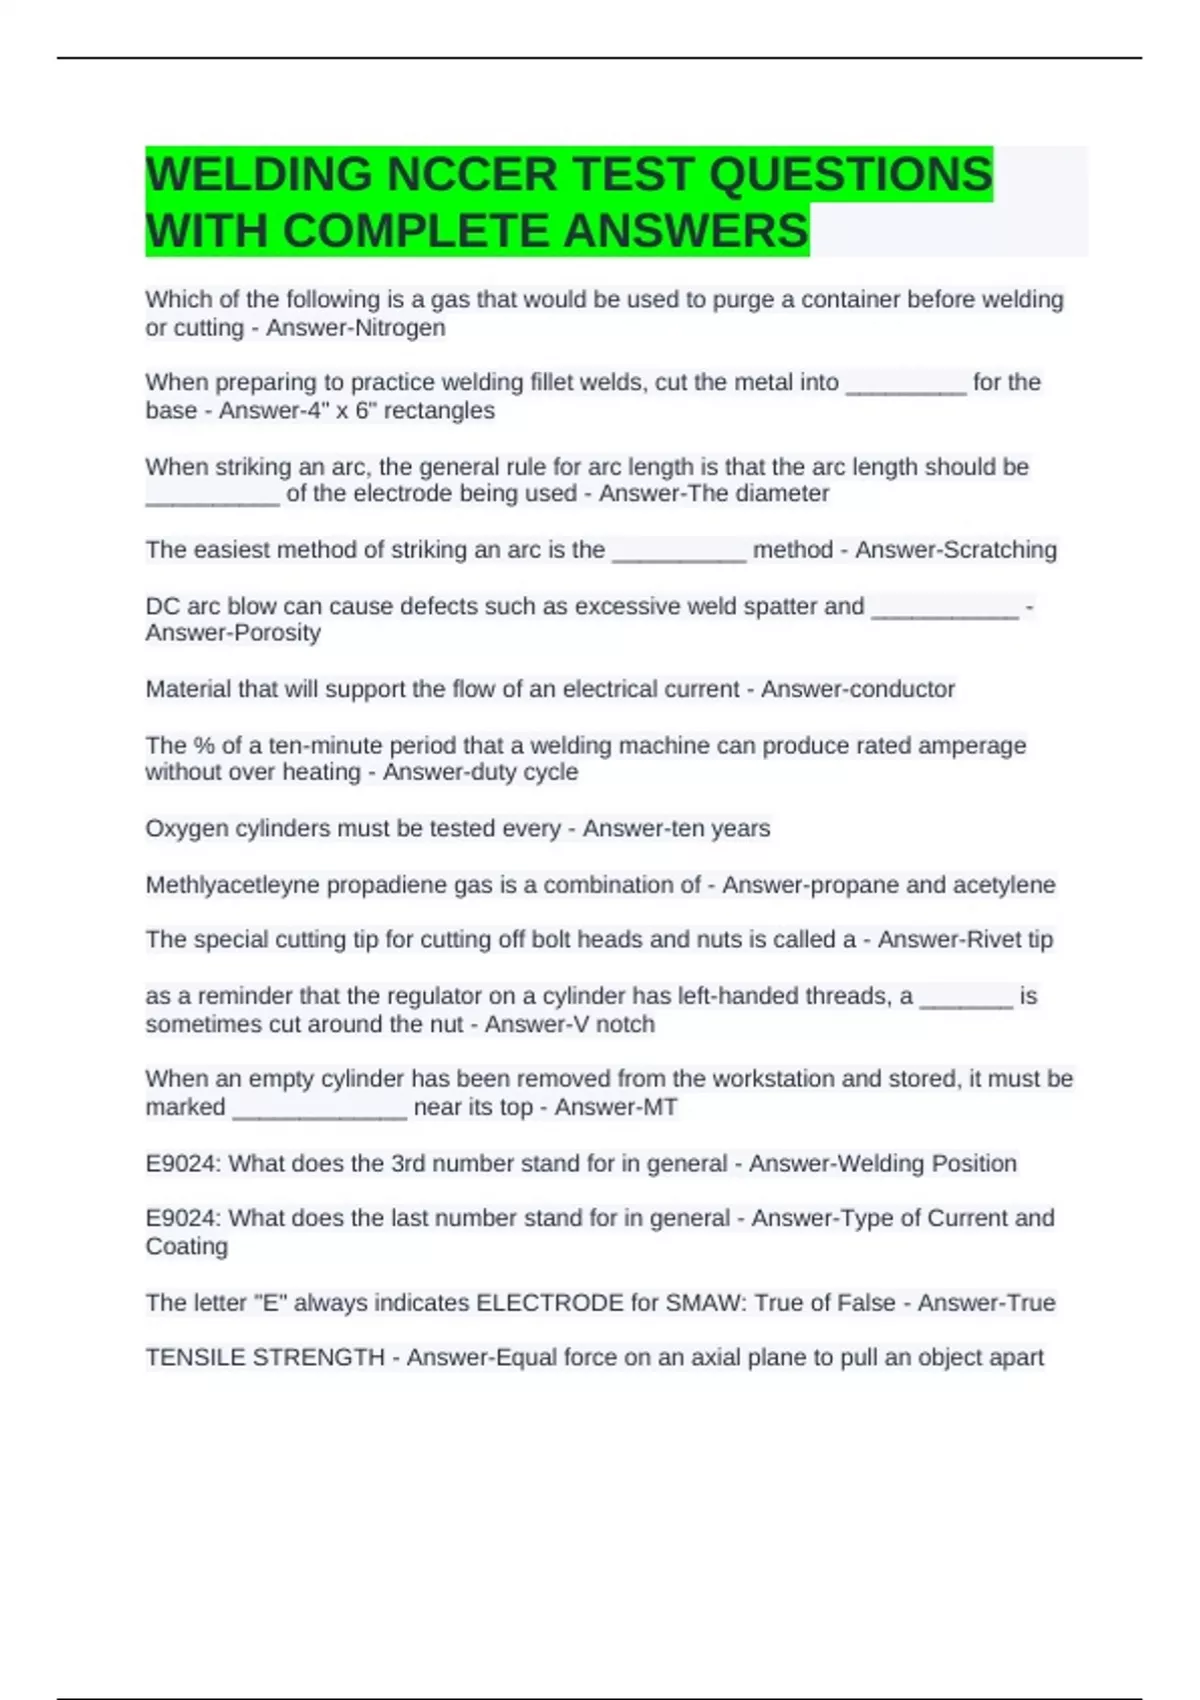
Most candidates look for a study guide early in the process and end up downloading whatever PDF shows up on the first page of results. A lot of those guides are outdated or written by people who've never actually proctored an NCCER evaluation. The materials that align with the current NCCER curriculum tend to cover the right weld symbol combinations, proper PPE identification, and the specific joint types they test on—the V-groove in single and double configurations, the J-groove, and the bevel-groove welds in plate and pipe. I ran into a real problem a couple years back with a candidate who'd memorized a study guide that listed SMAW as the primary process throughout. The program had shifted heavily toward GMAW by that point, and he showed up confused about wire feed settings, shielding gas composition, and contact tip maintenance because his reference material was two or three curriculum revisions behind. He eventually passed after spending a week drilling the actual process specifications his instructor was using, but that was wasted time he couldn't afford. The most reliable study material comes directly from the NCCER curriculum itself if you're enrolled in a recognized program. They publish module-specific review questions and sample performance tasks. If you're self-studying outside a formal program, you'll need to cross-reference the welding symbol standards from the American Welding Society's A2.4 documentation and make sure your study guide covers the 2015 or later revision. Older editions omit several symbol variations that appear on current tests.
How to Actually Prepare Without Wasting Time
Start with the written material because that part is straightforward if you've been attending class. Review weld symbols until you can draw them from memory without looking at a reference. The NCCER test expects you to identify everything from groove weld symbols to back welds and flush weld requirements. Joint type identification comes next—butt joints, tee joints, lap joints, and edge joints, along with the bevel angles and root openings specified for each configuration. For the performance side, the single biggest factor in passing is consistent practice on the actual positions you'll be tested on. A lot of beginners spend weeks welding in the flat position because it's comfortable, then show up unprepared for horizontal and vertical up. The 6G pipe position alone accounts for a significant number of failures. You need to practice root passes on pipe without rotation until you can maintain a consistent gap and penetration depth without burning through. Once the root is solid, the fill and cap passes mostly come down to travel speed control and electrode angle management. I remember one candidate who kept failing his practice coupons on the vertical up position because he was holding his stick angle too perpendicular to the workpiece. He'd get good-looking beads on top but the root side showed incomplete fusion when bent. Flipping his technique to a climbing vertical stance with about a 5 to 10 degree work angle relative to the vertical plane fixed it almost immediately. He hadn't failed because he couldn't weld—he'd been welding at the wrong angle the whole time.
Get the Full Details
What the Evaluators Actually Look For
The NCCER performance evaluation uses specific acceptance criteria, and understanding those criteria matters more than having the prettiest weld. Excessive reinforcement is a common rejection point. If your weld bead sits more than a certain height above the base metal surface, it fails regardless of how clean the rest of the weld looks. For most Level 1 plate groove welds, reinforcement shouldn't exceed roughly 3/32 inch on each side. Undercut is another frequent failure reason. Even shallow undercut along the toe of the weld can bring a coupon down if it runs the length of the bead. The bend test is where surface appearance stops mattering entirely. You're bending the weld through a specified face and root bend test, and the evaluator is checking the bent specimen for open defects. Cracks wider than 1/16 inch, lack of fusion longer than the allowed tolerance, or incomplete penetration will all result in a failure. A weld that looks perfect from the outside can still fail this test if the root didn't properly fuse during the first pass. This is why practicing proper root technique matters more than polishing your cap pass. Some candidates also underestimate the time pressure. The performance evaluation isn't just about producing an acceptable weld—it's about producing it within a reasonable timeframe. Racing through a weld to beat the clock while sacrificing joint preparation or travel speed control is a fast track to rejection. Plan your passes, prepare your bevels cleanly, and maintain consistent parameters throughout. Rushing the root pass is the most common way people dig themselves into a hole they can't recover from.
Where This Approach Falls Short
Studying from a general guide without access to actual NCCER evaluation samples leaves a gap. You might understand the theory perfectly and still fail the performance test because the specific setup your local eval center uses doesn't match what you practiced. Different training partners sometimes run slightly different qualification setups, and the pipe diameter, wall thickness, or groove configuration can vary. The best way to close that gap is to ask your instructor exactly what configuration you'll be tested on and practice on matching material. Self-study also has a real limitation when it comes to the performance portion. You can watch enough tutorial videos to understand the concepts, but you can't develop the hand-eye coordination required for vertical up or 6G pipe welding without actually doing it. A Study Guide For Nccer Weld Test helps with the written exam and gives you a framework, but it won't substitute for hours of live practice on the positions that will actually be evaluated. If you're not enrolled in a formal NCCER program, consider reaching out to a local training provider or community college welding department to see if they offer evaluation preparation sessions. Having an experienced welder watch your technique and correct your stance, angle, and travel speed before test day is worth more than any amount of additional studying. The written portion is mostly memorization and application. The performance portion rewards practice, not reading.
Final Notes on Getting Through This
The NCCER Level 1 welding test is designed to verify basic competency, not to find reasons to fail you. The criteria are published, the expectations are clear, and the failures are almost always preventable with adequate preparation. Focus your study time on weld symbols and joint identification for the written section. Spend the bulk of your hands-on time on the positions and pipe welding scenarios you'll actually face. Verify your study materials match the current curriculum version. And don't skip practice on the 6G position if pipe work is in your evaluation plan. One thing that catches people off guard is the safety component of the written exam. They expect you to know proper ventilation requirements, fire watch procedures, cylinder handling, and PPE selection. Don't brush past that section. It's usually a smaller portion of the exam, but it's easy points if you've reviewed it and an unnecessary deduction if you haven't. A few minutes of review there can make a measurable difference in your overall score. The whole process takes most candidates somewhere between two and four weeks of focused preparation if they're attending class regularly, and closer to six to eight weeks if they're studying independently while working a separate job. Plan accordingly, practice deliberately, and make sure your study resources are current. The test itself is fair if you're properly prepared.