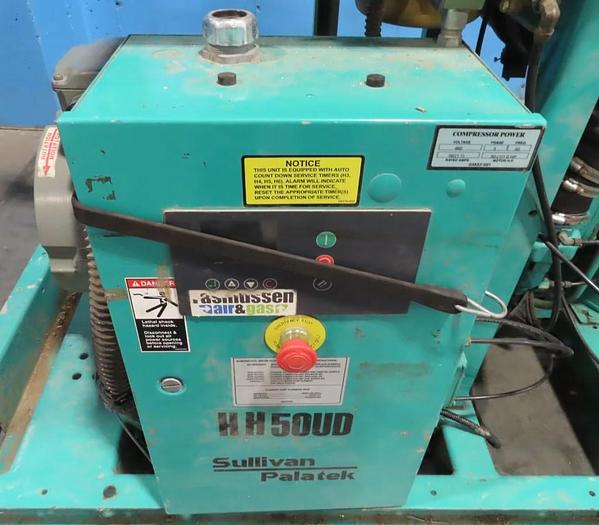
What the Sullivan Palatek 50 Ud Actually Is
The Sullivan Palatek 50 Ud is a vertical cylindrical grinder, one of several models that the company produced before they were acquired and the product lines were folded into larger organizations. The machine itself is a precision Grinder used mainly for external cylindrical grinding, plunge grinding, and profile grinding on small to medium workpieces. It uses a vertical spindle orientation, which is different from the more common horizontal spindle layout you see on older cylindrical grinders. The control system is CNC-based, and the manual covers setup, operation, maintenance, and troubleshooting for that particular variant. Getting your hands on the actual manual is not always straightforward. Sullivan Palatek went through ownership changes and many of the original paper manuals have been out of print for decades. What tends to circulate online are scanned PDFs that people pulled from old machine tool libraries or that were shared on specialty machining forums. The file I found most useful had the manual spread across roughly 200 pages, with a dedicated section for the control panel, wheel dresser adjustments, and the grinder's axis calibration procedure. If you are downloading one, check that it specifically mentions the 50 Ud and not just the 50 series in general. Some documents cover the 50 and 50-2 but leave out the variations that the Ud model introduced, especially around the vertical spindle head configuration. The control on this machine is not a modern Fanuc or Siemens system. It is a proprietary controller that was common in that era of American-made grinders. You will find parameters for wheel speed, infeed rates, spark-out time, and axis compensation. Learning to navigate the menu takes some patience, but once you understand the parameter structure, it is not difficult to work with. One thing the manual does not always make clear: certain parameter changes require the machine to be in a specific mode before they will accept the input. I learned that the hard way when I tried to change the wheel dressing feed rate and the controller kept rejecting the entry. The workaround was to put the axes in jog mode first, then enter the parameter, then switch back. Simple enough once you know it, but it is not in the manual in any obvious place.
A counter-intuitive thing about these vertical grinders is that the wheel dressers are more critical than most operators give them credit for. The manual describes the dresser setup in a few paragraphs, but in practice, the dresser condition and alignment have a much bigger impact on surface finish than people realize. I had a situation where the ground parts were coming out with a consistent taper across the face width. The obvious thing to check was the wheel balance and the tailstock alignment, but neither was the problem. The dresser diamond was worn on one side and the dressing path was not centered on the wheel face. After truing the dresser mount and centering the dressing pass, the taper disappeared. That kind of issue is exactly why having the manual nearby helps, even if it does not directly diagnose your particular problem. The maintenance section of the manual covers routine lubrication, spindle bearing inspection, and way cleaning. The lubrication intervals on the 50 Ud are conservative by modern standards. I would recommend following the manual's schedule but also keeping an eye on the central lubrication pump. Those pumps tend to clog or run dry if the reservoir is not topped off regularly, and when they do, the linear ways start to show wear faster than you want them to. There is no dramatic failure mode here, just slow degradation that adds up over months. If you are dealing with an error code on the control, the manual includes a fault list, but it is not exhaustive. Some errors only appear under specific conditions, like thermal drift or a servo fault that triggers intermittently. I once saw a code that the manual listed as a general servo alarm with no specific sub-code. The fix turned out to be a loose connection on the feedback cable for the Y-axis encoder. It is one of those things you only figure out after you have spent an afternoon tracing wiring harnesses. The manual will point you in the right direction, but it will not solve every edge case.
The down side of relying on any scanner PDF of an older manual is that the images can be unclear, and some pages may be missing or misordered. The parameter tables are usually the most important section, and they are also the ones most likely to suffer from scan quality issues. If the PDF you are looking at has blurry parameter tables, try to find an alternative copy. It matters more than you might expect when you are trying to read a setting value at 2 AM while production is stopped. For anyone who needs this information for a machine they actually own, the most practical approach is to download a copy, print the key sections you reference often, and keep them near the control panel. The manual is not something you read cover to cover. It is a reference document. The sections on wheel mounting, dresser adjustment, and axis calibration are the ones you will pull up most frequently. The troubleshooting section is useful but limited, so pairing it with a solid understanding of the machine's mechanical layout will serve you better than any single troubleshooting flowchart.
Get the Full Details