Getting Your Drill Jig Hole Patterns Right Without Losing Your Mind
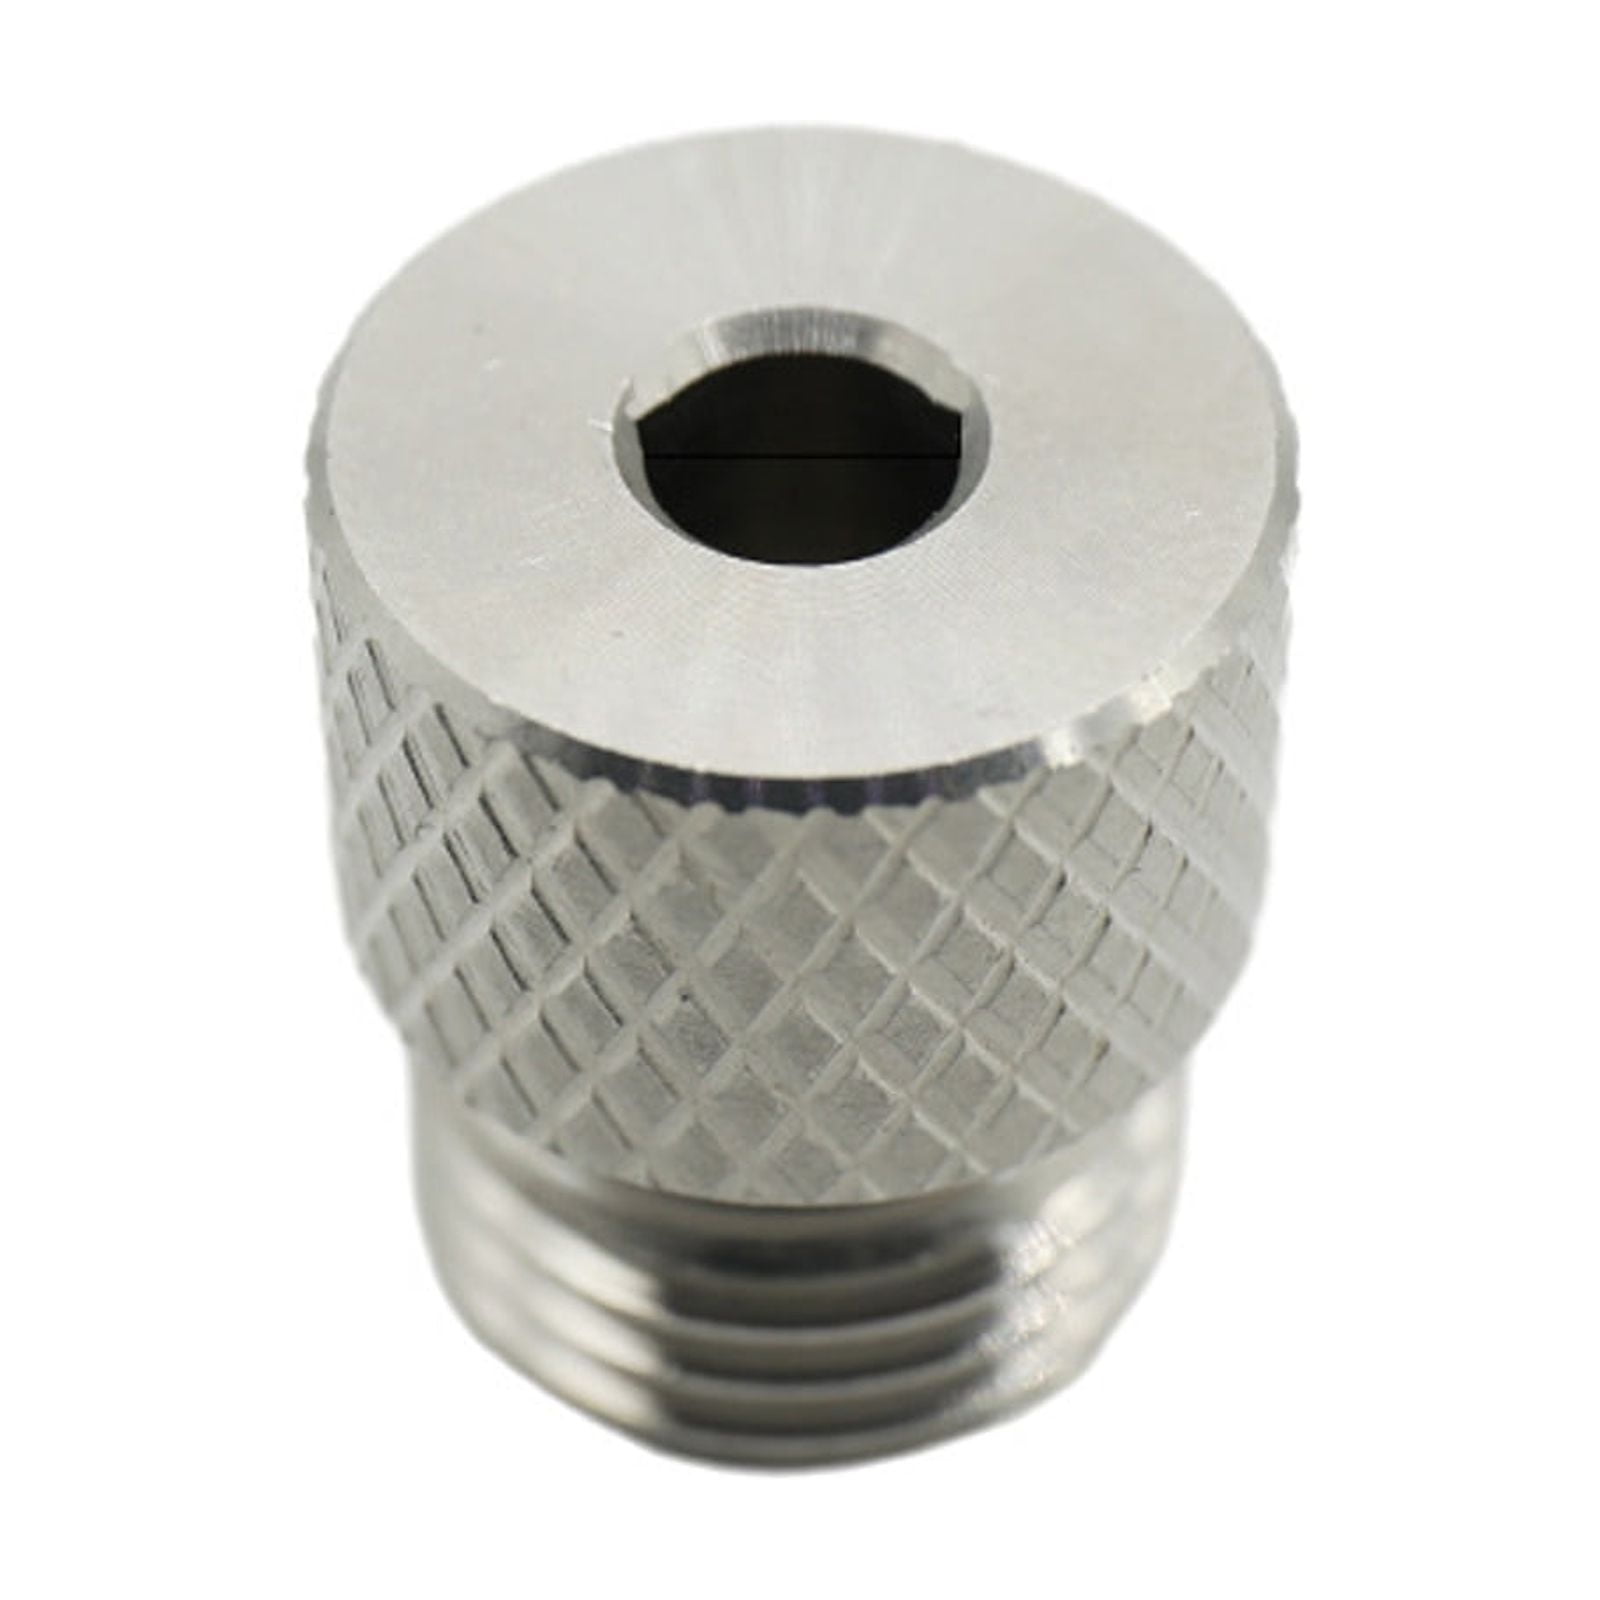
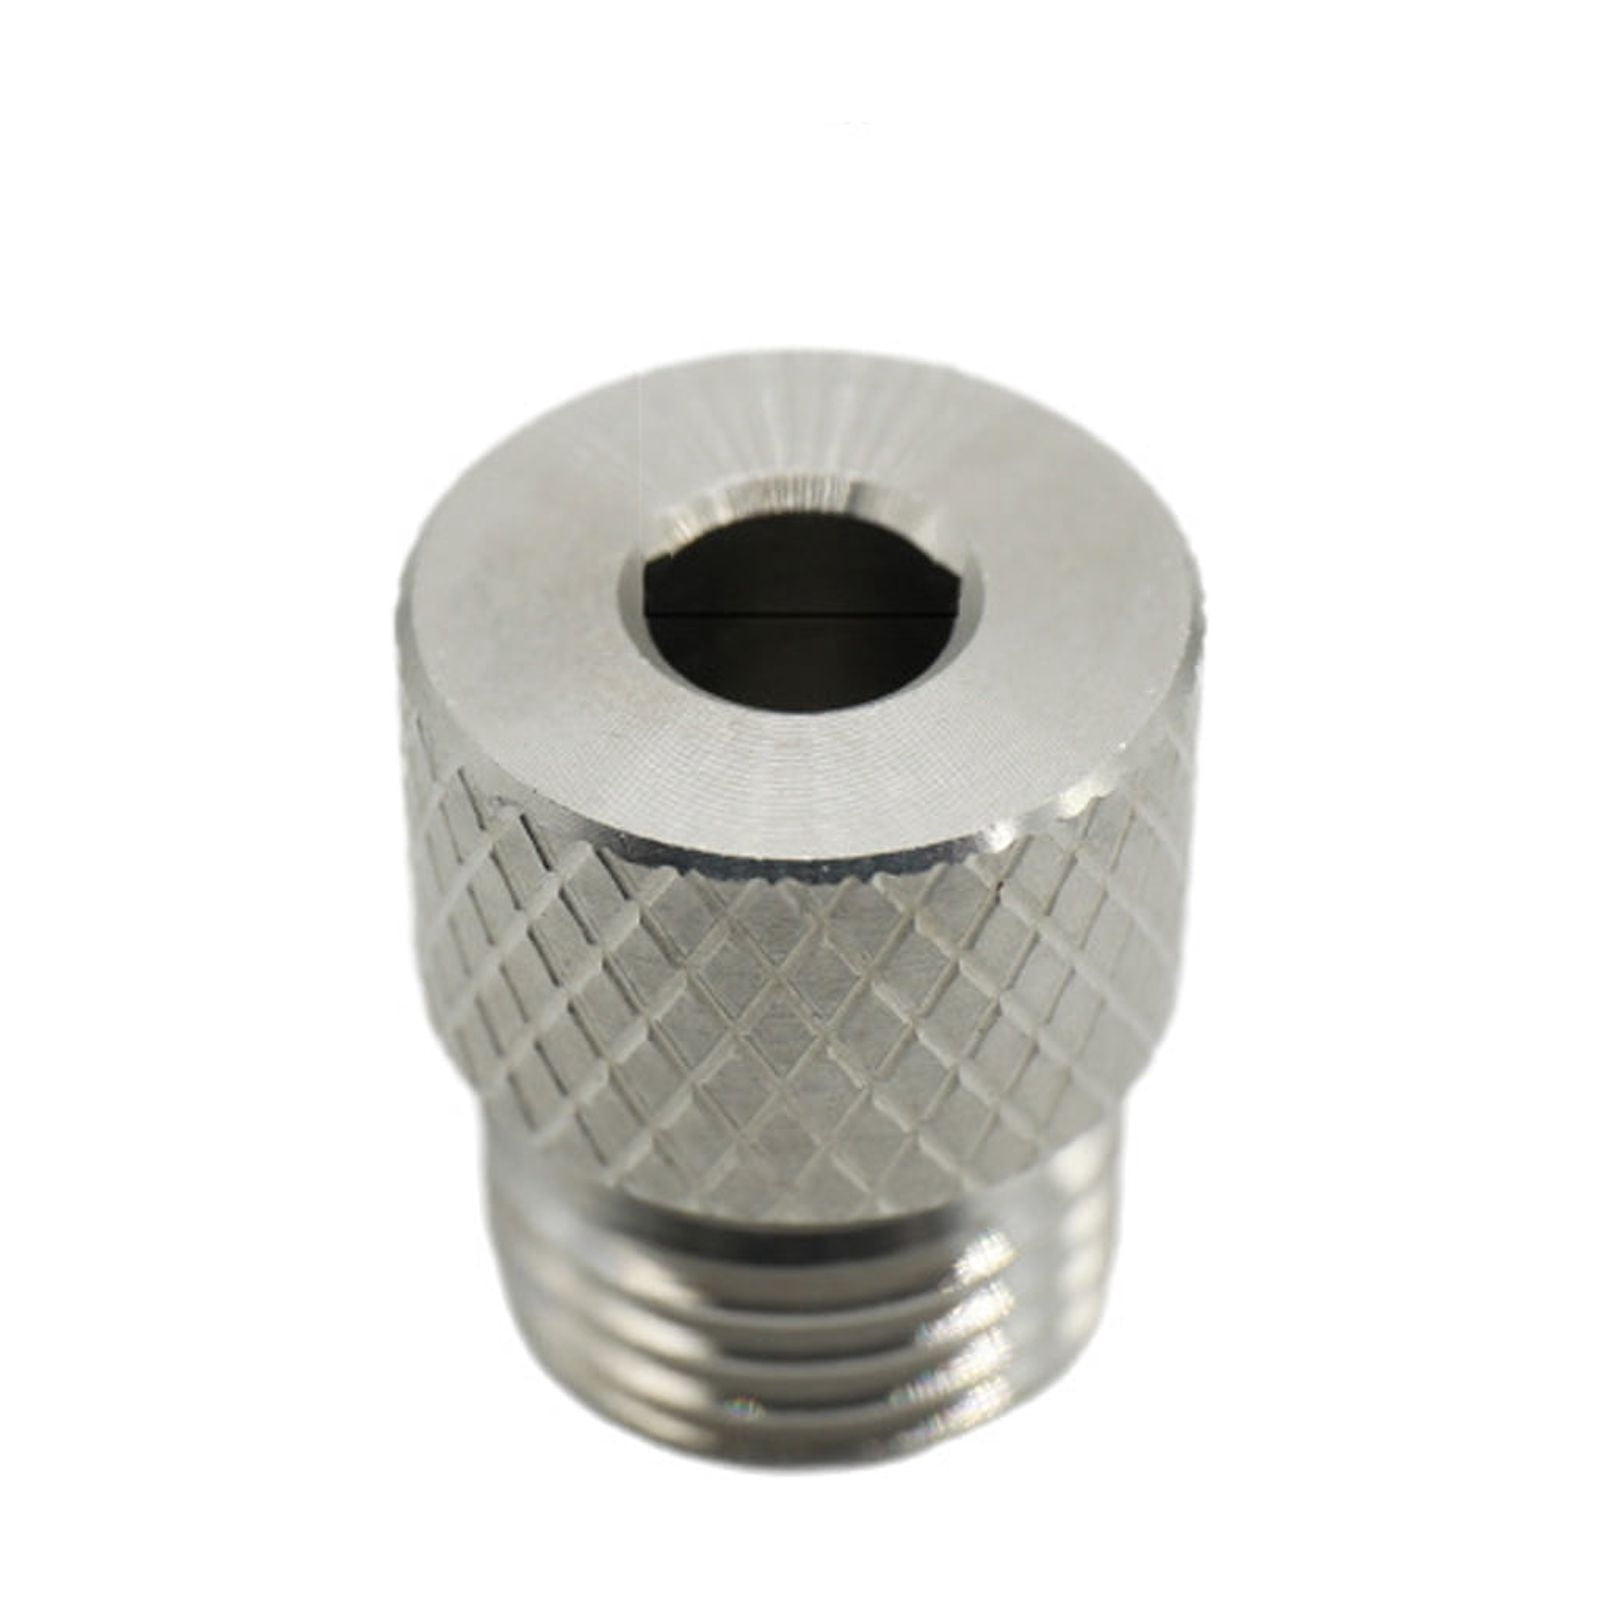
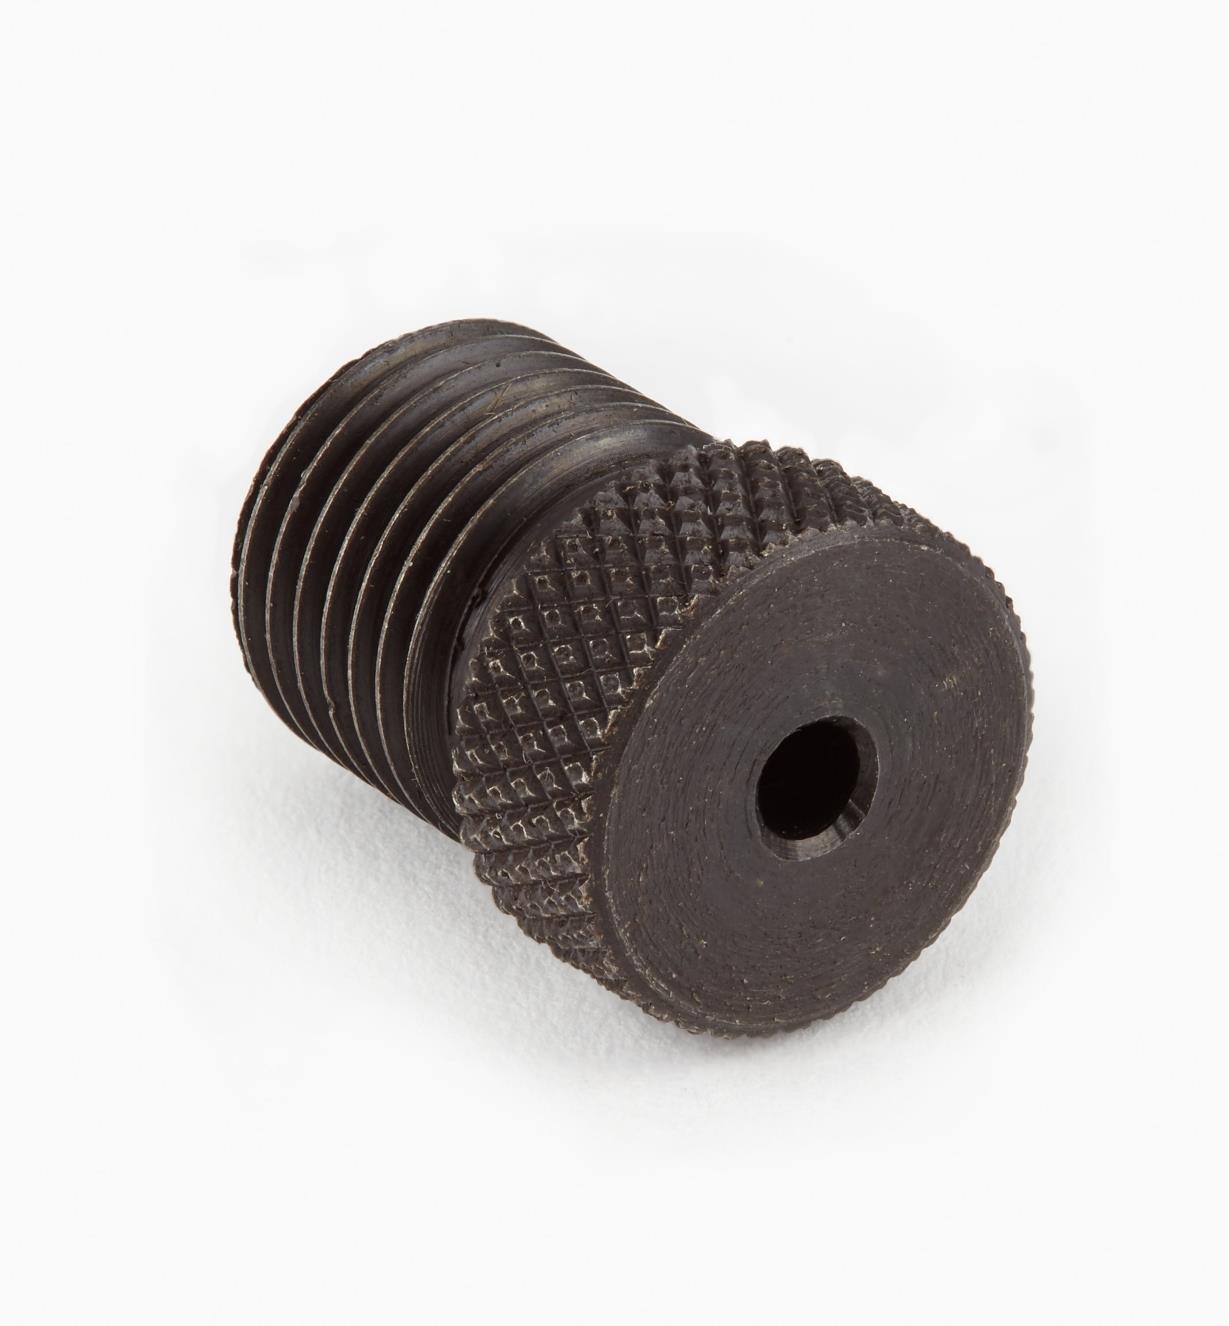
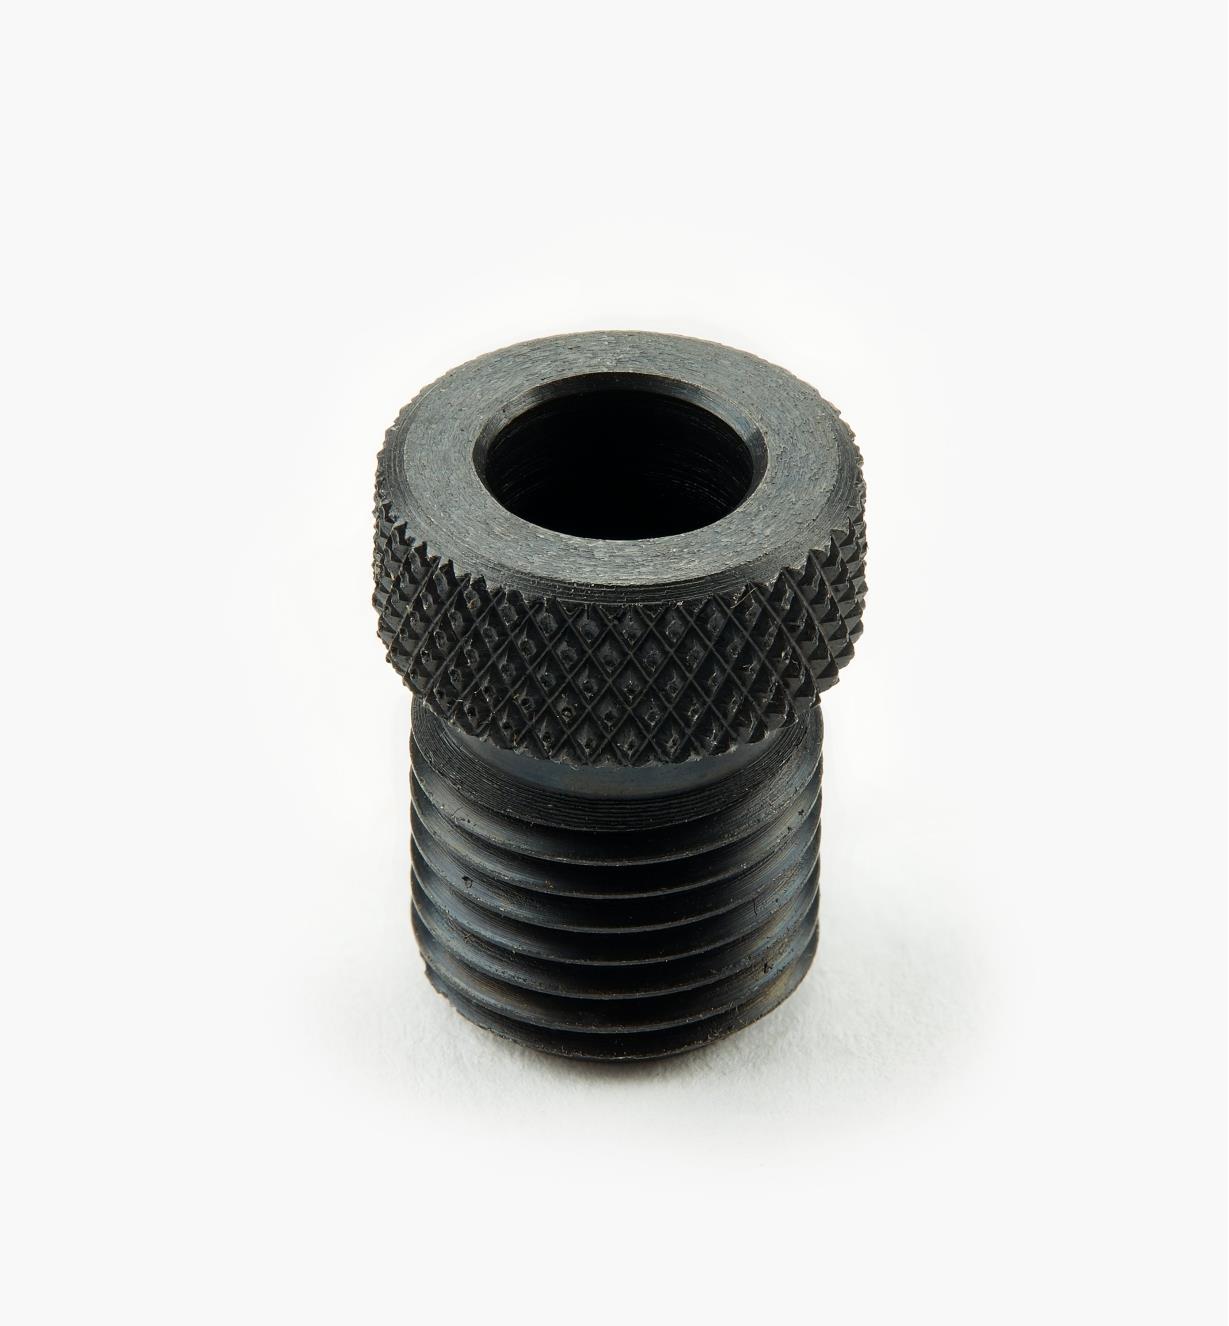
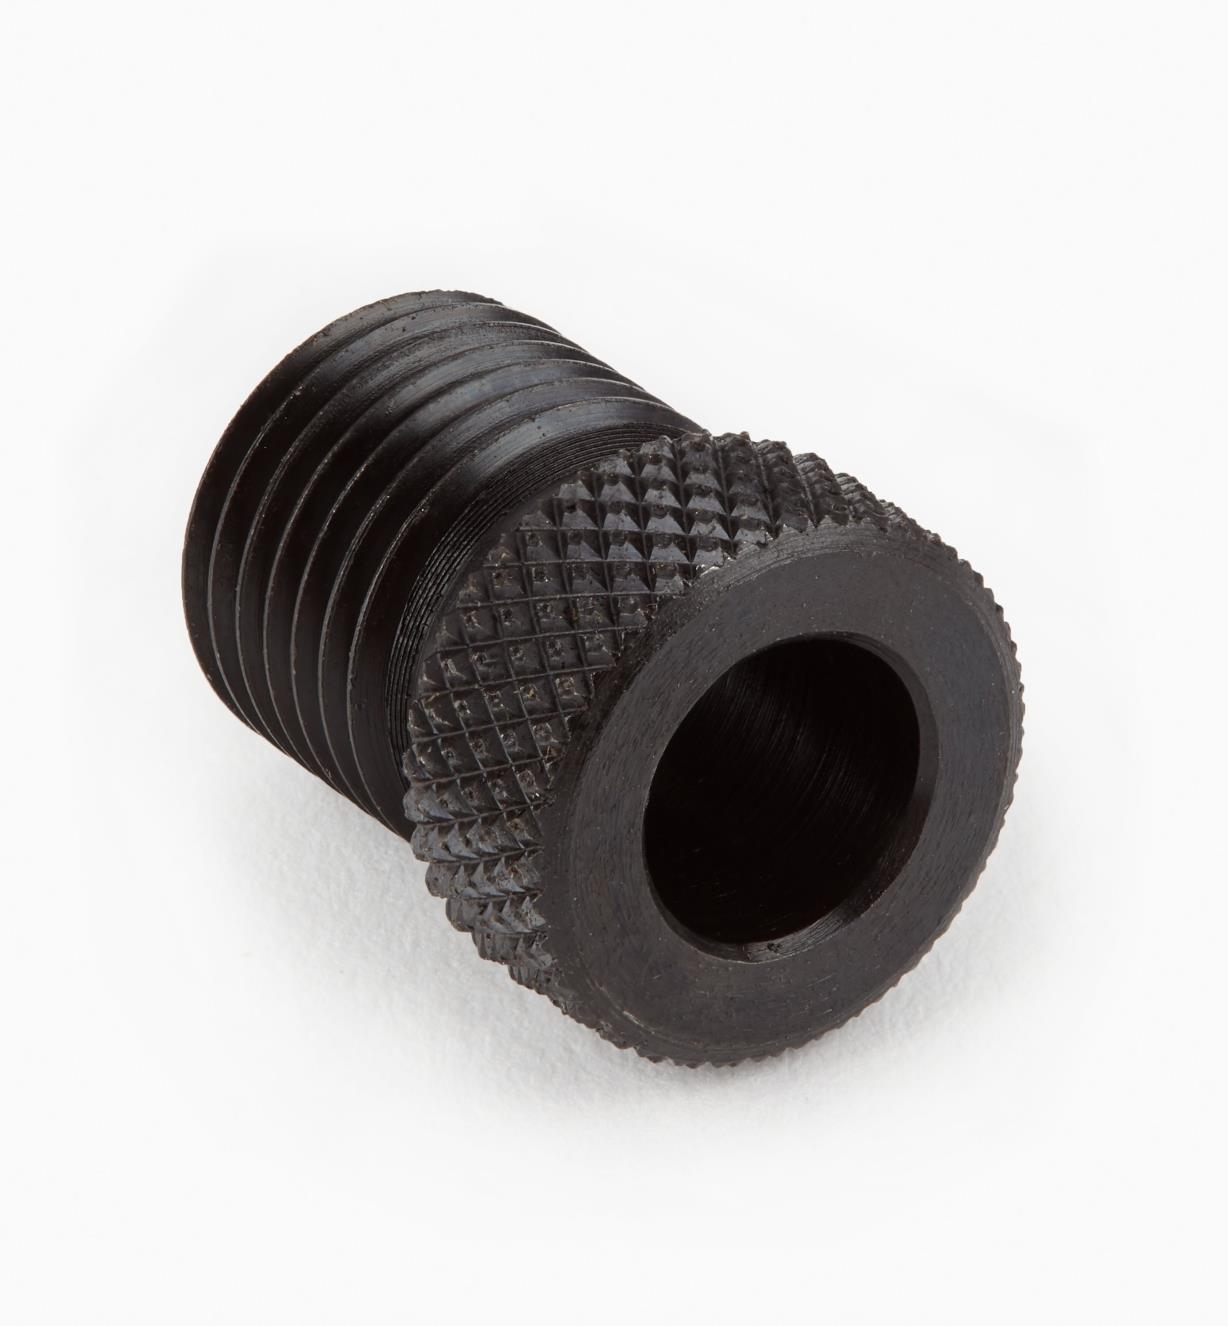
I spent three hours last year fighting with a drill jig that kept wandering off its marks. The issue wasn't my drill press. It was Threaded Drill Guide Bushings and how poorly they seat in standard aluminum template plate. Once I figured that out, the whole process became tolerable. Threaded Drill Guide Bushings are precision sleeves with external threads on one or both ends, designed to screw directly into tapped holes in a drill jig or template plate. Their purpose is simple: they hold a replacement liner that guides your drill bit exactly where you want it, and when the liner wears out — which it will — you unscrew the old one and drop in a new one. The threaded connection keeps them positioned and stable while you're cutting.
What You Actually Need to Know Before You Buy Them
Most people buying these for the first time pick the wrong thread pitch. Drill bushings come in two main threading standards: metric (M6, M8, M10 being the most common) and imperial (1/4-28, 5/16-24, 3/8-24). Mix them up even slightly and your bushing will cross-thread on the first attempt. Take a caliper and a pitch gauge to the store, or at minimum measure your existing tapped holes before ordering. Here's the thing nobody mentions: the external diameter of the bushing body matters just as much as the thread. If you're press-fitting the bushing body into a guide plate hole before threading it in, that outer diameter needs to match your guide plate clearance hole within roughly 0.05mm. Too loose and the bushing wobbles under drilling pressure. Too tight and you're either hammering it in or splitting your template plate. I once bought a batch of M6 bushings with an OD of 8.00mm for a plate with 8.02mm clearance holes. They fit, but under the side load of a long twist drill pushing through steel, each bushing would slowly rotate inside its hole over the course of a job. I lost accuracy within thirty holes. The fix was to mill the guide plate holes down to 7.98mm and use a thin layer of threadlocker on the internal threads. Solved it completely.
Installation and Setup
Start with clean, deburred tapped holes. A little chip or burr in the thread means your bushing seats at an angle, and your drill guide won't be perpendicular to the workpiece. That single degree of lean compounds fast — especially if you're drilling blind holes where the bit is already fighting for alignment. Screw the bushing in by hand until it's finger-tight, then use a proper bushing wrench or a pair of needle-nose pliers with tape wrapped around the jaws. Don't overtighten. The threads on soft aluminum templates strip easier than you'd think. You want the bushing seated firmly and square, not cranked down so hard you've deformed the template material around the threads. After installing, check runout. Put a dial indicator against the inner bore and rotate the bushing by hand. Anything over 0.02mm TIR is going to show up as oversized holes or poor surface finish. If it's out of spec, back it out, inspect the threads on both the bushing and the template, and look for debris or cross-threading damage. Sometimes the bushing itself is out of round — cheaper bushings from unknown suppliers have this problem more often than you'd expect.
Get the Full Details
Common Mistakes That Waste Time and Material
The biggest mistake I see people making is reusing worn liners without replacing the bushing body. The liner takes the wear from the drill bit, sure, but the bushing body's internal threads are what hold everything in position. If you've been wrestling bushings in and out for months, those threads are going to elongate. A bushing that feels loose when you hand-tighten it is a bushing that will shift under load, regardless of how fresh the liner is. Replace the whole unit when the threading starts feeling sloppy. Another pitfall: assuming all bushings with the same thread size are interchangeable. They're not. Inner bore diameters vary by hundredths of a millimeter between manufacturers, and some brands offer stepped bushings with two different bore sizes in one body. If you're swapping between brands on the same jig, verify each bore size individually rather than trusting the spec sheet. There are also situations where threaded bushings simply won't work well. If your template is made from a material that galls easily — like stainless steel or titanium — the constant insertion and removal of threaded bushings will eat into the threads faster than you'd anticipate. In those cases, consider press-fit bushings with a retention collar or welded-in bushing inserts instead. They cost more upfront but save you from rebuilding your template every few months.
A Note on Liner Selection
Liners are the consumable part. Hardened steel liners will last significantly longer in abrasive materials like fiberglass-reinforced composites or cast iron. For softer materials like aluminum or mild steel, standard unhardened liners are fine and cheaper to replace. The tradeoff is that unhardened liners will deform if you ever use a bit that's slightly undersized — the bore enlarges asymmetrically and stays enlarged. I keep a small caliper by my bench and check liner ID every time I swap one out. A liner reading 0.1mm larger than its nominal size is done, even if it looks fine to the naked eye. One practical tip that has saved me more than once: when you're setting up a new drill jig, drill a test pattern into scrap material of the same thickness and composition as your actual workpiece. You'll catch issues like bushing deflection, chip evacuation problems, or coolant path interference before you commit to the real part. Takes twelve minutes and prevents a twenty-dollar mistake. Threaded Drill Guide Bushings are a straightforward component that becomes frustrating fast if you treat them as generic hardware. Pay attention to thread form, OD fit, and seating angle, and they'll hold accuracy for hundreds of holes. Ignore those details and you'll be spending more time chasing alignment than actually machining.