Carbide Tool Bits: What Actually Matters When You're Cutting Metal
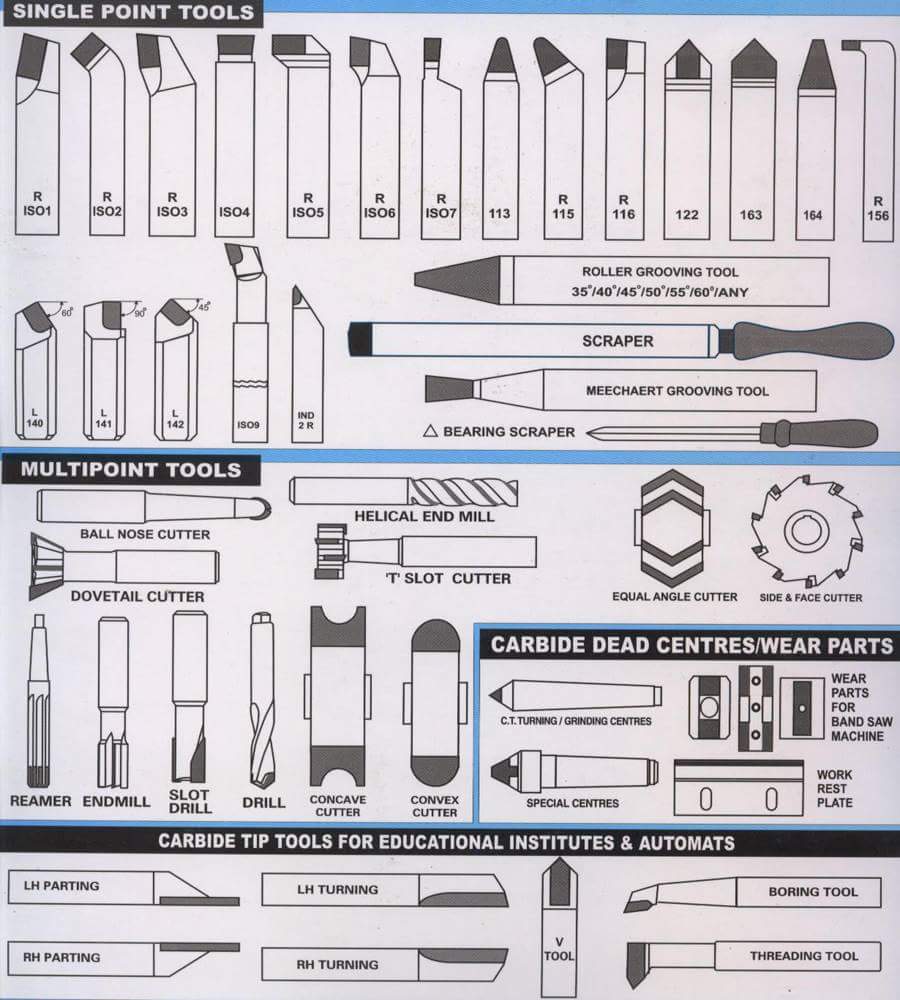
I spent three days last fall chasing a dimensional drift on a batch of 4140 shafts that should have been dead-on. We were holding .001" on a finishing pass, and every part was coming out about .0008" undersize by the time it hit the middle of the run. Turned out the problem wasn't our machine or our cooling setup. It was the way the tiny chamfer on the insert edge was loading up differently as the tool heated up, effectively changing the cutting geometry mid-cut. Once I switched to a insert with a slightly different nose radius and a different chipbreaker groove, the drift disappeared. That's the kind of thing you learn the hard way with carbide tool bits. A tool bit, in modern terms, is almost always a carbide insert clamped into a tool holder. The insert is the replaceable cutting edge. The holder is what mounts it to your machine. Understanding both pieces separately is the difference between running a reliable setup and guessing. The ISO standard designations on inserts look intimidating but they break down logically. Take something like CNMG 432-TS. CN is the shape code. M is the clearance angle, which is 25 degrees for an M-code insert. That 25-degree rear angle matters because it determines how much side clearance the insert has when it's cutting. G is the tolerance class. 432 is the size in eighths of an inch, so 432 equals 54 millimeters across. T is the thickness. TS is the chipbreaker style. Every letter and number in that code tells you something concrete about how the insert will behave.
Most people skip straight to the chipbreaker and ignore the shape and angle codes. That's a mistake. The shape code alone determines whether the insert can do facing, profiling, or both. A D style insert with its 35-degree diamond point does well in profiling and interrupted cuts. A C style with an 80-degree angle handles facing better. If you're primarily doing turning operations on a lathe, having a mix of both styles in your inventory matters more than people realize. When you're selecting an insert, the two variables that actually drive your decision are the workpiece material and the machine condition. Harder materials need stronger geometries with negative rakes. Softer, gummy materials like aluminum benefit from positive rakes and more aggressive chipbreakers. The chipbreaker isn't just about chip control. It shapes the effective cutting edge, determines the cutting forces, and affects surface finish directly. Two inserts made of the same carbide grade with different chipbreakers can cut the same material with completely different results. Hardness ratings on inserts use the RCA scale, though most people just look at the manufacturer's grade designation. A standard P-grade for steel might be around 86-88 RCA. An M-grade for stainless runs slightly higher. The higher the hardness, the more wear resistance you get, but also more brittleness. At 90 RCA and above, you're in territory where chipping becomes a real concern on interrupted cuts. If your setup has any kind of uneven stock or callouts, a 85-87 RCA insert will often outperform a harder one because it can absorb the shock.
Coatings are another area where the marketing oversells things. TiAlN coatings work well for steel at higher cutting speeds, giving you oxidation resistance up to about 900°C. AlCrN goes a step further and handles even higher temperatures. But on aluminum, neither helps much. Aluminum gums up coatings. For aluminum, an uncoated insert or one with a diamond-like carbon coating usually performs better. This isn't intuitive for most people. They see a shiny coated insert and assume it's universally superior. The tool holder is where a lot of good inserts go to waste. A holder with insufficient overhang will vibrate. A holder with poor clamping design will let the insert shift under load. Look at the clamping mechanism. Wedge clamps are the most common and they work fine when they're maintained. But if the wedge surface is worn or contaminated with chips, the insert won't seat properly. A properly seated insert should not move when you apply hand pressure to it after tightening. If it shifts at all, either the pocket is dirty or worn, or your torque procedure is wrong. Clamp torque matters more than most machinists account for. Under-tightened inserts migrate during cuts, which destroys dimensional stability and surface finish. Over-tightened inserts crack the carbide. Follow the manufacturer's torque specification exactly. Most insert pockets call for somewhere between 15 and 30 inch-pounds depending on the clamp style. A proper torque wrench costs about $40 and prevents a lot of wasted inserts.
Get the Full Details

Cutting fluid choice is tied directly to the material and the insert coating. For steel with a TiAlN coating, a sulfurized extreme pressure coolant works well. The sulfur forms a protective film on the cutting zone. For aluminum, a simple water-soluble oil at the recommended concentration is sufficient. Some people blast aluminum with high-pressure coolant and wonder why the part comes out pitted. The pressure itself can cause issues. Moderate flow at moderate pressure is usually better than maximum pressure on soft materials. Here's a practical setup method I use consistently. Start with the tool protruding from the holder about 1.5 times the tool diameter. That gives you stiffness without restricting chip flow. Set the tool height so the tip is at or slightly above the workpiece centerline. For roughing, a little above center helps. For finishing, exactly on center gives the best result. Mount the insert and torque the clamp. Run a test cut at half your target speed and half your target feed. Check the chip color. Blue chips mean you're running too hot. Adjust coolant flow or reduce speed. Grey or straw-colored chips are about right for most steel operations. Black chips mean the cutting speed is too low and you're rubbing instead of cutting. The common pitfall is assuming that faster is always better. Carbide can handle high speeds, but there's a point of diminishing returns. Once you exceed the optimal speed range for a given material and coating combination, the tool wears faster, the surface finish degrades, and your dimensional stability drops. The optimal speed range for roughing 4140 with a standard P-grade insert and TiAlN coating is typically 300 to 500 SFM. Finishing at 400 to 600 SFM with a finer chipbreaker gives better surface results. Going above 700 SFM on that same setup will dramatically shorten insert life with minimal productivity gain.
Another thing people miss is that insert reuse is almost never worth it. Some shops rotate inserts between operations to squeeze out extra cutting edges. The problem is that once an insert has been used, the geometry has changed. The sharp cutting edge has undergone plastic deformation. Reinstalling it at a different orientation changes the cutting dynamics and introduces variability. A fresh insert is cheap compared to a scrapped part. The biggest limitation of carbide tool bits is cost sensitivity. A single insert can run from $5 to $40 depending on size, grade, and coating. For a job shop running dozens of tools per shift, that adds up fast. In those situations, HSS tool bits are still viable for light cuts and setup work, though they can't match carbide at higher speeds. Ceramic inserts are another alternative for hardened materials above 45 HRC, but they're brittle and not suitable for most general machining. If you're just getting started with carbide inserts, the investment in quality holders pays for itself quickly. Cheap holders with imprecise pockets and weak clamping mechanisms will cost you more in ruined inserts and scrapped parts than a decent holder would in the first month. Stick with established brands for holders. For inserts, the major manufacturers all make competent products. The differences between brands often come down to consistency rather than performance. A Grade from one lot may perform differently from the same Grade in the next lot. That's just how coated carbide manufacturing works, and it's something to expect rather than fight.
Monitoring tool wear is straightforward if you know what to look for. Flank wear measured as VB on the ISO scale is the standard metric. For finishing operations, replace the insert when flank wear reaches 0.3 mm. For roughing, you can push to 0.8 mm or more before replacement. Surface finish deterioration usually precedes dimensional failure, so if your finished surface starts looking dull or shows visible chatter marks, the insert needs replacing regardless of what the wear measurement says. Checking insert condition every 15 to 30 minutes during a run, depending on the operation, takes about 30 seconds and catches problems before they become expensive. Coolant delivery through the tool is worth the extra cost if you're doing deep hole drilling or deep cavity milling. Through-tool coolant pushes chips out of the cut instead of letting them recut against the workpiece. The pressure required is typically 80 to 150 PSI through the tool itself. Most standard flood coolant systems don't deliver adequate pressure through internal channels. You'll need a high-pressure pump or a dedicated coolant manifold for that setup. The rule of thumb is that internal coolant gives you roughly 20 to 30 percent longer tool life in deep-cutting applications compared to external flood only. The insert pocket in the holder should be cleaned before every insert change. Use compressed air and a brass brush. Never use steel brushes or files on the pocket surfaces. A brass brush is hard enough to remove chips but won't damage the precision-ground surfaces. Chips left in the pocket create a gap between the insert and the seat, which allows the insert to flex during cutting and ruins both the insert and the workpiece.