TPM starts long before you write a single line of training material
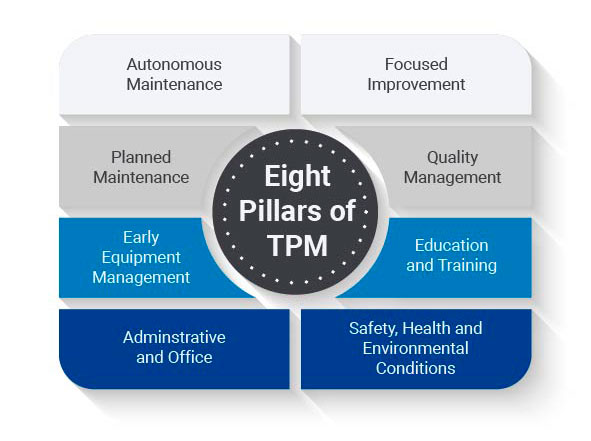
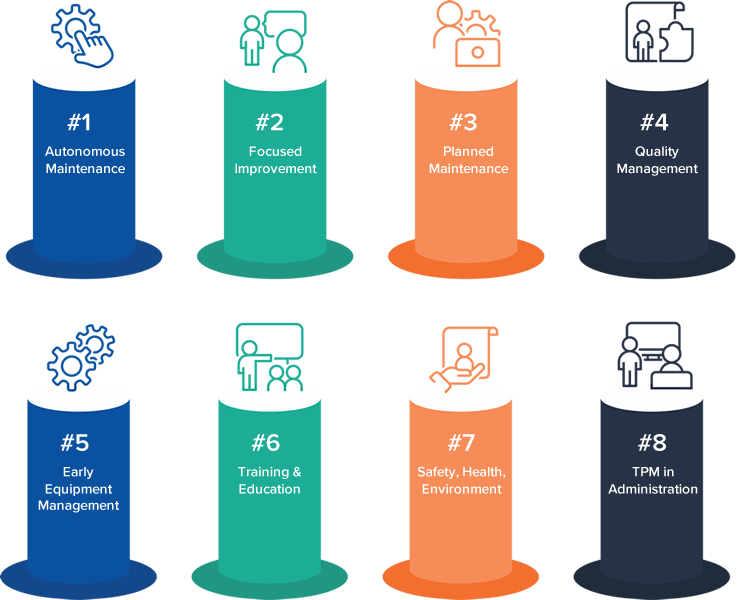
Most people think Total Productive Maintenance Training is about putting together a slide deck and sending it to floor operators. That's how you end up with a binder that nobody opens and equipment that still breaks down every Tuesday. The real work happens before the first training session. You need to understand what actually fails on your machines, how often it fails, and which failures cost the most in downtime. I spent three years working TPM into production lines where the previous attempt had left everyone cynical. The problem wasn't that TPM was bad. It was that nobody had bothered to connect the training to anything that operators cared about. Start by mapping the autonomous maintenance pillars. These are the seven steps where operators learn to care for their own equipment instead of calling maintenance for everything. The steps go from initial cleaning and inspection to systematic improvement, but jumping into step three without properly executing steps one and two is where most programs fall apart. Step one is total cleaning. Not wipe-down cleaning. This means taking the machine apart enough to find grease pockets, worn seals, cracked hoses, and misaligned guards that have been buried under grime for months. Operators will discover things that have been leaking or loose since installation. They will also discover that some of these problems have been there so long they accepted them as normal. Here's a practical detail that doesn't get enough attention: when you clean during step one, you take photos. Document the before state. These photos become the baseline for every future comparison and they are the only thing that keeps management interested when the initial excitement fades. Without visual evidence, TPM looks like organized cleaning to anyone who isn't directly involved.
Step two introduces basic inspections. This is where you teach operators what to look for — abnormal sounds, vibration patterns, oil levels, belt tension, unusual smells. The key is making these inspections specific and measurable. "Check the belt" is useless. "Check belt tension using a deflection gauge and record the reading between the two idlers" is something you can train, track, and act on. Operators need clear acceptance criteria, not general advice. Once steps one and two are locked in, you move to source and location problems. This is about eliminating contamination sources and making it impossible to miss a problem when it occurs. I worked on a packaging line where the training team spent six weeks just moving pneumatic lines and installing transparent sight glasses on reservoirs. The result was that operators could see a leak within minutes instead of discovering it when product quality dropped an hour later. The upfront effort felt extreme until we measured the reduction in unplanned stops.
The training methodology matters more than the content
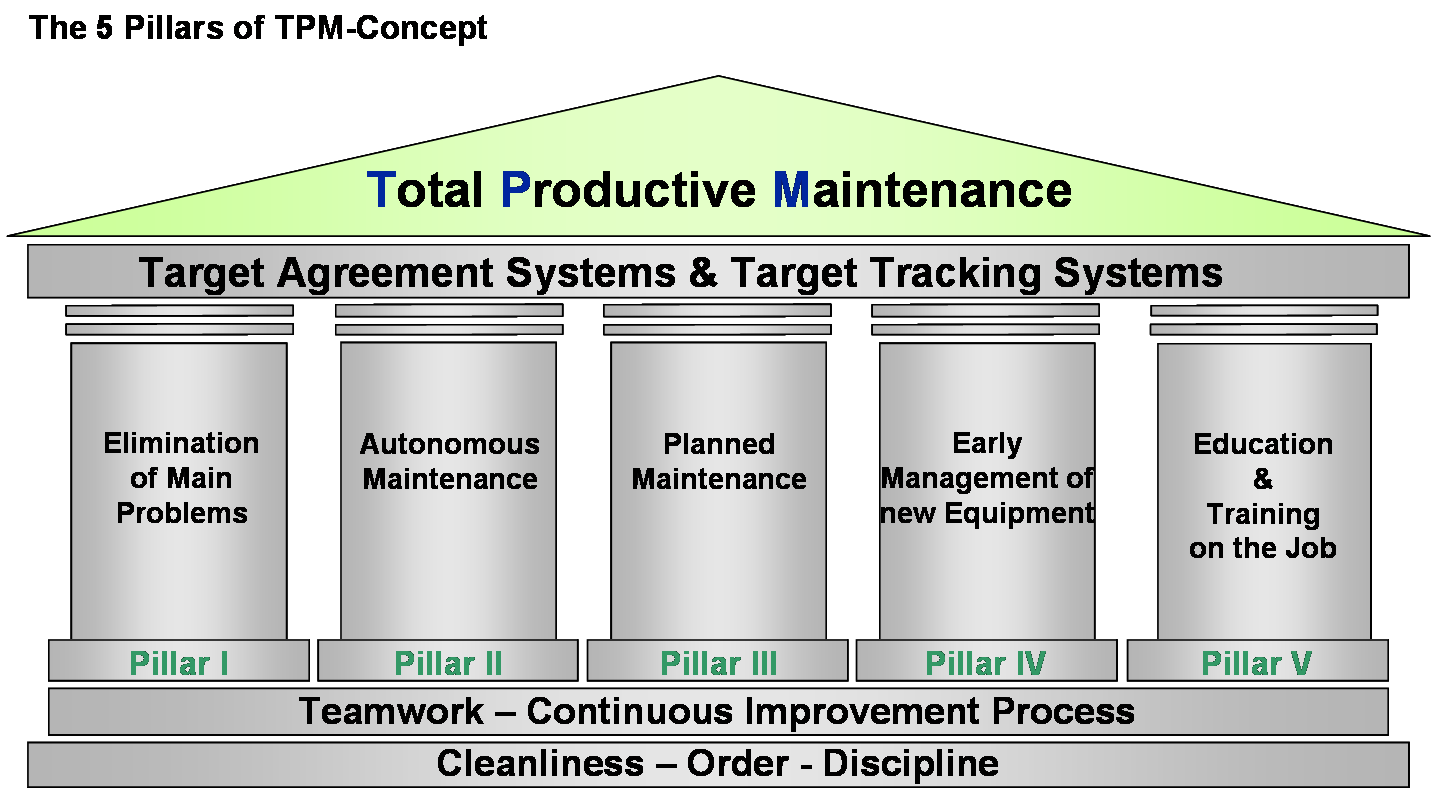
TPM training should follow the same structure as the maintenance pillars themselves. You start with knowledge transfer through classroom sessions, then move to hands-on practice on actual equipment, and finally to independent application with coaching. Skipping the hands-on portion is the most common mistake I see. Reading about bearing lubrication intervals doesn't help anyone until they've actually opened a housing, cleaned out old grease, packed it correctly, and reassembled it. I've seen seasoned mechanics argue against hands-on operator training because they felt it was "below their skill level." That attitude destroys TPM faster than anything else. Operators who understand how their equipment works internally will report issues earlier and more accurately. That alone justifies the training investment. Another counter-intuitive point: the best TPM training doesn't focus on prevention first. It starts with breakdown analysis. Take operators to the failed part. Show them exactly what happened, why it happened, and what the downstream consequences were. When an operator understands that a $40 seal failure caused $12,000 in damaged product and forty minutes of downtime, their attitude toward preventive care shifts immediately. Data creates urgency. Checklists don't. Train in small groups of four to six people maximum. Anything larger and you lose the ability to individualize and you waste machine time watching people who aren't touching equipment. Rotate the groups so everyone gets hands-on access during production windows. Coordinate with the scheduling team to use changeover times, lunch breaks, or low-demand shifts for practical sessions. Don't pull operators off the line during peak production unless it's an actual training day scheduled weeks in advance.
Get the Full Details
Common pitfalls that ruin TPM programs before they start
The biggest failure point I encounter is organizational misalignment. You can train operators perfectly, but if the maintenance department continues to treat them as non-technical staff who shouldn't touch equipment, the training will be undermined every single day. I had a situation where operators were trained to perform Level 1 maintenance tasks and had written approval from the plant manager. Two weeks in, the maintenance supervisor started rejecting their work and redid everything overnight. The operators learned the right lesson quickly: stop trying. The program died within three months. You need executive-level buy-in that goes beyond a signed memo. It needs to be visible in daily decisions about who has authority over equipment changes. A second pitfall is treating TPM as a maintenance initiative rather than an operational philosophy. When you position it solely under the maintenance department, production never fully engages. TPM requires production supervisors to invest their own time in the training process and to hold their teams accountable for the new standards. If production sees TPM as something maintenance does to them instead of something maintenance does with them, you'll get compliance at best and active resistance at worst. The OEE improvements that justify TPM come from production owning their equipment, not from maintenance fixing things faster. Don't expect immediate results. The first quarter of TPM training typically shows a dip in productivity as operators learn new procedures and spend time on cleaning and inspection tasks that weren't part of their routine. This is normal. The data from my experience shows that genuine OEE improvement usually becomes measurable around month four or five, with the steepest gains appearing between months six and twelve. If leadership doesn't understand this timeline, they will kill the program during the uncomfortable transition period.
Measuring whether the training is actually working
Track specific metrics from day one. Operator-led inspection completion rates, number of abnormality findings per shift, time to detect and report defects, and the ratio of reactive versus planned work orders. These numbers tell you whether the training is translating into behavior change. If inspection completion is high but abnormality findings are low, your operators aren't inspecting properly or they've become desensitized and stopped noticing deviations. If abnormality findings are high but work orders aren't being generated, there's a communication or authority breakdown between operators and the maintenance request system. Use Andon systems or simple color-coded boards where operators can post maintenance concerns in real time. I implemented a system where operators placed a red tag on any abnormality they found and the maintenance team had to respond within a defined timeframe. This created accountability on both sides. Operators couldn't claim they didn't notice problems when the tags were visible to everyone, and maintenance couldn't ignore reported issues without explanation. The system was simple enough to set up in a weekend and it reduced average response time from four hours to under forty minutes within two weeks.
Structured approach to building your training curriculum
Break your Total Productive Maintenance Training into modules that correspond to the autonomous maintenance pillars. Module one covers equipment fundamentals and safety protocols. Module two is cleaning and inspection techniques specific to your machinery. Module three addresses lubrication standards and oil analysis basics. Module four focuses on minor adjustment and tightening procedures. Module five deals with troubleshooting common failure modes. Each module should have a knowledge component, a demonstration, and a supervised practice session before the operator is considered competent. Create a competency matrix for each piece of equipment. Track which operators have completed which modules, which tasks they're qualified to perform independently, and which require supervision. This matrix becomes your roster for scheduling production coverage during training and for identifying skill gaps before they cause problems. Update it quarterly. People forget things. Competency isn't permanent. The training materials themselves should be visual and minimal. Use diagrams, photographs of correct and incorrect states, and simple checklists rather than paragraphs of text. Operators on the floor don't read manuals. They reference quick guides that fit on a laminated card or a nearby whiteboard. I've seen training programs fail because the instructional materials were designed for HR compliance instead of for actual field use. If your training document would take twenty minutes to read during an eight-hour shift, redesign it.
When TPM training doesn't work and what to do instead
TPM is not appropriate for every environment. Highly automated cells where equipment is sealed and requires specialized diagnostic tools to service are not good candidates for autonomous maintenance. In those cases, you're better off investing in targeted technical training for your maintenance specialists and using predictive maintenance technologies like vibration analysis and thermography. TPM assumes that operator involvement improves outcomes. When the equipment is beyond the operator's ability to meaningfully interact with, forcing TPM onto that equipment creates frustration and false confidence. Similarly, TPM training loses effectiveness in high-turnover environments where operators rotate through positions every few months. The knowledge base never stabilizes because the people who learned it are gone. If your turnover rate exceeds twenty-five percent annually, consider pairing TPM with a robust knowledge transfer system where departing operators document their learnings and train their replacements before leaving. Otherwise you'll be retraining the same concepts every quarter with diminishing returns. Small batch job shops present another challenge. TPM thrives on repetition and standardization. If you're running fifty different product configurations on the same line with different setups each time, the standardized cleaning and inspection routines become impractical. In these environments, focus TPM training on the common platform elements across all configurations rather than trying to create unique procedures for every product variant.
The training itself should be ongoing, not a one-time event. Schedule refresher sessions quarterly and conduct annual skill assessments using the competency matrix. New equipment introductions should trigger updated training modules before the equipment reaches the floor. If you introduce a new machine and expect operators to maintain it without updated training, you're setting them up to fail and the equipment to suffer. I've seen this happen repeatedly with capital equipment purchases where the vendor delivered the machine and the manual and considered their obligation fulfilled. The first breakdown usually reveals that nothing was ever taught about the specific failure modes of that particular unit.