Setting Up a Type 1 Gage Study in Minitab
A Type 1 Gage Study checks whether your measurement system is capable of distinguishing parts within a small, controlled range. It's usually the first gauge study someone runs, and it's also the one people get wrong most often because it feels too simple. In Minitab, you go to Stat > Quality Tools > Gage Study > Type 1 Gage Study. The dialog gives you two main paths: one where you supply your own reference values, and another where Minitab generates them for you based on a part width or tolerance range. Both work, but they answer slightly different questions. The part I keep seeing wrong is the reference value setup. People pick ten parts that look similar, measure each one ten times, and then run the study. The output comes back with an %P/T ratio that looks terrible, and they blame the gage. Usually the problem is that the reference standard deviation they fed into the analysis doesn't match the actual variation in their part set. Minitab uses that reference value to calculate process capability numbers, not to judge repeatability directly. If your reference std dev is off, all the ratios in the output are misleading.
Type 1 Gage Study Minitab
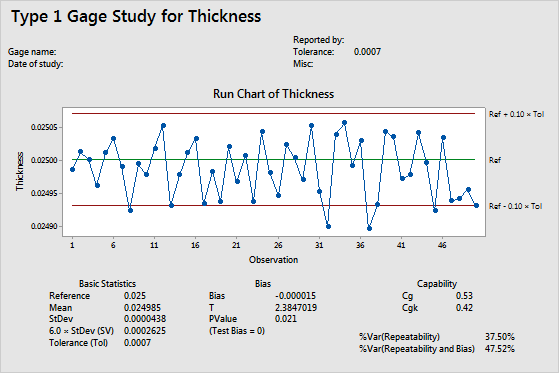
Here's the workflow I actually use. First, get a master part or a calibrated reference standard that sits at the midpoint of your expected measurement range. Measure it 25 times in a single session if possible—fewer setups, same environmental conditions, same operator. That 25-repeat sample gives you the repeatability estimate, which is the only thing this study is really designed to capture properly. When you open the dialog, select the option to enter reference values and use your own known standard. Minitab will then compute bias, precision, and the various capability indices. The bias test tells you whether the gauge reading systematically deviates from the reference. The precision-to-tolerance ratio tells you whether the gauge noise is acceptable relative to your specification limits. One thing that catches people off guard: the %Study Var and %P/T outputs in a Type 1 study assume you plug in an external estimate of process variation. If you don't have a reliable process sigma, these numbers are meaningless. The bias confidence interval is the only output you can trust without additional data. I've seen engineers sign off on a study because the %P/T came in under 30%, then later discover that the %P/T was calculated using a reference std dev pulled from a completely different product line.
A Specific Problem I Encountered
I was running a Type 1 study on a coordinate measuring machine with a reference gauge block set. The blocks were calibrated at 20 degrees Celsius, and the shop floor sat around 23. The initial study showed a bias of about 0.003 mm, which was right at the edge of what the spec allowed. I thought the probe was drifting, so I re-checked the setup, cleaned the block, re-zeroed everything, and ran it again. Same result. The workaround was straightforward but easy to miss. I measured the actual temperature of the gauge block with a contact thermometer before each trial, logged it, and then applied a thermal expansion correction based on the block's coefficient. Once I accounted for the 3-degree difference, the apparent bias dropped to near zero. The gage wasn't faulty. The reference value was just shifted by thermal expansion. Minitab has no built-in temperature compensation, so you handle that outside the software and feed the corrected reference value in.
Get the Full Details

What This Study Actually Tells You—and What It Doesn't
Type 1 studies measure repeatability and bias under ideal conditions. They do not measure reproducibility because there's only one operator. They do not capture linearity across the measurement range unless you run separate studies at multiple reference points. And they do not replace a full Gage R&R study when you need to understand variation between operators or over time. If your process variation is tight and your gauge needs to resolve small differences, a Type 1 study is fine for an initial screen. But once you move to production, you'll need a crossed or nested Gage R&R. The Type 1 result alone will not satisfy most auditors, and it won't give you enough information to set control limits or make pass/fail decisions on incoming parts. Minitab's output also includes an Anderson-Darling normality test on the repeated measurements. If that p-value is below 0.05, your measurement error isn't normally distributed, which invalidates the confidence intervals and capability estimates. In practice, this usually means your part surface isn't consistent enough for the probe, or there's a settling issue with the fixture. I had a case where the non-normality was caused by a magnetic chuck picking up fine metal particulate between readings. Cleaning the fixture surface between each measurement fixed it.
The key takeaway is that the Type 1 study in Minitab is a tool, not a verdict. It gives you a snapshot of one aspect of measurement system performance. Use it to catch obvious bias problems early. Don't treat the %P/T number as the final word on whether your gage is good enough.