How unitized curtain wall systems actually get designed from scratch
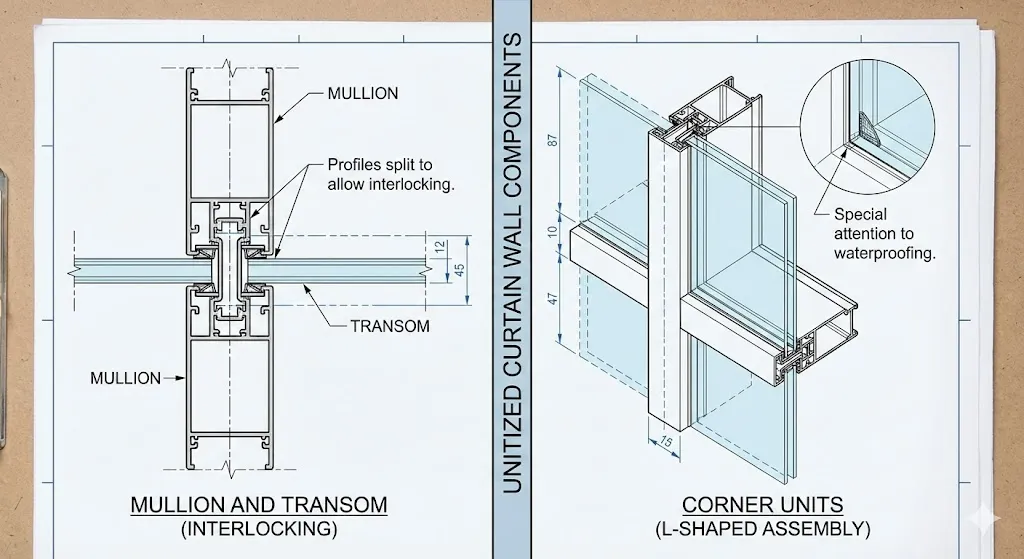
I have spent more years than I care to count dealing with unitized systems on projects across three continents. The design process is not glamorous, and it rarely goes exactly to plan. But once you understand the mechanics of how these systems move from concept to shop drawing to installation, the whole thing stops feeling like guesswork. This is a Unitized Curtain Wall Design Guide for people who actually need to get the work done without fighting the software or arguing with fabricators over tolerances that do not exist in reality. Unitized curtain walls are factory-assembled panels that get shipped to site and hung sequentially from the building structure. Unlike stick systems, where mullions and transoms are assembled piece by piece on the facade, unitized panels carry their own structural integrity within the module. That changes everything about how you approach design. The load path, thermal breaks, drainage, and tolerancing all shift because the panel itself becomes a completed assembly before it ever leaves the factory.
Starting with the Unitized Curtain Wall Design Guide framework
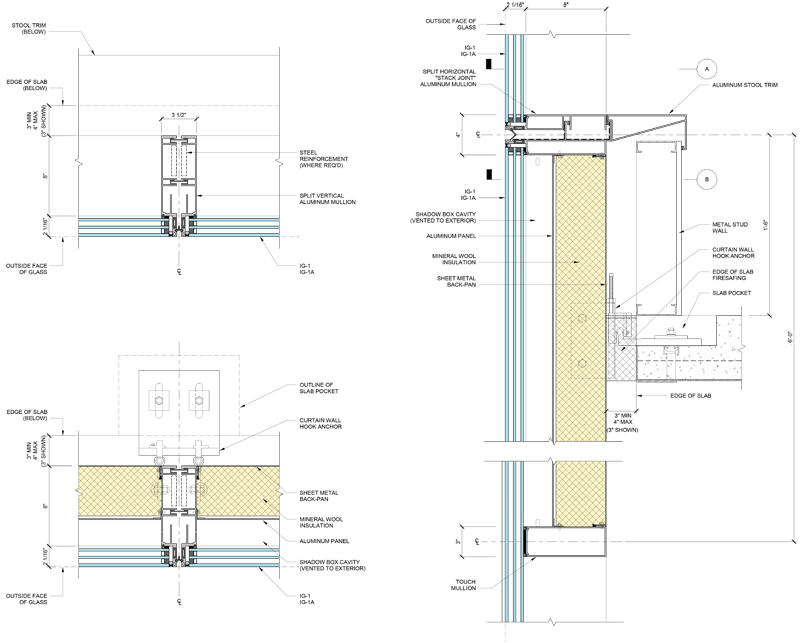
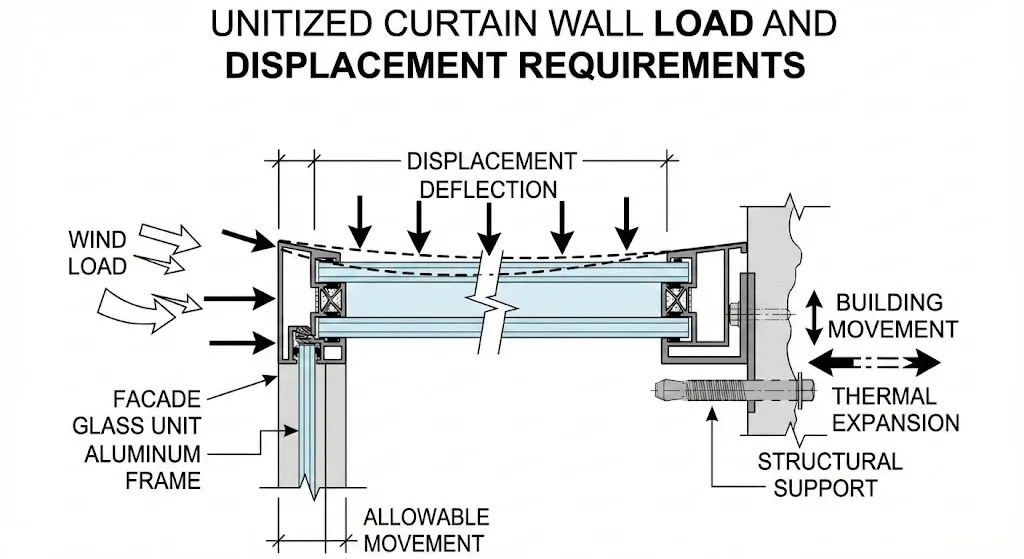
Most designers begin by pulling together the architectural intent, structural constraints, and performance requirements, then work toward a system layout that satisfies all three without one collapsing the others. Here is the order I actually use, which is different from what most textbooks suggest. First, define the bay grid. Not the aesthetic one. The structural one. The distance between primary building columns or floor edges determines your unit widths, and getting this wrong early means reworking every shop drawing later. I once had a project in Dubai where the structural engineer's column location was off by 40 millimeters from the architectural drawing. Because we had already locked in a unit module based on the architectural plan, the facade coordinator had to develop custom transition units and adjust the anchorage pattern across 200 panels. It cost us six weeks and roughly 180,000 dollars in rework. The lesson was simple: verify structural coordinates against as-built conditions before you commit to a unit grid, and build in adjustment ranges at every anchor point. After the bay grid, you establish the vertical panel height. This is typically tied to floor-to-floor dimension, but you need to account for floor slab tolerance, which is usually plus or minus 15 millimeters per floor in reinforced concrete construction. Your unit design should incorporate slotted connections or shims that can absorb that variance without compromising the weather seal.
The core design elements that actually matter
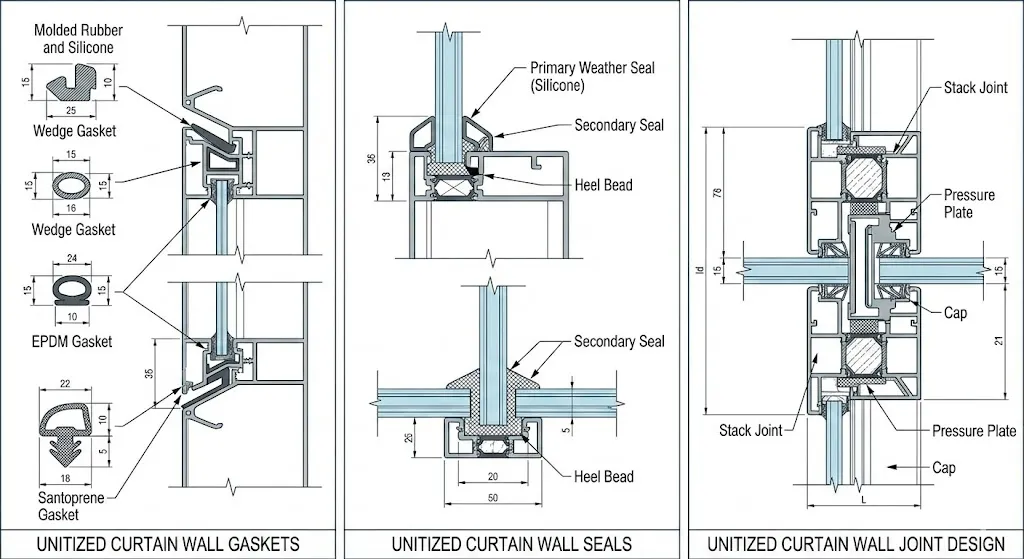
There are several components in a unitized system, but only a few of them cause real problems in practice. The rest are details you can look up. The ones that require actual thought are the anchorage interface, the inter-panel joint, and the thermal management strategy. Anchorage is where the unit connects to the building structure. Most systems use a bracket attached to the floor slab or beam, with a slotted connection that allows for vertical and horizontal adjustment. The bracket spacing typically runs between 1200 and 2400 millimeters on center, depending on the panel size and wind load. I find it useful to design the anchorage first because it dictates the panel size limits. If your brackets are too far apart, the mullion section needs to be heavier, which increases material cost and shipping weight. If they are too close, you get too many interface points and more potential for leakage. The inter-panel joint is the second critical element. This is where unit A meets unit B horizontally and vertically. The joint design controls water infiltration, air permeability, and thermal bridging. Most failures in the field happen at these joints, not within the panel itself. A typical joint uses a combination of compressed foam backing rod, structural silicone sealant, and a water reservoir channel that directs any incidental water back outward. The key detail that people miss is the pressure equalization. If the joint cavity is not properly vented, wind pressure differences between the interior and exterior of the joint can force water through microscopic gaps. I specify a minimum of two vent holes per linear meter of horizontal joint, placed at the lowest point of the reservoir channel.
Get the Full Details
Thermal management in unitized systems is more complex than people assume. The aluminum frameconducts heat readily, so thermal breaks are non-negotiable. A proper thermal break uses a polyamide strip with a minimum thermal resistance of 0.05 square meter-kelvin per watt. But here is the counter-intuitive part: adding a thermal break does not automatically give you a good U-value. The overall thermal performance depends heavily on the glazing area to frame area ratio. I have seen designs where a fancy thermal break was undermined by a frame that was too bulky, resulting in a worse U-value than a simpler system with better glass selection. The fix is usually to optimize the mullion profile first, then add the thermal break to what remains, rather than the other way around.
Simulation and analysis before you commit to fabrication
Once the basic geometry is locked, you run structural analysis on the mullions and transoms under wind load, seismic drift, and self-weight combinations. Most engineers use software like SAP2000, RISA, or dedicated facade analysis tools for this. The output tells you whether your selected extrusion profiles are adequate or if you need to upgrade to a heavier section. Water and air infiltration testing follows the structural analysis. Standalone test panels are subjected to cyclic pressure differentials while water spray is applied at specified rates. The industry standard references are ASTM E331 for water infiltration and ASTM E283 for air permeability. A well-designed unitized panel should achieve a water resistance rating of at least 600 pascals and an air leakage rate below 0.3 cubic feet per minute per square foot at the design pressure. If your initial design does not meet these targets, you adjust the gasket configuration or add additional sealant lines rather than simply increasing the frame size. Thermal simulation is the third pillar. Tools like Therm by LBNL or Wolfsteel's software package model the heat transfer through the entire panel assembly, including the glazing, frame, and spandrel sections. The result is a U-value and a solar heat gain coefficient that feed into the building energy model. I always run this simulation iteratively, adjusting glass specs and frame geometry until the values align with the project's energy targets. Skipping this step is one of the most common mistakes I see, and it leads to complaints from occupants and failed energy compliance reviews.
Shop drawing production and coordination
After analysis passes, you produce shop drawings. These are the documents the fabricator uses to manufacture the units, and they need to be precise. Every panel gets a unique identifier, along with dimensions, anchor locations, gasket specifications, glazing schedules, and opening sequences. The shop drawings also include the installation sequence, showing how each unit connects to the previous one and how adjustments are made for tolerance accumulation. Coordination with other trades is where this process often falls apart. The curtain wall designer needs input from the structural engineer on anchor points, from the MEP team on penetrations through the spandrel area, and from the interior designer on sill details and head conditions. I recommend establishing a coordination matrix at the start of the project that tracks every interface point and assigns responsibility. Without this, you will get last-minute clashes that force design changes mid-production, which is the fastest way to blow a schedule and a budget. One practical tip that has saved me multiple times: always include a mock-up panel in the contract. A full-scale test assembly built at the fabricator's facility allows you to verify the joint details, installation sequence, and appearance before committing to full production. It typically takes one to two weeks to build and inspect a mock-up, but it prevents issues that would otherwise cost ten times that amount to fix in the field. I have found that about 70 percent of the problems I encounter during production could have been caught during mock-up review.

Known limitations and when unitized systems are the wrong choice
Unitized curtain walls are not a universal solution. They have clear constraints that designers sometimes overlook. The primary limitation is transportation. Units are large, heavy, and awkward to ship. Maximum panel widths are typically limited to about 3000 millimeters by road transport regulations in most countries, and heights are constrained by container or truck dimensions. If your project is in a remote location with poor logistics access, unitized systems become impractical, and a stick system may be the only viable option despite the longer on-site installation time. Another limitation is the lead time. Factory fabrication requires tooling setup and production scheduling, which typically runs 8 to 12 weeks from approved shop drawings to delivered panels. For fast-track projects with compressed schedules, this lead time can be a bottleneck. I have worked on projects where the construction team needed panels in four weeks, and the only solution was to pay premium expediting fees to the fabricator or revert to a stick system for those sections. Cost is the third constraint. Unitized systems have higher upfront costs due to factory assembly, quality control, and packaging. The per-square-meter price is typically 20 to 40 percent higher than an equivalent stick system. The trade-off is faster installation and better quality control, but if the project budget is tight, that premium can be prohibitive. In these cases, a hybrid approach works well: use unitized panels for the standard floors and switch to stick construction for complex or irregular sections.
There is also a design flexibility limitation. Unitized systems work best with repetitive panel geometries. If your facade has many unique angles, curved sections, or varying panel sizes, the cost and lead time advantages diminish significantly. Custom units require individual tooling and longer production cycles, which erodes the efficiency that makes unitized systems attractive in the first place.
A realistic edge case I dealt with recently
Last year I worked on a high-rise project in Singapore where the building had a twisted floor plan. Each floor rotated approximately 2 degrees relative to the one below it, which meant the unitized panels could not use a standard rectangular grid. The facade coordinator initially proposed custom-fabricated triangular transition units for every third floor, but the lead time for those custom pieces would have delayed the entire procurement schedule by eight weeks. The workaround was to design a modular system with adjustable anchor brackets that could accommodate the rotational offset within a single unit width. Instead of changing the panel geometry, we changed the attachment interface. The brackets allowed a horizontal adjustment range of plus or minus 50 millimeters, which absorbed the cumulative drift from floor to floor without requiring custom units. We ran finite element analysis on the adjusted bracket configurations to confirm structural adequacy, then produced standard units for 95 percent of the facade. The remaining 5 percent used slightly modified transoms at the transition zones. This solution cut the fabrication time by roughly three weeks and saved about 25 percent on the total unit cost compared to the original custom-panel approach.
What to watch for during quality control
Even with thorough design and analysis, problems can emerge during manufacturing and installation. The quality control process needs to catch these before the panels reach the site. Key inspection points include the thermal break integrity, gasket compression and continuity, silicone application quality, anchor slot alignment, and glazing bead seating. I recommend a three-stage inspection: incoming material verification, in-process production checks, and final pre-shipment review. Each stage should have documented checklists with pass-or-fail criteria, and any failures should trigger a corrective action report before the affected batch proceeds. Field installation quality is equally important. A perfectly manufactured panel installed incorrectly will fail. Installers need clear instructions on bracket engagement sequence, leveling procedures, joint alignment, and sealant application conditions. Temperature and humidity affect silicone cure times, so installation windows should be specified based on local weather data. I always include a site-specific installation manual with every shipment, tailored to the project location and season. This Unitized Curtain Wall Design Guide covers the practical steps I rely on when designing these systems. The process is iterative and requires coordination across multiple disciplines, but the fundamentals remain the same regardless of project size or location. Get the bay grid right, design the joints thoroughly, verify with simulation, build a mock-up, and maintain strict quality control. The details matter, but the sequence matters more.