Heat Transfer Tags on the Production Floor
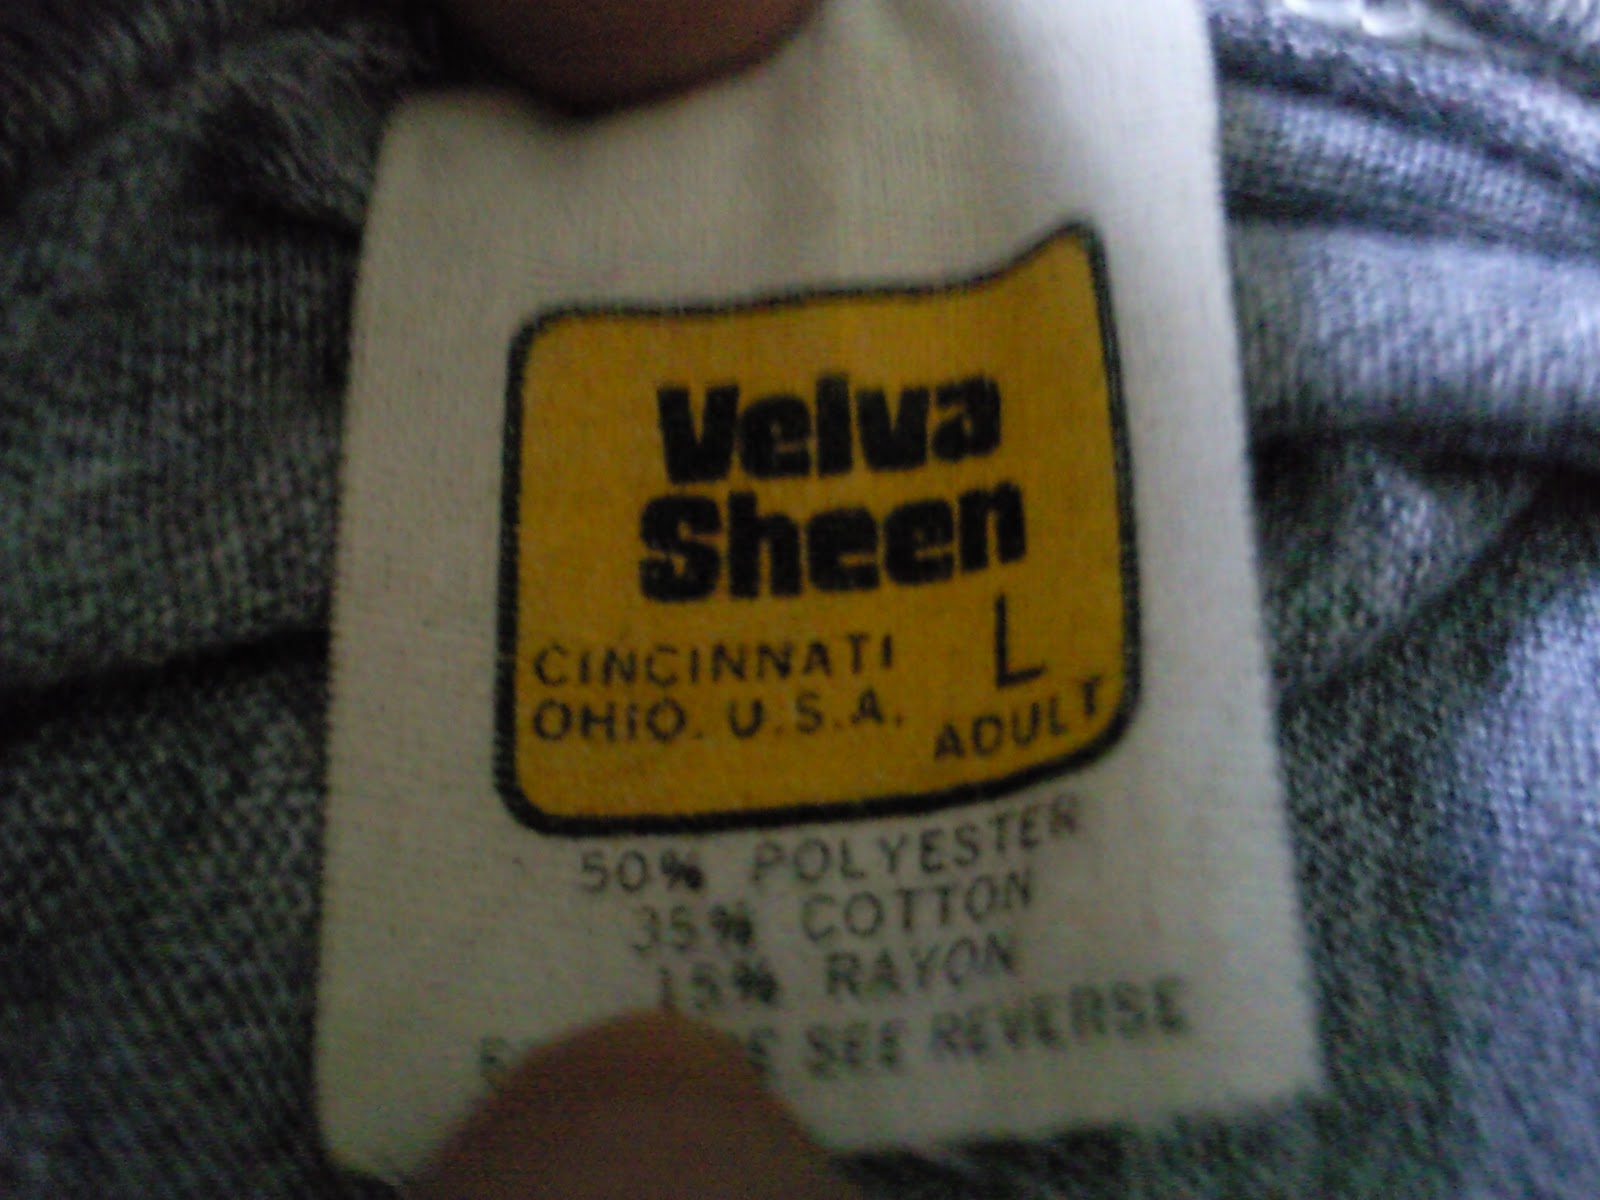
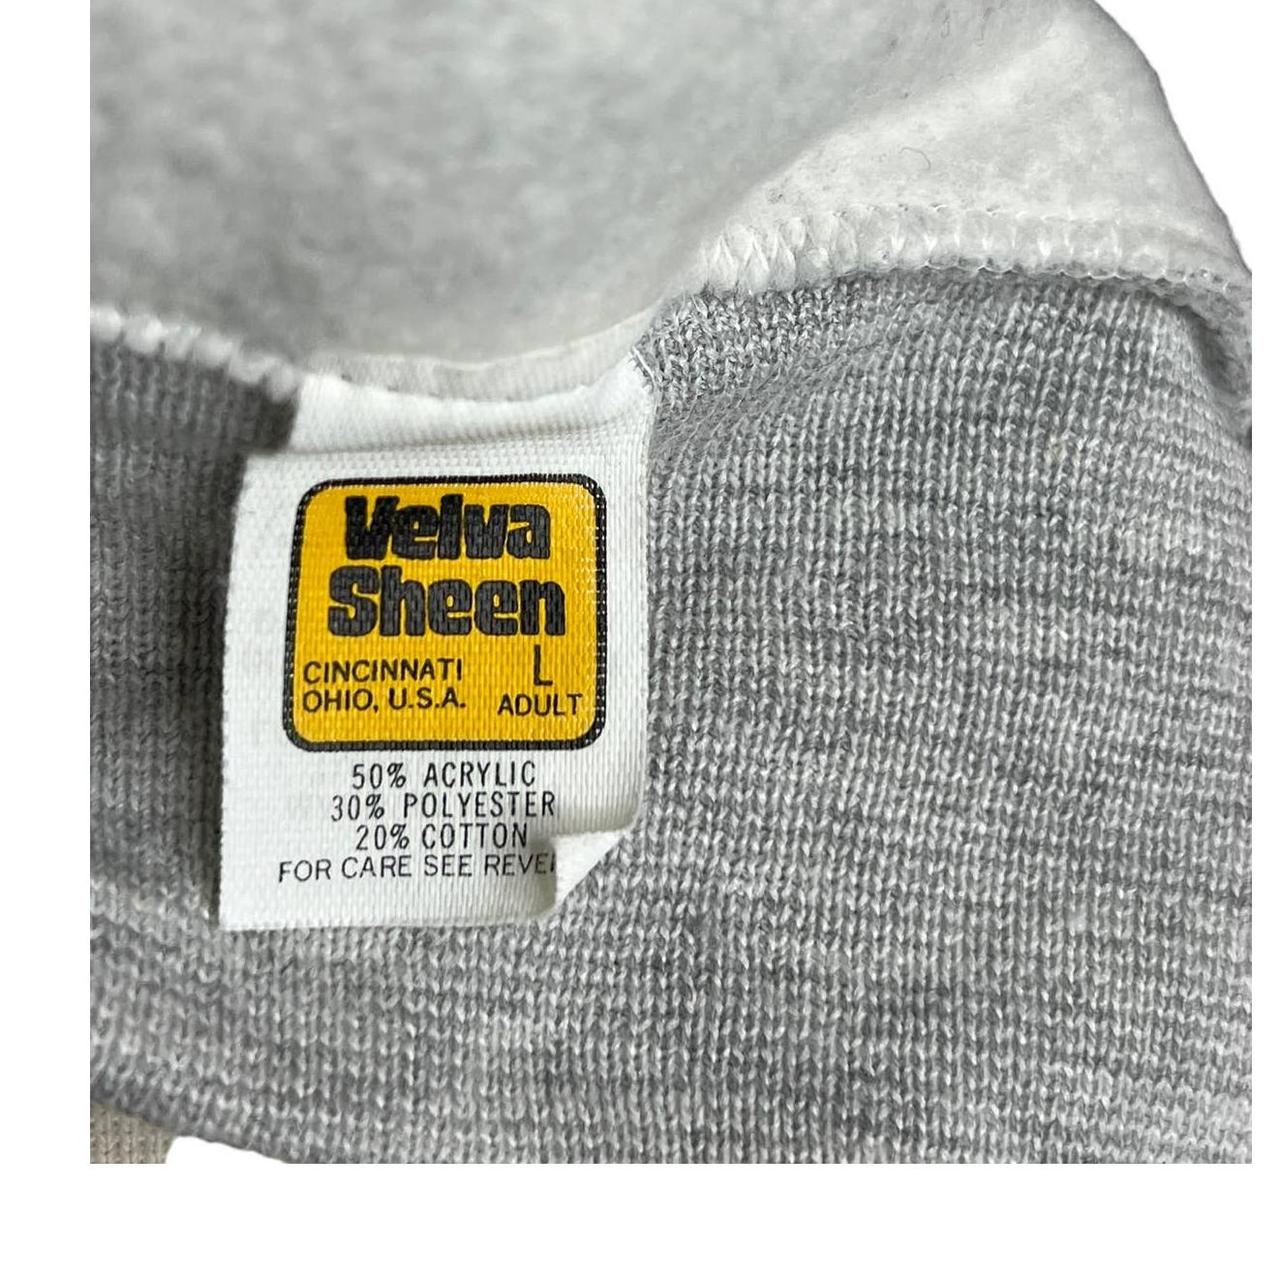
Velva Sheen is one of the older names in heat transfer labeling. The company originally came out of the textile industry when manufacturers were shifting from stitched woven labels to printed heat-applied ones. That transition happened mostly in the 1980s and 1990s, and Velva Sheen tags became a standard reference point in garment factories across North America and Mexico. If you've worked with apparel production for any length of time, you've probably seen their logos on supplier spec sheets. The tag history aspect comes down to tracking which label runs, which batch, and which order those tags belong to — basically a production traceability record.Understanding Velva Sheen Tag History
Tag history in this context means the documentation trail that follows a heat transfer label through the manufacturing process. It starts when the label design is approved and ends when the finished garment ships. In a typical setup, your tag history file contains the order number, SKU, label position, material specs, ink type, and the date the tags were applied. Some operations also track the temperature and pressure settings used during application, though that's more common in higher-compliance environments like workwear or uniforms. I'm not going to pretend there's a single universal format for this. Different factories use different systems. Some track it in spreadsheets. Others use dedicated PLM software. The core information stays roughly the same regardless of tool.
How Heat Transfer Tag Application Actually Works
The process itself is straightforward, but the details matter if you want consistent results. Velva Sheen tags are printed on a silicone-coated carrier film with thermoplastic adhesive on the back. You position the tag on the garment, apply heat and pressure with a flatbed or swing-away press, then peel the carrier film away while the adhesive is still molten. The label bonds to the fabric. That's the basic cycle. What most people don't account for is how fabric composition changes the process. A 100% cotton polyester blend at 65/35 behaves differently than a ring-spun cotton or a tri-blend. The adhesive melt point is fixed, but the fabric's heat tolerance and moisture content vary. I learned this the hard way on a run of women's activewear labels. The spec sheet called for 320 degrees Fahrenheit with a 12-second dwell time. Standard stuff. Worked fine on the test swatches. Then we ran it on the actual garment fabric and the labels started delaminating after about eight wash cycles. The tri-blend fabric had a different thermal expansion rate than the cotton swatches, and the adhesive bond was stressed enough to crack microscopically over repeated laundering. The workaround was reducing the press temperature to 295 degrees and extending the dwell time to 15 seconds. Lower peak heat but longer exposure gave the adhesive a more gradual bond formation that accommodated the fabric's movement. It also meant slower throughput on the press — about 20 percent more time per unit — but the reject rate dropped to near zero. That tradeoff is worth knowing before you commit to a full production run.
Common Problems and Practical Fixes
There are a few recurring issues with heat transfer tag application that show up regardless of brand. Here's what actually causes them and what tends to work. Ink cracking after wash — This usually means the adhesive didn't fully wet out the fabric fibers, or the press temperature was too high and carbonized the ink layer. Check your platen flatness. A worn silicone pad or a press plate that isn't perfectly parallel will create uneven pressure zones where the bond fails in spots. I've seen this on old 16x20 presses where the lower platen had minor warping from years of thermal cycling. The fix isn't always replacing the platen — sometimes a proper silicone pad replacement and recalibration of parallelism is enough. Peel temperature errors — Hot peel vs. cold peel is baked into the tag design. Velva Sheen tags typically specify cold peel, meaning you wait for the assembly to cool before removing the carrier film. Some operators peel hot because it's faster, not realizing the adhesive hasn't fully cured. The result is edge lifting and reduced wash durability. There's no shortcut here. Wait for the cooling period. It adds about 30 to 45 seconds per label, which adds up across a full production run but prevents returns.
Get the Full Details

Fabric contamination — Sizing agents, fabric softeners left over from pre-treatment, or even oils from handlers can create a barrier between the adhesive and the fiber. This is especially relevant with synthetic fabrics that go through antimicrobial or stain-resistant finishing treatments. If labels are failing adhesion tests on a particular fabric lot, run a simple wipe test with isopropyl alcohol on a hidden area before committing to the full run. It won't damage the garment and it will tell you whether the surface is clean enough for bonding.
Setting Up a Reasonable Tag History System
You don't need expensive software to track tag history. A structured spreadsheet with consistent columns works fine for small to mid-volume operations. The columns that actually matter are order number, style number, label position, quantity ordered, quantity applied, vendor lot number, and application date. Add wash test results and reject rates if your quality process requires that level of detail. The real value in tag history isn't the record-keeping itself. It's the ability to trace a problem backward. When a customer reports that labels are curling after three washes, you should be able to pull the tag history and identify which fabric lot, which press setting, and which application date that garment came from. That traceability is what separates a professional operation from one that reacts to problems instead of preventing them. If you're dealing with larger volume or multiple SKUs, the spreadsheet approach breaks down. At that point you're looking at integrating tag data into your existing ERP or PLM system. The migration cost is real, but so is the cost of losing track of label batches across hundreds of orders. Start simple, then scale the system to match your actual throughput rather than whatever the software vendor recommends.
When Heat Transfer Tags Are the Wrong Choice
They aren't universally applicable. Printed heat transfer labels struggle on high-pile fabrics like fleece or terry cloth where the adhesive can't make full contact with the fiber surface. They also perform poorly on fabrics treated with durable water repellent finishes, since those coatings create a hydrophobic barrier that interferes with adhesive bonding. In those cases, woven labels or printed folded labels stitched into the garment are more reliable. It's not a branding issue. It's a materials science issue, and pushing heat transfer tags into applications they weren't designed for will cost you more in rework than you'd save on production time. Velva Sheen Tag History ultimately comes down to documenting what you did, why you did it that way, and having the data available when something goes wrong. That's it. The technology behind the labels has been around long enough that most of the surprises are avoidable if you pay attention to the details that matter.