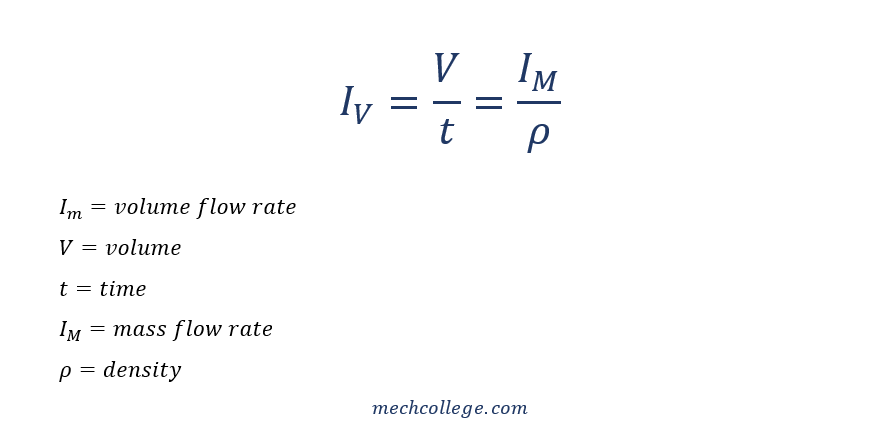
Working with Flow Rates in Real Piping Systems
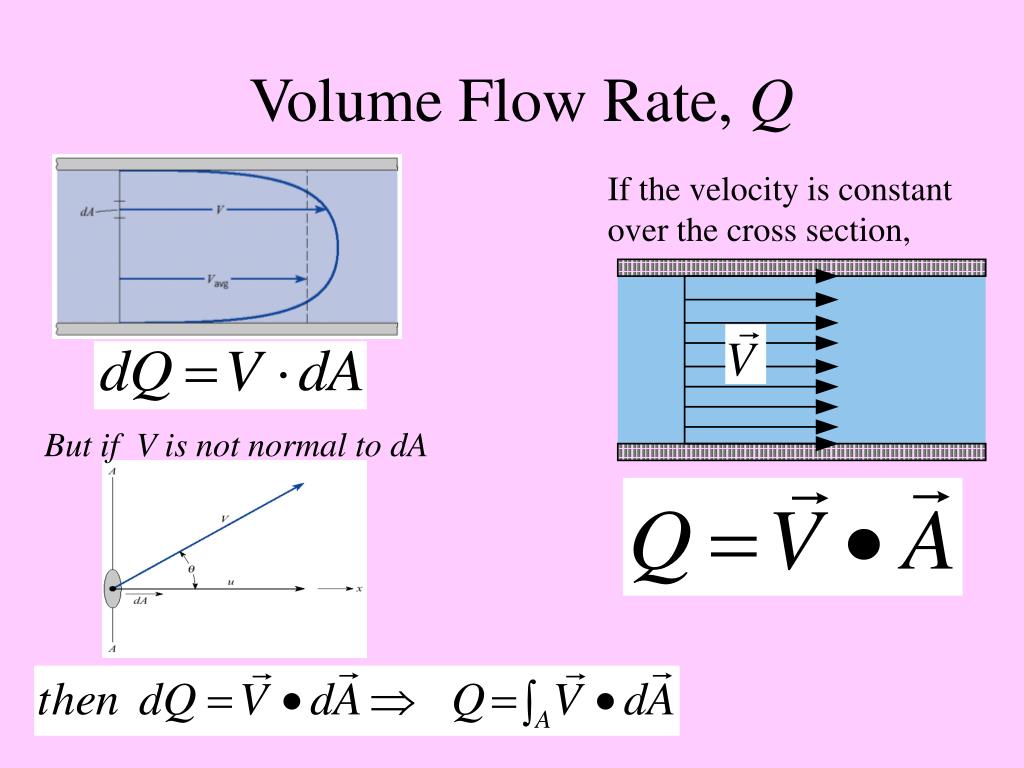
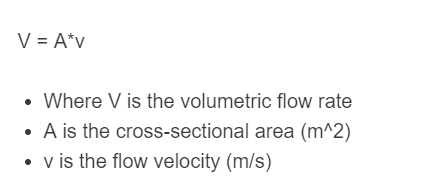
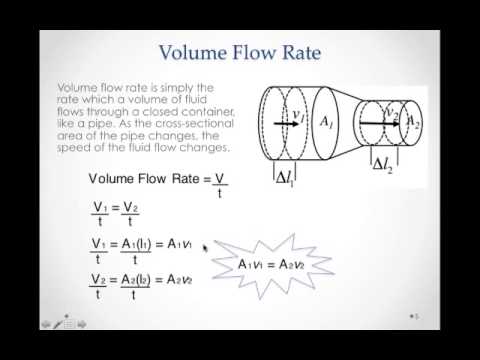
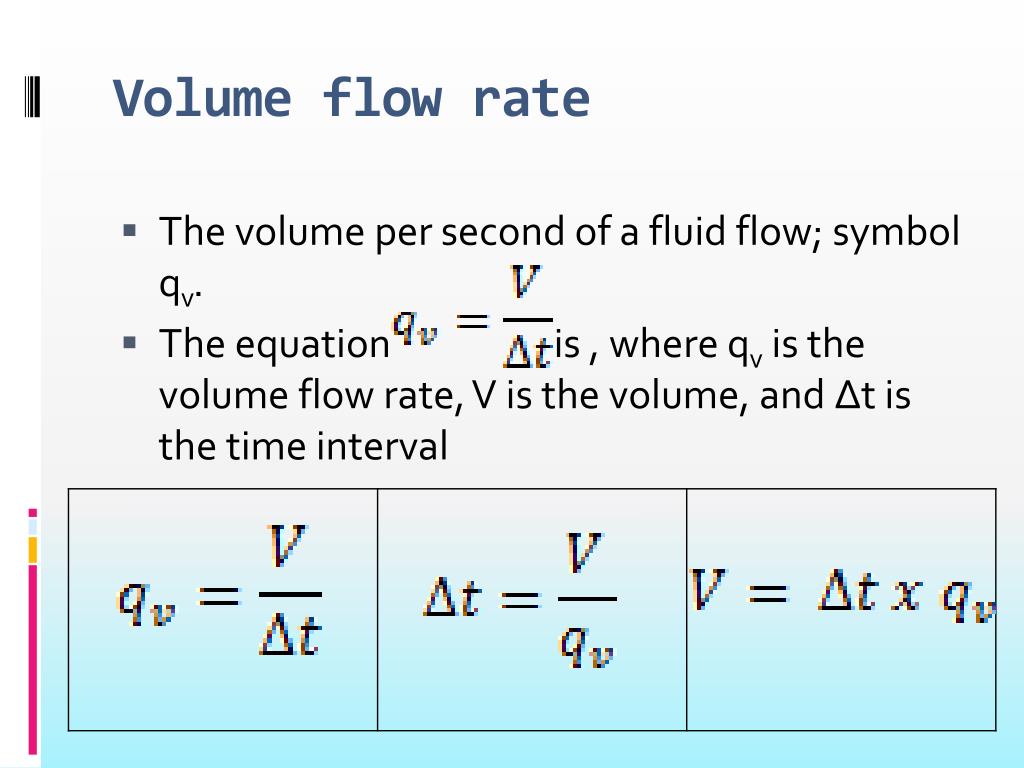
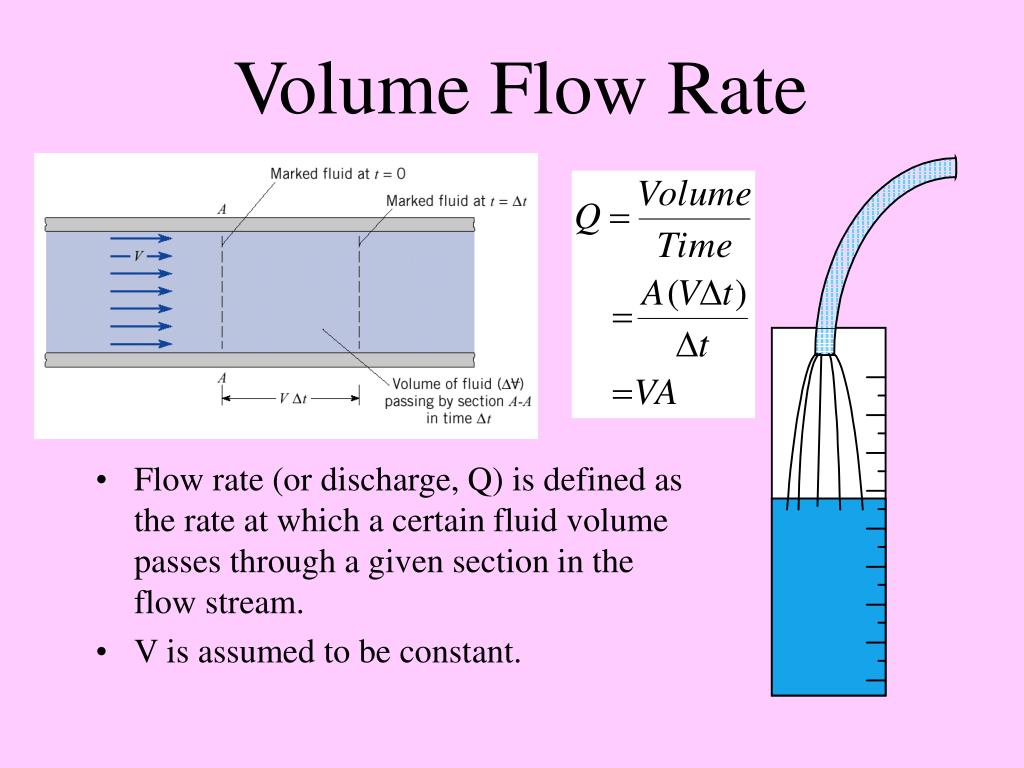
The Volumetric Flow Rate Equation is Q = A × v, where Q is flow rate, A is cross-sectional area, and v is fluid velocity. It sounds like something you'd learn in a freshman fluid mechanics class and immediately forget, but it's the backbone of literally every process I've worked on in chemical engineering and water treatment over the last decade. The problem isn't the formula itself. It's what happens when you try to use it on a real system where everything is slightly wrong. Start with what you actually know. In practice, you're rarely given both area and velocity. More often, you're looking at a pipe schedule, a pump curve, or a flow meter reading, and you need to back into one of those variables. Here's the sequence I use. Identify the pipe inner diameter from the schedule. A 2-inch Schedule 40 steel pipe doesn't have an inner diameter of 2 inches. It's 2.067 inches, which is about 0.1723 feet or 0.0524 meters. Get that wrong and your area calculation is off by however much you were off on the diameter assumption. Square that radius, multiply by pi, and you have your cross-sectional area.
Now for velocity. If you have a flow rate given in GPM, convert it to cubic feet per second or cubic meters per second depending on your unit system. One GPM is approximately 0.002228 cubic feet per second. Divide that by your area and you get velocity in feet per second. If you have velocity and need flow rate, reverse it. Multiply area by velocity and convert back to whatever unit your system expects. I ran into a specific issue last year on a cooling water loop that was designed for 800 GPM through a 4-inch line. The pump was delivering about 920 GPM based on the flow meter, but the pressure drop across the heat exchanger was way higher than the design called for. I recalculated the velocity using the actual flow meter reading and the correct inner diameter of the 4-inch Schedule 40 pipe, which came out to roughly 10.2 feet per second. The design velocity should have been around 8.8 feet per second. The excess pressure drop wasn't a blockage or a valve issue. It was just velocity squared acting on the exchanger's internal channels. We throttled the discharge valve and brought it back into the designed range. That's the kind of thing the equation tells you, but only if you actually do the math with real numbers instead of design spec numbers.
Where People Mess This Up
Unit conversion is the most common failure point. I've seen people plug GPM directly into an equation that requires cubic feet per second and then wonder why their result is off by a factor of 448. Another frequent mistake is using the outer diameter instead of the inner diameter for the area calculation. Pipe sizing has been standardized for over a century and nobody seems to remember that the nominal size isn't the actual size until they get a result that's 20 percent too high and can't figure out where it came from. There's also a subtler issue with compressible fluids. The Volumetric Flow Rate Equation assumes incompressible flow, which is fine for liquids and for gases at low pressures relative to their absolute pressure. If you're working with gas flowing through a restriction where the pressure drops significantly, the volume changes as the gas expands. Using a single volumetric flow rate at inlet conditions will give you increasingly wrong answers the higher the pressure drop gets. In those cases, you need to switch to mass flow rate or use an expansion factor correction. I had a natural gas sampling line where the differential pressure across the orifice plate was about 15 percent of the absolute upstream pressure. The vendor's flow calculation was off by roughly 8 percent because they treated it as incompressible. Once I applied the expansivity factor Y from ISO 5167, the numbers matched the reference meter within 1 percent. Another thing that trips people up is turbulent versus laminar flow assumptions. The equation Q = A × v doesn't care about the Reynolds number. It works regardless. But if you're using velocity to infer flow rate through a measurement device that has a known operating range, being outside that range means your (reading) is meaningless. For vortex shedders and orifice plates, the lower turndown ratio is usually around 3:1. Below that, the signal becomes dominated by noise and pulsations from pumps or valves upstream. I've seen engineers trust flow readings from vortex meters on lines with recirculation loops that were creating low-frequency pressure waves. The meter was reporting flow that varied by plus or minus 40 percent even though the actual pump speed was constant. The issue wasn't the equation. It was the installation geometry. Thirty diameters of straight pipe upstream is the textbook recommendation, but field conditions rarely cooperate.
Get the Full Details
A Practical Walkthrough
Let me walk through a real example from a recent project. We were sizing a chemical dosing line for a water conditioning system. The specification called for a maximum chemical feed of 50 GPM through a 1.5-inch Schedule 80 PVC pipe. I needed to verify the velocity wouldn't exceed recommendations for that type of service. First, the inner diameter of 1.5-inch Schedule 80 PVC is 1.402 inches, or 0.1168 feet. Radius is half of that, so 0.0584 feet. Area equals pi times radius squared, which gives 0.01072 square feet. Converting 50 GPM to cubic feet per second: 50 times 0.002228 equals 0.1114 cubic feet per second. Velocity is flow rate divided by area, so 0.1114 divided by 0.01072 equals about 10.4 feet per second. For liquid chemical service in PVC, velocities above 10 feet per second start raising erosion and noise concerns, and above 15 feet per second you're looking at real pipe wear over time. At 10.4 feet per second, we were right on the edge. I upsized to 2-inch Schedule 80 PVC, which has an inner diameter of 1.939 inches or 0.1616 feet. The new area is 0.0819 square feet. Same flow rate of 0.1114 cubic feet per second divided by 0.0819 gives 1.36 feet per second. That's a much more reasonable velocity for continuous chemical service. The pressure drop across the line dropped by roughly a factor of ten because velocity squared is what drives friction losses in turbulent flow.
Limitations You Should Actually Care About
The Volumetric Flow Rate Equation is deceptively simple. It gives you a number, but that number is only as good as your inputs. If your pipe isn't completely full, the area is wrong. If your fluid is a slurry or contains entrained gas, the velocity you measure at one point isn't representative of the bulk flow. If your pipe has significant build-up or corrosion reducing the inner diameter, your calculated area from the nominal size is optimistic and your velocity is understated. For open channel flow, this equation doesn't apply at all. You'd use Manning's equation or a similar relationship instead. For multi-phase flow, you're dealing with slip velocities between phases and the concept of a single bulk velocity breaks down. I once tried to apply Q = A × v to a two-phase steam-water mixture in a reheater feed line and got results that made no physical sense because the void fraction was changing along the length of the pipe. Switching to a two-phase flow correlation and using mass flux instead of volumetric flow rate resolved the discrepancy. If you need a downloadable reference for the basic equation and common unit conversions, most engineering handbooks and the NIST Engineering Statistics Handbook have sections on flow rate calculations. The ASME MFC-3M standard covers flow measurement instrumentation tolerances if you're working with certified meters. Those documents are generally available through professional societies or university libraries.
When to Trust the Math and When to Measure
The equation works perfectly when your conditions match its assumptions. In the field, they rarely do. I've found that the most reliable approach is to calculate first, then verify with an independent measurement. If your calculated flow rate based on pipe dimensions and pump curves differs from what a calibrated ultrasonic clamp-on meter is reporting by more than 5 percent, something is wrong. It could be the pipe isn't full. It could be the meter needs re, or it could be that your assumed pipe diameter doesn't match the actual installed pipe. Go back to the source data and check each variable individually rather than assuming the entire model is flawed. Temperature also matters more than most people account for. Liquid viscosity changes with temperature, which affects the Reynolds number and the friction factor, which affects the pressure drop and therefore the flow rate for a given pump curve. I worked on a site where the process fluid was heated from 60 degrees Fahrenheit to 140 degrees Fahrenheit during summer operation, and the flow rate through a fixed-orifice metering point increased by about 12 percent purely because the viscosity dropped and the friction losses decreased. The pump curve shifted slightly too, but the dominant effect was the viscosity change. Nobody had updated the flow calculations for the higher temperature condition. The Volumetric Flow Rate Equation isn't complicated. It's easy to misuse because it's easy to trust. The ones who get burned are the ones who plug numbers in without checking whether the assumptions behind those numbers still hold under actual operating conditions.