How An Orifice Actually Works In The Field
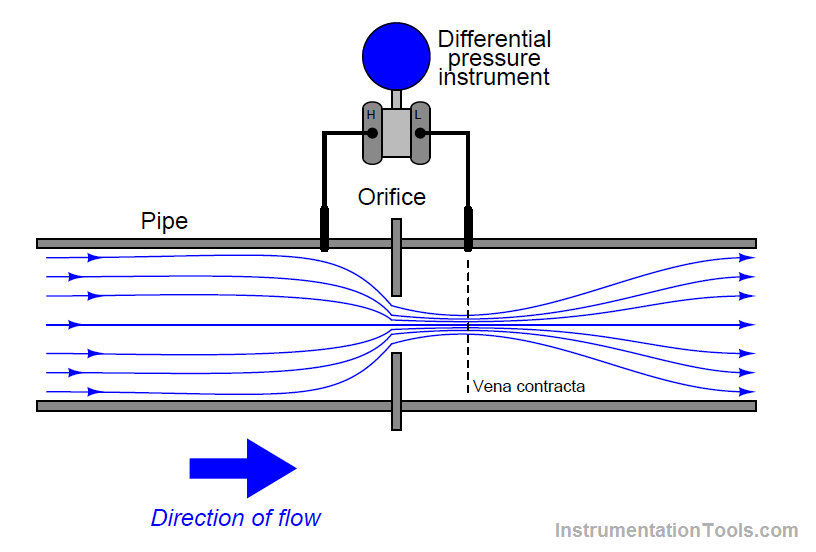
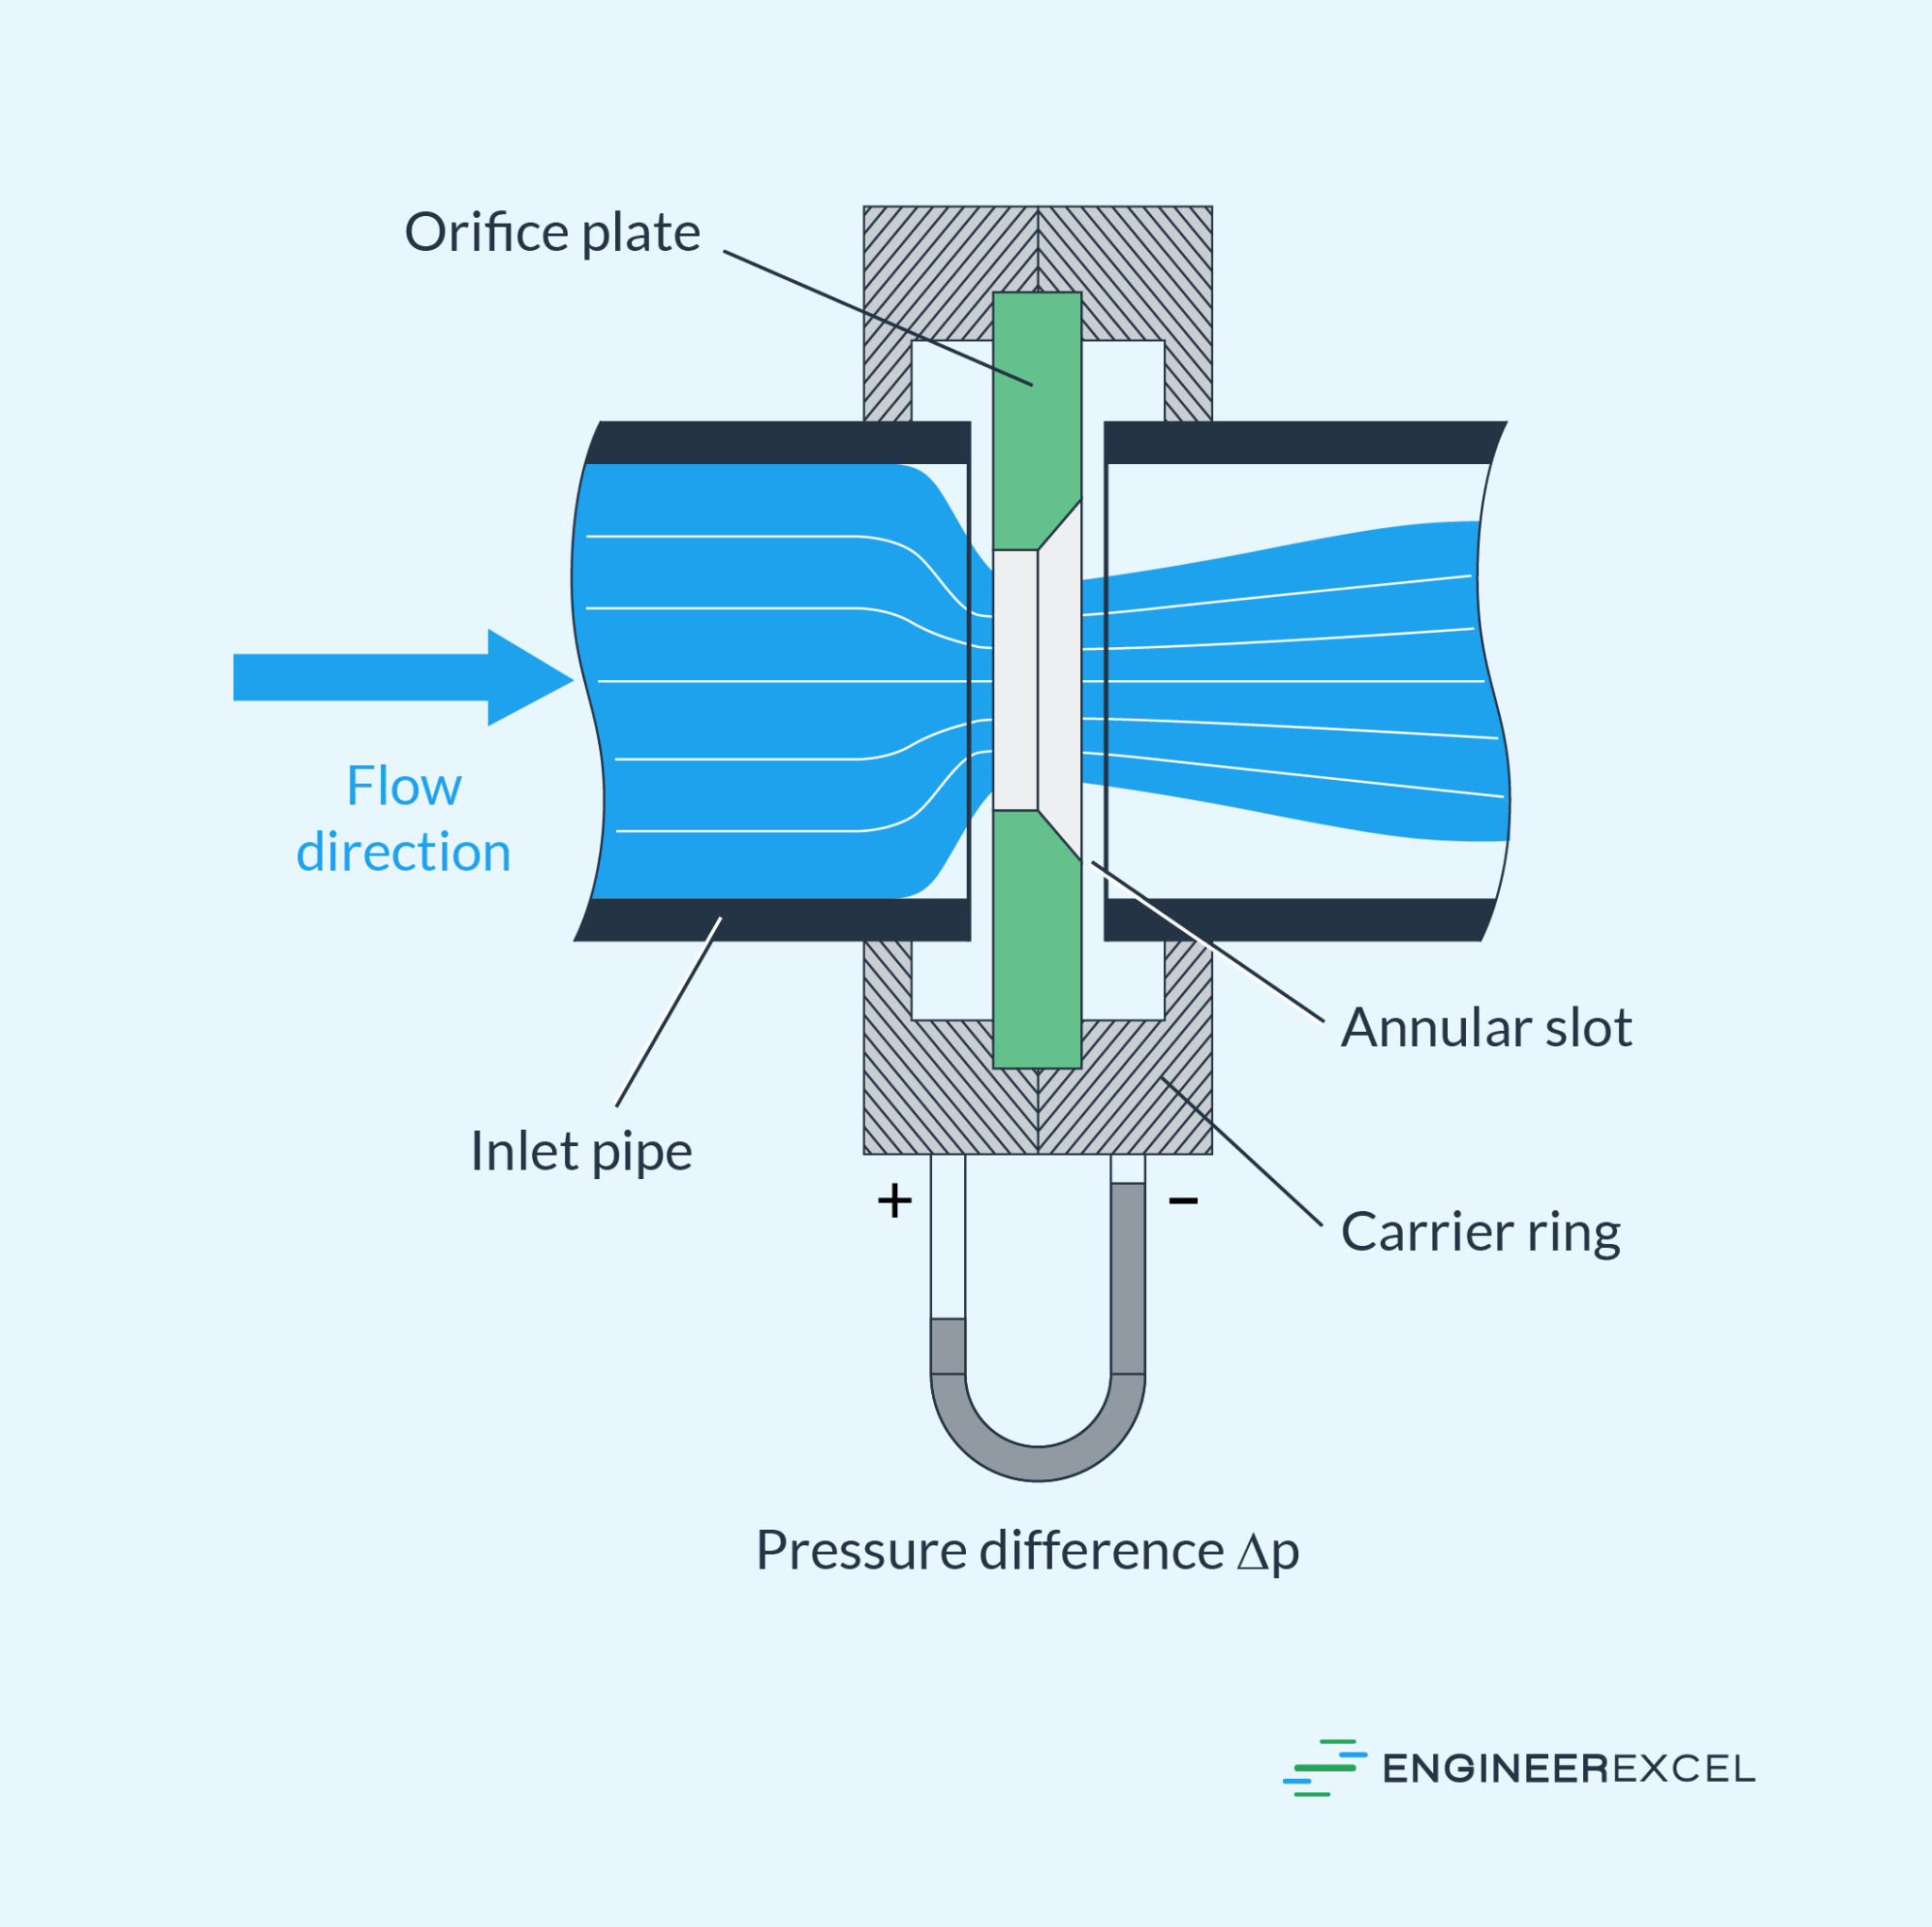
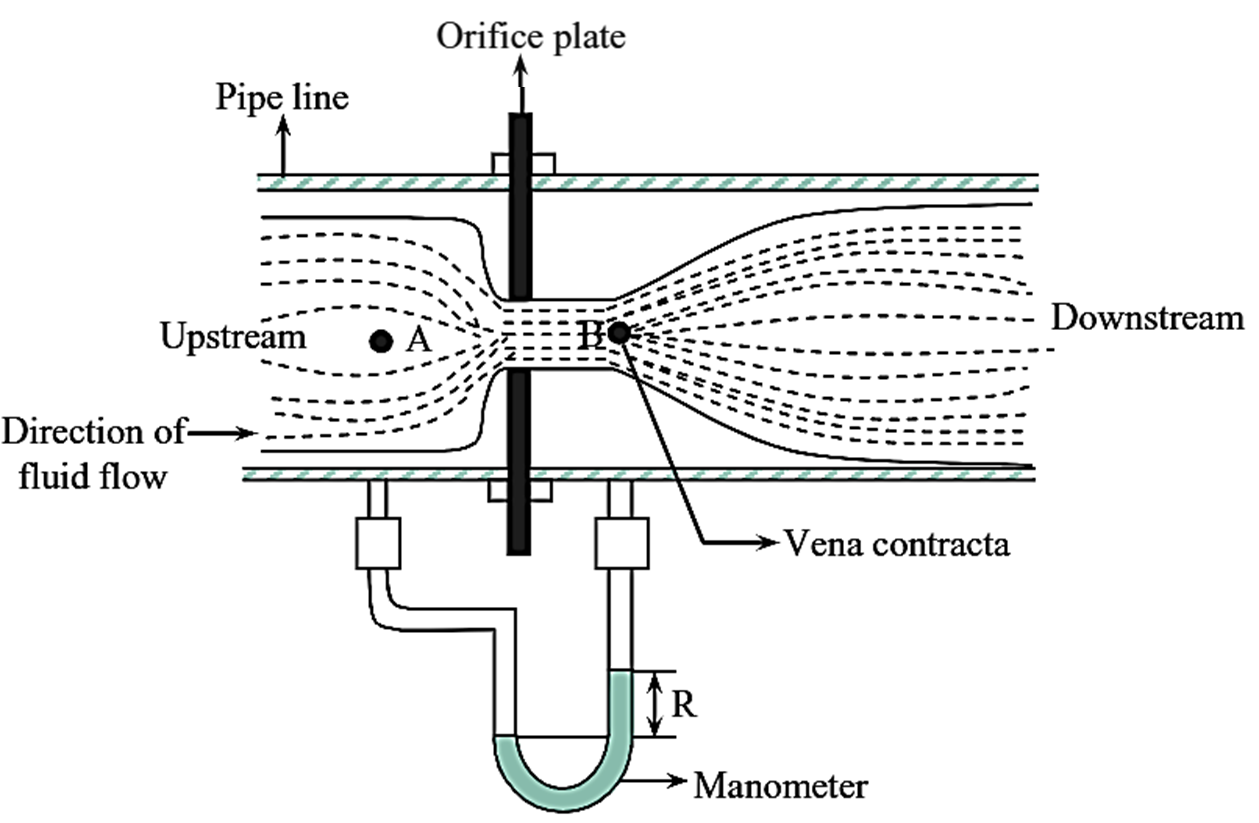
You hang a flat plate with a hole in it inside a pipe and suddenly you have a differential pressure that tells you how much fluid is moving. That is the entire concept. Most people treat orifice plates like they are some kind of precision instrument from day one, but they are really just a piece of metal that creates a predictable restriction. The math behind it is older than modern control systems, and it still holds up when you do it right. An orifice is simply a restriction placed in a flow path to create a measurable pressure drop. In practice, that usually means an orifice plate, which is a thin disk with a circular hole machined into it. You install it between flanges, the fluid accelerates through the hole, and you measure the pressure upstream and downstream. Bernoulli does the rest. The basic equation relates the differential pressure to flow rate, and once you understand that relationship you can troubleshoot the installation or read a gauge without needing a consultant. The hole is called the bore. The plate thickness matters. The tap locations matter. The approach velocity matters. Get any of those wrong and your flow reading will be off, sometimes by a large margin.
The Installation Reality
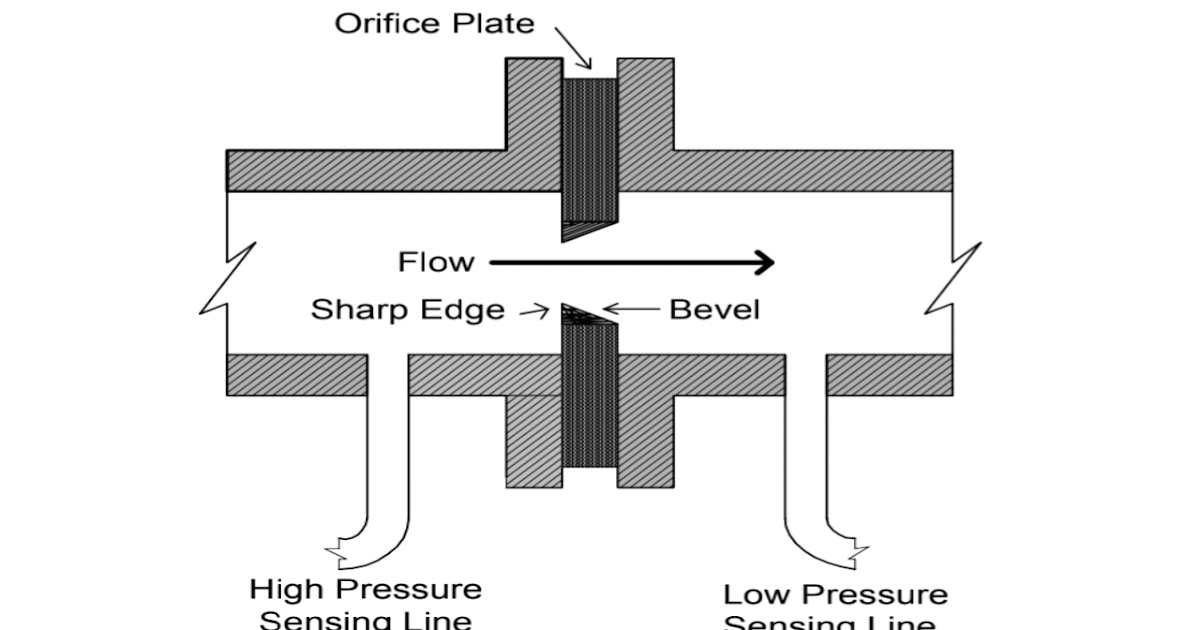
I spent three days once trying to figure out why our steam flow readings were consistently 8 percent low. We had installed the orifice plate backward. The bevel on the downstream edge was meant to point upstream, and when we flipped it the effective discharge coefficient changed in a way that was not obvious from a visual inspection alone. The manual did not mention it clearly. It took a borescope and a reference to ISO 5167 before I realized what happened. That is the kind of thing you learn slowly. Here is how you actually get it right the first time.
Step one: pick the right beta ratio
Beta is the bore diameter divided by the pipe inner diameter. Common values sit between 0.2 and 0.75. A higher beta gives you less permanent pressure loss, which saves pumping energy, but it also reduces the differential pressure signal, making it harder to measure accurately. A lower beta gives you a stronger signal but costs more in permanent loss. I usually aim for a beta around 0.5 for liquid service and let the permanent loss settle where it may. For gas or steam, I tend to go slightly lower to keep the differential in a usable range for the transmitter. You need enough straight pipe upstream and downstream for the flow profile to develop properly. The standard tables from ISO 5167 or AGA Report No. 3 give specific numbers. For a typical orifice plate with flange taps, you want at least 10 to 20 pipe diameters upstream and 5 downstream. If you have a valve or elbow close by, add more. I never cut corners on straight run. Every time I have skipped it, the accuracy went to hell. The sharp edge of the bore faces upstream. The beveled edge faces downstream. The plate must be centered. Use spacers if the manufacturer provides them. Make sure the gaskets do not protrude into the pipe. I have seen gaskets cut wrong and left sticking into the flow stream, and that will distort your reading consistently. Torque the flange bolts in a star pattern so you do not warp the plate.
Get the Full Details

Flange taps are located one inch upstream and one inch downstream from the plate faces. Corner taps are right at the faces. D-D plus half D taps are located one pipe diameter upstream and half a diameter downstream. Each type has different equations. Pick the one your calculation software expects, or your results will be wrong even if everything else is perfect. The basic flow equation for an orifice plate in SI units looks like this: Q = C × Y × (/4) × d² × (2 × P / )
Where Q is volumetric flow, C is the discharge coefficient, Y is the expandability factor, d is the bore diameter, P is the differential pressure, and is the fluid density. The discharge coefficient is not a constant. It changes with Reynolds number, beta ratio, and tap location. The expandability factor matters only for compressible fluids like gas and steam. For liquids, Y equals 1. If you are working in imperial units, the equation gets a unit conversion factor slapped onto the front of it. You can either remember the factor or let a spreadsheet handle it. I let the spreadsheet handle it.
Common Pitfalls
Wear on the bore is a real problem in abrasive service. Sand in oil lines, slurry in mining, catalyst particles in refining. The bore rounds over time and the effective diameter increases. That means your calculated flow will be higher than the actual flow because the meter thinks the hole is smaller than it really is. I recommend inspecting the plate every 12 to 24 months depending on service severity. Micrometer the bore at three points minimum. If the variation is more than 0.001 inches, replace the plate. Erosion is different from wear. Erosion happens fast in high velocity gas service, especially if there are droplets or solids. You will see the upstream edge become sharp again in a bad way. The plate gets pitted. Discard it. Another thing people miss is temperature. The bore diameter changes with temperature. If you calibrated the plate at room temperature and it is running at 400 degrees Fahrenheit, the steel has expanded. For carbon steel, that is roughly 0.01 percent per 100 degrees. Over a large temperature swing, that adds up. Apply thermal expansion correction to the bore diameter before running your calculations. The formula is straightforward.
Pressure tap lines can also cause trouble. If they are not properly vented and drained, you will get pockets of gas in liquid service or condensate in steam service. That gives you a drifting reading. Bleed the lines properly and keep them full of the correct seal fluid.
When An Orifice Plate Is The Wrong Choice
Orifice plates are cheap and simple, but they have limits. They require a relatively high differential pressure to achieve good accuracy, which means permanent pressure loss. In low pressure gas systems, that loss can be significant. If you need turndown better than 3 to 1, an orifice plate struggles. Variable area meters, ultrasonic meters, or magnetic flow meters may serve you better depending on the fluid. For highly viscous liquids, the Reynolds number stays low and the discharge coefficient becomes unstable. You will get scatter in your readings. In that case, consider a venturi tube or an averaging pitot tube instead. They handle low Reynolds number better.
A Quick Reference Table
Here is a rough guide for common services. These are starting points, not final answers. Always run the full calculation with your actual conditions. Liquid service: beta 0.4 to 0.6, straight run 20D upstream and 5D downstream, check Reynolds number is above 10,000 for standard coefficients. Gas service: beta 0.3 to 0.5, straight run 30D upstream and 5D downstream, apply expandability factor, watch for choked flow if the downstream to upstream pressure ratio drops below the critical value.
Steam service: beta 0.3 to 0.5, straight run 20D upstream and 5D downstream, ensure proper condensate pot installation, correct for temperature and pressure changes. Two phase flow: do not use a standard orifice plate without specialized calibration. The readings will be unreliable and you will waste time chasing ghosts.
Where To Get Calculations Done
There are several standard references. ISO 5167 covers orifice plates for liquids, gases, and steam. AGA Report No. 3 is the North American standard for gas measurement. ISA RC20.1 and RC20.2 have useful data too. If you need a quick calculation tool, open source spreadsheets exist, and I have used a few over the years. The key is to verify the assumptions match your installation, not just plug numbers into whatever you find online. For field verification, a simple test is to compare your calculated flow against a known reference, like a calibrated positive displacement meter or a well maintained ultrasonic clamp on meter. If they agree within your expected uncertainty band, your orifice is probably in good shape. If they do not agree, start checking the obvious things first: tap lines, plate orientation, temperature correction, and bore condition.
Final Thoughts
Orifice plates are not fancy. They do not have moving parts. They do not need power. They are simple metal disks that give you a reasonable flow measurement if you respect the installation requirements. Most errors come from poor installation, not from bad math. Take the time to get the straight run, the plate orientation, and the tap configuration right. Inspect the bore periodically. Correct for temperature. Bleed the lines. Do those things and the orifice plate will serve you well for years.