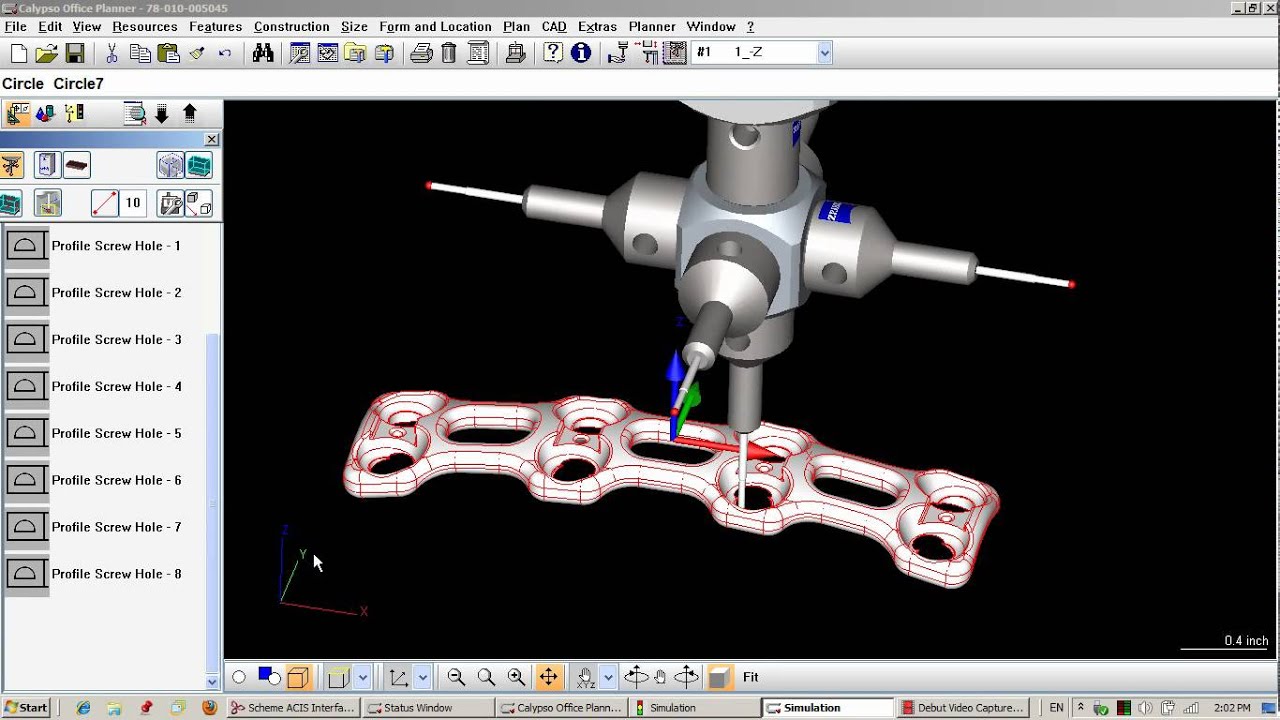
Getting Your Arms Around Zeiss Control Software
The official route for learning Zeiss CMM programming runs through CP-CLANG and DELMIAprism. It is not the easiest CNC language to pick up if you are coming from manual programming or fanuc-style systems. The learning curve has a steep chunk right at the beginning where you deal with vector math and construction geometry, and then it flattens out once you understand how Zeiss structures a program. I signed up for the official training because my shop was standardizing on a Contura with CALYPSO software. The classroom portion lasted two days. It covers basics: running manual measurements, building features, creating alignments, writing simple programs. What the training does not cover is what happens when your part does not cooperate with the algorithm.
What Zeiss Cmm Programming Training Actually Covers
The course material moves through several modules. You start with software navigation and probe calibration. Then you build basic alignments using the 3-2-1 method, which every metrologist knows but rarely understands deeply enough to debug when it fails. After that you move into feature construction, tolerance inspection, and basic program flow control. The advanced day touches on scanning, CAD comparison, and automation setups. The programming language itself is CP-CLANG. It is a high-level language that resembles BASIC. You write commands like ALIGNMENT LEVEL, FIT CYLINDER, and MEASURE FEATURE. The syntax is forgiving but strict about execution order. Run a measurement before you define a fit and the program throws a fit. Literally. Here is a practical detail most people skip: you should always run a self-alignment check after building your primary alignment. The software gives you residual values. If your residuals are above two microns on a part that calls for five, your alignment is holding more uncertainty than you think. The training mentions this in passing. Nobody pays attention until their first audit fails.
A Real Problem That Was Not in the Coursework
Last year we were programming a housing component with a thin flange. The flange was 1.2 millimeters thick and made of cast aluminum. We built a standard alignment using three hit points on the base and two on a bore. Program ran clean on the first article. Second article came in warped about four microns out of flat. The alignment shifted because the software was picking the warped surface as the primary plane reference. Residuals looked fine because the software did not know the part was distorted. The workaround was to use a CAD-based alignment instead of the feature-based 3-2-1. We imported the nominal CAD model, used the BEST FIT alignment command, and let the software iterate across the full surface geometry rather than relying on three discrete points. It took about twenty minutes to restructure the program. The program ran in about 45 seconds per part after that instead of the previous hour because we eliminated manual probing corrections. This is the kind of thing that does not get covered in standard training. You learn the commands. You do not learn when the commands lie to you.
Get the Full Details

What the Training Leaves Out (And What You Should Do About It)
The official courses assume you are working with properly prepared parts on a stable machine in a controlled environment. They do not teach you about thermal drift on a cast iron base during a fifteen-minute program cycle. They do not teach you how to handle a probe that has been bumped twice and you are not sure about the calibration date. They do not cover the situation where your CAD model has a different datum scheme than your engineering drawing. One counter-intuitive thing worth knowing: more probe hits are not always better. On soft materials like aluminum or plastic, pushing the probe into the surface too many times can cause indentation. Five hits are usually sufficient for a cylinder fit. Twelve hits on a soft part will give you a smaller diameter reading than six hits. I learned this the hard way on a polycarbonate optical mount. Our first article looked great. The second article was out of spec because we had probed the same spot repeatedly and created a small divot. We switched to five hits with reduced trigger force and the program stabilized. Another thing beginners miss: the difference between best fit and minimum zone. Best fit minimizes the overall deviation across all points. Minimum zone finds the narrowest band that contains all measured points. For positional tolerance callouts, minimum zone is usually the correct evaluation method according to ASME Y14.5. The default in CALYPSO is often best fit unless you change it. If you ship parts inspected with best fit to a customer who evaluates with minimum zone, your numbers will not match and nobody will believe you.
Alternatives to the Official Route
If you cannot get someone to pay for the two-day workshop, there are other options. Zeiss offers online modules through their learning portal. They are free but lighter than the classroom version. YouTube has walkthroughs of specific functions. The quality varies wildly. Some channels give accurate information. Others give information that will cost you a rejected lot. Third-party trainers exist. They are not affiliated with Zeiss. Their pricing is usually lower and they sometimes cover edge cases the official trainers skip. But you lose the certification that comes with the official route, which matters if your customer requires documented training records. For a shop that runs one CMM occasionally, self-study through the manual and online resources plus a mentor for the first real program may be sufficient. For a production environment running CMMs twenty-four seven, the official training is worth the expense because it gives you a baseline that prevents expensive mistakes.
Practical Steps Before You Touch the Machine
Before enrolling in any training or writing a single line of code, make sure your probe is calibrated within the last forty-eight hours. A stale calibration stone will not tell you anything useful. Check that your granite table is at the proper temperature. Read the room log. If the temperature has swung more than two degrees from the calibration temperature, your measurements carry an unknown variable you cannot program away. Load your CAD model and verify the datum structure matches the drawing. This takes five minutes and prevents three hours of rework later. I have seen programmers build entire alignments on the wrong datum scheme because they assumed the CAD origin matched the engineering drawing and it did not. Write a test program on a known artifact before touching production parts. A certified calibration sphere or gauge block stack will tell you immediately whether your alignment, probing strategy, and evaluation settings are producing valid results. If your program measures a 25mm gauge block as 25.003mm, you have a problem before you ever see a real part. Fix it there. The cost of fixing it in the lab is nothing compared to the cost of fixing it after you have measured fifty production housings and shipped them.

The training gives you the tools. The experience teaches you when not to use them.


