Yield Calculation in Semiconductor Manufacturing
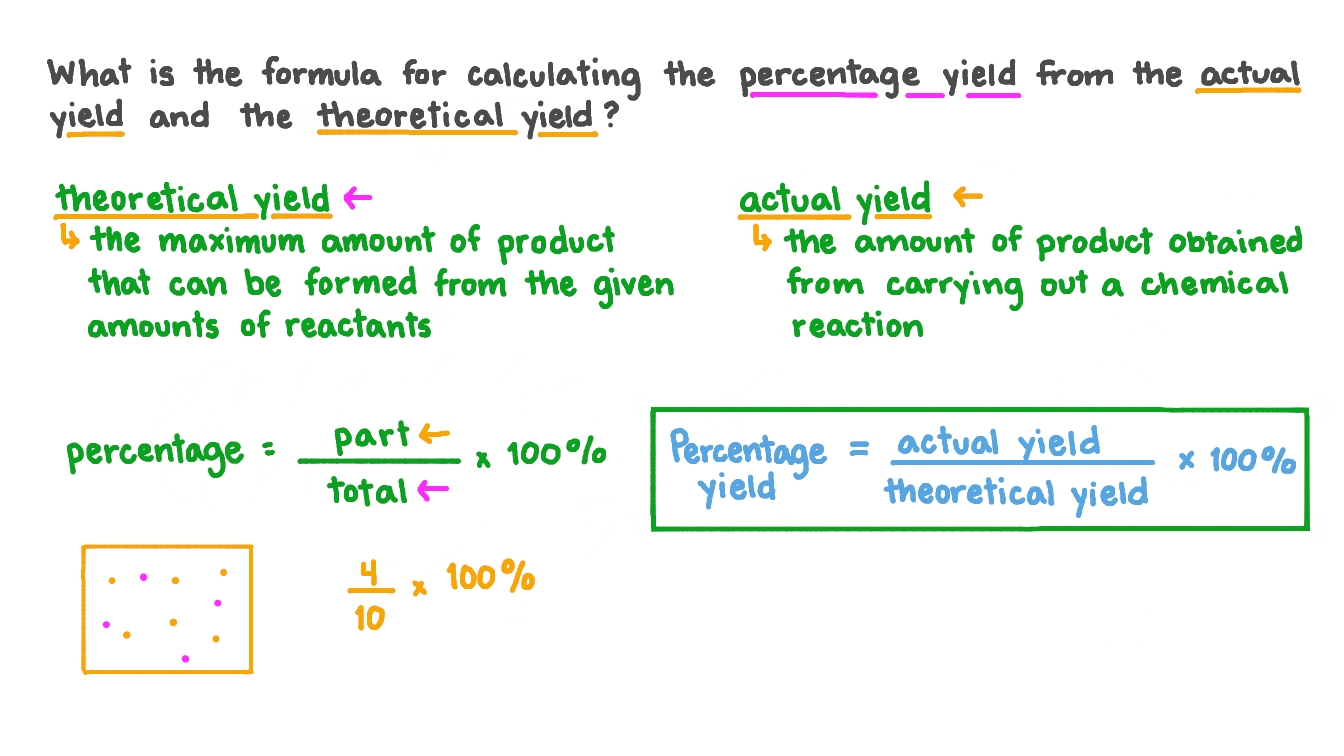
I spent about eight years working fab operations, and the first time I actually had to calculate yield myself, I thought the spreadsheet was broken. It wasn't. The math was simple, but the assumptions hiding behind the numbers made it easy to draw the wrong conclusions. If you're trying to understand How Do I Calculate Yield, start with the definition that actually matters on the floor, not the textbook version. Yield is the percentage of working units you get out compared to how many you put in. In fabs, that usually means good dies on a silicon wafer divided by total dies fabricated. A 65 percent yield on a 300-millimeter wafer with two thousand dies means roughly thirteen hundred chips that meet spec and seven hundred that don't. Simple enough. The part nobody warns you about is that "good" and "bad" aren't always clear-cut.
How Do I Calculate Yield in Practice
The basic integrated yield formula is Y = N_good / N_total. But that's the starting line, not the finish line. Most fabs break it into steps because you need to know which process module is dragging you down. Step yield looks at one operation—like lithography or etch—and measures what fraction of features survive that step. Multiply the step yields together and you get the overall process yield. This is where people usually mess up. They take the final number and assume it tells them where to focus. It doesn't. A 98 percent yield on every single step looks great until you multiply twelve of them together and end up with a 78 percent overall yield, which then makes you panic about whether the equipment is underperforming when really it's just compound loss. I dealt with this exact problem on a DRAM project. The top-level yield was 62 percent, and the engineering team wanted to tear down the photoresist module because it showed the lowest individual step yield at 94 percent. When I dug into the data, the photoresist was fine. The real killer was a thin-film deposition step sitting at 99.1 percent that most people dismissed because it looked good in isolation. At scale, that 0.9 percent loss compounded across thousands of layers and accounted for nearly forty percent of the total yield gap. We reworked the chamber maintenance schedule, bumped that step to 99.6 percent, and the overall yield jumped to about 74 percent without touching the lithography at all.
Defect Density and the Poisson Model
When you're not just measuring pass or fail but trying to predict what yield will look like before you run the line, you use defect density models. The most common is the Poisson yield model: Y = e^(-A × D), where A is the active die area and D is the defect density per unit area. It's imperfect but it gets you in the right neighborhood fast. There's a more accurate version called the Murphy yield model that factors in wafer edge effects and cluster distribution: Y = (3 / (×D × A)^3) × ((×D × A)^2 + 2 ×D × A + 2) × (1 - e^(-×D × A)). It sounds worse than it is. You plug in your measured defect density and your die size, and it gives you a prediction that's usually within a few percentage points of actual results for mature processes. The counter-intuitive thing here is that smaller dies don't always mean better yield in the way people assume. Yes, a smaller die has less area exposed to defects, which is true. But if you make the die too small, the non-active areas—scribe lines, test structures, wiring channels—start eating up a meaningful chunk of the wafer. The sweet spot is usually where the die area is large enough that overhead percentages stay low but small enough that random defects don't kill half your chips. I've seen teams optimize for pure yield and accidentally increase their cost per good die because they were producing too many tiny, low-value chips instead of focusing on the area where the margin was actually better.
Get the Full Details

Parametric vs. Functional Yield
You need to separate these two. Functional yield is binary: the chip works or it doesn't. Parametric yield is the percentage of working chips that meet all their performance specifications—clock speed, power draw, signal integrity, whatever the design requires. A chip can pass functional tests and still fail parametric ones, which means it ships as a lower-bin product instead of getting scrapped entirely. In my experience, parametric yield is where the real money lives. If your functional yield is 80 percent but your parametric yield is only 55 percent, you're not losing 45 percent of your production. You're losing 25 percent to scrap and giving yourself a margin problem on the remaining 55 percent. Binning strategies—sorting chips into performance grades—can recover a lot of that. An Intel processor from a few years ago was literally the same die as a cheaper model, just tuned and tested at different frequencies. The yield math didn't change, but the revenue per wafer did, because the higher bins commanded higher prices.
What Breaks Yield Calculations
Yield numbers lie. They're only as honest as your measurement system. Here are the most common ways that happens: Inline metrology gaps. If you're measuring defects on sample wafers instead of every wafer, your yield prediction is a guess. Automated optical inspection helps, but inspection tools miss sub-micron defects on certain materials, especially in advanced nodes. I once saw a fab report 99.3 percent yield and then ship a product that failed in the field at a 12 percent rate. The inline tools weren't catching the defect mode because it only manifested after thermal cycling, not at room temperature where the inspections happened. Test coverage is never complete. Every test program has blind spots. Stuck-at tests catch obvious faults but miss timing violations. Built-in self-test structures help, but they add area overhead that reduces your functional die count. There's a tradeoff between how much test coverage you buy and how much yield you lose to test structures eating into active area. The industry standard sits somewhere around 95 to 98 percent fault coverage for most commercial products, which means you're accepting a small but real risk of escapes.
Lot-to-lot variation. Yield calculated on a single lot tells you nothing about process stability. I've seen fabs celebrate a 91 percent yield on one run and then get crushed to 73 percent the next week because the incoming silicont was a different supplier lot with slightly different oxygen content. The yield calculation was correct for each lot individually, but the comparison between lots revealed a material compatibility issue that nobody had flagged.

Yield Ramp Curve Basics
New product introduction doesn't start at target yield. It starts low—sometimes 20 to 40 percent for complex nodes—and ramps as you debug. The typical curve follows a learning rate pattern where each doubling of cumulative production improves yield by a fixed percentage. For mature CMOS processes, that learning rate is often 10 to 15 percent. For cutting-edge nodes with new materials or architectural changes, it can be 20 to 30 percent because there's more unknown unknowns. If you're forecasting production timelines, don't assume linear improvement. The first percentage points are the easiest to gain. Going from 40 to 60 percent might take three weeks. Going from 80 to 90 percent could take three months. The last ten percent is usually fighting fundamental physical limits or supplier constraints that you can't accelerate without massive capital investment.
Tools and Spreadsheets
Most fabs use custom Excel models or proprietary software like Synopsys' YieldStar or KLA's SPIRE platform. If you're doing this academically or for a startup without fab access, you can build a reasonable approximation in a spreadsheet. You'll need defect density data from your process documentation, die area in square millimeters, and the step yields for each major process module. The Poisson model alone gets you reasonably close for preliminary estimates. Once you're past that stage, you'll want to layer in the Murphy correction or move to a Monte Carlo simulation if your defect distribution isn't uniform. There are open-source yield analysis scripts available on GitHub from a few university research groups. They're not production-grade but they're useful for understanding the mechanics. I found the one from MIT's microelectronics lab particularly clean for learning purposes. Search for "yield analysis python" and you'll turn up a handful of implementations.
When Yield Math Doesn't Apply
I should be clear about where this framework breaks down. Yield models assume defects are random and independent. That's not always true. Clustered defects from contamination events, systematic defects from alignment errors, or wear-out patterns from tool degradation all violate the Poisson assumption. When you have significant clustering, the Murphy model gets closer but still underestimates losses. In those cases, wafer map analysis—looking at the spatial distribution of bad dies—tells you more than any formula. A defect cluster in one corner of the wafer points to a mechanical issue. A ring pattern around the edge suggests thermal gradient problems. A center-heavy distribution often means something in the deposition or etch tool is degrading. Also, yield calculations don't account for reliability. A chip can pass every yield test and still fail after eighteen months in the field due to electromigration, oxide breakdown, or packaging stress. Reliability screening—burn-in testing, accelerated life testing—catches some of these, but not all. That's why automotive and medical chip specs have different yield requirements than consumer electronics. The yield floor is higher because the cost of field failure is dramatically higher, even if the probability of failure is the same. If you're working with foundry partners instead of your own fab, yield data is often treated as proprietary and you'll get aggregated numbers rather than detailed defect maps. Ask for it anyway. The more granular the data, the faster you can solve problems, and most foundries will share it if you have a legitimate quality concern on an active tapeout.


