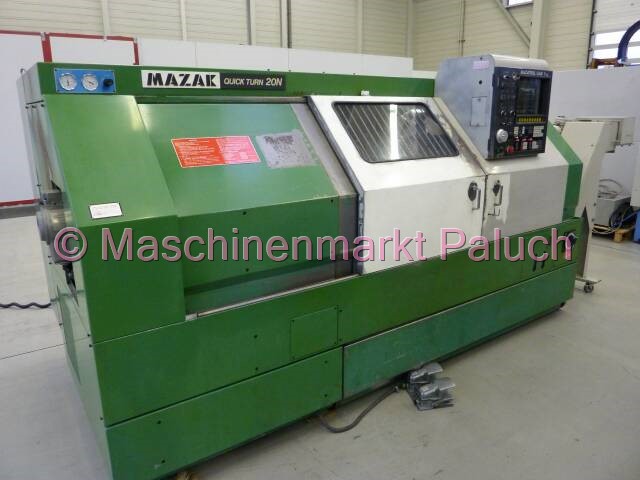
CNC Lathe Manuals Are Harder To Find Than They Should Be
The Mazak Quick Turn 20 T1 was a solid production lathe from the late 1980s through the 1990s. It ran on Mazak's earlier dual-cursor or early MIL-style control systems depending on the exact configuration and year of build. The manual you need covers the machine frame, turret, tailstock, coolant system, and the control interface. You won't find a single PDF that has everything in one neat package anymore. Mazak stopped distributing physical manuals years ago and pulled most of the old ones from their website. That means hunting is part of the job now. The best place to start is the Mazak corporation website's support or archive section, though their older documentation portal has been inconsistent over the years. You can usually locate a service manual or a parts catalog by entering your serial number. The serial number plate is on the right-side rear panel of the machine, behind the chip guard. Write it down before you do anything else. Mazak's service department will sometimes email you a PDF directly if you request it with your serial number and machine model. It takes a few days and you have to be polite but persistent on the phone. Your second option is machine tool manual repositories. Sites like CNC-Manuals.info, ManualsLib, and various CNC-focused forums occasionally have uploaded copies. Search for "Mazak Quick Turn 20 T1 manual PDF" and cross-reference the file dates and page counts. A complete operator and maintenance manual for this machine should run somewhere between 150 and 300 pages depending on whether it includes the electrical schematic section. If a file is only 40 pages, it's just the quick reference card, not the full thing.
A word of caution on downloaded manuals: many of the PDFs floating around are scanned images, not searchable text. That makes them useless when you're trying to Ctrl-F a specific alarm code at 2 AM. If you can, find a text-based version or plan to type out the sections you need most often into a personal document. I keep a Google Doc with just the alarm codes, lubrication schedule, and the turret indexing procedure copied from whatever manual I can find.
What The Manual Actually Covers
Every Mazak Quick Turn 20 T1 manual is split into roughly four sections. The first is the operator manual, which walks you through powering up, homing, loading programs, and handling basic alarms. The second is the maintenance manual, which covers daily, weekly, and monthly checks plus the lubrication points. The third is the electrical schematic, and the fourth is the parts list with exploded views. You may not get all four sections from any single source. The electrical drawings are the hardest to find and the most valuable when something goes wrong. The control interface on the 20 T1 is a Mazak Dual Cursor system in most configurations. This means you have two program cursors and one address cursor, and you navigate between them using the SELECT key and the coordinate selection keys. If you've only worked on Fanuc or Siemens controls, this takes some getting used to. The machine will hold three active programs simultaneously, and switching between them is a multi-step process. The manual explains it, but watching someone do it once is worth more than reading the paragraph three times. One detail the operator manual doesn't stress enough is the backplot function. The 20 T1 can simulate a program before you run it, and using that feature prevents a lot of costly mistakes. I learned this the hard way. Early in my time working on these machines, I loaded a program that had a subtle mistake in the turret indexing block. The tool didn't retract far enough before the turret rotated, and it knocked the nose of tool 4 against the collet cap. The control didn't alarm because the block looked legal to the interpreter. The backplot would have shown the tool path colliding with the workholding before I ever powered on the axis. Now I backplot every new program, even simple ones.
Get the Full Details

Common Problems The Manual Won't Warn You About
The lubrication system on the Quick Turn 20 T1 uses a fixed-volume metering block. Each lubrication point gets the same amount of oil per cycle. Over time, the lines to the tailstock and the rear guide ways clog with old grease and metal fines. The panel will show normal lubrication activity because the pump is cycling, but those points aren't actually getting oil. I've seen two spindles wear out prematurely on machines where the operator checked the gauge and assumed everything was fine because the indicator was moving. The fix is to disconnect each line at the metering block and confirm flow individually. It takes about 45 minutes and prevents a ten thousand dollar mistake. The turret indexing mechanism is another area where the manual is adequate but not thorough. The 20 T1 uses a cam-driven indexing system with a stepper motor and a mechanical lock. The common failure is the indexing cam wearing a flat spot, which causes the turret to settle slightly off position. The control compensates through software offset for a while, then you start seeing chatter marks on finished diameters and occasional tool breakage because the tool nose is sitting a fraction too high or too low relative to the workpiece center. The manual tells you to check the cam bolts and lubricate the indexing mechanism. It does not tell you to measure the turret stop pin wear with a micrometer and compare it to the specification, which is usually around 0.002 inches of allowable clearance. If you're past that, the cam isn't the only thing wearing. Another edge case that comes up regularly is the spindle encoder reference mark. The Quick Turn 20 T1 uses an absolute encoder for spindle positioning, and the reference mark needs to be aligned during setup. If you replace the encoder or disconnect the battery that holds the absolute position, you have to realign the mark. The manual describes the procedure, but the visual reference point on the encoder coupling is easy to miss if you're working in poor light. I tape a small piece of white electrical tape to the coupling before I start, then use a flashlight to line it up with the mark on the housing. Without that tape, I've missed the reference by a couple of degrees and spent an hour wondering why the threading was out of pitch.
Working With The Electrical Schematics
If you don't have the electrical section of the manual, your machine troubleshooting becomes guesswork. Mazak's schematics use a mix of JIC and custom symbols, and the numbering system tracks every relay, solenoid, and sensor by its circuit position. A typical fault diagnosis might involve tracing a 24VDC signal from the control board through a series of relays to the turret clamp solenoid. The schematic tells you the expected voltage at each test point. Without it, you're just probing wires and hoping. The control board layout is mounted on the left interior panel behind the electrical door. There are fuses for each major circuit, and the manual lists the amperage and location. I always keep a handful of the correct spare fuses in a labeled container near the machine. The spindle drive fuse, in particular, blows periodically during heavy cut cycles when the chip load varies suddenly. It's a $15 part and replacing it takes three minutes. Not having it on hand means a half-hour call to order one while the machine sits idle.
Programming Notes Specific To This Machine
The 20 T1 supports Mazak's older M-code programming format, which includes G-code and a set of proprietary macros. If you're writing programs from scratch, the manual's programming section covers the canned cycles for facing, turning, grooving, and threading. The threading cycle is particularly finicky because the spindle encoder must be correctly aligned and the pitch parameter has to match the actual gear ratio in the spindlebox. Get that wrong and your threads will be consistently off, and the machine won't alarm because the math in the control is correct even if the mechanical linkage isn't. For most shops running these machines, the program library is already established and you're modifying existing code rather than writing new routines. The manual includes a section on program editing, recall, and offset entry that's straightforward if you follow it step by step. Don't skip the tool offset entry procedure. Entering the wear offset backwards is a common mistake that causes the tool to dig in instead of taking a light cut. The display shows the offset value, but it doesn't indicate whether you're adding or subtracting from the current position unless you watch the direction arrow on the screen.

What To Do When You Can't Find The Manual
If your copy is lost or damaged, try the Mazak dealer network. Some regional dealers still have physical archives and will scan pages for you. CNC repair shops that specialize in vintage Mazak equipment sometimes keep complete sets. A few forum members have mentioned success reaching out to former Mazak service technicians through LinkedIn or industry groups. Those people often have personal copies and will share sections if you ask nicely. As a last resort, you can photograph the pages of a colleague's manual and compile them yourself. It's not elegant, but it gets you the information you need. I've done it twice. The resulting document isn't pretty, but it's searchable if you run it through an OCR tool afterward, and having it on a USB drive in the machine cabinet is better than nothing when the spindle alarm goes off at 6 PM on a Friday.