Understanding Freezing Point From the Bench
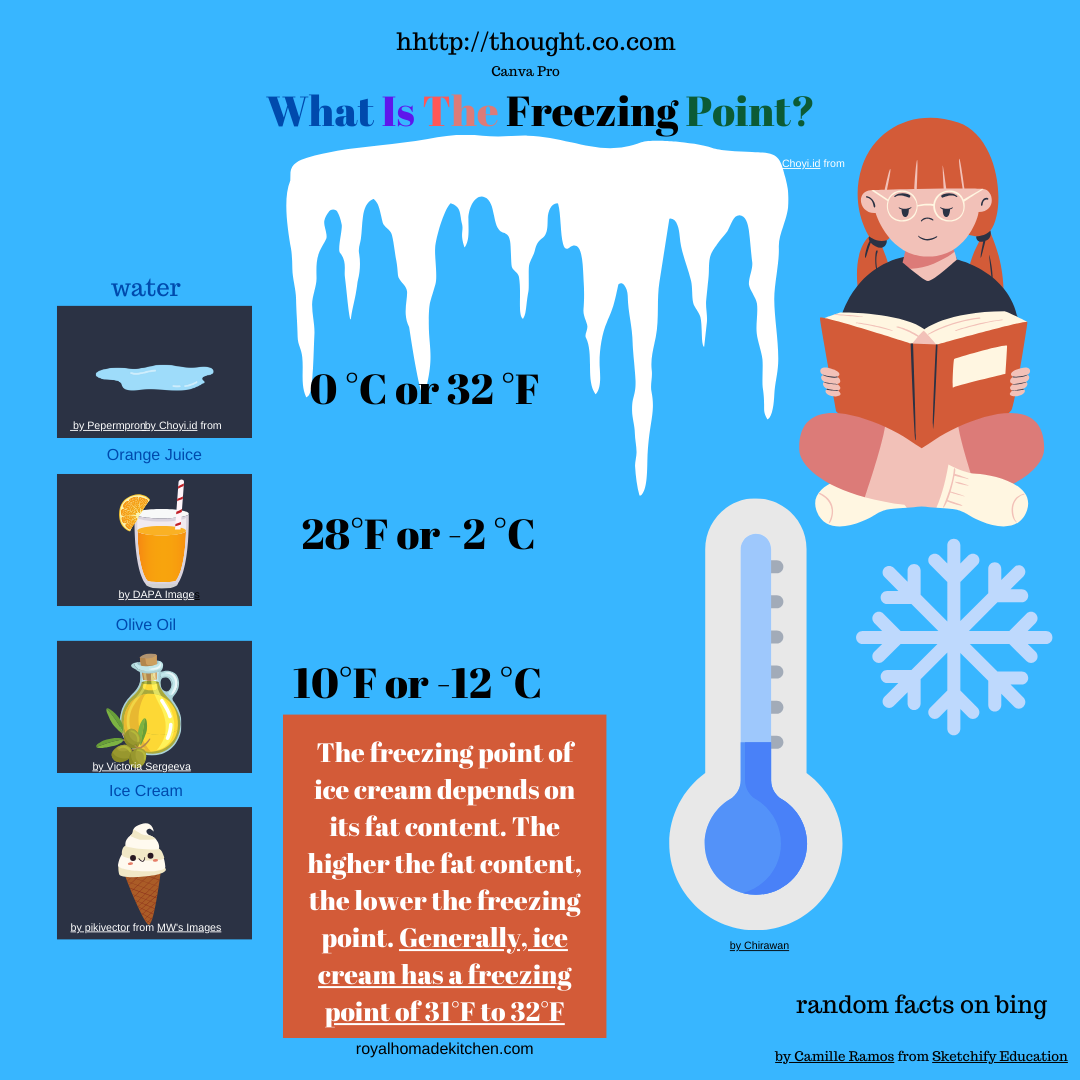
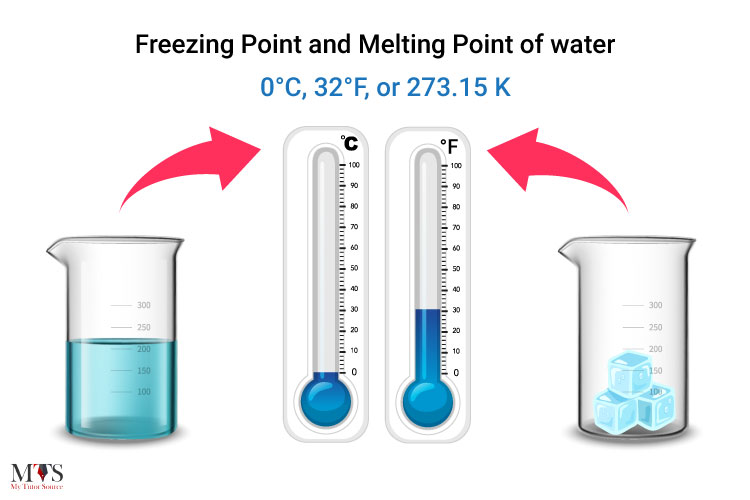
The freezing point is the temperature at which a liquid turns into a solid under normal atmospheric pressure. It sounds simple, but getting it right in a lab or production setting requires more attention than most people give it. The value isn't fixed for every sample of the same substance. Impurities shift it. Pressure changes it slightly. The cooling rate matters more than you'd think. I learned that the hard way when I spent three days troubleshooting why two batches of the same polymer looked identical but behaved completely differently during molding. At the molecular level, freezing happens when molecules slow down enough for intermolecular forces to lock them into a structured arrangement. For pure water, that's 0°C at one atmosphere. For most industrial purposes, though, you're rarely dealing with pure anything. Antifreeze in a car radiator, chocolate tempering, pharmaceutical crystallization, cryogenic shipping — they all depend on knowing the exact freezing behavior of your material. Here's the part nobody tells beginners: the freezing point you measure on a cheap digital thermometer while stirring a beaker in a home lab is often wrong by a few degrees, and that error cascades into real problems downstream. I ran into this when a client insisted their eutectic mixture was "off-spec" because it wouldn't solidify at the temperature listed on the datasheet. The datasheet assumed equilibrium conditions. Their process cooled the material at roughly 5°C per minute. The observed freezing point was about 3.2°C lower than expected due to supercooling — the liquid stayed fluid past its theoretical transition temperature because nucleation sites weren't available fast enough. Once we slowed the cooling rate to 0.5°C per minute and seeded the mixture, the readings aligned with the spec sheet.
Supercooling is the biggest practical trap with freezing point measurement. A liquid can drop well below its equilibrium freezing point without actually solidifying if it lacks nucleation points. This isn't theoretical — I've seen technicians record temperatures 8 to 10 degrees below the actual freezing point and conclude their sample was contaminated when it was perfectly fine. The workaround is straightforward: use a mechanical stirrer running at low speed, introduce a small seed crystal of the same material, or run multiple cool-down cycles and look for the thermal plateau on your temperature-time graph. That flat region where temperature holds steady while the phase change happens is your real freezing point. The lowest point before it recovers is just supercooling artifact.
How to Measure Freezing Point Correctly
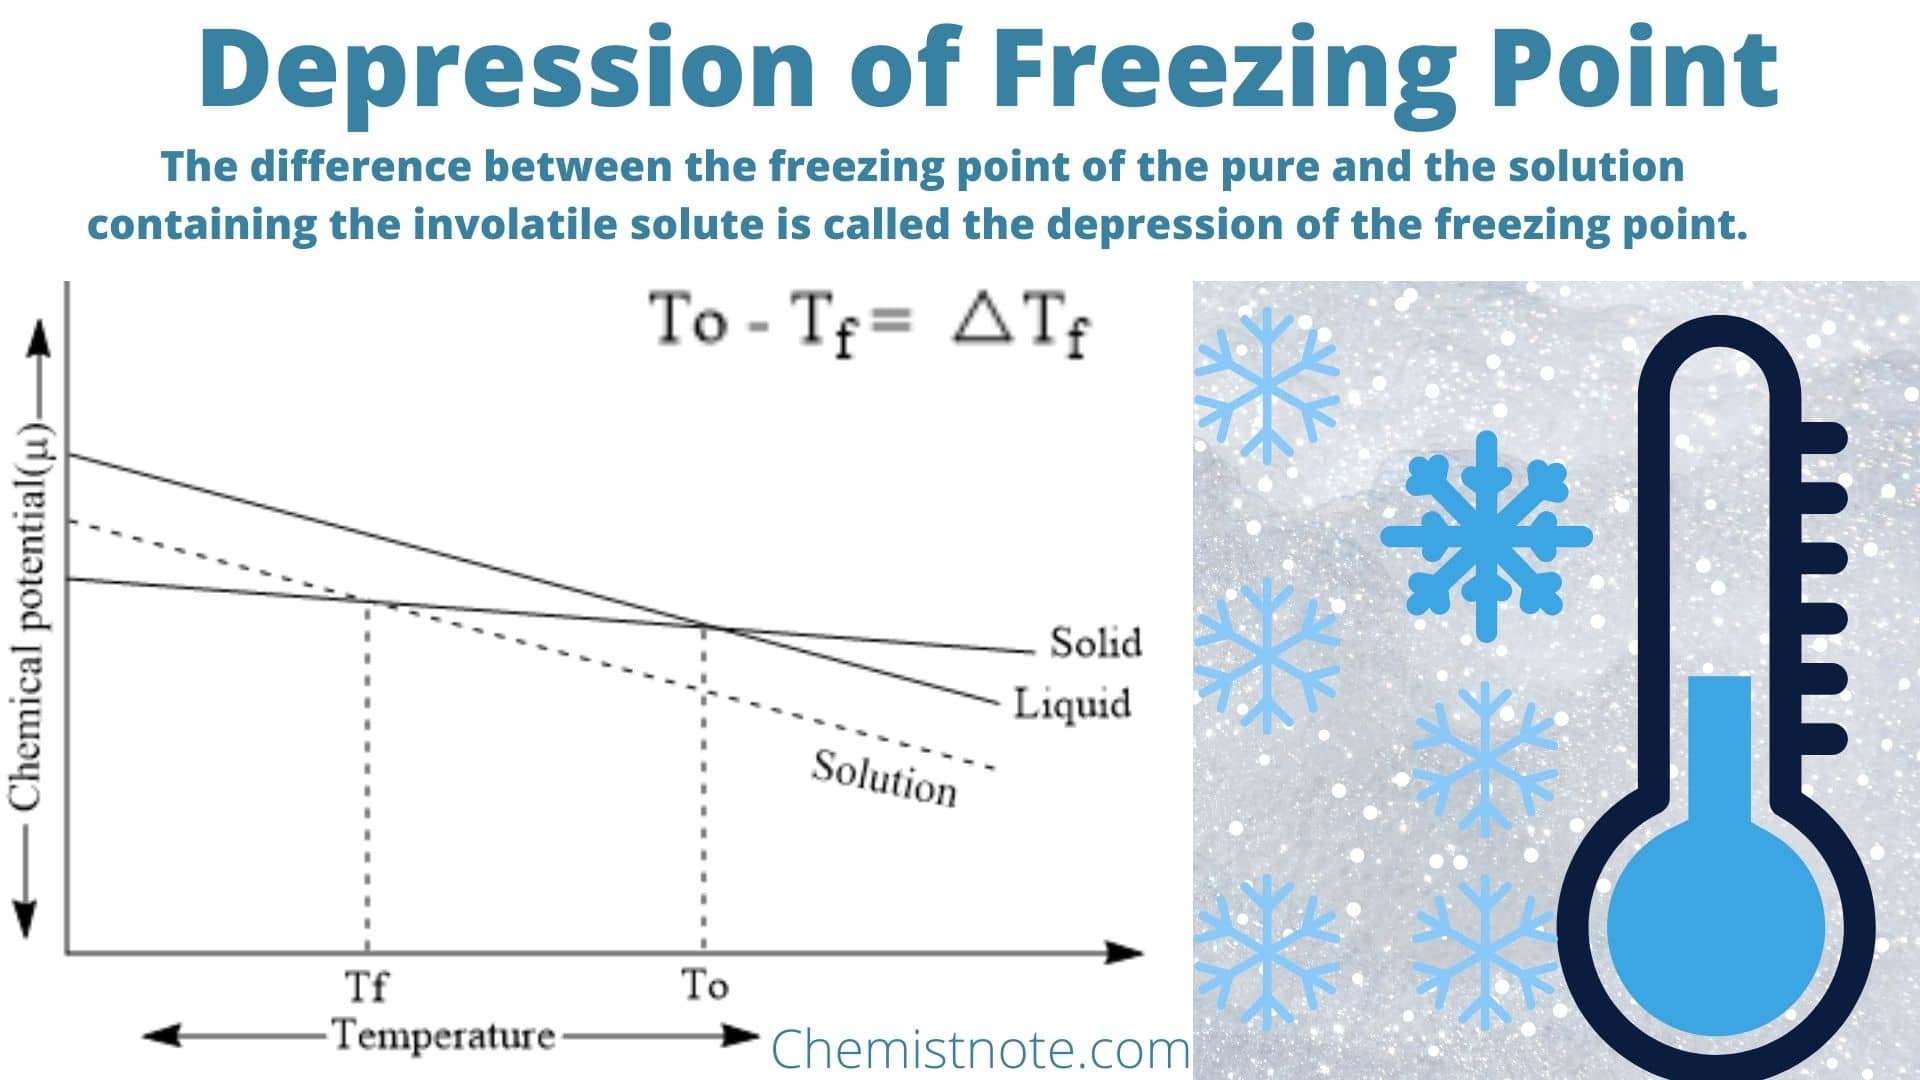
You need a temperature-controlled bath or a programmable cooling block, a calibrated thermometer or thermocouple with at least 0.1°C resolution, a sample container that promotes uniform heat transfer, and something to agitate the sample gently. The sample should be pure enough that impurities don't depress the reading beyond your acceptable tolerance, or you need to account for that depression mathematically using colligative properties. For routine work with organic liquids, the capillary tube method is still valid and widely used in pharmacopeial standards. You seal a small amount of sample in a thin glass tube, insert a thermometer, and lower the whole assembly into a cooling bath. Watch for the first sign of solid formation and record the temperature. The bath temperature should drop no faster than 1°C per minute near the expected freezing point. Anything faster and you're measuring undercooling, not the actual transition. If you're working with mixtures or solutions, the approach changes. You're looking for the liquidus temperature — the point where the first crystal appears as you cool. That's different from the solidus temperature where the last bit of liquid freezes. The gap between those two points is the freezing range, and for alloys and polymer blends, that range determines everything about cast quality and mechanical properties. A narrow range usually means better flow and fewer defects. A wide range means you're dealing with segregation and potentially weak spots in the final product.
Get the Full Details
One detail that saves a lot of headaches: make sure your thermometer or thermocouple is in direct contact with the sample, not just measuring the bath temperature. I once had a setup where the probe was reading the oil bath surrounding a glass vial. The bath was 2°C colder than the sample inside because of thermal resistance through the glass and the still air gap. We wasted a full day adjusting process parameters based on bad data before someone noticed the probe placement. Put the sensor inside the sample container whenever possible. If you can't, calibrate for the thermal lag and document it.
Common Misconceptions and Where Things Break Down
The first misconception is that freezing point equals melting point. For a pure crystalline substance under equilibrium conditions, they're the same temperature. But in practice, especially with impure or amorphous materials, the observed transition on heating and on cooling don't match. Hysteresis is real. A sample might melt at 72°C but freeze at 68°C on the way down. If you're spec-ing a process around a single number, you need to specify which direction you mean. The second misconception is that freezing point is an intrinsic constant you can look up and trust. Tables give values for pure substances at standard pressure, but your actual material has additives, solvents, moisture content variations, and possibly degradation products from previous handling. A pharmaceutical raw material lot that's 0.5% water off from spec can shift the freezing point enough to throw off a crystallization step. Check your material certificate of analysis before assuming the literature value applies to your batch. There are also scenarios where freezing point measurement simply doesn't work well enough. Amorphous materials like glasses and some polymers don't have a sharp freezing point — they undergo a glass transition over a temperature range instead. Differential scanning calorimetry can detect the transition, but calling it a "freezing point" is misleading. Similarly, materials that decompose before they freeze can't be measured by conventional methods. In those cases, you're better off using rheological testing to find the point where viscosity spikes dramatically, or switching to DSC if your lab has the equipment.
Pressure is another factor that gets ignored until it causes problems. The freezing point of most substances increases with pressure because the solid phase is denser. Water is the notable exception — ice is less dense than liquid water, so increased pressure actually lowers the freezing point. That's why ice skating works, or at least, that's the simplified explanation. The real mechanism involves surface melting, but the pressure-dependence point stands. If your process operates at elevated or reduced pressure, the standard atmospheric freezing point value is wrong for your conditions.
When You Should Skip Freezing Point Testing Altogether
If you're doing quality control on a commodity chemical with a well-characterized, stable formulation, freezing point measurement might be overkill. A density check or refractive index test could verify identity faster and with less variability. Freezing point is most useful when you're dealing with novel formulations, suspecting contamination, or troubleshooting a phase behavior issue. Don't use it as a routine pass/fail gate for something you already understand well. The technique introduces more variance than it resolves in those cases. The equipment also matters. A $40 USB thermocouple from an online marketplace won't give you repeatable results within 0.5°C unless you calibrate it against ice water and boiling water before every session. A proper platinum resistance thermometer or a calibrated thermistor system costs significantly more but holds its accuracy over time. If you're going to invest in this kind of testing, get equipment that justifies the investment. Cheap sensors drift, and drift is invisible until your product fails a customer spec.