What Happens When You Pull Something Until It Breaks
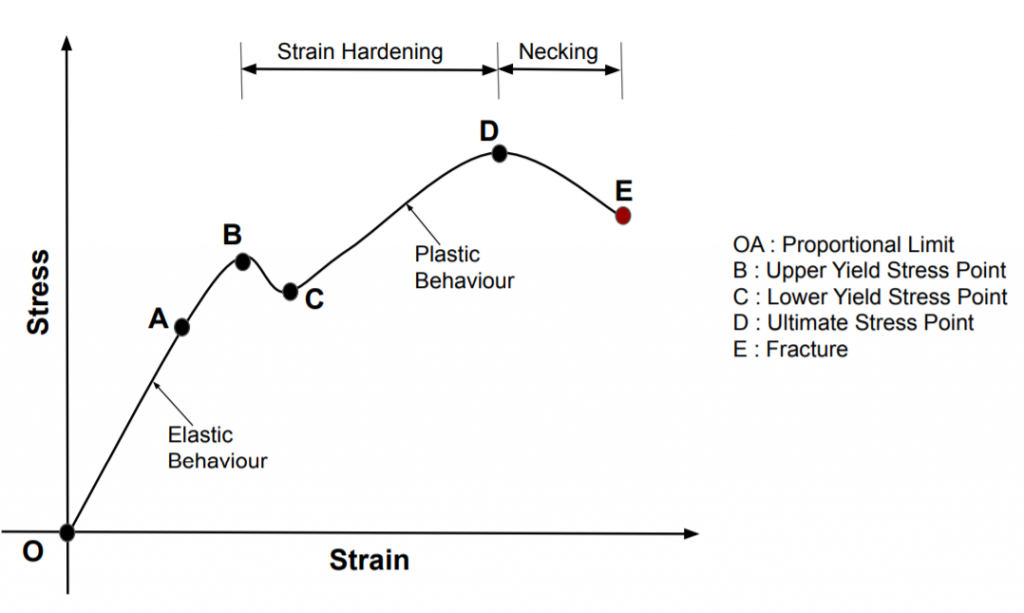
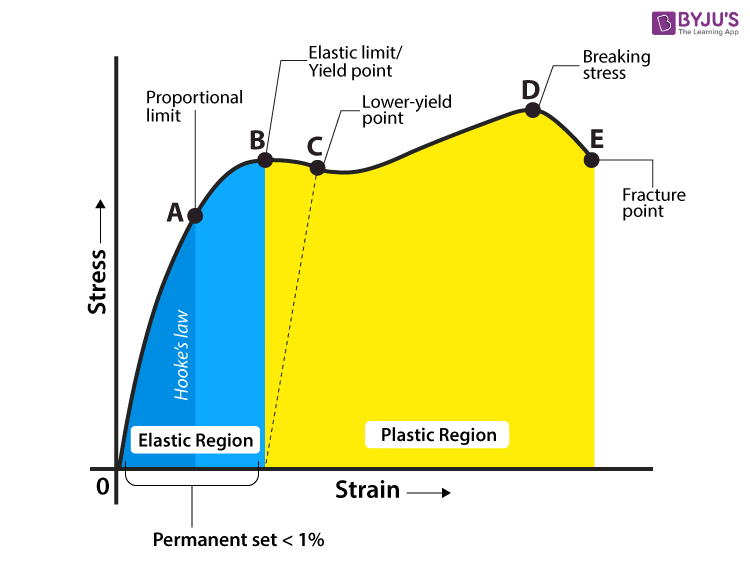
The Stress And Strain Curve is just a graph. You take a specimen—usually a dumb metal dog-bone shape—and clamp it into a testing machine. The machine pulls. It measures how much force you're applying and how much the thing stretches. You plot those two numbers against each other and you get a line. That line tells you everything about the material: how stiff it is, when it yields, how much it can stretch before it necks down and finally snaps. In practice, I've run this curve on everything from structural steel to aluminum extrusions to some weird titanium alloy that someone's company spent $40,000 developing. Each one tells a different story. The curve doesn't lie, but it doesn't volunteer every truth either. You have to know what to look for.
How to Build One From Scratch
Start with a tensile test. You need a universal testing machine—an Instron is the gold standard, but any machine with load cell and extensometer capability works. The extensometer is the critical part. Don't skip it and use crosshead displacement instead. Crosshead displacement includes the compliance of your entire setup—the grips, the load train, the machine frame bending microscopically. For the elastic region, that error alone can shift your modulus calculation by 5 to 15 percent. Extensometers clip directly onto the specimen and measure only the gauge length. That's the difference between a number you can trust and a number that looks reasonable. Prepare the specimen per ASTM E8 or ISO 6892. Standard round bar at 12.5mm diameter with a 50mm gauge length is the usual default. The fillet radii at the transition to the grip section matter more than people realize. Sharp transitions create stress concentrations that can initiate premature failure in the grip zone instead of the gauge length. That ruins the test because you can't properly characterize yielding or necking if the specimen never actually reaches uniform plastic deformation. Set the strain rate. This is where most people mess up. ASTM E8 specifies a stress rate of 1 to 10 MPa/s in the elastic region and a strain rate of 0.0005 to 0.0025/s in the plastic region. For low-carbon steel at room temperature, hitting that strain rate means pulling at roughly 0.5 to 2.5 mm/min depending on your gauge length. Go too fast and you'll overestimate yield strength by 5 to 10 percent due to strain-rate hardening. Go too slow and temperature effects start creeping in. There's a narrow operating band and you should respect it.
Record the data at a sufficient sampling rate. 10 Hz minimum. I'd recommend 50 Hz or higher if your machine supports it. The yield point for low-carbon steel can be extremely sharp—sometimes a sudden drop of 10 to 20 percent in load over a few thousandths of strain. At 10 Hz, you might miss the peak entirely and your 0.2% offset yield calculation will be wrong. At 50 Hz, you capture the Luders band propagation and you get an accurate upper and lower yield point.
Get the Full Details

Reading the Curve—The Parts That Actually Matter
The first thing on the curve is the elastic region. It's linear, mostly. The slope is Young's modulus—stiffness. Steel sits around 200 GPa, aluminum around 70 GPa. If your measured modulus is 20 percent off the textbook value, something is wrong with your measurement setup, not the material. Check the extensometer calibration, check that the specimen dimensions are correct, check that you're measuring in the gauge length and not somewhere closer to the grip where strain distribution is already non-uniform. Then comes yield. For low-carbon steel, you see a distinct upper yield point followed by a lower yield point and a flat plateau. The Luders bands form at the yield point and propagate along the gauge length. You can literally watch it happen on a large specimen—streaks of localized deformation marching from one end to the other. For materials without a sharp yield point—aluminum, brass, most high-strength steels—you use the 0.2% offset method. Draw a line parallel to the elastic slope starting at 0.2% strain. Where it intersects the curve is your yield strength. It's arbitrary by definition, but it's the standard and everyone uses the same standard so the numbers are comparable. After yield, strain hardening begins. The curve rises again. Dislocations multiply and tangle. The material gets harder to deform because the crystal lattice is full of defects that impede further dislocation motion. The peak of the curve is the ultimate tensile strength. Not the yield strength, not the fracture strength—the ultimate. This is where necking begins for ductile materials. Below UTS, the material strain-hardens faster than its cross-sectional area decreases, so it can still carry more load. Above UTS, necking accelerates and the engineering stress drops even though the true stress in the neck is still increasing.
That distinction between engineering stress and true stress is the single most important concept beginners miss. Engineering stress divides load by original area. True stress divides by the actual area, which is decreasing as the specimen stretches. After necking starts, the engineering curve goes down because the original area is a fixed reference point while the load is genuinely dropping. The true stress curve keeps rising until fracture. If you're doing finite element analysis or any simulation work, you always need the true stress-strain curve. Feeding the engineering curve into a solver past the UTS will make your model predict that the material suddenly becomes weaker in a way that violates conservation of energy. It looks like a numerical artifact but it's actually just using the wrong curve.
The Part Nobody Talks About—Fracture Toughness and Its Limits
The end of the Stress And Strain Curve is fracture. Ductile materials show significant necking and a cup-and-cone fracture surface. Brittle materials fracture with almost no plastic deformation—glass, cast iron, high-carbon steel that's been quenched and tempered improperly. The elongation at break is your ductility metric. Steel might give you 20 to 30 percent. Aluminum 10 to 25 percent. Ceramics basically zero. Here's something my experience has taught me that textbooks gloss over: the curve you get depends heavily on the specimen geometry and the loading conditions. A thin sheet will show different behavior than a thick plate of the same material because of plane stress versus plane strain. In thick sections, the constraint is higher, the yield point shifts up, and the material behaves more brittly. This is whyCharpy impact tests show a ductile-to-brittle transition in some steels at low temperature but a tensile test on the same material at the same temperature won't necessarily show it as dramatically. The constraint changes everything. I encountered this problem directly when a client sent me fracture samples from a pressure vessel that had failed at service temperature. The material was A516 Grade 70 steel, which should be perfectly ductile at room temperature. The tensile test came back normal—yield, UTS, elongation all within spec. But the failed vessel had cleavage fracture features. The answer turned out to be that the vessel was operating at about -20C, near the lower shelf of the transition region. The tensile curve at that temperature showed reduced ductility but still passed the minimum elongation requirement. The Stress And Strain Curve didn't predict the failure because it doesn't account for constraint effects or crack-tip plastic zone size. We needed a fracture mechanics approach—J-integral or K_IC testing—to understand what actually happened. The curve is necessary but not sufficient.

Common Pitfalls and What to Do About Them
Slippage in the grips is the most common experimental error. The specimen slips before the load cell registers any meaningful force, creating a false initial compliance. You'll see a curved bottom on your elastic region instead of a straight line. Use serrated grips, apply the correct grip pressure, and check that the specimen doesn't move more than 0.01mm during a preload hold. I've seen entire test reports thrown out because of grip slippage, and the root cause was usually that the operator tightened the grips by feel instead of using a torque wrench. Temperature drift matters more than people expect. A 10C change can shift yield strength by 2 to 5 percent in steel. If you're running comparative tests, do them in a temperature-controlled room and let the specimens equilibrate for at least 30 minutes before testing. Don't pull them straight out of a box that's been sitting in a cold warehouse. Alignment errors create bending stresses that compound as the specimen stretches. The official standard says misalignment should be less than 0.1 degrees, but in practice most shop-floor testing rigs don't achieve that. The result is asymmetric strain distribution across the gauge length and scatter in your data. If your replicate tests show coefficient of variation above 3 percent for yield strength, check alignment before you blame the material.
Another thing that catches people out: the Stress And Strain Curve from a hot-rolled specimen is different from one taken from the same material after cold working. Work hardening increases yield strength and reduces ductility. If you're specifying material properties for a design, make sure the test specimen represents the actual condition of the material in the finished part. A cold-formed bracket tested against a hot-rolled coupon will fail prematurely because the curves don't match the real microstructure.
When the Stress And Strain Curve Lies to You
The curve assumes uniform deformation across the gauge length. That assumption breaks down at high temperatures where creep becomes significant, in materials with strong texture where deformation localizes into shear bands, and in polymers where viscoelasticity makes the curve rate-dependent to an extreme degree. For polymers, the same material tested at 1 mm/min and 100 mm/min can give completely different curves—one brittle, one ductile. The Stress And Strain Curve isn't a fundamental property in those cases. It's a snapshot of behavior under specific conditions. If you need material data for high-temperature applications, you're better off with creep curves or stress-rupture data. If you're working with composites, the tensor nature of their stiffness means a uniaxial tensile test captures only one component. The curve exists but it's insufficient for design. In those cases, supplement it with microstructural analysis and multi-axial testing. The curve is a tool, not a verdict. Know its assumptions, know its limits, and it will serve you well. Ignore either and you'll get numbers that look right and lead you wrong.